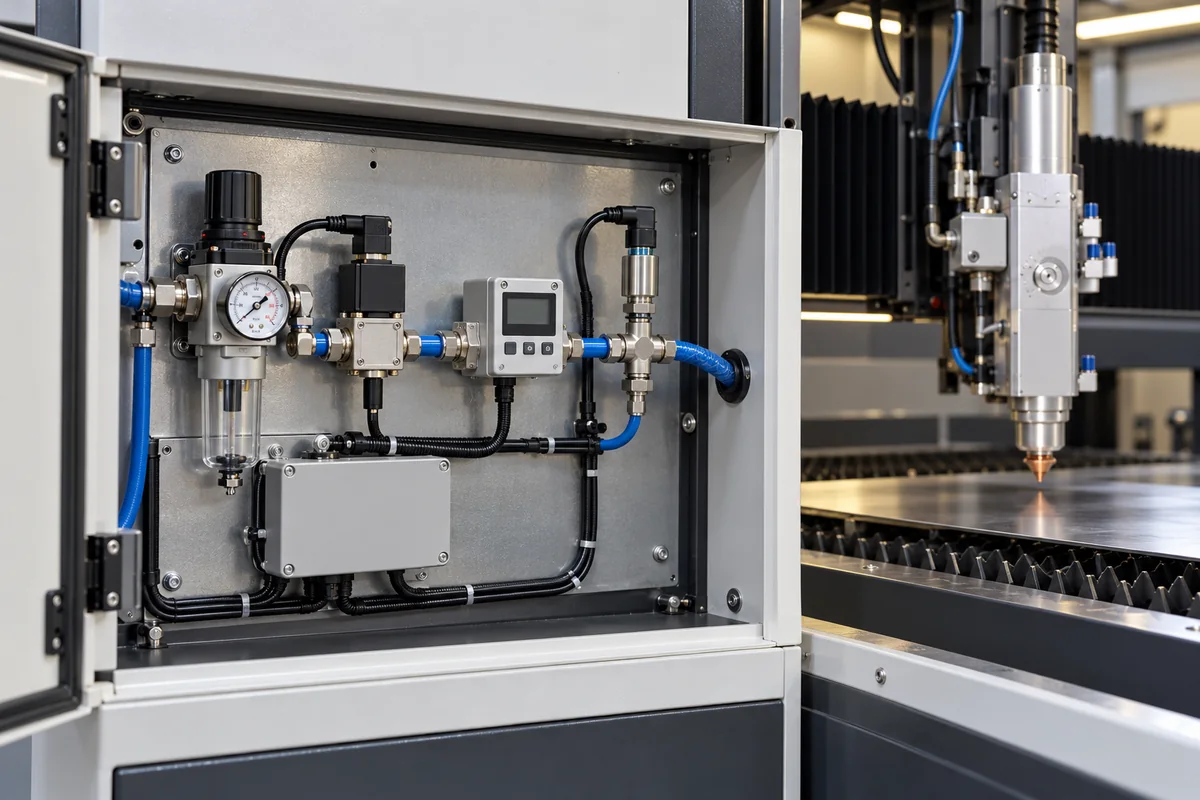
Define the gas path from the supply connection to the cutting nozzle
A laser-cutting assist gas system delivers the selected cutting gas to the cutting zone. Its supply connections, regulators, valves, piping, sensing and nozzle interface must meet the host machine’s cut-chart conditions. Define which assemblies the supplier provides and how the gas circuit communicates with the machine controls.
Integrated assist-gas supply, regulation, switching and delivery subsystems for laser-cutting machines, including the machine-side valves, sensing and cutting-head/nozzle interface. Upstream stand-alone gas panels are covered on page 9229; complete sheet laser cutters on page 440; semiconductor gas-stick assemblies on page 8995. Laser resonator gases and cutting-unit ventilation have separate duties.
CNFX editorial research · Sources checked October 19, 2026 · 3 sources
Assign the supply panel, machine circuit and nozzle interfaces
GCE’s published TDS panel page describes tank-fed oxygen/nitrogen supply using control and main pressure regulators. That upstream panel is one supply assembly; specify the machine-side delivery and control scope separately. [1]
Draw the gas path from the agreed supply connection through isolation, regulation, filtration where specified, switching valves and hoses to the cutting head. Mark supplier boundaries, connection sizes, pressure ratings and the locations of test points.
Identify the exact gas service for every path and component, including cleaning, seal and material compatibility requirements. Obtain the gas supplier’s and machine builder’s installation requirements; a material name alone does not establish suitability for oxygen service.
Specify the cutting-head and nozzle interface, including the nozzle identification and replacement scope. Keep any cutting-unit ventilation or other purge connection identified separately from the gas directed through the cutting nozzle.
02
Measure available pressure at the defined point while gas is flowing
The TruLaser 2030 (L82) installation chapter distinguishes flowing inlet pressure, maximum static inlet pressure and cutting gas pressure. Its supply guidance also addresses the combined demand of connected machines. Use the applicable machine revision for the installation. [3]
Record the required pressure and allowable variation at each agreed measurement point, with the gas, nozzle and flow condition stated. A shut-off gauge reading cannot establish the pressure available during a cut.
Ask the supplier to demonstrate the specified demand cycle, including cut starts and any simultaneous demand from other machines. Record inlet and downstream pressure traces, supply condition and the installed hose/pipe arrangement.
For flow results, state whether the volume is at line conditions or a defined reference temperature and pressure. Include the nozzle and operating pressure with the result, and identify any separate ventilation demand when sizing the source.
03
Define the CNC command, measured response and fault reaction
Specify the interface between the host CNC and the supplied gas circuit. Separate a valve’s electrical actuation result from the time taken for pressure at the agreed downstream point to reach and remain within its acceptance band.
Document gas selection, pressure commands, enable signals and status/fault feedback supported by the delivered hardware. Identify sensor locations and whether control is on/off, proportional or a closed loop implemented with the host controller.
Define the start event, target pressure, acceptance band, measurement point and sampling method for response tests. Include switching between the required operating states and the conditions for restarting after a gas fault.
Agree the machine’s response to low supply, a failed sensor or valve, and loss of control power. Validate the implemented reactions with the machine builder; a component data sheet alone does not validate the integrated sequence.
04
Keep the cutting process and auxiliary gas duties explicit
TRUMPF describes nitrogen or argon in fusion cutting as expelling melt and shielding the edge from air. Its TruLaser 2030 installation chapter separately specifies nitrogen for cutting-unit ventilation, regardless of the cutting gas. [2][3]
Select the cutting gas from the machine’s qualified material/thickness cut chart and the required edge condition. Confirm gas composition, impurity limits and delivery conditions with the machine and gas suppliers.
For compressed-air cutting, obtain the machine-specific air-quality and supply requirements. For a multi-gas assembly, document the approved services and switching sequence; do not infer interchangeability from matching ports.
Use a loaded production trial with the specified material, nozzle and recipe to accept the installation. Record the agreed edge-quality observations and process limits with the gas-circuit configuration.
05
Regulation, switching, sensing and delivery functions
This functional reference covers the gas path and its control interfaces. Obtain the actual assembly drawing; a separate flow meter, pressure-feedback loop or controller is included only where the delivered design provides it.
Function
Define for the supplied assembly
Evidence
Gas pressure regulator
Gas service, inlet conditions, outlet range and flow capacity.
Gas-specific rating and pressure/flow performance.
Solenoid / control valve
Isolation or modulation role, gas compatibility and command.
Valve identification, wiring and installed response test.
Flow meter, if fitted
Gas calibration, range, location and volume-reference conditions.
Calibration and measurement uncertainty.
Gas nozzle / head interface
Nozzle identification, connection and delivery path.
Head compatibility and cut-chart configuration.
Pressure sensor, if fitted
Location, range, accuracy basis and feedback use.
Calibration, signal mapping and fault handling.
Control electronics / host CNC interface
Command, gas selection, feedback and fault sequence.
Interface specification and integrated sequence test.
06
Specify the gas service and acceptance conditions
Bind every pressure, flow and response requirement to the same assembly drawing and operating cycle. Retain separate electrical, environmental and mechanical limits for the supplied scope.
Field
Define in the order
Acceptance evidence
Gas service and supply pressures
Approved gases, inlet flow/static limits and downstream test points.
Gas-specific component ratings and machine installation requirements.
Flow rate (L/min or stated basis)
Gas, nozzle, pressure, duty and volume-reference conditions.
Measured capacity at the agreed points and demand cycle.
Gas purity (%)
Gas identity, composition and individual impurity limits.
Gas specification and point-of-delivery verification method.
Response time (ms)
Command/start event, target, measurement point and settling band.
Pressure trace with stated sampling and supply conditions.
Pressure regulation accuracy (MPa or bar)
Setpoint, flow range, inlet variation and error definition.
Steady and transient results at defined test points.
Supply voltage (V)
Valves, sensors and control interface requirements.
Electrical schematic and delivered component ratings.
Power consumption (W)
Electrical scope and operating modes.
Mode-specific demand for the delivered assembly.
Operating temperature (°C)
Gas and ambient limits for the installed assembly.
Component limits and machine installation conditions.
Storage temperature (°C)
Storage, packaging and condensation restrictions.
Supplier storage and recommissioning instructions.
Ingress protection
Exposed components, connectors and installed enclosure.
Declared protection for the specified installation.
Wetted materials
Gas-contact metals, seals, cleaning and gas-service suitability.
Material/cleanliness records and approved service ratings.
Weight (kg)
Panel, valves, piping and mounting scope.
Assembly mass and mounting-load information.
Dimensions (L×W×H, mm)
Mounting envelope, service access and hose routing.
Controlled assembly and interface drawings.
07
Send the machine gas requirements and delivery boundary
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Request an assist-gas circuit matched to the laser cutter
Provide the machine’s gas installation requirements, cut-chart conditions and a marked supply boundary. Ask for the proposed gas path, service-rated components, CNC interface and installed pressure/flow evidence.
Sourcing Assist Gas System from China?
Tell us your specification and target quantity — we will match it against
manufacturer records and come back with the factories that fit.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Confirm who supplies the upstream connection, machine-side controls, sensing and cutting-head interface. Agree the integrated response and cut-trial acceptance with the machine builder and gas supplier. How we source and review
· Page last updated 19 October 2026
Buyer questions
Can an upstream supply panel rating define cutting-head pressure?
Specify the required pressure at the machine and downstream test points under the agreed flow condition. [1][3]
Does a closed-valve inlet gauge establish cutting capacity?
Verify flowing pressure with the required nozzle, demand cycle and supply configuration. [3]
Should cutting-unit ventilation be included in nozzle flow?
Record it as a separate duty and include its demand in the supply assessment where applicable. [3]
Can one purity value be used for every cutting gas?
Use the gas composition and impurity requirements specified for the actual machine and process. [3]
Sources and what still needs a direct check
Sources checked 2026-10-19. GCE describes an upstream supply panel; TRUMPF provides a fusion-cutting explanation and a model-specific installation example. Confirm current documentation for the exact delivered machine.