Stick welding · AWS A5.1 classification and E7018 H4R test minimums, current and diameter, low-hydrogen storage and holding ovens, exposure limits and redrying
A covered stick electrode supplies filler metal and flux for shielded metal arc welding of structural steel. Select the classification and diameter against the steel, joint and qualified welding procedure, then plan packaging and moisture control for the delivered brand. Classification test values describe weld metal under prescribed test conditions.
Covered (stick) electrodes for carbon and low-alloy structural steel, including low-hydrogen and rutile types. Plastic welding rods, carbide hardfacing rods, brazing rods, solid wires and electrode ovens themselves are outside this page.
CNFX editorial research · Sources checked October 18, 2026 · 6 sources
Match classification tests to the required weld procedure
AWS describes A5.1/A5.1M:2012 as establishing the requirements for classification of carbon steel electrodes for shielded metal arc welding: mechanical properties of weld metal, weld metal soundness and usability, plus weld metal composition, moisture content of low-hydrogen electrode coverings, standard sizes and lengths, marking, manufacturing and packaging, with optional supplemental requirements for improved toughness and ductility, lower moisture contents and diffusible hydrogen limits. The AWS store now lists that 2012 edition as historical. Low-alloy steel covered electrodes fall under A5.5/A5.5M:2022, which adds chemical composition and moisture tests of the low-hydrogen covering, with optional tests for absorbed moisture and diffusible hydrogen. Both use U.S. Customary and SI units independently of each other. [2][3]
Hobart 418’s revision 250225 sheet lists AWS A5.1 E7018 H4R and E7018-1 H4R, and AWS A5.1M E4918. Confirm the required classification, applicable standard edition and supporting documentation for the delivered product; listed approvals need their applicable scope and current records. [4]
Hobart’s sheet lists minimum tensile strength 490 MPa, yield strength 400 MPa, elongation 22% in its stated gauge length and Charpy energy 27 J at its printed temperatures of −30 °C and −45 °C. It lists diffusible hydrogen 4.0 mL/100 g as the AWS specification value, against a “typical” 2.9 mL/100 g test result. Its “typical” as-welded values include 518 MPa tensile strength, 413 MPa yield strength and 29% elongation; the sheet explicitly presents “typical” data without guarantee or warranty. [4]
Lincoln’s June 2015 Excalibur brochure gives E7018 H4R requirements of 400 MPa yield, 490 MPa tensile, 22% elongation, 27 J at −29 °C and 4.0 mL/100 g weld deposit maximum hydrogen. The E7018-1 H4R table gives its impact requirement at −46 °C. These are the temperatures printed by Lincoln, distinct from Hobart’s printed Celsius values. Use the required classification and unit system independently, as the AWS abstracts specify. Lincoln warns that its test results should not be assumed for a particular weldment. [5][2][3]
Request the lot documentation required by the order, welding procedure and applicable code. A data-sheet example or a percentage above a classification minimum does not establish the properties of the delivered lot or the finished structural joint. [4][5]
Ask for the classification printed on the electrode and packaging, the diffusible hydrogen designator (for example H4), the 'R' moisture-resistant suffix where exposure is long, and lot test certificates rather than illustrative values.
02
Set diameter, current and length
Hobart 418 runs on DCEP or AC. Its amperage ranges are 75–100 A for 3/32 in (2.4 mm), 90–150 A for 1/8 in (3.2 mm), 110–230 A for 5/32 in (4.0 mm), 150–300 A for 3/16 in (4.8 mm) and 270–380 A for 1/4 in (6.4 mm), with optimum settings of 90 A and 22.0 V, 130 A and 26.5 V, 170 A and 28.0 V, 220 A and 28.5 V, and 340 A and 32.0 V respectively. It advises reducing optimum amperage by 15% out of position, an arc length of less than half the electrode diameter, and does not recommend vertical-down. [4]
At the listed optimum parameters with DCEP, Hobart calculates deposition rates from 0.8 kg/h for 2.4 mm to 3.6 kg/h for 6.4 mm. Its calculation allows a 2 in stub loss. These values exclude the broader work cycle and do not establish deposited metal per shift. Its size table lists 355 mm length through 4.8 mm diameter and 457 mm length for 6.4 mm. [4]
Lincoln’s June 2015 Excalibur 7018 MR brochure lists 2.4–6.4 mm diameters, with 350 mm and 450 mm lengths. For 2.4, 3.2 and 4.0 mm, its respective DC+ ranges are 70–110, 90–160 and 130–210 A; AC ranges are 80–120, 100–160 and 140–210 A. These belong to that product and publication, not every E7018 electrode. [5]
Editorial arithmetic: assume the delivered consumable is Hobart 418 at 3.2 mm and apply only the sheet’s stated 15% reduction to its 130 A optimum for out-of-position work: 130 × 0.85 = 110.5 A, approximately 110 A. This is a calculated adjustment of the sheet value, not a qualified setting for a particular joint; use the approved welding procedure. [4]
03
Store low-hydrogen electrodes and limit exposure
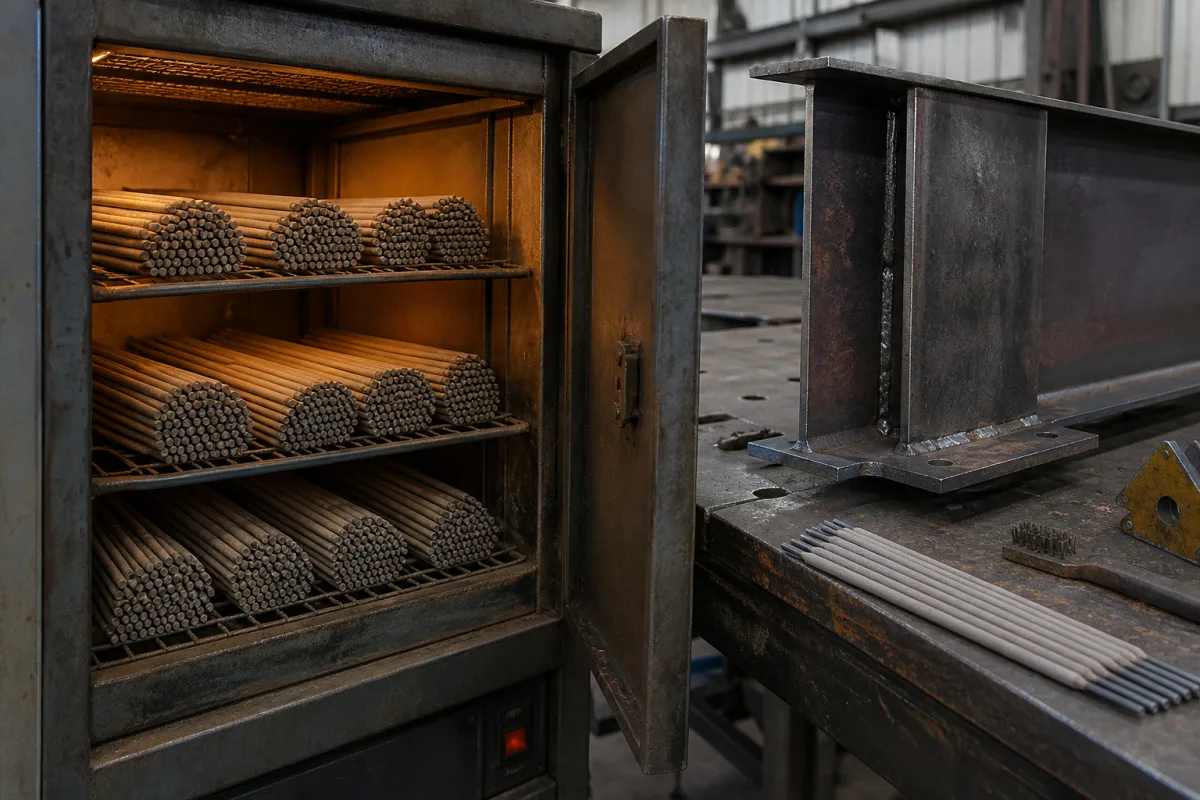
Lincoln Electric says stick electrodes that absorb moisture can cause cracking or porosity and poorer arc performance. Unopened hermetically sealed containers protect low-hydrogen electrodes; opened cans should be held in a cabinet at 250–300 °F (120–150 °C). Moisture in low-hydrogen coatings can cause hydrogen-induced cracking, particularly in steels of 80,000 psi (550 MPa) yield and above. Standard EXX18 electrodes should be issued to welders twice per shift, while moisture-resistant types with an 'R' suffix may be exposed for up to 9 hours; codes may set different limits. [1]
Lincoln describes rising effects of moisture: internal porosity found only by x-ray or destructive testing, then visible porosity, fluid slag, rough surfaces and difficult slag removal, and with severe pickup weld and under-bead cracking. Non-low-hydrogen electrodes from opened containers can be held at 100–120 °F (40–50 °C) if moisture is a problem. [1]
Hobart’s revision 250225 sheet prints an oven storage range of 220–350 °F beside 104–117 °C. Editorial unit check using °C = (°F − 32) × 5/9 gives approximately 104–177 °C for the Fahrenheit endpoints, so the printed ranges conflict. Obtain Hobart’s corrected instruction before setting the oven; the conversion is not a confirmed storage recommendation. The same sheet separately specifies one hour at 575 °F (302 °C) for reconditioning after extended exposure. [4]
Magmaweld’s information form instructs redrying of basic-covered electrodes before first use unless vacuum packed, using the manufacturer’s time and temperature, followed by controlled storage. Lincoln describes protection from its unopened hermetic containers. These are product-specific packaging and handling instructions; obtain the procedure for the actual supplied brand and pack condition. [6][1]
Lincoln’s twice-per-shift issue frequency does not specify a maximum exposure duration for each batch. Track the actual opening, issue and return times and apply the delivered product’s instructions and applicable code limits. The cited up-to-9-hour statement concerns Lincoln’s moisture-resistant types under its guidance. [1]
Give the supplier the steel grades and strength, code (e.g. AWS D1.1 or EN equivalents), classification and diameters, packaging (hermetically sealed or vacuum packed), moisture-resistant 'R' requirement, quantities, certificates and test reports, and storage conditions on site.
04
Use the delivered product’s redrying procedure
Lincoln’s MC22-140 guidance specifies one hour at the final redrying temperature and says longer time at a lower temperature is not equivalent. Its E7018/E7028 table gives 650–750 °F (340–400 °C) for electrodes exposed to air for less than a week without direct water contact. For direct water contact or high humidity it adds a 1–2 hour pre-dry at 180–220 °F (80–105 °C). Its separate E8018-and-higher instruction limits redrying to three one-hour cycles at 700–800 °F (370–430 °C). Apply the corresponding product and condition row. [1]
Lincoln’s non-low-hydrogen table does not recommend rebaking its listed E6010/E6011 fast-freeze products. Its listed E7024/E6027 fast-fill products have a different final-drying schedule of 400–500 °F (200–260 °C) for 30–45 minutes. Confirm any associated pre-drying conditions from that table. [1]
Magmaweld’s form describes a gradual temperature rise from a 100 °C furnace starting condition for its basic-electrode redrying example. Obtain its complete product-specific schedule. Lincoln separately requires electrodes spread out so each reaches temperature and describes rejection where excessive redrying damages the coating or changes handling/arc behaviour. [6][1]
Hobart’s one hour at 302 °C and Lincoln’s one hour at 340–400 °C are instructions from different manufacturers. Select the procedure for the delivered product, rather than combining the two ranges or treating their difference as a universal E7018 allowance. [4][1]
05
Xiang’s covered carbon-steel electrode range
Xiang lists covered E6013, E7016 and E7018 electrodes, separately from MIG and submerged-arc wire. Specify the delivered classification, sizes and pack condition, with the required lot documentation and that product’s storage instructions. The Hobart and Lincoln data-sheet values are separate reference examples.
06
Core, coating, packaging and moisture-control equipment
Part
Role
Fix in the order
Core wire
Carbon steel electrodes under A5.1; low-alloy under A5.5. [2][3]
Wire grade and diameter.
Flux coating
Shields the arc; basic coverings absorb moisture and must stay dry. [1][6]
Coating type and moisture limit.
Classification
E.g. E7018 H4R, metric E4918; 'R' suffix for moisture resistance. [1][4]
Classification, H designator and suffix.
Packaging
Hermetically sealed or vacuum packs protect from moisture. [1][6]
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Xiang Welding Industrial Co Ltd
TBC
Lists covered AWS E6013, E7016 and E7018 electrodes, separately from MIG and SAW wires. Confirm the delivered designation and its handling instructions.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How should opened low-hydrogen electrodes be stored?
Lincoln’s guidance gives 250–300 °F (120–150 °C) for opened cans of its low-hydrogen electrodes. Obtain the delivered brand’s instruction; Hobart 418’s printed storage-unit ranges conflict and need clarification. [1][4]
How long can E7018 electrodes be out of the oven?
Lincoln gives a twice-per-shift issue frequency for standard EXX18 and up to 9 hours for moisture-resistant types, subject to code requirements. Issue frequency alone does not establish a batch exposure-time limit. [1]
How are E7018 electrodes redried?
Use the delivered brand’s procedure. Lincoln’s table gives one hour at 340–400 °C for its E7018/E7028, with specified pre-drying for water contact or high humidity; Hobart 418 separately states one hour at 302 °C after extended exposure. [1][4]
What do H4 and R mean in E7018 H4R?
Lincoln’s Excalibur sheet lists a maximum 4.0 mL/100 g weld deposit for its H4 requirement; Lincoln’s storage guidance describes the R suffix as resistance to moisture pickup. Obtain the classification and required test documentation. [5][1]
Sources and what still needs a direct check
Sources checked 2026-10-18. Lincoln Electric, Hobart and Magmaweld are welding consumables makers; their storage, redrying and operating figures are for their own products, and codes may set different limits. AWS store abstracts describe what the A5.1 and A5.5 specifications cover; the specifications themselves were not reviewed.