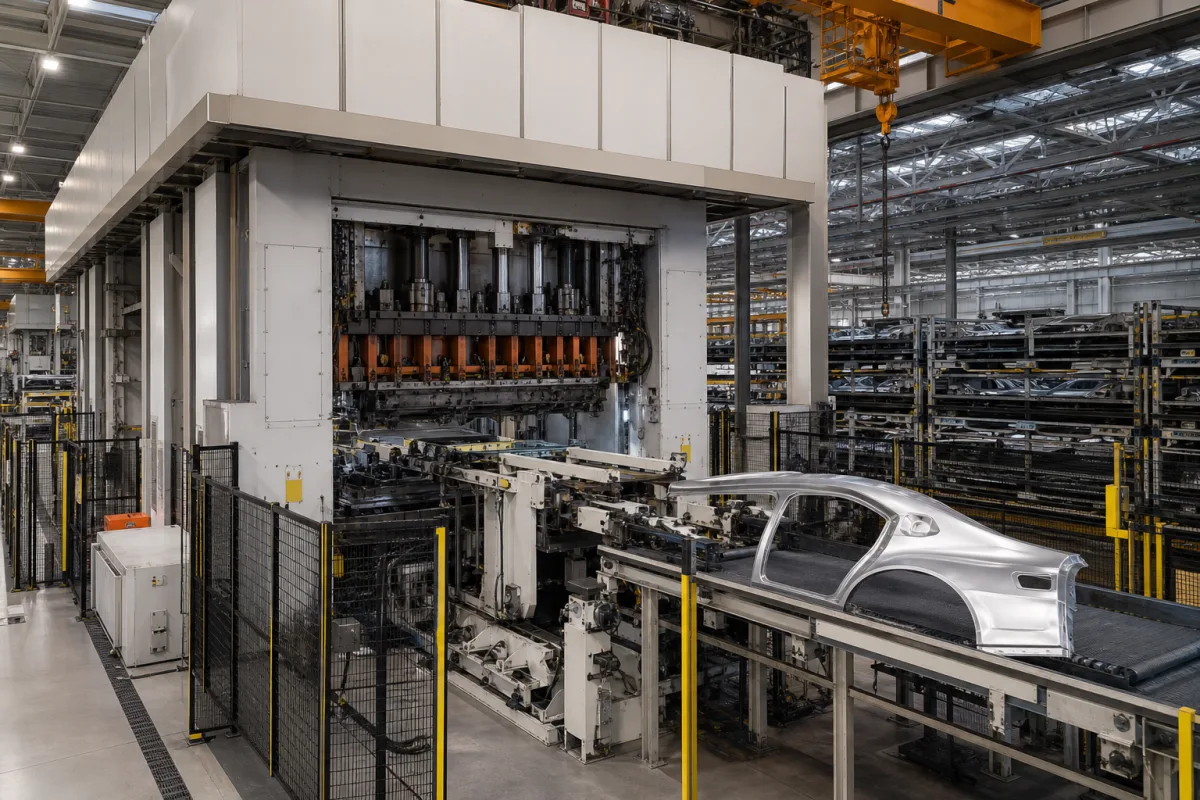
Automotive body panel stamping press (draw press with die cushion, single press or tandem line)
Draw presses for car body panels · hydraulic press speeds and table, servo tandem lines in strokes per minute, die cushion force and response
An automotive body panel stamping press draws and forms doors, hoods, fenders, roofs and body sides from sheet, with a die cushion holding the blank edge while the slide draws it into the die. It may be a single hydraulic press for low volumes and tryout or a line of mechanical or servo presses with automated transfer for production. Ask three things first: the draw depth and table size the largest panel needs, how the die cushion force is controlled at the start of the draw, and how many strokes per minute the press or line must reach.
Presses and press lines for drawing and forming car body panels: hydraulic draw presses with die cushions, and mechanical or servo tandem and transfer lines. General-purpose hydraulic presses are covered on the Hydraulic press page; press brakes, forging presses and stamping dies as separate tooling are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
PDH describes its 630T hydraulic press for car body panels, built for stretching, pressing and bending door panels and other sheet parts, as a three-beam, four-column, four-nut design (a frame version is offered), with welded and annealed Q355B beams, hard-chromed 45 steel columns and two-stage slide speed: fast for the no-load approach and slow for drawing. For the 630T model its table gives a liquid pressure of 25 MPa, an effective slide stroke of 900 mm, an opening height of 1,500 mm, a worktable of 1,600 × 1,600 mm, a lowering speed of 150 mm/s, a pressing speed of 9-18 mm/s, a return speed of 150 mm/s, 45 kW motor power and a 1,000 kN ejector with 300 mm stroke. [1]
For high-volume production, a paper by Honda, Honda Engineering and AIDA describes a tandem press line of four servo presses and servo feeders for deep-drawn body panels that reaches a maximum of 18 strokes per minute (SPM), which it states was not possible with conventional press lines; the presses were developed to run at 27 SPM in continuous mode with a 1,100 mm slide stroke, the highest-capacity draw press is rated at 23,000 kN and driven by four servo motors, and the line is reported to use over 30% less energy in production than a conventional mechanical press line. [2]
Editorial calculation: on the 630T table, an assumed cycle of 700 mm approach at 150 mm/s (about 4.7 s), 200 mm of drawing at 9-18 mm/s (about 11-22 s) and a 900 mm return at 150 mm/s (6 s) takes roughly 22 to 33 s, or about 2 to 3 strokes per minute, against 18 SPM for the servo line described; 630 tonnes-force is about 630 × 9.81 ≈ 6,180 kN, about a quarter of the 23,000 kN draw press. Use your own draw depth and approach distance, and ask for the cycle time the supplier guarantees. [1][2]
Give the supplier the panels (largest size, material and thickness, draw depth), required force and die cushion force, table and opening sizes, stroke and speeds, output in parts per hour or strokes per minute, single press or line, automation and die change, energy supply, foundation and quantity.
02
Control the die cushion force at the start of the draw
An AIDA patent on die cushion force control (US 9,707,612 B2) states that a servo die cushion needs a force response time of about 0.03 to 0.1 second to raise the force from the load that balances the moving mass of blank, blank holder, cushion pins and pad to the set die cushion force, which it describes as "from several times to several tens times larger". If the press slide has already started drawing during that delay, the force pressing the blank edge is insufficient at the beginning of the draw and wrinkles form radially from the edge. [3]
In the Honda line, the die cushion of the draw press uses a hybrid motorized hydraulic system with NC controls, with small high-speed servo motors controlling the pressure in hydraulic cylinders so that the cushion pressure can track the press motion for deep drawing. [2] PDH's 630T table lists an ejector force of 1,000 kN for that hydraulic press. [1]
Editorial calculation: at a slide speed of 300 mm/s at cushion contact (an assumed value), a 0.03 to 0.1 s force response lets the slide travel 300 × 0.03 = 9 mm to 300 × 0.1 = 30 mm before full cushion force, which is the drawing distance at risk of wrinkles described in the patent; ask how the supplier's cushion avoids that delay, for example by preliminary acceleration or pressurisation. [3]
03
PDH hydraulic body-panel presses and World Group stamping presses
PDH lists the 630T car body panel press, with custom models from 100 to 3,000 tons in four-column or frame designs; World Group lists automotive stamping press machines among its power and hydraulic presses. Ask each for table size, stroke, speeds and die cushion data for your panels.
04
Frame, slide drive, die cushion and transfer of a draw press
The die cushion holds the blank edge under a set force at the start of the draw; if that force builds too late, wrinkles form from the edge.
Component
Role
Fix in the order
Frame (four-column or frame type)
Carries the force; frame resists off-centre loads. [1]
Type and deflection.
Slide and drive
Hydraulic two-speed slide or servo crank drive. [1][2]
Stroke, speeds, drive.
Die cushion
Holds the blank edge; force must rise without delay. [3][2]
PLC on one press; synchronized servo control in a line. [1][2]
Control and safety.
05
Tonnage, stroke, strokes per minute and bed size for panel drawing
The published examples run from a 630 t hydraulic press with a 1,600 × 1,600 mm table to a 23,000 kN servo draw press, so state stroke and strokes per minute for the panel, not tonnage alone.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How fast can a servo press line draw body panels?
A Honda and AIDA paper reports a four-press servo tandem line reaching a maximum of 18 strokes per minute. [2]
What speeds does a hydraulic body panel press run at?
PDH lists 150 mm/s lowering, 9-18 mm/s pressing and 150 mm/s return for its 630T model. [1]
Why does die cushion response time matter?
An AIDA patent states a 0.03 to 0.1 s delay in building cushion force can leave the blank edge under-held at the start of the draw and cause wrinkles. [3]
How much energy can a servo press line save?
The Honda line is reported to use over 30% less energy than a conventional mechanical press line. [2]
Sources and what still needs a direct check
Sources checked 2026-10-12. PDH is a press maker describing its own model; the AIDA paper describes a line built with Honda; the AIDA patent describes die cushion control. Figures apply to the machines named.