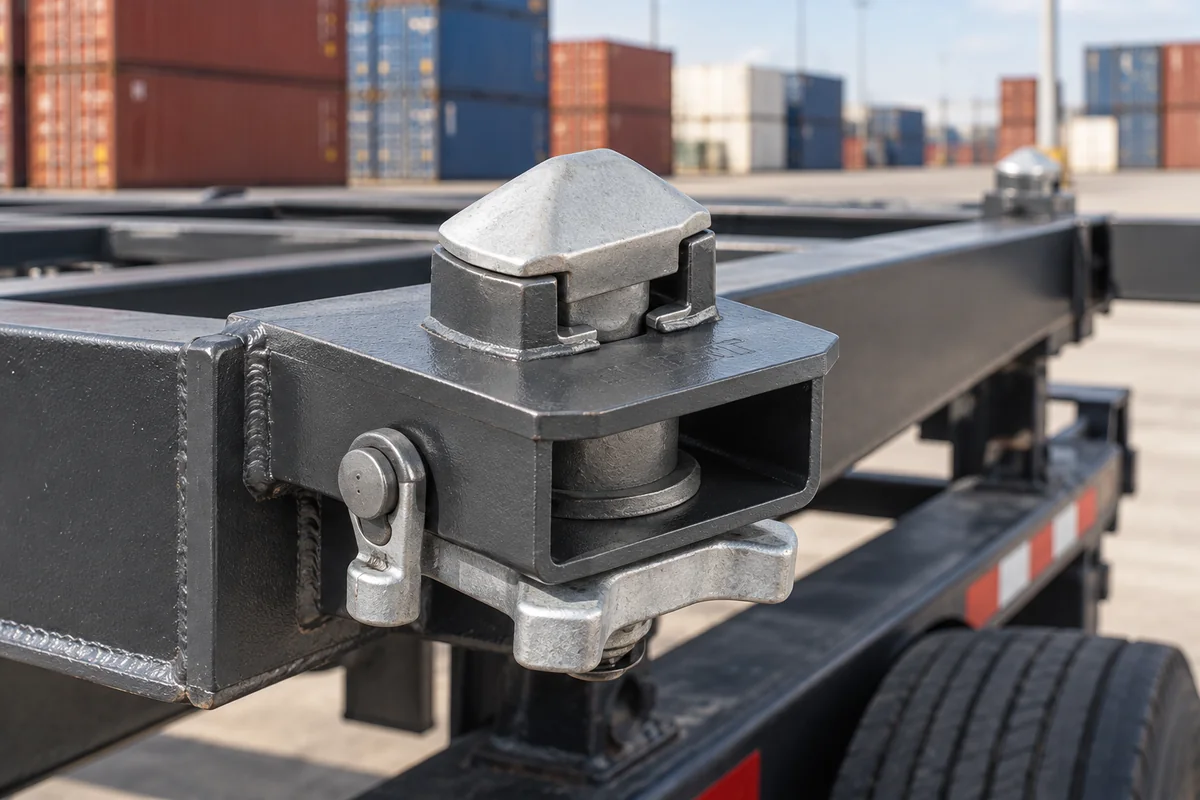
Container corner fittings (corner castings) · ISO 1161 interface, cast carbon steel chemistry and heat treatment, tensile and Charpy requirements, lot testing and certification, and how containers may be lifted by their fittings
Container fittings, or corner castings, are the cast steel blocks at the corners of a freight container whose standard apertures and faces let cranes, spreaders, twistlocks and lashings lift, stack and secure it. Ask three things first: which fitting type and ISO 1161 interface you need, what steel, heat treatment and mechanical tests the castings must meet, and which certification body will survey them.
Cast steel corner fittings (top and bottom, left and right) and intermediate fittings for ISO series 1 freight containers and similar boxes, sold to container builders and repairers. Twistlocks, lashing bars, spreaders and complete containers are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
The ABS Rules for Certification of Cargo Containers (1998) define a corner fitting as a fixture with standard apertures and faces giving a shared interface for handling and securing containers, and in Section 14 set requirements for carbon steel corner castings, accepting special designs only if their strength is not less than ISO 1161 requires. Castings are to be fully annealed, normalised, or normalised and tempered; steel is limited to 0.25% carbon, 1.20% manganese (more allowed if C + Mn/6 ≤ 0.45%), 0.80% silicon, 0.06% sulphur and 0.05% phosphorus. Each heat-treatment lot is tension tested to ASTM A370 for at least 450 N/mm² (65 ksi) tensile strength, 240 N/mm² (35 ksi) yield, 22% elongation in 50 mm and 30% reduction of area, and each heat is Charpy V-notch tested at −20 °C for an average of at least 20 J (15 ft·lb). [1]
Certification may be by heat-treatment lot with surveyor-witnessed tests, or under a quality-assurance programme; the application must include material specifications, manufacturing process, detail drawings and a test agenda, and the container builder must make certified mill test reports for the corner fittings available to the surveyor. [1]
Editorial calculation: a heat with 0.20% C and 1.40% Mn exceeds the 1.20% Mn limit but gives C + Mn/6 = 0.20 + 0.23 = 0.43%, within the 0.45% allowance. [1]
Bloxwich Group, a UK container parts maker, shows how corner castings are ordered and certified in practice. It supplies castings conforming to ISO 1161 for dry freight containers, reefers, open tops, tank containers and offshore containers, as four position-specific parts — bottom left (BCP14377), bottom right (BCP14378), top left (BCP14379) and top right (BCP14380) — and as lower, upper, end and complete sets, a complete set for one container being two of each, eight castings in all. The castings come with an EN 10204:2004 type 3.2 certificate, which Bloxwich equates to 3.1C in ISO 10474, and it advises the buyer or builder to have the batch certificates pre-approved by the end certifier (for example DNV, Lloyd's Register, ABS or Bureau Veritas) before welding the castings to any structure, since the user must demonstrate compliance to that certifier. [3]
Editorial calculation: an order for 25 containers needs 25 × 8 = 200 castings — 50 of each of the four positions — plus any spares; state the inspection-certificate type (such as EN 10204 3.2) and the certifying society in the enquiry so that the lot tests under the ABS rules above can be witnessed accordingly. [3][1]
Give the supplier the fitting types and positions (top/bottom, left/right, intermediate), the ISO 1161 edition or drawing, steel specification and heat treatment, mechanical and Charpy test requirements, certification society and survey method, marking, finish (primed or bare), quantity per heat lot, and test certificate format.
02
Understand how containers are lifted by their fittings
OSHA's marine terminal rule 29 CFR 1917.71 requires containers to be handled using lifting fittings or other arrangements intended for the purpose. Loaded containers of 20 ft or more lifted by top fittings must have lifting forces applied vertically from at least four fittings, with less-than-vertical lifts allowed only for sound ISO closed boxes within stated limits (lift angle 80–90°, at least 2.5 m between beam and load, spreader length at least 5 m for 20 ft and 11.1 m for 40 ft). When lifted from bottom fittings, the connections must bear only on the fittings, with bridle legs at no less than 30° to the horizontal for 40 ft, 37° for 30 ft and 45° for 20 ft containers. Twistlock systems must be designed so a suspended load cannot be released accidentally. [2]
The ABS rules also note that the reactions of a stack of containers are taken through the four bottom corner fittings of the lowest container, which is why corner fitting strength and attachment to the frame receive special attention during container manufacture. [1]
03
State which edition of ISO 1161 the castings follow
ISO 1161:2016, Series 1 freight containers — Corner and intermediate fittings — Specifications, "establishes the basic dimensions and the functional and strength requirements of corner and intermediate fittings for series 1 freight containers", meaning containers that conform to ISO 668 and ISO 1496, except air mode containers covered by ISO 8323. It is the fifth edition, published on 11 July 2016, and replaced ISO 1161:1984, titled Corner fittings — Specification, together with its 1990 corrigendum and 2007 amendment. A further revision is listed as a draft. [4]
The ABS rules this page already cites date from 1998 and accept special designs only if their strength is not less than ISO 1161 requires [1], which at that time meant the 1984 edition, titled for corner fittings only; the 2016 edition names intermediate fittings in its title [4]. Ask the foundry which ISO 1161 edition its drawings and strength tests follow, and whether the classification society approving the container accepts that edition.
OSHA's terminal rule requires loaded containers lifted by their top fittings to be lifted vertically from at least four fittings [2], and the 1984 edition describes its dimensions as design details "vital to container interchange in automatic, semi-automatic and conventional systems" [4]. Ask for dimensional inspection of the castings against the ISO 1161 drawing as well as the mechanical test certificate.
Editorial calculation: ISO 1161:1984 stayed current from 1 December 1984 to 11 July 2016, about 31.6 years, and its 2007 amendment came 23 years after first publication. [4]
Item
ISO 1161:1984 (edition 4)
ISO 1161:2016 (edition 5)
Title scope
Corner fittings
Corner and intermediate fittings
What it fixes
Basic dimensions; functional and strength requirements; design details vital to interchange in automatic, semi-automatic and conventional systems
Basic dimensions; functional and strength requirements
Containers covered
Series 1, except air mode
Series 1 to ISO 668 and ISO 1496, except air mode (ISO 8323)
Published / withdrawn
1 December 1984 / 11 July 2016
11 July 2016 / current
Changes recorded
Cor 1:1990; Amd 1:2007
New revision in draft
Values are from the Standard Norge catalogue pages for ISO 1161:2016 and ISO 1161:1984; the dimension tables were not reviewed.
04
Trace the fitting features
This is a functional reference built from the sources cited; it is not one maker's design.
Fill the specification fields with values for your fittings
A corner fitting quotation needs values for your order. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Field
What it means and published values
Ask the supplier for
Fitting Type
Top/bottom, left/right, intermediate; 8 corner castings per container. [1][3]
Drawing per type.
Standard
ISO 1161 interface and strength [1]; current edition ISO 1161:2016 (corner and intermediate fittings). [4]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 12 October 2026
Under the ABS rules, carbon steel with at most 0.25% C and 1.20% Mn, annealed or normalised, with at least 450 N/mm² tensile and 240 N/mm² yield strength. [1]
What impact toughness do corner castings need?
ABS requires an average Charpy V-notch energy of at least 20 J at −20 °C from three specimens per heat. [1]
How must loaded containers be lifted by their fittings?
OSHA 1917.71 requires vertical lifts from at least four top fittings, or bottom-fitting bridles at not less than 30°–45° to horizontal depending on length. [2]
How many corner castings does one container need?
Eight: Bloxwich Group's complete set is two each of bottom left, bottom right, top left and top right castings, supplied with EN 10204 3.2 certificates. [3]
Which standard defines container corner castings?
ISO 1161:2016 establishes the basic dimensions and functional and strength requirements of corner and intermediate fittings for series 1 freight containers (ISO 668 and ISO 1496), replacing the 1984 edition. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. The ABS rules are a classification society's certification rules (1998 edition reviewed); OSHA's rule is a US federal requirement; Bloxwich Group describes how it supplies and certifies its own castings. ISO 1161 itself is not freely available.