Case Forming and Drawing Press
View system integration details
This page explains how Forming Die Set is classified within Machinery and Equipment Manufacturing. Technical values and manufacturer relationships are research references; confirm the current specification and supplier evidence for each order.
A precision tool assembly used in metal forming processes to shape sheet metal into specific geometries through pressing operations.
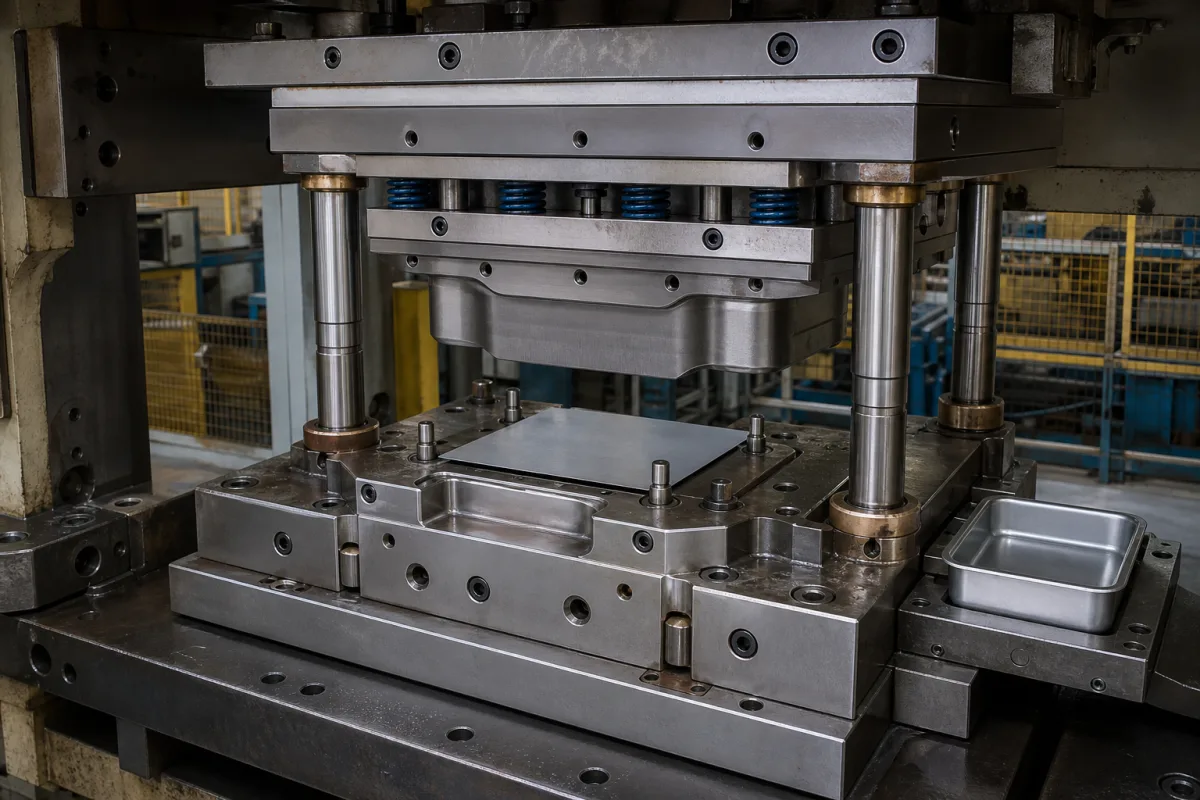
Technical details and manufacturing context for Forming Die Set
| Parameter | Typical range | Notes & selection driver |
|---|---|---|
| Die Height | 150–400 mm | Determines press shut height compatibility |
| Die Set Weight | 500–3000 kg | Affects handling and press capacity |
| Working Area | 300×300–800×800 mm | Defines maximum part size |
| Operating Pressure | 1.0–1.6 MPa | |
| Maximum Force | 50–200 kN | Must exceed forming force requirement |
| Stroke Length | 50–150 mm | Determines draw depth capability |
| Guide Pillar Diameter | 20–50 mm | Affects alignment accuracyGB/T 2861.1 |
| Guide Pillar Count | 2–4 pcs | More pillars improve stability |
| Parallelism Accuracy | ±0.02 mm | Ensures uniform part thicknessISO 1101 |
| Surface Hardness | 58–62 HRC | Wear resistance for long service lifeASTM E18 |
| Material Grade | Cr12MoV | High carbon chromium steel for durabilityGB/T 1299 |
| Operating Temperature | -20–80 °C | Outside range may affect material properties |
Ranges are indicative industry figures for RFQ preparation, not a supplier commitment. Confirm every value and standard with the legal manufacturer before ordering.
| pressure: | Up to 1000 MPa (145,000 psi) depending on die material and construction |
| other spec: | Sheet thickness range: 0.5-6.0 mm (0.02-0.24 in); Cycle rate: Up to 60 strokes/minute for precision applications |
| temperature: | Ambient to 200°C (392°F) for standard tool steels; up to 500°C (932°F) with high-temperature alloys |
Indicative industry ranges for design and RFQ preparation. Confirm the exact figures and applicable standard with the manufacturer before specifying.
Quoted from the published standard.
A practical evidence checklist for RFQ preparation and supplier evaluation.
Compare the published product scope and source details, then include your specifications and quantity in an enquiry.
Manufacturer profiles associated with Forming Die Set.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.
Common materials include tool steel, carbide, and high-speed steel, as listed in the directory. The specific material grade, such as Cr12MoV, should be confirmed with the manufacturer for the intended application.
Selection depends on press shut height, required forming force, part size, and draw depth. Reference parameters like die height (150–400 mm), maximum force (50–200 kN), and working area (300×300 to 800×800 mm) provide a starting point, but verify with the press specifications and manufacturer.
Relevant standards include GB/T 2861.1 for guide pillar diameter, ISO 1101 for parallelism accuracy, ASTM E18 for surface hardness, and GB/T 1299 for material grade. These are verification references, not proof of compliance.
Signs include reduced part quality, wrinkles or tears in formed parts, misalignment, excessive noise, or visible surface damage. Regular inspection of guide pillars, die surfaces, and parallelism accuracy is recommended. Operating beyond rated force or temperature can accelerate failure.
This component is essential for the following industrial systems and equipment:
Editorial classification, named public sources where available, and source-reviewed manufacturer records.
Compare manufacturer profiles with relevant product and process capability.