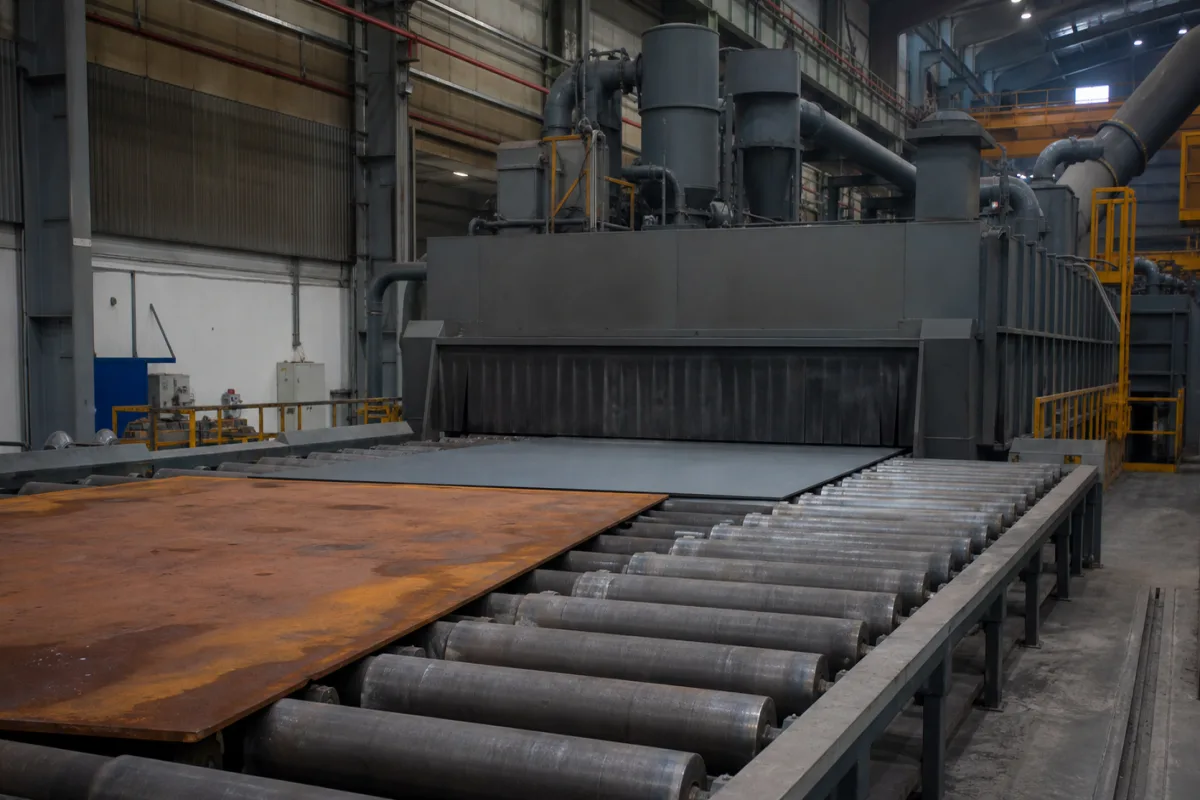
Hull plate preservation line: preheat, blast to Sa 2½ and shop-prime steel plates for shipbuilding
Shipyard plate preservation line · preheating, wheel blasting to Sa 2½ with a 30–75 µm profile, zinc silicate shop primer at about 15 µm and drying, set against the IMO coating standard for ballast tanks
A shipyard does not blast hull steel once: plates are blasted and given a thin, weldable shop primer as they arrive, then cut, welded into blocks and given their full coating system months later. The plate preservation line that does the first step is a chain of preheating, wheel blasting, cleaning, automatic spraying and drying on one conveyor. What it has to achieve is set less by the blast machine than by the coating rules the plates must later meet — for ballast tanks, the IMO Performance Standard for Protective Coatings — and by the shop primer's own application window.
Plate preservation (pretreatment) lines in shipyards and steel service centres that preheat, wheel-blast, clean, shop-prime and dry steel plates for hull construction, with the surface requirements the primed plate must meet. Single wheel blast machines, blast wheel sizing and abrasive flow for plates, sections and loose parts are covered on the Wheel shot blasting machines page, and wheel shaft bearings on the Wheel drive shaft and bearings page. Air-nozzle blasting of erected blocks, secondary surface preparation equipment and the main hull coating system are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
Primary surface preparation under IMO PSPC: Sa 2½, 30–75 µm profile, 50 mg/m² salt and the weather limits
IMO resolution MSC.215(82), the Performance Standard for Protective Coatings (PSPC), covers dedicated seawater ballast tanks in ships of 500 gross tonnage and above and double-side skin spaces of bulk carriers. It defines a shop primer as the prefabrication primer applied to steel plates, naming automatic plants as one place it is applied, and its table 1 sets the primary surface preparation that such a plant performs. [1]
The last row is why the choice of shop primer on the plate line matters to the coating budget: a pre-qualified zinc silicate shop primer can be kept and only sweep-blasted or washed at the block stage, while one that is not must be blasted off to at least 70% before the ballast-tank coating goes on. [1]
Editorial note: the humidity and dew-point limits apply at the blast machine, so a line that brings cold plates in from outdoor storage needs plate temperature measured at the blast inlet, not only in the hall.
Relative humidity above 85%, or steel surface temperature less than 3 °C above the dew point [1]
Water-soluble salt
Limit equivalent to ≤ 50 mg/m² of sodium chloride [1]
Shop primer
Zinc-containing, inhibitor-free zinc silicate based or equivalent; compatibility with the main coating confirmed by the coating manufacturer [1]
Records before blasting
Steel surface temperature, relative humidity and dew point measured and recorded before blasting starts and when the weather changes suddenly [1]
Checks on the plate
Plates tested for soluble salt and checked for oil, grease and other contamination; cleanliness monitored in the shop-primer process [1]
Later, at the block stage
Sa 2 removing at least 70% of intact shop primer unless the shop primer passed pre-qualification with the epoxy system; Sa 2.5 on damaged shop primer and welds [1]
02
Preheat oven, eight-wheel blast, cleaning, airless spraying and drying tunnel on a Pangborn plate line
Pangborn's description of a preservation line built for a Russian shipyard gives a station order that the plate passes without being handled by hand. The line takes plates up to 250 mm thick and 4,500 mm wide at 2.5–3 m/min, depending on how much scale they carry, and blasts to Sa 2.5. [2]
Editorial calculation: a 4,500 mm wide plate at 3 m/min presents 13.5 m² of top surface a minute, 810 m² an hour; primed on both faces that is 1,620 m² an hour of shop primer. [2]
Station
Published detail
Preheating oven
Plates warmed to about 35 °C so the primer's solvent leaves faster; oven heated to 280 °C by gas burners in ceramic-clad burner pipes, heat by convection fans and/or flame ledges [2]
Intermediate conveyor
Visual check; sensors detect plate height and width and set blasting capacity and cleaning automatically [2]
Shot blast machine
8 blast wheels arranged in space for uniform coverage; abrasive recycled through a gravity air-wash separator; wear areas lined with hardened manganese steel [2]
Cleaning station
Brushes and nozzles with blow-off fans remove abrasive; brushes clean the underside [2]
Painting station
Light barriers rescan plate height; upper airless guns move on dust-insensitive linear axes to about 200 mm from the plate; upper and lower guns have scanning units so only the plate is sprayed; designed to EN 12215; extraction to a filter [2]
Solvent treatment
Regenerative thermal oxidiser (RTO), designed to run nearly autothermally [2]
Chain conveyor and drying tunnel
Parallel chains with traverses touch the wet underside only at points; drying tunnel reuses warm exhaust air from the preheating oven, with an optional gas burner [2]
03
The 15 µm zinc silicate film the spray station lays down, and the abrasive that suits it
AkzoNobel's data sheet for Interplate 997, a two-pack heat-resistant zinc silicate shop primer for newbuilding, states that shop primers should be applied with automatic blasting and spraying equipment and is not recommended for manual spray application. [3]
Editorial calculation: at 16.67 m²/litre, the 1,620 m² an hour from the line example above needs about 97 litres of mixed primer an hour before loss factors. [3][2]
Two humidity limits pull in opposite directions here: PSPC stops blasting above 85% relative humidity, while this primer cures slowly below 50%. [1][3] Ask the line maker how the drying tunnel compensates when hall air is dry, and ask the primer maker for the cure time at the line's plate temperature.
Item (Interplate 997)
Published value
Blast standard
Minimum Sa 2½ (ISO 8501-1:2007); SSPC-SP10 may be used in North America [3]
Abrasive
Steel grit 0.6–1.0 mm, or a mix of that grit with steel shot 0.6–1.4 mm, to give a profile in which angular grit marks dominate [3]
16.67 m²/litre at 15 µm dft, before loss factors [3]
Airless spray
Tip 0.48–0.58 mm; fluid pressure at the tip not less than 60–100 kg/cm² [3]
Limits
Cure retarded below 50% relative humidity; higher film thickness may affect welding and cutting; apply before the blasted steel oxidises, or reblast [3]
Heat and welding
Corrosion protection stated even after heating up to 800 °C; Lloyd's Register weld quality approval of prefabrication primers as part of an approved scheme [3]
04
Data for a plate preservation line enquiry
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Plates: [max width; max length; thickness range; mill scale condition]
Output: [plates or m² per shift; line speed]
Surface: [blast grade; profile range; salt limit; PSPC applicability]
Abrasive: [grit, shot or mix; size]
Primer: [product; dry film thickness; both faces; pre-qualification status]
Preheat and drying: [plate temperature; fuel; exhaust reuse]
Emissions: [solvent treatment; dust collection]
Inspection: [temperature, humidity and dew-point logging; salt and profile checks]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What surface does IMO PSPC require on blasted hull plate?
Sa 2.5 with a 30–75 µm profile, soluble salt equivalent to ≤ 50 mg/m² NaCl, and no blasting above 85% RH or when steel is less than 3 °C above the dew point. [1]
Why are plates preheated before blasting and priming?
In Pangborn's shipyard line, plates are warmed to about 35 °C in a 280 °C gas-fired oven so the primer's solvent leaves faster. [2]
How thick is a zinc silicate shop primer?
AkzoNobel's Interplate 997 is applied at 15 µm dry (60 µm wet), covering 16.67 m²/litre before losses. [3]
Does the shop primer have to be removed later?
Under PSPC, at least 70% of intact shop primer is removed to Sa 2 unless it passed pre-qualification with the epoxy system. [1]
Sources and what still needs a direct check
Sources checked 2026-10-12. Surface requirements come from IMO resolution MSC.215(82); the line description from Pangborn's article on a preservation line for a Russian shipyard; shop primer and abrasive data from AkzoNobel's Interplate 997 data sheet.