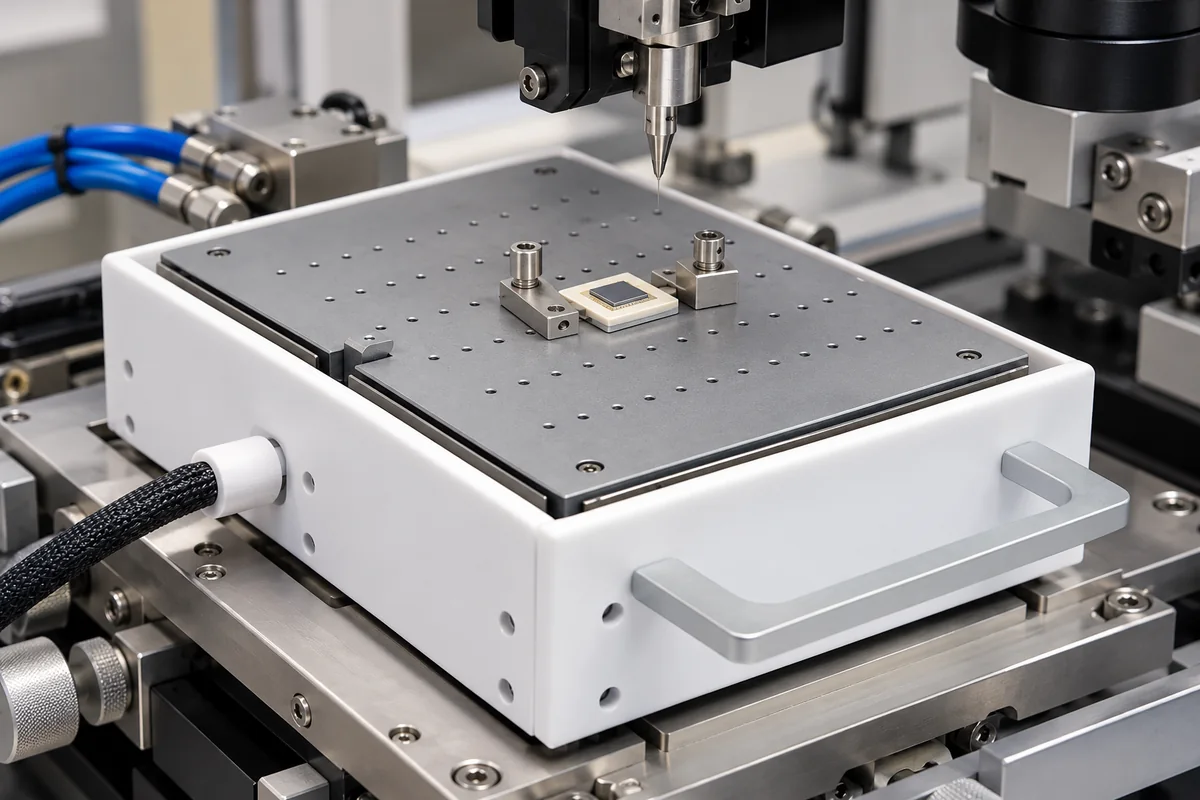
Hold the substrate securely and verify temperature where the bond is made
A wire-bonding heater stage supports and heats the substrate or package while the bonder makes the interconnections. Its workholding surface, clamp or vacuum arrangement and installed height must fit the part and bonder. Specify the thermal requirement at the loaded workpiece as well as the stage and controller ratings.
Heated substrate/package workholders and interchangeable heater stages for wire-bonding machines, including their top plates, clamping/vacuum interfaces and temperature-control connections. Complete wire bonders are covered on page 8639. Underfill/adhesive dispensing preheat zones on page 3511, ovens, microscope hot stages and capillary/tool heaters have separate supply scopes.
CNFX editorial research · Sources checked October 19, 2026 · 3 sources
Fit the support and clamping arrangement to the part and bonder
TPT lists height-adjustable stages with vertical clamps or vacuum fixation, replaceable top plates and an external-controller option. Match these options to the part and bonder. [1]
Provide the substrate/package drawing, underside features and bond locations. Define the support/contact surface and the areas available for mechanical clamps or vacuum sealing. Include acceptable part deflection and surface marking in the fixture review.
Check the working height, mounting datums and clearance to the capillary or wedge, clamp and vision field throughout the bonding motion. Approve any custom top plate and the part-loading method against the specific bonder model.
02
Keep stage capability, controller rating and workpiece results separate
TPT’s stage page states up to 250 °C; HB100’s controller row states up to 200 °C ±1 °C. Obtain the delivered combination’s limits. [1][2]
Define the required temperature at the relevant workpiece surface, with the actual substrate, fixture and clamping arrangement installed. Agree sensor locations, measurement method, calibration and the allowed heating/soak conditions.
Specify spatial uniformity separately from time stability. For uniformity, identify measurement locations and the permitted spread; for stability, identify the location, time interval and permitted change after settling.
Request warm-up, settling and cooling results under the intended load and ambient conditions. Include controller sensor type, sensor placement, electrical connections and any independent over-temperature protection in the assembly specification.
03
Choose the heating arrangement from the qualified bonding process
Palomar’s manufacturer-authored study demonstrates heated-capillary gold-ball bonding for selected plastic-packaged parts while the parts remain at room temperature. It is an alternative heating arrangement for those applications, not a universal replacement for substrate heating. [3]
Set the part’s thermal budget with the bonding-process owner, including limits from the package, die attach and other materials. Identify whether the process uses substrate heat, tool heat or a defined combination.
Qualify the fixture and temperature conditions with the actual wire, bond tool, substrate and recipe. Agree the required bond-quality inspections and tests before approving a temperature or workholder change.
04
Top plate, heating, sensing and thermal management
This functional reference describes the workholder and its interfaces. Obtain the actual construction; heater technology, insulation, controller integration and active cooling depend on the supplied design.
Function
Define for the stage
Evidence or drawing
Top plate and workholding
Support surface, clamp/vacuum arrangement and part loading.
Part-fit drawing, clearance and retention trial.
Heating elements
Heater location, electrical connection and replacement scope.
Actual heater specification and assembly thermal results.
Temperature sensing
Sensor type, location and connection to the controller.
Sensor map, calibration and workpiece-measurement method.
Insulation / thermal isolation
Heat path toward the stage mount and surrounding equipment.
Construction and installed thermal assessment.
Cooling channels / active cooling, if fitted
Cooling medium, connections and operating sequence.
Specified cooling performance, leakage and utility requirements.
Temperature controller, PID if implemented
Power regulation, feedback, setpoint limits and protection.
Matched controller/firmware, wiring and tested response.
05
Define the loaded stage and the thermal acceptance method
Use the delivered workholder, top plate, controller and part as the test configuration. The complete bonder’s electrical and mass data apply to the machine scope.
Field
Define in the order
Acceptance evidence
Heating plate size (mm)
Working/support area, vacuum/clamp zones and part clearances.
Controlled top-plate and mounting drawing.
Temperature range (°C)
Required loaded-part range and limits of the stage/controller combination.
Configuration-specific ratings and measured workpiece results.
Temperature uniformity (°C)
Measurement locations, surface, load, soak and permitted spatial spread.
Calibrated temperature map under the agreed conditions.
Temperature stability (°C)
Measurement point, time interval and settled operating conditions.
Recorded temperature versus time for the loaded fixture.
Heating rate (°C/min)
Start/end temperatures, load and allowed overshoot.
Measured heating and settling profile.
Cooling rate (°C/min)
Start/end points and natural/active cooling arrangement.
Measured profile with stated utilities and load.
Power supply (V)
Stage/controller electrical scope, connector and supply requirements.
Matched wiring and power-source specification.
Power consumption (W)
Heater/controller demand during warm-up and holding.
Mode-specific demand for the supplied assembly.
Temperature control accuracy (°C)
Measurement quantity, reference, sensor and operating conditions.
Calibration/error basis distinct from surface uniformity.
Heater type
Actual heating element and replaceability.
Construction and replacement instructions.
Plate material
Support/contact material, finish and surface requirements.
Part drawing and material compatibility.
Weight (kg)
Stage, top plate, mounting and controller scope.
Mass and bonder-mounting compatibility.
Operating humidity (% RH)
Ambient exposure and condensation restrictions.
Assembly environmental limits.
IP rating
Exposed assembly/components and installation conditions.
Declared protection evidence for the supplied scope.
Bonder fit and workpiece retention
Working height, access, clamp/vacuum and mounting datums.
Installed fit check and agreed process trial.
06
Send the part drawing and bonding thermal requirement together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Bonder: [make/model; stage mount; working height; tool/vision clearance]
Workpiece: [substrate/package; dimensions; underside; bond locations]
Fixture: [support; top plate; clamp/vacuum; part-loading method]
Temperature: [loaded-part target; thermal budget; uniformity/stability method]
Assembly: [heater; sensor; controller; power; cooling if required]
Acceptance: [fit/retention; temperature map/profile; process and bond checks]
Request a heated workholder matched to the bonder and substrate
Provide the part and bonder-interface drawings with the loaded-workpiece temperature requirements. Ask for the top plate, retention method, controller/sensor configuration and the fit, thermal and process evidence for the proposal.
Sourcing Heater Stage from China?
Tell us your specification and target quantity — we will match it against
manufacturer records and come back with the factories that fit.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Confirm responsibility for the fixture, heating controls and bond-process qualification. Keep the accepted part/stage/controller combination and measurement method with the production recipe. How we source and review
· Page last updated 19 October 2026
Buyer questions
Can a heater stage be ordered from plate dimensions alone?
Confirm its working height, clamping/vacuum arrangement, top plate and controller connection. [1]
Does the HB100 controller row establish workpiece temperature uniformity?
Request a separate temperature map of the loaded workpiece and fixture. [2]
Can the stage catalogue temperature be applied to any bonder/controller combination?
Obtain the rating and validation for the exact delivered combination. [1][2]
Is substrate heating required for every gold-ball bonding application?
Palomar reports a heated-tool alternative for selected parts; qualify the actual process and thermal budget. [3]
Sources and what still needs a direct check
Sources checked 2026-10-19. TPT separates workholding options from its HB100 host/controller example. Palomar demonstrates a heated-tool process for selected applications. Keep each example within its stated scope.