Editorial Technical Reference

Integrated Radiotherapy Linear Accelerator Assembly System

This page explains how Integrated Radiotherapy Linear Accelerator Assembly System is classified within Manufacture of Irradiation, Electromedical and Electrotherapeutic Equipment. Technical values and manufacturer relationships are research references; confirm the current specification and supplier evidence for each order.

Technical Definition & Core Assembly

Automated production line for assembling radiotherapy linear accelerator treatment heads
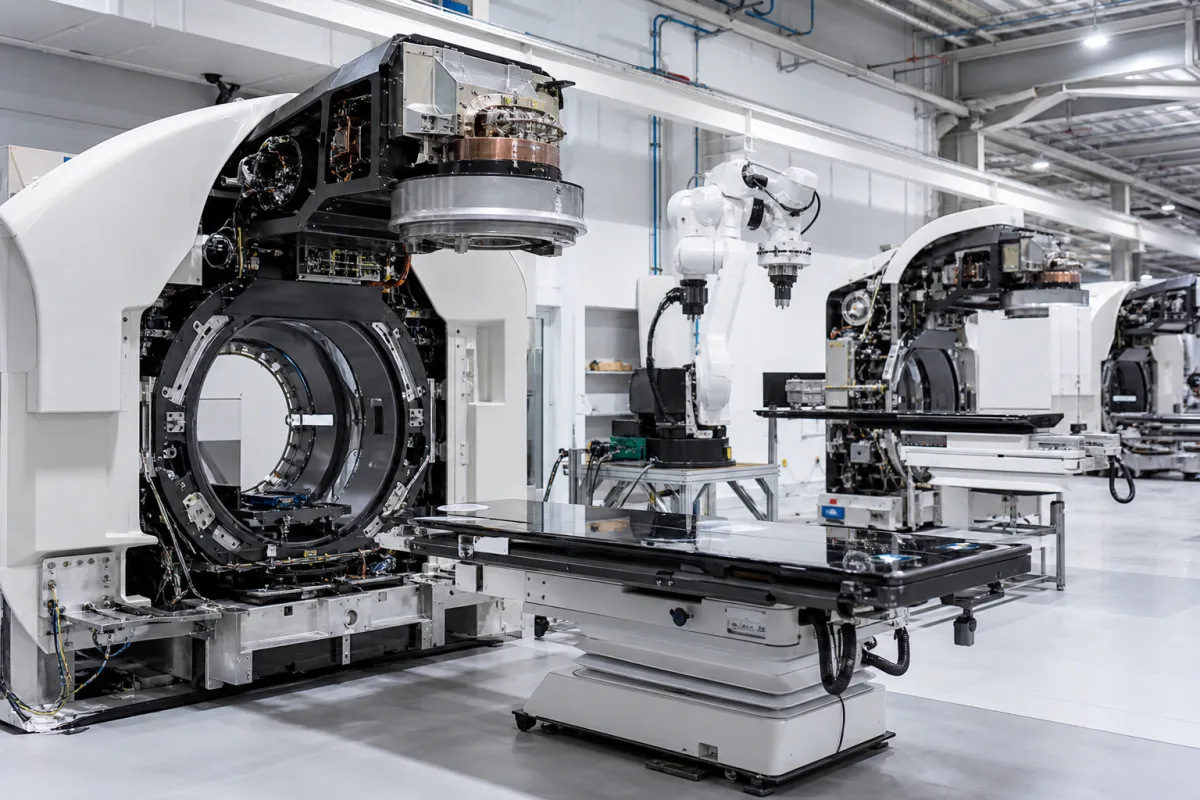
Integrated Radiotherapy Linear Accelerator Assembly System in a manufacturing environment
Representative product image. Confirm appearance and specifications with the manufacturer.

Product Specifications

Technical details and manufacturing context for Integrated Radiotherapy Linear Accelerator Assembly System

Definition
A fully integrated industrial manufacturing system designed for the automated assembly of linear accelerator treatment heads used in external beam radiotherapy. This coordinated multi-module solution handles precision component integration, alignment verification, and functional testing of critical radiation delivery subsystems. The system ensures consistent quality and throughput in producing the complex mechanical and electronic assemblies that generate and shape therapeutic X-ray beams for cancer treatment applications. It comprises a series of sequential workstations, typically 8 to 16, where robotic arms with a payload capacity of 500–2000 kg perform precision placement of components. The robotic arms achieve a positioning repeatability of ±0.05 mm per ISO 9283, ensuring high accuracy in assembly. The system integrates automated fastening with torque accuracy of ±3% per ISO 5393 for critical fasteners, and laser alignment verification to confirm the precise geometry of the beam generation and collimation systems. Functional testing validates the performance of beam generation and shaping subsystems. The system requires a floor space of 120–300 m² and weighs 15,000–30,000 kg (excluding product). Electrical power consumption is 380–480 kW per IEC 60204-1, and compressed air consumption is 500–1500 L/min at operating pressure per ISO 8573-1. The operating environment should be maintained at 15–35 °C and 30–75% relative humidity (non-condensing). Electrical enclosures are rated IP54–IP65 per IEC 60529. The cycle time for a complete head assembly is 45–90 minutes. Pneumatic circuits are leak-tested at 0.6–1.0 MPa. Materials used include Stainless Steel 316L, Medical-Grade Aluminum Alloy, High-Purity Copper, and Radiation-Shielding Tungsten Alloy. This system is intended for manufacturers of radiotherapy equipment. Verify all model-specific values and standards with the legal manufacturer or supplier before procurement.
Working Principle
Automated material handling transports components through sequential assembly stations. Robotic arms perform precision placement of heavy components, followed by automated fastening with controlled torque. Laser alignment verification ensures correct positioning of beam generation and collimation elements. Integrated functional testing validates the performance of the assembled head, including beam generation and shaping. The system operates in a controlled environment with specified temperature, humidity, and air quality.
Common Materials
Stainless Steel 316L, Medical-Grade Aluminum Alloy, High-Purity Copper, Radiation-Shielding Tungsten Alloy
Technical Parameters
ParameterTypical rangeNotes & selection driver
Maximum Payload CapacityRequired500–2000 kgMaximum component weight handled by robotic arms
Assembly Station CountRequired8–16 unitsNumber of sequential workstations in the production line
Positioning RepeatabilityRequired±0.05 μmRobotic arm positioning consistencyISO 9283
System FootprintRequired120–300 Total floor space required for installation
Electrical Power RequirementRequired380–480 kWTotal electrical power consumptionIEC 60204-1
Compressed Air Consumption500–1500 L/minPneumatic system air flow rate at operating pressureISO 8573-1
Operating Temperature Range15–35 °CFor optimal performance
Relative Humidity Range30–75 % RHNon-condensing
Ingress Protection RatingIP54–IP65For electrical enclosuresIEC 60529
Cycle Time per Assembly45–90 minFor complete head assembly
Torque Accuracy±3 %For critical fastenersISO 5393
Leak Test Pressure0.6–1.0 MPaFor pneumatic circuitsISO 5208
System Weight15000–30000 kgExcluding product

Ranges are indicative industry figures for RFQ preparation, not a supplier commitment. Confirm every value and standard with the legal manufacturer before ordering.

Components / BOM

Industry Taxonomies & Aliases

Commonly used trade names and technical identifiers for Integrated Radiotherapy Linear Accelerator Assembly System.

Industrial Ecosystem & Supply Chain Structure

Complementary Systems
Downstream Applications
Specialized Tooling

Application Fit & Sizing Matrix

Operational Limits
pressure: Atmospheric (cleanroom pressure positive to 0.1-0.2 in. H₂O)
other spec: ISO Class 5-7 cleanroom, vibration <25 µm/s RMS, humidity 30-60% RH, electromagnetic interference <1 V/m
temperature: 15-25°C (controlled cleanroom environment)
Media Compatibility
✓ Medical-grade stainless steel components ✓ High-precision tungsten collimators ✓ Ceramic insulators and RF components
Unsuitable: Corrosive chemical processing environments or areas with conductive dust/particulates
Sizing Data Required
  • Annual production volume (units/year)
  • Treatment head model variants to be assembled
  • Maximum component weight/size for handling systems

Reliability & Engineering Risk Analysis

Failure Mode & Root Cause
Beam Steering Magnet Coil Insulation Degradation
Cause: Thermal cycling and high-voltage stress causing insulation breakdown, leading to short circuits or arcing in the magnet power supply system.
Target/Window Assembly Thermal Fatigue Cracking
Cause: Repeated thermal stress from pulsed electron beam bombardment causing micro-cracks in the target or beam window, potentially leading to vacuum leaks or beam instability.
Maintenance Indicators
  • Audible high-frequency arcing or popping sounds from the waveguide or magnetron assembly indicating vacuum degradation or insulation failure
  • Visual beam symmetry distortion or intensity fluctuations on the beam profile monitor display during routine quality assurance checks
Engineering Tips
  • Implement predictive maintenance through continuous monitoring of magnet coil temperature trends and insulation resistance measurements to detect early degradation before catastrophic failure
  • Establish strict thermal management protocols including controlled cooldown cycles and maintaining optimal cooling water temperature/purity to minimize thermal stress on target assemblies

Indicative industry ranges for design and RFQ preparation. Confirm the exact figures and applicable standard with the manufacturer before specifying.

Compliance & Manufacturing Standards

Applicable Standards
IEC 60601-2-1:2017 - Medical electrical equipment - Part 2-1: Particular requirements for the basic safety and essential performance of electron accelerators in the range 1 MeV to 50 MeV ANSI N43.2-2017 - Radiation Safety for the Design and Use of Cabinet X-ray Systems and Other Radiation Emitting Products

Quoted from the published standard.

Manufacturing Precision
  • Beam isocenter alignment: +/- 0.5 mm
  • Gantry rotation concentricity: +/- 0.1 mm
Quality Inspection
  • Daily QA output constancy test (e.g., beam energy, dose rate, flatness/symmetry)
  • Annual comprehensive performance verification (including mechanical, dosimetric, and safety system tests)

Manufacturers of Integrated Radiotherapy Linear Accelerator Assembly System

Manufacturer profiles associated with Integrated Radiotherapy Linear Accelerator Assembly System.

Sourcing Integrated Radiotherapy Linear Accelerator Assembly System from China?
Tell us your specification and target quantity — we will match it against manufacturer records and come back with the factories that fit.
Request manufacturers We manufacture this

Manufacturer listings support early research and capability understanding. They are not certification, ranking, or transaction guarantees.

Share this page
Technical documentation
Request current drawings, revision history, and a signed specification sheet.
Manufacturing capability
Verify equipment lists, process limits, capacity, and representative production evidence.
Inspection readiness
Confirm test methods, calibrated equipment, sampling plans, and traceable reports.
Supplier transparency
Check the legal entity, factory address, ownership, certifications, and direct contacts.

CNFX does not score or rank suppliers. Buyers must verify all claims and documents with the legal manufacturer before ordering.

Frequently Asked Questions

What is the typical cycle time for assembling a complete treatment head?

The cycle time per complete head assembly is 45–90 minutes, depending on the specific configuration and options. This includes all assembly steps, alignment verification, and functional testing.

What standards are referenced for positioning repeatability and torque accuracy?

Positioning repeatability is specified per ISO 9283, and torque accuracy for critical fasteners is per ISO 5393. These standards provide testing methods and acceptance criteria, but actual compliance must be confirmed with the manufacturer.

What are the environmental requirements for installation?

The system requires an operating temperature range of 15–35 °C and relative humidity of 30–75% (non-condensing). Electrical enclosures are rated IP54–IP65 per IEC 60529. Ensure adequate ventilation and clean air supply.

Can the system handle different models of linear accelerator treatment heads?

The system is designed for flexibility within its specified payload and station count. However, tooling and programming may need adjustment for different head models. Consult the manufacturer for compatibility and customization options.

Data Basis

Editorial classification, named public sources where available, and source-reviewed manufacturer records.

Preliminary Technical Classification
This page supports structured research, RFQ preparation, and supplier evaluation. It does not replace buyer-led supplier qualification, standards review, or technical approval.
Buyer enquiry

Request manufacturing insight for Integrated Radiotherapy Linear Accelerator Assembly System

Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.

Where it goes
Straight to the CNFX editorial desk, and to the manufacturer if this product is linked to a claimed profile. Nothing is broadcast to a supplier list.
Your details stay here
We do not sell or rent enquiry data, and we do not add you to a mailing list. Used only to answer this request.
No commission, no middleman
CNFX is a directory. We take no cut of any order and never negotiate on a supplier's behalf.
What we don't claim
A listing is not an endorsement. Qualify every supplier and verify every figure yourself before ordering.

Your business information is used only to process this request.

Thank you! Your message has been sent. We'll respond within 1–3 business days.
Sorry, we couldn't send your message. Please try again, or email us at [email protected].

Need to Manufacture Integrated Radiotherapy Linear Accelerator Assembly System?

Compare manufacturer profiles with relevant product and process capability.

Previous Product
Integrated Medical Imaging System Production Line
Next Product
Integrated Radiotherapy Treatment Planning and Delivery System
Get QuotesChat