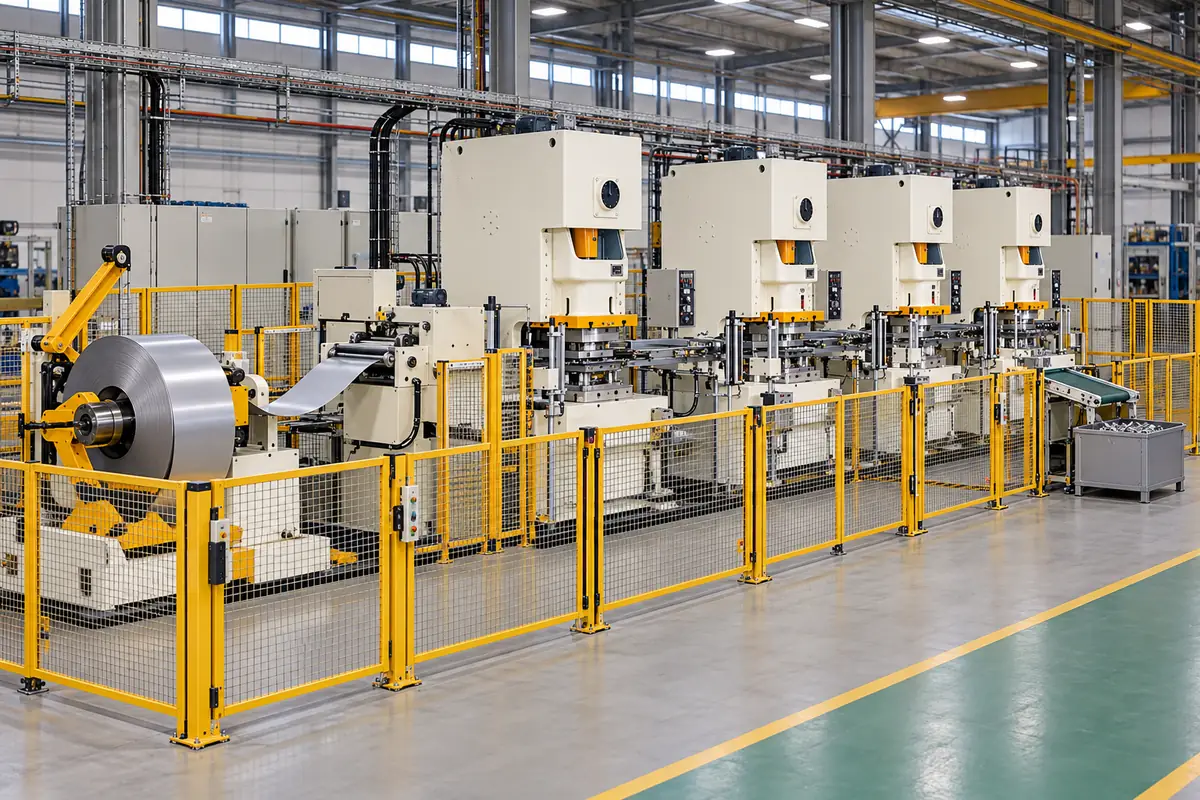
Automated stamping lines for automotive, appliance and electrical sheet-metal parts · coil-fed press lines, tandem robot lines, multi-station and progressive-die lines, three-in-one decoiler-straightener-feeders, press safeguarding, brake monitoring and safety distance (OSHA 1910.217)
An automated stamping line feeds sheet metal from coil or blanks through one or more presses and moves parts between dies automatically, producing car body panels, appliance shells, TV backplanes and motor laminations with little manual handling. Ask three things first: the parts, material, coil or blank size and output rate, which decide between a progressive-die line, a multi-station (transfer) press or a tandem line of presses with robots; the presses' force, bed size and stroke rate; and how the line will be safeguarded and inspected to meet press-safety rules.
Automated stamping lines — coil-fed press lines with decoiler, straightener and feeder, progressive-die lines, multi-station transfer press lines, robot or single-arm tandem press lines, and coil blanking lines — with die-change, oiling and stacking equipment. Stand-alone presses (separate pages), press brakes, forging lines, laser blanking and individual dies are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Press makers show how stamping lines are configured. Jiangsu Yawei, a listed Chinese metal-forming machine maker, lists fully automatic stamping lines including single-arm fast flexible lines and robot stamping lines, multi-station press automatic lines and progressive-die lines, and coil blanking, swing-shear, cut-to-length and slitting lines; its press options include a three-in-one feeding unit, an oiling unit, three-axis transfer automation and stacking, with eccentric or multi-link drives, quick die change and heavy-duty lubrication. [2] Yangli Group lists closed single-, double- and four-point presses, four-point multi-link and multi-station presses and blanking presses, with stamping solutions for automotive, appliance shells, TV backplanes, can-making and motor stator and rotor laminations. [3]
Editorial note: ask each supplier which configuration — progressive-die, multi-station or tandem — it proposes for your part and why, with the output rate and die-change time it can demonstrate on a reference line.
Give the supplier the part drawings and annual volume, material grade, thickness and coil width or blank size, line type (progressive, transfer, tandem), press force, bed size, stroke, stroke rate and drive (mechanical, servo, multi-link), feeder (three-in-one decoiler-straightener-feeder) and transfer automation, die-change system, oiling and stacking, safeguarding and controls, floor space and foundations, power supply, installation and training, and delivery time.
02
Plan safeguarding, brake monitoring and inspection
In the United States, 29 CFR 1910.217 covers mechanical power presses; it excludes press brakes, hydraulic and pneumatic presses, forging presses and hammers. The employer must provide and ensure the use of point-of-operation guards or properly applied devices on every operation, unless the point-of-operation opening is 1/4 inch or less. Clutch and brake controls must prevent single-stroke or continuous operation unless the drive motor is energised and running forward and must deactivate on loss of power or air, and a brake monitor must stop a further stroke if stopping time or braking distance deteriorates below the safety distance in use. Presence-sensing devices must stop the slide if a hand is in the field during the downstroke and may not be used on full-revolution clutch presses; their minimum safety distance is Ds = 63 in/s × Ts, where Ts is the press stopping time measured at about 90° of crankshaft rotation. Employers must use dies and methods that control hazards, provide means to handle scrap from roll-fed presses, and run an inspection and maintenance programme covering the clutch and brake, anti-repeat feature and single-stroke mechanism. [1]
Editorial calculation: a press with a measured stopping time of 0.20 s needs a light curtain at least 63 × 0.20 = 12.6 in (about 320 mm) from the danger point; if the brake wears and stopping time rises to 0.25 s, the distance must grow to about 15.8 in (400 mm), which the brake monitor is there to catch. [1]
Editorial note: OSHA 1910.217 applies only to mechanical presses in the US; servo and hydraulic lines and other markets follow other rules, so ask the supplier which safety standards the line is designed and certified to.
03
Match the line type to a press family and tonnage band
AIDA-America, a press maker, lists its presses by line type and tonnage, separating servo and mechanical families. Its Dallas Industries feed-line business, founded in 1962, offers servo feeds, coil straighteners, single- and double-end reels, load cars, cradles, threading tables, mechanical shears and compact SpaceSaver™ lines, which AIDA says "can reduce floorspace requirements by up to 50%". [4]
The same page lists the automation that links the presses: the A-8II press-to-press transfer robot, NCTHL press-to-press transfer, NCAH III and TCS intra-press transfer, and coil feeding by the LFA Servo Coil Feeder, L Series combined uncoiler straightener and F-III NC roll feeder. [4] Yawei's listing groups lines in a similar way, from single-arm and robot lines to multi-station and progressive-die lines [2]. Use the line type to narrow the press family, then ask for the stroke rate, bed size and die height that the tonnage band leaves open.
A tonnage band does not settle safeguarding. OSHA's 29 CFR 1910.217 applies to mechanical power presses and excludes hydraulic and pneumatic presses [1]; ask whether the press offered is mechanical or servo-mechanical and which safeguarding and brake monitoring the supplier provides for it.
Editorial calculation: AIDA does not state whether its tons are metric or US short tons; 3,000 tons is about 29,400 kN if metric (9.81 kN per tonne-force) or about 26,700 kN if US short tons (8.90 kN per ton-force). [4]
Line type
AIDA servo model (tonnage)
AIDA mechanical model (tonnage)
Progressive die and transfer
DSF-M2, 315-1,250 tons
MCX, 315-1,250 tons
Progressive die (and cut-to-length)
DSF-P, 200-3,000 tons
PMX, 200-3,000 tons
Tandem and transfer
DSF-S2/4, 800-3,000 tons
SMX, 300-3,000 tons
Transfer
DSF-T Servo Transfer, 800-3,500 tons
TMX, 800-4,000 tons
Ultra-high precision
DSF-U, 80-2,500 tons
ULX, 80-2,500 tons
Gap frame
DSF-C1-A, 80-250 tons
NC1, 35-250 tons; NC2, 110-250 tons
Model names and tonnage ranges are from AIDA-America's Dallas feed lines page and its press menu; individual specification sheets were not reviewed.
04
Compare what suppliers offer
Suppliers linked to this page list automated stamping lines or the presses that make them up; each card links to the page reviewed.
Listings include fully automatic and robot stamping lines, multi-station and progressive-die lines, coil blanking lines, and single-, double- and four-point and multi-link presses with industry stamping solutions; ask each for reference lines running similar parts, output rates and the safety standards applied.
05
Trace the line from coil to finished part
This is a functional reference built from the sources cited; it is not one maker's line.
Fill the specification fields with values for your project
An automated stamping line quotation needs values for your project. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Field
What it means and published values
Ask the supplier for
Nominal press force (kN)
Press families listed from 35 to 4,000 tons by line type. [4]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 12 October 2026
OSHA 1910.217 sets Ds = 63 in/s × Ts, where Ts is the press stopping time at about 90° of crankshaft rotation. [1]
Does OSHA 1910.217 cover hydraulic presses?
No. It excludes press brakes, hydraulic and pneumatic presses, forging presses and hammers. [1]
What feeding options do stamping lines use?
One maker lists three-in-one feeders, oilers, three-axis transfer automation and stacking as press options. [2]
What press tonnage does a transfer or progressive-die stamping line use?
AIDA-America lists progressive die and transfer presses at 315-1,250 tons, progressive die presses up to 3,000 tons and transfer presses from 800 tons to 3,500 (servo) or 4,000 tons (mechanical). [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. 29 CFR 1910.217 is a US workplace-safety regulation. Yawei and Yangli are press makers that also appear as suppliers on this page.