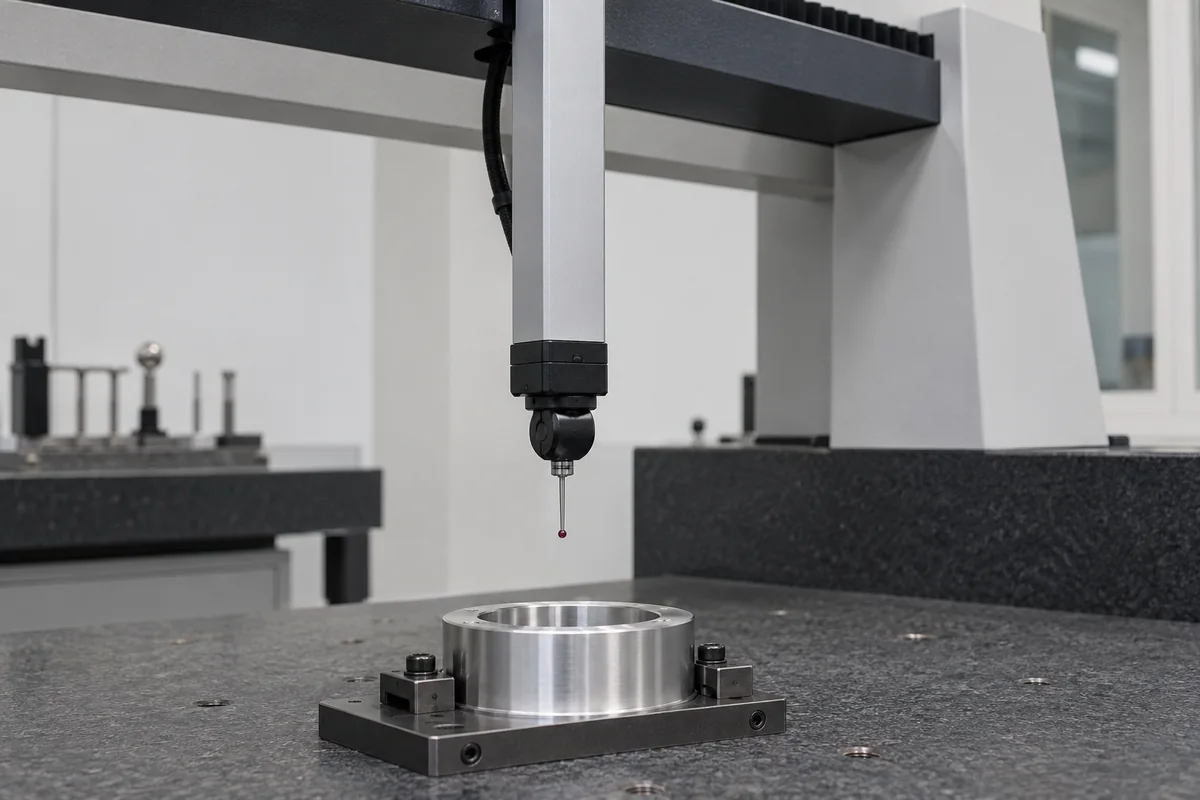
Z-axis quill assemblies for bridge coordinate measuring machines
CMM vertical quills — mechanical fit, head mounting and recommissioning
The vertical quill carries the measuring head through the bridge CMM’s working volume. A replacement enquiry needs the machine identity and mechanical interfaces, together with a plan to restore the installed measuring system after the quill or head is disturbed.
Machine-specific Z-axis quill or ram assemblies carrying a probe head on bridge coordinate measuring machines, for builder integration or service replacement. The assembly boundary covers the moving member, carriage-guide interface and head mounting. Bridge Structure covers the spanning beam and uprights; Exposed linear encoders covers scale products; Multi-sensor probe head and Touch-trigger probe cover the sensing hardware. Complete CMMs and rotating cutting spindles have separate functions and supply boundaries.
Match the moving quill to its carriage and installed drive
Renishaw describes the bridge CMM’s vertical quill as a low-inertia member carrying the touch probe. Its carriage and quill drive examples include belt, screw and linear-motor arrangements. Identify the machine’s arrangement before defining the replacement assembly. [1]
Record what is supplied with the quill: bare member, guide hardware, drive attachments, readout hardware or head-mount adaptor. List the items transferred from the installed machine and have the builder review the resulting combination.
Hexagon describes air bearings as providing a compressed-air film between moving members and their guides, with a clean air supply essential to that arrangement. Where the installed quill uses air guidance, obtain its machine-specific air requirements and guide-care instructions. [3]
Keep transport supports, lifting and vertical-axis securing instructions in the service work pack. Agree access and responsibility for removing the installed member before ordering the replacement; use the machine builder’s procedure for the actual assembly.
Installed bearing arrangement, guide-surface requirements and the builder’s service-supply specification.
Drive and vertical support
Existing drive connection, supported moving assembly and the builder’s procedure for securing and exchanging the vertical member.
Head and services
Head-mount drawing, cable route and service clearances throughout the required motion.
Readout installation
Scale/readhead positions, mounting instructions, reference arrangement and configuration to retain or restore.
02
Treat head mounting as a measurement interface
The Renishaw MH8 installation guide calls for a rigid head mounting and a shank specified by the CMM manufacturer. Movement at that joint adds measurement error. It also requires requalification of every head position in use when the head is replaced or repositioned in the quill. [2]
Name the head, shank or adaptor and connection drawing in the order. Specify whether the interface hardware is supplied fitted or transferred, and retain its orientation and cable-access requirements. Include the head and probing configuration in the recommissioning record.
For its MH8 arrangement, Renishaw lists the PEL1 as a 50 mm reach extension and advises against the PEL2, PEL3 and PE series. This is an example of a head-specific extension restriction; check the documentation for the installed head and probe combination. [2]
Review the complete swept envelope with the planned head positions, probe and fixture. Ask the integrator to confirm clearances at the quill’s travel limits and along the measurement path, including the cable route and any changer access.
Separate a head qualification record from the machine checks agreed for the mechanical replacement. Define who will restore the machine configuration, qualify the probing setup and demonstrate the required measurements before returning the CMM to service.
03
Preserve the relationship between the quill, its scale and temperature model
Renishaw distinguishes floating scales, which follow their own thermal expansion, from mastered scales, which follow the supporting substrate. Its CMM example explains why scale mounting and structural temperature response need to be considered together. [1]
Record the quill material, scale mounting, readhead location and temperature-sensing arrangement from the builder’s documentation. If any of these changes with the replacement, obtain a review of the measurement configuration rather than carrying its settings forward by assumption.
Hexagon explains that temperature affects both the inspected part and the CMM structure. Record the environmental conditions specified for the machine checks, together with the conditions observed during the post-installation measurement run. [3]
Agree the acceptance work before dismantling: mechanical installation checks, restored service and readout operation, head qualification and the applicable machine measurement checks. Keep the replacement identity, installed configuration, test method and results in the service record.
If the work includes a new scale, head or controller configuration, identify that additional change explicitly. This makes the acceptance record describe the assembly actually returned to service and gives future repairs a usable configuration baseline.
04
Bridge CMM quill replacement and recommissioning brief
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Machine identity: [builder, model, serial number and current configuration]
Quill: [part/drawing revision, material, section, guide datums and required travel envelope]
Assembly boundary: [supplied parts and hardware transferred from the installed machine]
Motion and support: [guide arrangement, drive connection, vertical securing and exchange procedure]
Head interface: [head/probe models, shank/adaptor drawing, orientation, services and swept clearances]
Readout and temperature: [scale/readhead, mounting, reference configuration, sensors and changes proposed]
Installation: [builder review, responsible service provider, access, supports and required supplies]
Return to service: [installation checks, head qualification, machine measurement checks, environmental conditions and retained reports]
Provide the CMM model and serial number, quill and head-mount drawings, transferred hardware list and agreed recommissioning work with the service enquiry.
Sourcing Z-axis Ram/Spindle from China?
Tell us your specification and target quantity — we will match it against
manufacturer records and come back with the factories that fit.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 23 October 2026
Buyer questions
Does a CMM quill assembly always use a ballscrew?
Confirm the installed drive. Renishaw’s bridge CMM description includes belt, screw and linear-motor arrangements for the carriage and quill. [1]
What must be restored after repositioning an MH8 head in the quill?
Renishaw requires a rigid mounting and requalification of all head positions in current use. Include those positions and the actual probing configuration in the service record. [2]
Why retain the scale mounting details with the replacement drawing?
The mounting determines whether the scale follows its own thermal expansion or that of its supporting substrate. Renishaw’s CMM example treats that choice as part of the machine’s thermal measurement behavior. [1]
Sources and evidence scope
Sources checked 2026-10-23T16:39:12+08:00. Original CMM construction and mounting references from Renishaw and Hexagon. The MH8 instructions apply to that named head; use the installed machine and probing-system documentation for the replacement procedure and acceptance requirements.