Die Head
View system integration details
This page explains how Die Body/Housing is classified within Machinery and Equipment Manufacturing. Technical values and manufacturer relationships are research references; confirm the current specification and supplier evidence for each order.
The main structural component of a die head that houses and supports all internal die components.
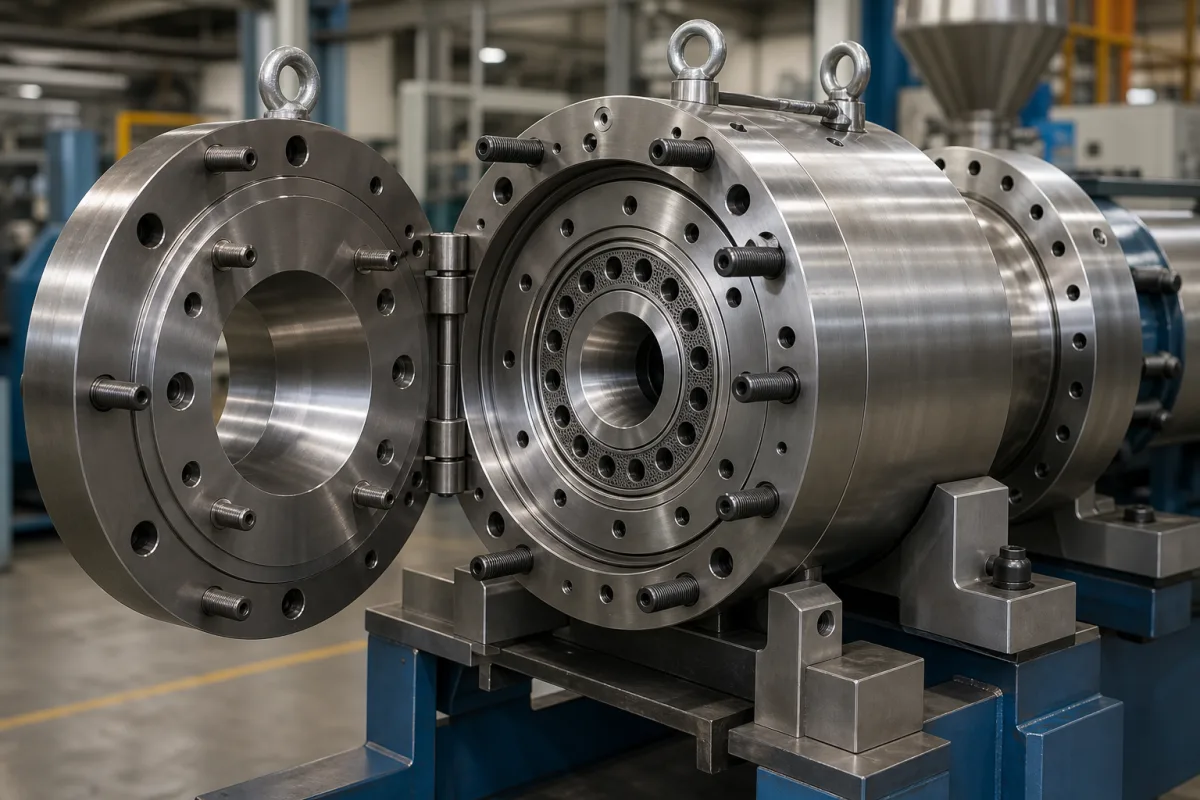
Technical details and manufacturing context for Die Body/Housing
| Parameter | Typical range | Notes & selection driver |
|---|---|---|
| Material Grade | 45# steel or 40Cr | Higher strength and wear resistance for high-pressure diesGB/T 699, GB/T 3077 |
| Hardness | 28–32 HRC | Balances toughness and wear resistanceGB/T 230.1 |
| Surface Roughness | Ra 0.8–1.6 μm | Affects die life and product finishGB/T 1031 |
| Cavity Diameter | 50–300 mm | Determines maximum part size |
| Overall Dimensions | 200×200×150 – 600×600×400 mm | Must fit press and die set |
| Weight | 50–500 kg | Affects handling and press capacity |
| Operating Temperature | -20–200 °C | Above 200°C may require heat-resistant alloys |
| Operating Pressure | 1.0–1.6 MPa | |
| Tolerance Grade | IT7–IT8 | Critical for alignment of internal componentsISO 286-1 |
| Concentricity | ≤0.02 mm | Ensures uniform wall thickness and balanceISO 1101 |
| Flatness | ≤0.05 mm | Affects sealing and mountingISO 1101 |
| Sealing Surface Finish | Ra 0.4–0.8 μm | Prevents leakage under pressureGB/T 1031 |
| Corrosion Resistance | Salt spray 48–72 h | Required for humid or chemical environmentsGB/T 10125 |
Ranges are indicative industry figures for RFQ preparation, not a supplier commitment. Confirm every value and standard with the legal manufacturer before ordering.
| pressure: | Up to 10,000 psi (690 bar) standard, higher with specialized designs |
| flow rate: | Dependent on internal geometry and port sizing |
| temperature: | -40°C to 400°C (dependent on material grade) |
| slurry concentration: | Up to 60% solids by weight (material dependent) |
Indicative industry ranges for design and RFQ preparation. Confirm the exact figures and applicable standard with the manufacturer before specifying.
Quoted from the published standard.
A practical evidence checklist for RFQ preparation and supplier evaluation.
Compare the published product scope and source details, then include your specifications and quantity in an enquiry.
Manufacturer profiles associated with Die Body/Housing.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.
Common materials include tool steel, stainless steel, and alloy steel. Specific grades such as 45# steel or 40Cr are referenced in standards GB/T 699 and GB/T 3077. The choice depends on required strength, wear resistance, and operating environment.
Hardness is typically specified as 28–32 HRC, and surface roughness is Ra 0.8–1.6 μm for general surfaces. Sealing surfaces may require a finer finish of Ra 0.4–0.8 μm. These values affect die life and product finish.
Check the specified parameters such as cavity diameter, overall dimensions, weight, operating temperature, pressure, tolerance grade, concentricity, flatness, and corrosion resistance. Always confirm these values with the legal manufacturer or supplier for your specific model and application.
Relevant standards include GB/T 699 for material, GB/T 3077 for alloy steel, GB/T 230.1 for hardness, GB/T 1031 for surface roughness, ISO 286-1 for tolerance, ISO 1101 for geometric tolerances, and GB/T 10125 for salt spray testing. These are verification references, not proof of certification.
This component is essential for the following industrial systems and equipment:
Editorial classification, named public sources where available, and source-reviewed manufacturer records.
Compare manufacturer profiles with relevant product and process capability.