Multi-axis, multi-path CNC controller for multi-turret lathes, turn-mill centres and transfer machines: up to 10–15 paths and 96 axes in one control
CNC controls that run two or more part programs at once on one machine · paths, channels and part systems, how many axes each can carry, and the synchronisation that keeps turrets, spindles and loaders apart
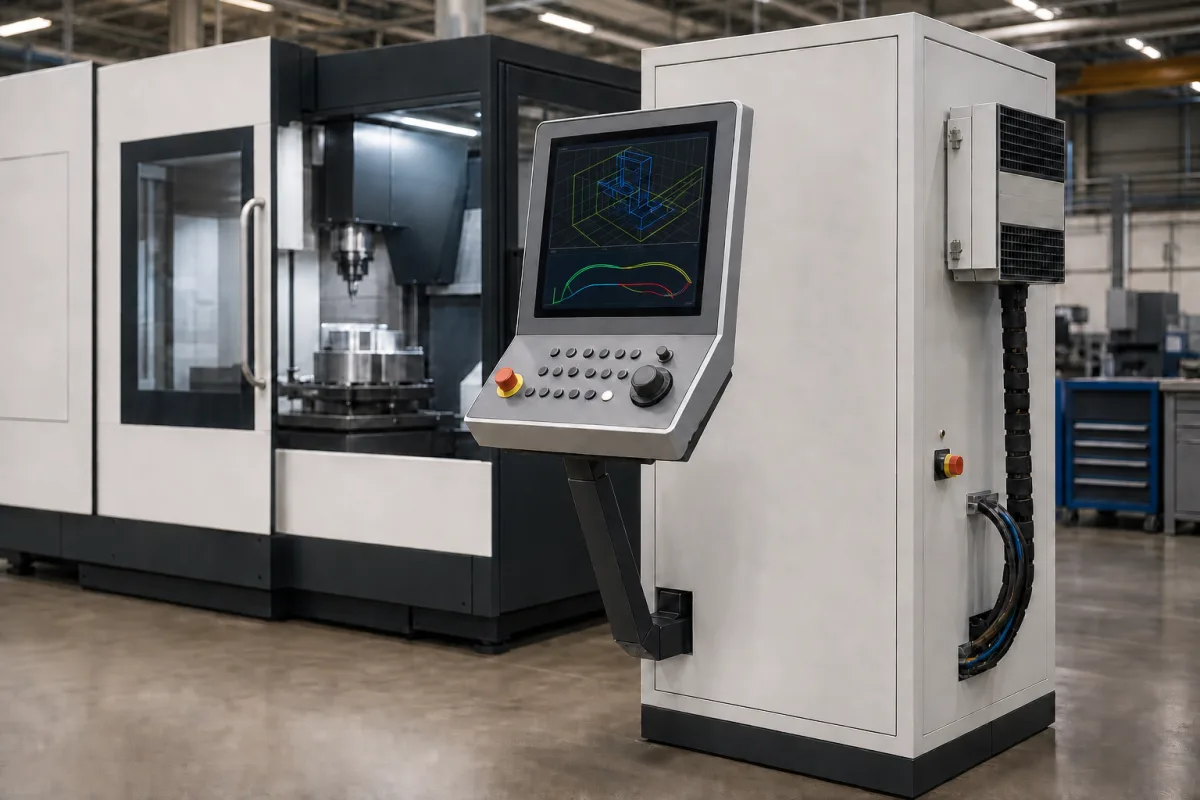
A single-channel CNC runs one part program and interpolates one group of axes. A multi-turret lathe, a Swiss-type automatic, a turn-mill centre with a milling head and lower turret, or a rotary transfer machine has two or more tools cutting at the same time, each following its own program. The control for such machines splits its axes and spindles into paths (FANUC), channels (Siemens) or part systems (Mitsubishi), each with its own program decoding and interpolation, and adds functions to synchronise them, pass axes between them and stop them colliding. Choosing one means counting paths and axes, checking how many axes each path can move together, and confirming which synchronisation and interference functions the machine needs. The picture shows the arrangement on the shop floor: a free-standing control cabinet with a cabinet cooler and cable chain, carrying a swing-arm operator panel with a screen showing a 3-D toolpath, next to a machining centre.
CNC controls whose defining feature is the number of independent paths, channels or part systems and the total and per-path axis count, for multi-turret and multi-spindle lathes, turn-mill and multi-tasking machines, rotary transfer machines and machines with loaders: path structure, axis assignment and interchange, waiting and synchronisation functions, and multi-path PLC. Five-axis simultaneous control with RTCP and kinematic transformation is covered on the 5-axis CNC controller page; CNC controls for milling machines, machining centres and lathes, with look-ahead and path-accuracy settings, on the CNC controller page; press brake controls on the CNC control system for press brakes page; encoder interfaces on the Feedback interface for CNC axes page; drive modules on the Axis control module page.
CNFX editorial research · Sources checked October 13, 2026 · 3 sources
Paths, channels and part systems: FANUC's 10–15 paths, Siemens' 10 channels and Mitsubishi's 8 part systems
The three makers use different names for the same unit: an independent program with its own interpolation. What a buyer compares is how many such units the control allows and how many axes and spindles they share.
Siemens defines a channel as having its own program decoding, block preparation and interpolation, so that a part program runs independently within it; a mode group combines channels with axes and spindles into a machining unit whose channels always run in the same mode, and corresponds to an independent multi-channel NC. Its example is a large machining centre where one part of the machine runs a program in AUTOMATIC while a workpiece is set up in JOG on another, a task that would otherwise need two controls. [2]
Editorial calculation: FANUC's 96 axes over 10 paths average 9.6 axes per path, and 72 axes over 15 paths 4.8; Mitsubishi's 48 axes over 21 part systems on three C80 units average about 2.3. The averages show where a control's ceiling is axes rather than paths. [1][3]
Control
Paths / channels / part systems
Axes
Simultaneous axes
FANUC Series 30i-B Plus
10 to 15 paths
96 axes (72 feed, 24 spindles) with 10 paths; 72 axes (56 feed, 16 spindles) with 15 paths
List each turret, spindle, milling head, loader or station that must move independently, with its axes, and say which of them must cut at the same time.
02
Waiting, superimposed and composite control, axis interchange and interference check between paths
Once two or more programs run at once, the control has to coordinate them. The makers name the functions that do this; the machine builder decides which are enabled.
FANUC lists synchronous and composite control, superimposed control, flexible axis assignment, a waiting function and interference check as the multi-path functions of the 30i-B Plus, for multi-path lathes with more than one turret, compound machines with a milling head and automatic lathes; its program management lets all part programs for one job be selected together, shown and edited on one screen (up to three at a time) and input or output as one file. [1]
In the SINUMERIK 840D sl an axis or spindle belongs at power-on to one channel and can only be moved there; axis/spindle interchange releases it to another channel, from the part program (GET/GETD or by programming the axis name), from the PLC or from motion-synchronous actions. The processes in the channels of one mode group can be synchronised in the part programs. On the 828D, interchange between channels is not possible. [2]
The PLC side multiplies as well: FANUC's multi-path PMC runs up to five independent ladder programs, for example machine, loader and peripheral control, with up to 300,000 steps in total and up to 40 ladder programs. [1]
Name the synchronisation functions the process needs (waits between turrets, superimposed motion, synchronous spindles, axis transfer, collision check) and the number of PLC programs for loaders or peripherals.
03
Block change time and control cycle: what a compact single-channel CNC delivers
Path count is one limit; the speed at which each channel processes blocks is another.
FANUC gives the 30i-B Plus an increment system from 0.1 µm down to 1 nm and high-speed 1 ms sampling of servo data. [1]
Editorial calculation: at a 3 ms minimum block change time a channel can execute at most about 333 blocks per second (1 ÷ 0.003); at 9 ms about 111. With an example 0.1 mm block length (an example value), those rates correspond to about 2.0 m/min and 0.67 m/min before the control has to slow down. [2]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How many paths can a multi-path CNC run?
FANUC gives 10 to 15 paths for the Series 30i-B Plus, Siemens up to 10 channels for the SINUMERIK 840D sl, and Mitsubishi up to 8 part systems on lathe systems of the M800V/M80V/E80. [1][2][3]
How many axes can such a control handle?
The FANUC 30i-B Plus handles 96 axes (72 feed, 24 spindles) with 10 paths or 72 axes with 15 paths, with up to 24 moving simultaneously. [1]
Can an axis move from one channel to another?
On the SINUMERIK 840D sl, yes: axis/spindle interchange can be triggered from the part program (GET/GETD), the PLC or synchronous actions. On the 828D it is not possible between channels. [2]
What is a part system?
Mitsubishi's term for an independent program and axis group; one part system is standard, with up to eight on lathe systems and two on machining-centre systems. [3]
Sources and what still needs a direct check
Sources checked 2026-10-13. Three documents from three CNC makers: FANUC's Series 30i/31i/32i-B Plus catalogue, Siemens' SINUMERIK 840D sl / 828D Extended Functions manual (section K5, mode groups, channels and axis interchange), and Mitsubishi Electric's M800V/M80V/E80/C80 NC specification selection guide.