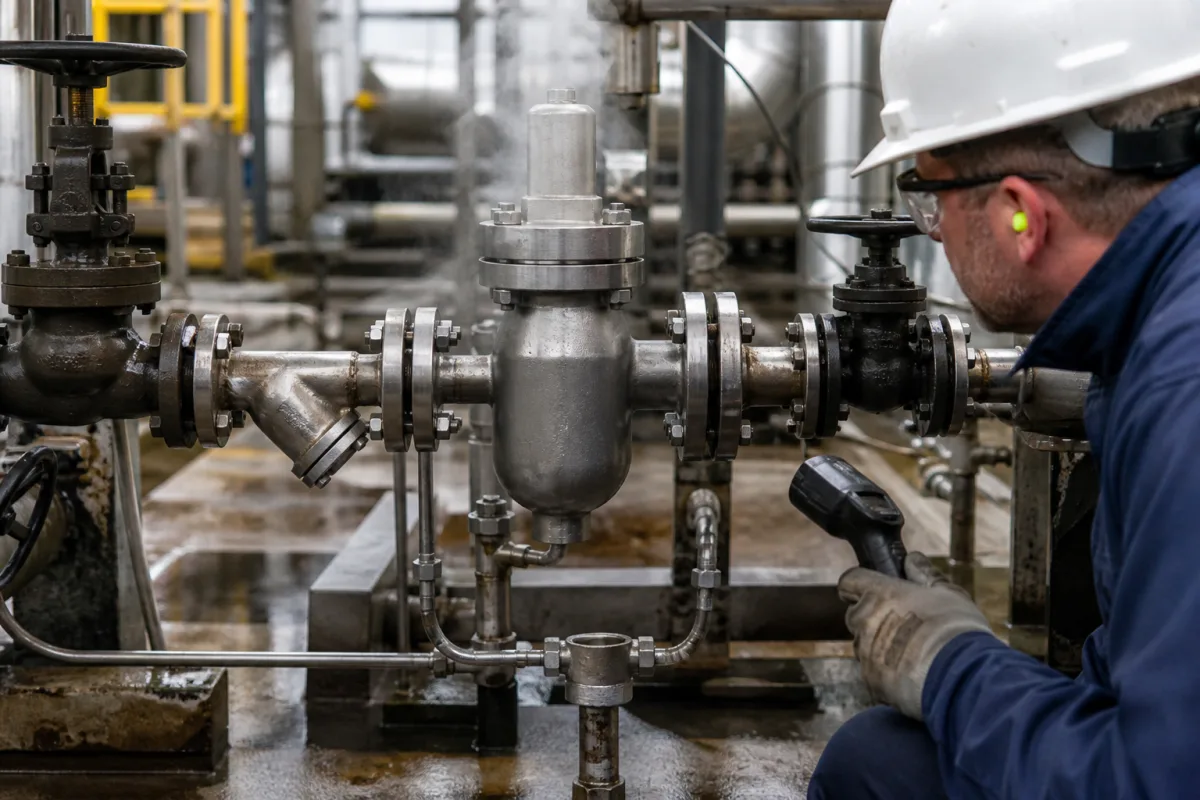
Steam systems · Trap type, layout and failed-trap losses
A steam trap must hold back live steam while letting condensate, air and other gases out. Pick the type for the application, give it a drain pocket, a strainer and a free path to the return line, and test it regularly: the US Department of Energy reports that 15% to 30% of traps may have failed in systems left unmaintained for 3 to 5 years, and a failed-open trap blows steam into the return around the clock.
Thermostatic, mechanical (float and inverted bucket) and thermodynamic steam traps for steam mains, process equipment, heat exchangers and clean-steam service. Steam separators and condensate pumps are outside this page.
CNFX editorial research · Sources checked October 11, 2026 · 7 sources
Spirax Sarco explains that the duty of a steam trap is to discharge condensate, air and other incondensable gases without letting live steam escape, and that all traps fall into three groups classified by ISO 6704: thermostatic, operated by changes in fluid temperature; mechanical, operated by the density difference between steam and condensate, such as ball float and inverted bucket traps; and thermodynamic, relying partly on flash steam formation, such as disc, impulse and labyrinth traps. [2]
Fixed-orifice traps are loosely grouped with thermodynamic traps, but Spirax Sarco notes they are simply a fixed hole and cannot be clearly defined as automatic devices. [2]
Ask the supplier for the trap's discharge capacity at your differential pressure, its maximum allowable and operating pressures, and whether it handles air venting at start-up.
Give the supplier the application (main drainage, heat exchanger, dryer, tracer), steam pressure, condensate load at start-up and running, back pressure in the return line and whether condensate must lift after the trap.
02
Lay out drainage to prevent waterhammer
Spirax Sarco calls waterhammer a symptom of system problems such as failing to remove condensate from high-velocity steam, poorly designed pipework, the wrong trap or a leaking trap; if a trap keeps failing from waterhammer, the layout is probably at fault. It states that "as a general rule, steam mains should be drained at regular intervals of 30 to 50 metres with adequately sized drain pockets", and that the bottom of any riser must also be drained. [3]
Temperature-controlled heat exchangers drain properly only if condensate can flow freely; where condensate must lift after the trap there will be a tendency to waterhammer whichever trap is fitted, and Spirax Sarco advises complementary measures. Strainers ahead of traps arrest scale and dirt and reduce maintenance. [3]
03
Test traps and count what failed traps cost
The US Department of Energy reports that in steam systems not maintained for 3 to 5 years, 15% to 30% of traps may have failed and pass live steam into the return; with scheduled maintenance, leaking traps should be under 5%. It recommends a regular inspection, testing and repair programme, and says to "Consider online monitoring of the most important steam traps or those associated with your most important processes to quickly identify steam loss trends." [1]
DOE's table, from the Boiler Efficiency Institute, gives steam loss through a stuck-open 1/8-inch orifice as 75.8 lb/h at 150 psig; at $10 per 1,000 lb, repairing it saves about $6,640 a year. As an editorial conversion only: that is about 34 kg/h at about 10 barg, or roughly 300 tonnes of steam a year. [1]
Spirax Sarco warns that listening devices, sight glasses and temperature checks can all mislead, because condensate and steam can coexist at the same temperature, and that ultrasonic testers need trained operators; sensors inside or beside the trap that detect steam by conductivity give a clearer result. [4]
04
Ball float and thermodynamic traps, and traps sold among industrial valves
SAFVAL lists ball float and thermodynamic steam traps; Kosen and NTGD list steam traps among valves; VATAC lists steam traps on two sites. Ask for the type, capacity charts and test data rather than relying on the name 'steam trap'. [5][6][7]
05
Trap body and seat, operating element, strainer, isolation valves and drain pocket
Isolation valves and a test point are part of the station because Spirax Sarco finds listening, sight glasses and temperature checks misleading; a sensor chamber in or beside the trap gives a clearer test. [4]
Part
Role
Fix in the order
Trap body and seat
Holds the valve that opens to condensate and closes to steam. [2]
Body material, pressure rating and connections.
Operating element
Thermostatic element, float or bucket, or disc. [2]
Size and orifice, PMA and TMA, capacity at your differential pressure and body material for a trap order
Only two rows carry a published figure, DOE's 75.8 lb/h loss through a stuck-open 1/8 in orifice and Spirax Sarco's 316L hygienic trap; capacity has to be read from the maker's chart at your own differential pressure. [1][2]
Field
What it means and published values
Ask the supplier for
Nominal diameter (mm)
Connection size; capacity comes from the orifice and type.
Size and orifice.
Operating pressure (MPa)
Steam pressure at the trap.
Operating pressure range.
Maximum allowable pressure (MPa)
Body rating.
PMA and TMA.
Maximum operating temperature (°C)
Steam temperature at pressure.
Maximum operating temperature.
Minimum operating temperature (°C)
Frost exposure.
Frost protection.
Capacity (kg/h)
Must cover start-up and running condensate loads.
Capacity at your differential pressure.
Leakage rate (% of rated capacity)
Failed-open traps lose steam, e.g. 75.8 lb/h through 1/8 in at 150 psig. [1]
Steam loss test data.
Body material
316L stainless traps are offered for hygienic and clean-steam duties. [2]
Body material.
Connection type
Must match the pipework.
Connection type and standard.
Weight (kg)
Pipe support.
Mass.
07
Send the application, pressures and loads together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Application: [steam main; heat exchanger; dryer; tracer; clean steam]
Steam: [pressure; temperature; superheat]
Loads: [start-up and running condensate kg/h]
Return: [back pressure; lift after trap; open or closed return]
Type: [thermostatic, float, inverted bucket or thermodynamic]
Station: [strainer; isolation valves; test point or sensor]
Documents: [capacity chart; PMA/TMA; materials; steam loss test]
9 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What are the main types of steam trap?
Spirax Sarco lists three groups under ISO 6704: thermostatic (temperature), mechanical such as float and inverted bucket (density) and thermodynamic such as disc traps (fluid dynamics). [2]
How much steam does a failed trap waste?
DOE's table gives 75.8 lb/h through a stuck-open 1/8-inch orifice at 150 psig, about $6,640 a year at $10 per 1,000 lb. [1]
How often should steam mains be drained?
Spirax Sarco's general rule is every 30 to 50 metres from adequately sized drain pockets, and at the bottom of every riser. [3]
Sources and what still needs a direct check
Sources checked 2026-10-11. The DOE steam tip sheet is a US government source (2012). Spirax Sarco is a steam trap manufacturer; its learning pages describe trap types, selection and testing. Supplier pages describe their own offers. ISO 6704 and ISO 5117 were not read for this page.