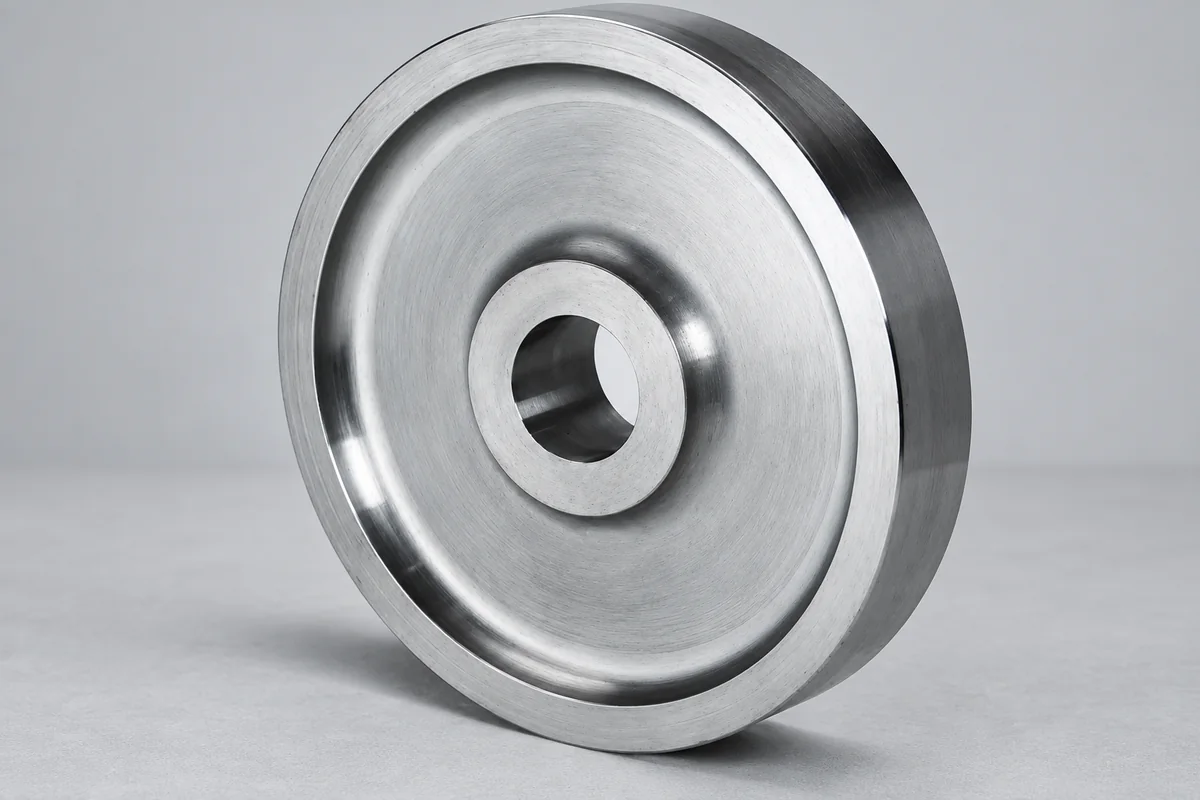
Custom carbon, alloy and stainless steel forgings made to order · Choosing the ASTM product specification and class, melting and remelting route, hot, warm or cold forging, heat treatment, chemical and mechanical tests, ultrasonic examination and certification
A steel forging is a part shaped from a heated (or, for some classes, cold or warm) steel ingot, bloom or billet by compressive working on a hammer or press, in open dies or closed dies, then heat treated, tested and machined to the buyer's drawing — shafts, discs, rings, flanges, blocks, gear blanks and valve bodies among them. Ask three things first: which product specification and class or grade the part must meet, what size, shape and weight it is and how much machining allowance it carries, and which heat treatment, mechanical tests, ultrasonic examination and certification the order requires.
Custom carbon, alloy and stainless steel forgings supplied to drawing: open-die and closed-die forgings, seamless rolled rings, shafts, discs, blocks and hollow forgings. Forging presses and hammers (see hydraulic forging press), forging ingots (see high-strength forging steel ingot) and specific forged products with their own pages, such as forged steel flanges and forged steel valve bodies, are outside this page except where compared.
CNFX editorial research · Sources checked October 11, 2026 · 8 sources
Name the product specification, class and heat treatment
ASTM A788/A788M-24 sets the general requirements that apply to steel forgings ordered to any of a list of ASTM product specifications unless the product specification states otherwise — among them A266 carbon steel for pressure vessel components, A291 pinions, gears and shafts for reduction gears, A336 alloy steel for pressure and high-temperature parts, A470 vacuum-treated turbine rotors and shafts, A473 stainless steel, A508 quenched and tempered vacuum-treated pressure vessel forgings, A668 general industrial use, A729 railway axles and A837 carburizing forgings. Where they conflict, the product specification prevails, and the purchaser may add requirements only by agreement in the order. [1]
ASTM A668/A668M-23 covers untreated and heat-treated carbon and alloy steel forgings for general industrial use, excluding hot-rolled or cold-finished bars, and points to other specifications for pressure vessels, railroad use, turbine generators and gearing. It lists six carbon steel classes (A–F) and seven alloy steel classes (G, H and J–N): Class A may be supplied without heat treatment; B, C, D and G are annealed, normalized, or normalized and tempered; E is normalized and tempered or double-normalized and tempered; F is quenched and tempered or normalized, quenched and tempered; H is normalized and tempered; J is normalized and tempered or normalized, quenched and tempered; and K, L, M and N are normalized, quenched and tempered. A suffix H allows supply after hardness testing only. [2]
Give the supplier the product specification and year, class or grade, the drawing with forged and finished dimensions and machining allowance, weight, quantity, heat treatment condition, and any supplementary requirements you are adding.
02
Set the melting route, tests, examination and certification
A788 allows primary melting by electric furnace, basic oxygen, vacuum induction (VIM) or open hearth, optionally with separate degassing or refining and with secondary electroslag (ESR) or vacuum arc (VAR) remelting; it classes forging as cold-worked, hot-cold-worked or hot-worked by forging temperature, requires forgings to cool before reheating for heat treatment, covers heat and product chemical analysis and tension and hardness tests (including elongation and reduction of area), and does not allow repair welding unless the product specification permits it. The certification must quote the number and year of A788 and of the product specification, and forgings supplied partly complete must be certified and marked to show which requirements have been met. [1]
A668 requires heat and product analyses conforming to its limits for manganese, phosphorus and sulfur, and tensile strength, yield, elongation, reduction of area and Brinell hardness to the class. ASTM A388/A388M-23 covers contact pulse-echo ultrasonic examination of steel forgings by straight-beam techniques — with sensitivity set by back reflection, reference blocks or the distance-gain-size (DGS) method — and by angle-beam techniques for rings and hollow forgings, and applies whenever the inquiry, contract, order or specification calls for it. [2][3]
One Chinese forge's product listings show how suppliers describe the route: melting by EF+LF+VD (electric furnace, ladle furnace, vacuum degassing), forging ratios of at least 3 or above 4, 4 t and 8 t hammers for smaller parts, heat treatment of N+T or Q+T, and materials such as A105, LF2, F304/304L, F316/316L, F51, F53, 34CrNiMo6 and 50Mn. [4]
State the melting and remelting route, any vacuum degassing, minimum forging reduction, heat treatment and test locations, mechanical properties, ultrasonic examination standard and acceptance level, other NDT, dimensional inspection, marking, and the certificate type and contents.
03
Choose the forging type for the part
Forges in the supplier list below describe open die forgings, closed die forgings and seamless rings (Jiangyin Xinyu); heavy shafts, gear blanks, rolls, turbine rotor forgings, flanges and cylinders (Jiangsu Huixuan, Rongli); ring forgings, tubesheets and wind power and pressure vessel forgings (Jiangyin Fangyuan); and a forged range from bars, blocks and discs to rings, rotors and valve bodies (Epowermetals). [5][4][6][7][8]
Editorial note: the product specification follows from the service — pressure-retaining parts, turbine and generator rotors, gearing and railway axles each have their own ASTM specifications under A788, with A668 for general industrial forgings [1][2]. Name it before asking for prices so every bidder quotes the same tests.
Describe the part (shaft, disc, ring, block, hollow, flange, gear blank), whether open-die, closed-die or ring rolling is expected, the service (pressure, rotating, gearing, structural), and annual volumes.
04
Know what a forging order controls
This is a functional reference built from the sources cited; it is not one forge's procedure.
Specification numbers and years; extent of completion. [1]
Certificate type.
05
Fill the order fields with values for your part
A forging enquiry needs values from your drawing and service. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Field
What it means and published values
Ask the supplier for
Product specification
A788 with a product specification such as A668, A266, A336 or A508. [1]
Not allowed unless the product specification permits. [1]
Confirmation.
Size and weight
Set by your drawing.
Forged and finished size, weight.
06
Send the drawing, specification and test data together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Part: [drawing; forged and finished sizes; weight; quantity]
Specification: [ASTM or other; year; class or grade]
Route: [melting; degassing; forging reduction]
Heat treatment: [condition; test location]
Tests: [tension; hardness; impact; UT standard and level]
Documents: [certificate type; marking; inspection witness]
These companies list steel forgings or forging services on their websites. Their pages show what they offer, not tested performance.
Jiangsu Huixuan New Energy Equipment Co., Ltd.
Manufacturing site to be confirmed for the order
Lists heavy steel forgings, open die forgings, alloy and carbon steel forgings, axle shafts, gear blanks, forged rolls and turbine rotor forgings, with melting routes, forging ratios and heat treatments on its product listings.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, forge, specification compliance and certificates for your order. How we source and review
· Page last updated 11 October 2026
Which ASTM specification covers general industrial steel forgings?
ASTM A668, with six carbon and seven alloy steel classes; A788 sets the general requirements. [2][1]
Is repair welding allowed on steel forgings?
Under A788 it is not allowed unless the product specification permits it. [1]
How are steel forgings ultrasonically examined?
ASTM A388 covers contact pulse-echo straight-beam and angle-beam examination, including the DGS method. [3]
Which melting routes are allowed for ASTM steel forgings?
Electric furnace, basic oxygen, VIM or open hearth, with optional degassing and ESR or VAR remelting. [1]
Sources and what still needs a direct check
Sources checked 2026-10-11. The ASTM pages are public scope summaries of the standards; supplier pages describe what each company offers. Requirements for your part must come from the full specification text and the supplier's offer.