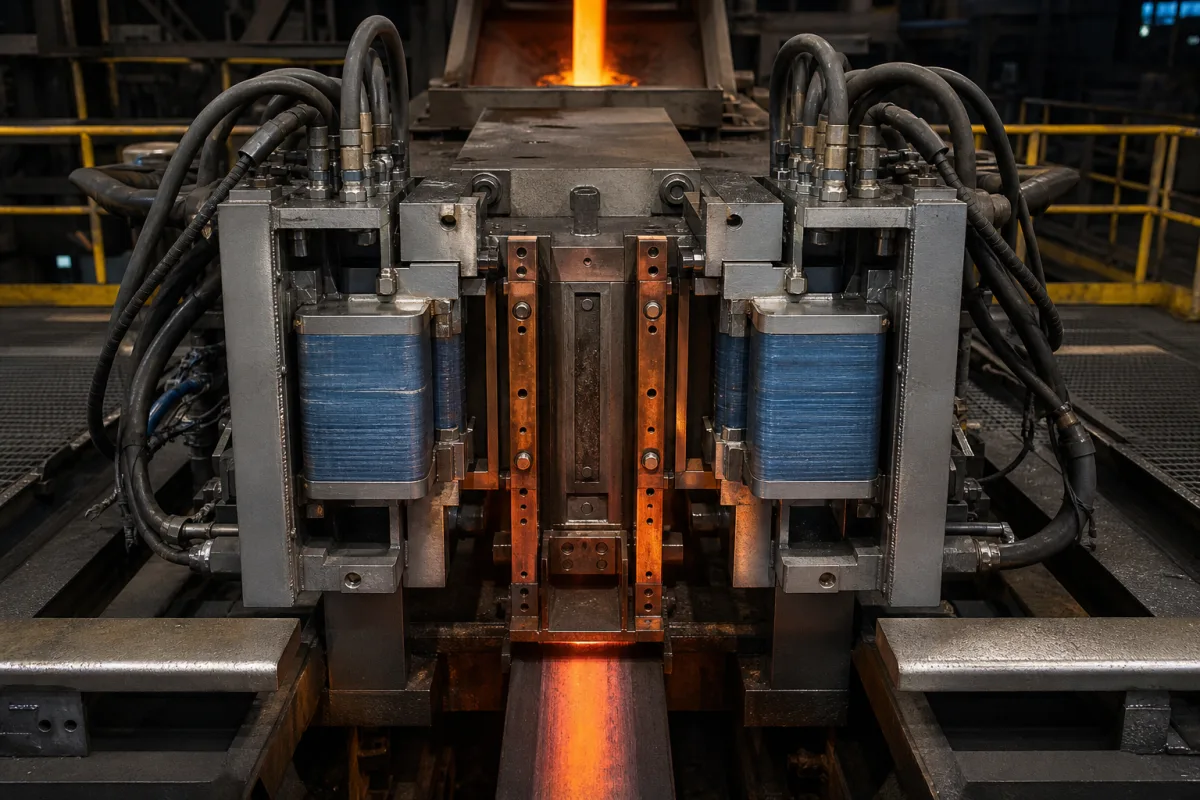
Industrial-grade continuous casting mold electromagnetic brake system
Electromagnetic brakes (EMBR) for slab moulds · A static DC magnetic field across the mould brakes the submerged-entry-nozzle jets and calms the meniscus: coil arrangement on the wide faces, thyristor converter, water-cooled hollow copper coils, field strength and the risk of flow reversal at high fields
A mould electromagnetic brake (EMBR) places a static DC magnetic field across the mould of a slab or thin-slab caster. Moving liquid steel crossing the field is slowed, so the jets from the submerged entry nozzle are braked and the meniscus is calmer, cutting mould powder entrapment. Ask three things first: which caster and mould it must fit, what coil layout and field strength the flow needs, and what power, cooling and level-control integration the plant must supply.
Static-field electromagnetic brakes for slab and thin-slab continuous casting moulds, with their coils, power converters, cooling and controls. Electromagnetic stirrers, mould oscillators (see heavy-duty continuous casting mold oscillator), mould level sensors and industrial clutch-brake units (see industrial electromagnetic clutch brake unit) are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
ABB describes its EMBR as using a steady DC magnetic field to control liquid steel flow inside the mould, braking the SEN jets and helping maintain a uniform velocity profile across the strand; the braking force rises automatically with jet speed and turbulence. It offers EMBR for all thin-slab mould designs, new or modernised, including compatibility with electromagnetic mould level control systems, and says EMBR is installed on about 40% of thin-slab strands. [1]
ABB claims lower meniscus turbulence cuts mould powder entrapments by up to 90%, that a calmer, hotter meniscus reduces surface imperfections at higher casting speeds, that reduced level fluctuation lessens copper plate thermal cycling and extends mould life, and that controlled flow reduces inclusion penetration depth so thin-slab casters can approach the cleanliness of conventional slab casters. [1]
A 2021 study in Metallurgical and Materials Transactions B modelled a ruler-type brake placed at the SEN port level, based on HZDR mini-LIMMCAST experiments, for field strengths up to 441 mT (Hartmann number about 600), taking the conductivity of the solidified shell into account. [2]
Give the supplier the caster type (thin slab or conventional slab), mould width and thickness range, casting speed range, SEN design and port position, steel grades, the existing mould level control system, available power supply, cooling water quality, flow and temperature, and space around the mould and oscillator.
02
Specify power, cooling and field limits
ABB's EMBR uses two- or four-part coils on each mould wide face, fed by a dedicated thyristor converter for stable current. The coils have no mechanical contact with the strand and are built from hollow copper conductors with internal water cooling, dry external insulation and a protective silicone-rubber casting. [1]
The 2021 study found that increasing the applied field can reverse the flow direction at the meniscus, forming a multi-roll pattern: induced currents accelerate steel in previously slow regions, creating an opposite vortex near the jet that grows until it reaches the surface. Ask the supplier how field strength will be set against casting speed and width to avoid unwanted flow reversal. [2]
An industrial-scale study in Metals (13(1):167, 2023) modelled a multi-mode electromagnetic brake on a 1,520 mm × 90 mm funnel thin-slab mould casting at 6 m/min, computing flux density at different coil currents and checking the model against nail-board measurements on the production caster. With the magnetic pole current at no less than 800–600 A, the maximum liquid-level fluctuation fell from 18 mm without the brake to under 5 mm, and the authors judged 800–600 A a reasonable setting given braking effect and production cost. [3]
Editorial calculation: at 6 m/min a 1,520 mm × 90 mm strand passes about 0.82 m³ of steel per minute (1.52 × 0.09 × 6), about 6.4 t/min at an assumed 7.8 t/m³, which shows the jet energy the brake has to calm in a thin-slab mould. [3]
03
Ask where the peak field sits relative to the nozzle ports
A University of Illinois paper by Thomas, Singh, Chaudhary and Vanka (Fifth Baosteel Biennial Academic Conference, 2013) modelled a single-ruler EMBr with Large Eddy Simulations validated against a GaInSn model and plant conditions. It concludes that placing the strongest field "directly across the nozzle ports" leads to unstable large-scale, low-frequency vortical structures, while moving the maximum field below the nozzle bottom deflects the jet consistently upward and gives more stable flow and higher surface velocity. [4]
The paper also found that the solidified steel shell, which conducts current, stabilises the flow with EMBr compared with insulated walls [4]. The HZDR study on this page reports that a ruler-type brake can generate reverse meniscus flow [2], and the industrial study in Metals gives level fluctuations falling from 18 mm without the brake to under 5 mm [3]. Read together, the field strength alone does not settle the result; ask the supplier for the vertical field profile, the height of its peak relative to the nozzle ports at your submergence depth, and any modelling or plant trial on a similar mould.
ABB states that its EMBR braking force rises automatically with jet speed and turbulence [1], and the Illinois authors note that induced electromagnetic force varies with flow strength, giving a "theoretical ability to be self-stabilizing" that is "difficult to achieve" in practice [4]. Ask how the supplier sets coil current and position for each casting speed and width.
Editorial calculation: in the paper's Table 1 the real caster is six times the model in width (840 ÷ 140) and thickness (210 ÷ 35), and the 92 mm and 121 mm model field positions correspond to about 552 mm and 726 mm below the top surface at that scale. [4]
Parameter (Table 1 of the paper)
GaInSn model
Real caster
Mold width x thickness
140 mm x 35 mm
840 mm x 210 mm
Casting speed
1.35 m/min
1.64 m/min
Volume flow rate / inlet velocity
110 mL/s / 1.4 m/s
4.8 L/s / 1.7 m/s
SEN submergence depth
72 mm
432 mm
Nozzle port (width x height)
8 mm x 18 mm
48 mm x 108 mm
Stuart number (based on mold width)
4.84
4.84
Field positions studied (model)
Peak 92 mm below top surface (across ports) and 121 mm (below nozzle)
Scaled by a factor of six
Values are from the University of Illinois BAC2013 paper (text extracted from the PDF on the Continuous Casting Consortium site); it is a modelling study, not a supplier specification.
Hunan Zhongke Electric's product page lists electromagnetic brakes for slab casting moulds; put the questions below to it and to any other bidder.
Ask any supplier for coil layout and field distribution, maximum flux density at the mould centre, current and converter rating, cooling water flow, pressure and quality, insulation and protection, control interface with mould level and caster automation, flow modelling for your conditions, installation scope and references.
Field strength, peak height and coil cooling in an EMBR offer
Ask for flux density and field peak position together: the Illinois study ties stable mould flow to the peak sitting below the nozzle ports, not to field strength alone. [4]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How does a mould electromagnetic brake work?
ABB's EMBR applies a steady DC magnetic field that brakes the SEN jets and keeps a uniform velocity profile in the mould. [1]
Can a stronger field always improve mould flow?
No; a 2021 study found stronger fields can reverse meniscus flow and form a multi-roll pattern. [2]
How are EMBR coils built?
ABB uses two- or four-part coils per wide face of hollow, water-cooled copper conductors fed by a thyristor converter. [1]
How much can an EMBr calm the mould level?
A 2023 Metals study of a 1,520 × 90 mm funnel mould at 6 m/min found maximum level fluctuation fell from 18 mm to under 5 mm with pole currents of at least 800–600 A. [3]
Where should the electromagnetic brake field be placed in a slab mould?
A 2013 University of Illinois modelling study found that placing the strongest ruler field directly across the nozzle ports caused unstable low-frequency flow and should be avoided, while placing the peak below the nozzle gave more stable flow and higher surface velocity at deep submergence. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. ABB makes the EMBR mould brake; HZDR lists a 2021 peer-reviewed study of brake-induced flow.