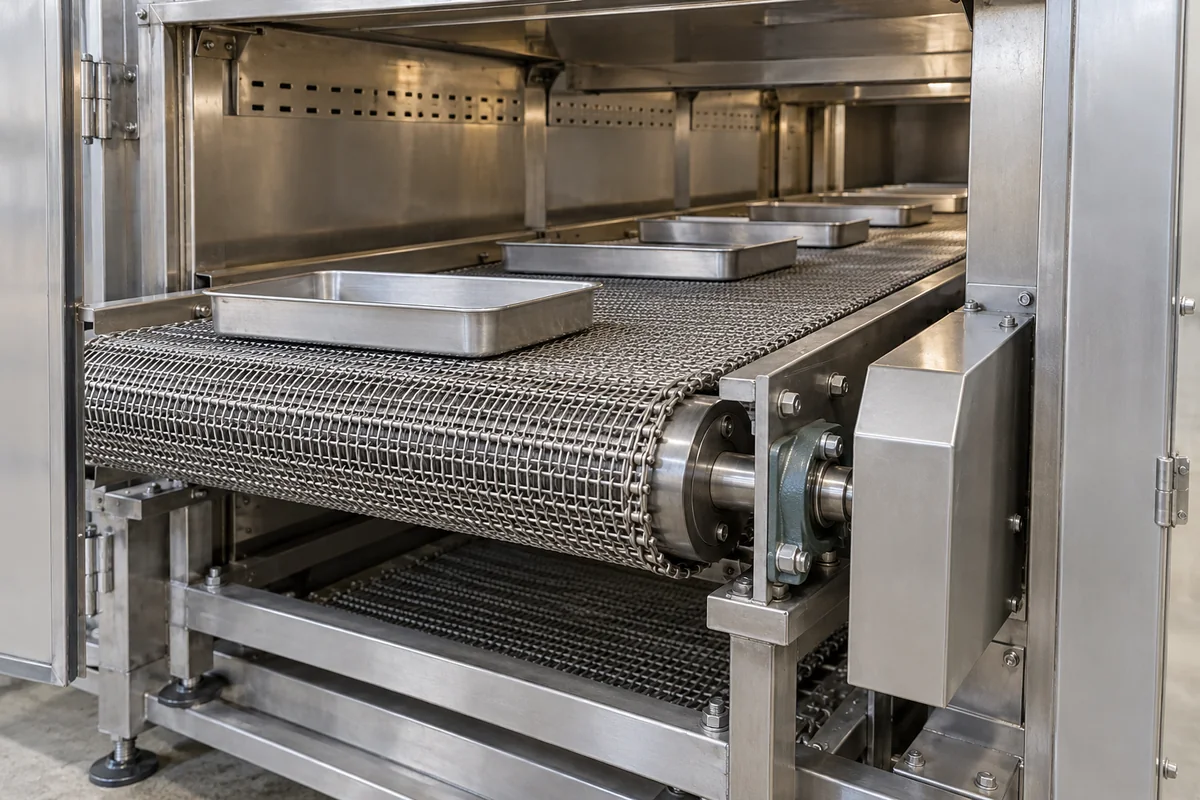
Conveyor inside a drying tunnel: open-mesh PTFE belt, tracking and speed control that set the time in heat
Dryer tunnel conveyors · PTFE-coated glass and Kevlar open-mesh belts, lacing, aligner tracking, DC speed control and time in heat
In a conveyor dryer the belt is the part that touches every print: it carries garments, films or sheets under the heaters, lets air pass through, and its speed decides how long each item stays in the heat. This page covers that conveyor as a component — the open-mesh belt, its lace joint, the aligner and tension setting, and the variable-speed drive — whether it is specified with a new tunnel or bought as a replacement or extension.
Conveyors fitted inside drying and curing tunnels: open-mesh PTFE-coated fibreglass and Kevlar belts, lacing, tension and tracking hardware, and variable-speed drives that set the dwell time. Complete infrared drying and curing tunnels are covered on the IR drying/curing tunnel page; enclosed batch curing ovens on the Curing chamber page; general belt, roller and chain conveyors on the Conveyor systems page.
CNFX editorial research · Sources checked October 17, 2026 · 5 sources
Open-mesh belt grades: coating, thickness, strength and the 260 °C ceiling
Taconic describes open-mesh belting as built to let air move through the belt during drying, curing and cooling while it conveys, and lists it for drying, curing, textile processing and screen printing. [1] The table sets Taconic's published grades beside PAR Group's blue PTFE glass mesh.
Taconic states that its table values are "averages based on the authoritative testing of several lot numbers" and are intended for comparison only. [1] PAR Group gives a temperature resistance of −73 to +260 °C, notes that PTFE begins to soften at 260 °C with increased wear, and that fumes are given off somewhat above 300 °C; it supplies the mesh up to 3,200 mm wide and 50 m long, as endless belts or with joining strips. [3][2]
Editorial calculation: 3,000 N per 5 cm is 600 N/cm; at 1 lb/in = 1.751 N/cm that is about 343 lb/in, against Taconic's 225 lb/in warp strength for 8303 glass mesh and 450 lb/in for the Kevlar 8305K. The figures come from different publishers and test conditions, so treat them as a starting point for asking each supplier for the same test basis. [3][1]
Specify width, endless length or lace type, mesh size, coating and reinforcement (glass or Kevlar), edge treatment and the maximum temperature the belt will see under the heaters.
02
Belt speed expressed as time in heat
Vastex sets cure with three variables: belt speed, temperature and heater height. Its EconoRed manual relates the DC voltage on the belt motor to time through the heat chamber, and tells the operator to verify each machine's label chart with a stopwatch. [4]
For plastisol, the manual gives an ink cure temperature of 310–320 °F (154–160 °C), a recommended starting point of 800 °F (427 °C) set point, 3 in heater height and about 30 s in the chamber, with 20–25 s as a starting point elsewhere in the same manual; for water-based and discharge inks it reports cure times of 50 to 90 s. [4]
The ERVP-III-24 brochure lists a 24 in (61 cm) wide belt, 4.5 ft (137 cm) chamber length and 10,800 W, and states capacities with plastisol at 25 s and water-based ink at 50 s; more chambers can be added in 4.5 ft modules with belt extensions in 18 in (46 cm) increments, and a rear idler is required over 17 ft. [5]
Editorial calculation: with the 137 cm chamber and 25 s in heat, the belt moves at 137 / 25 ≈ 5.5 cm/s, or about 3.3 m/min. Doubling the heated length to 275 cm at the same 25 s dwell gives about 6.6 m/min, which is why added chambers raise belt speed rather than dwell. [5]
Lace joint, sag and aligner tracking on a PTFE mesh belt
The Vastex manual describes the belt as Teflon-coated fibreglass joined with an alligator lace and a steel pin, with a top and bottom side, routed over every brace and over the aligner. [4]
Tension is set by raising both sides of the aligner roller equally; the manual calls 1 to 2 in of sag on the underside desirable and warns against over-tightening. Tracking is corrected in small increments while the belt runs, and the belt need not be perfectly centred but must not hang over either pulley edge. [4]
The drive is a 130 V DC gear motor at the rear turning the rear pulley through a #35 chain, with a digital voltmeter showing the voltage sent to the motor. The belt must keep moving while the heaters are above 300 °F (149 °C), and at shutdown the conveyor stays on until the heaters have dropped to that temperature. [4]
The maintenance table lists belt tracking and belt condition among the checks, together with oiling the drive chain. [4] PAR Group advises not folding or creasing the PTFE glass mesh when handling and installing it. [3]
04
Belt and drive details for the dryer builder
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Belt: [width; endless length; mesh; glass or Kevlar; coating]
Joint: [lace and pin; endless; joining strip]
Temperature under the heaters: [°C]
Drive: [motor; speed range; display]
Heated length and dwell needed: [m; seconds]
Tracking: [aligner type; edge guides]
Quantity: [belts; spares]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 17 October 2026
Buyer questions
What temperature can a PTFE-coated glass mesh dryer belt take?
PAR Group lists −73 to +260 °C and notes PTFE starts to soften at 260 °C; Vastex says the belt must keep moving while heaters are above 300 °F (149 °C). [3][4]
How tight should a dryer conveyor belt be?
The Vastex manual calls 1 to 2 in of sag on the underside desirable and warns against over-tightening; tension is added by raising both sides of the aligner roller equally. [4]
How is belt speed set for a given cure time?
Vastex relates belt-motor voltage to time through the chamber on a label chart, for example 25 s at 60 V and 50 s at 30 V on its example chart, and says to confirm with a stopwatch. [4]
Sources and what still needs a direct check
Sources checked 2026-10-17. Belt figures come from Taconic's open-mesh range table and PAR Group's datasheet; speed, tracking and dwell come from the Vastex EconoRed manual and brochure.