Editorial Technical Reference

Upper Blade Holder

This page explains how Upper Blade Holder is classified within Machinery and Equipment Manufacturing. Technical values and manufacturer relationships are research references; confirm the current specification and supplier evidence for each order.

Technical Definition & Core Assembly

A structural component that securely positions and supports the upper stripping blade within a stripping blade assembly.
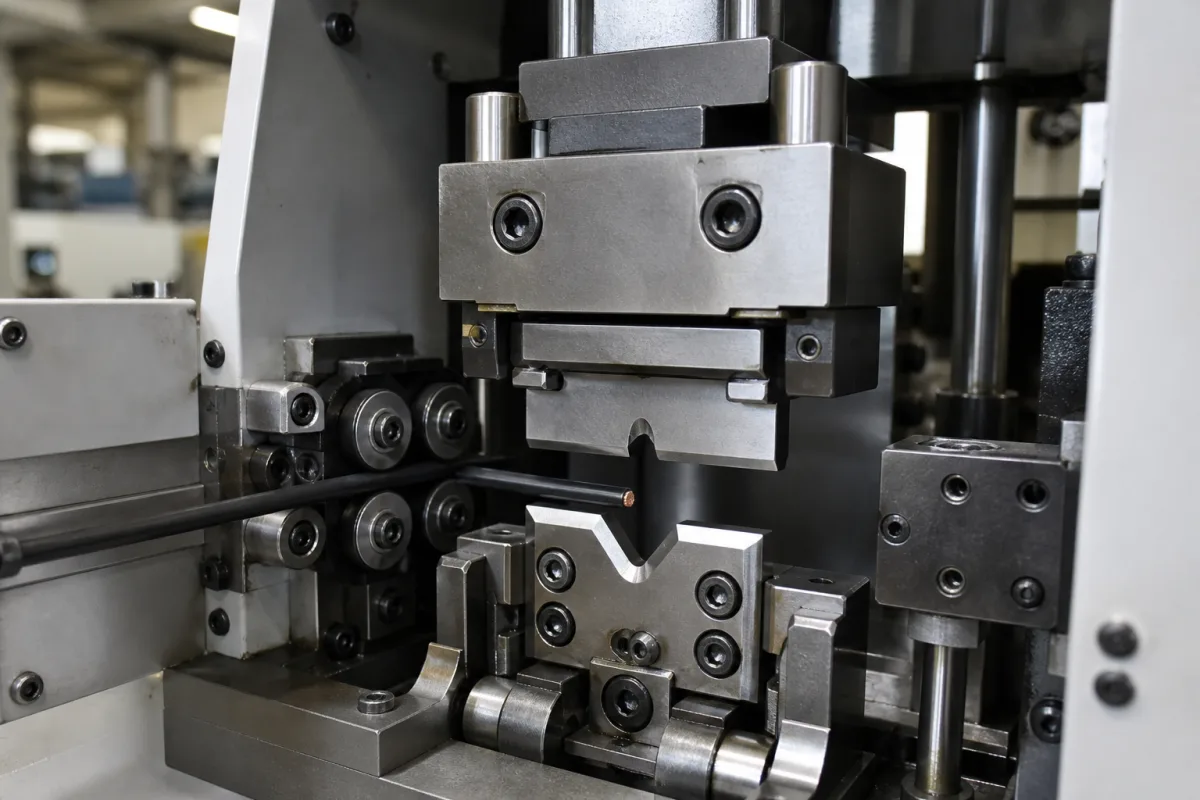
Upper Blade Holder in a manufacturing environment
Representative product image. Confirm appearance and specifications with the manufacturer.

Product Specifications

Technical details and manufacturing context for Upper Blade Holder

Definition
The Upper Blade Holder is a critical component of the Stripping Blade Assembly, designed to rigidly mount and align the upper stripping blade. It ensures precise blade positioning relative to the material being processed, maintains consistent blade angle and pressure during operation, and provides structural stability to prevent blade deflection or vibration during high-speed stripping operations. The holder is typically mounted to the machine frame or actuator. It clamps or bolts the upper stripping blade in place, maintaining its fixed position. During the stripping cycle, it transfers operational forces from the machine to the blade while resisting reactive forces from the material, ensuring the blade performs its cutting or stripping function accurately and consistently. This component is manufactured from tool steel or hardened alloy steel, with a typical material grade of 45# carbon steel per GB/T 699, hardness of 38–42 HRC per GB/T 230.1, and a Ni-P surface treatment per GB/T 13913 for corrosion resistance. Key dimensional parameters include an overall length of 120–200 mm, width of 50–80 mm, height of 30–60 mm, mounting hole diameter of 10–16 mm (for M10–M16 bolts per GB/T 5277), and mounting hole spacing of 80–120 mm. Precision requirements include flatness ≤0.05 mm and parallelism ≤0.03 mm per GB/T 1184, and surface roughness Ra 0.8–1.6 μm per GB/T 1031. The operating temperature range is -20 to 80 °C, and weight ranges from 1.5 to 3.5 kg depending on size. These values are reference ranges; actual specifications must be confirmed with the legal manufacturer or supplier for the specific model and application. The holder is designed for use in machinery and equipment manufacturing, specifically within stripping blade assemblies. It is not a standalone product but a component that requires proper integration and verification. Always consult the manufacturer for detailed engineering drawings and installation instructions.
Working Principle
The holder is typically mounted to the machine frame or actuator. It clamps or bolts the upper stripping blade in place, maintaining its fixed position. During the stripping cycle, it transfers operational forces from the machine to the blade while resisting reactive forces from the material, ensuring the blade performs its cutting or stripping function accurately and consistently. The rigid mounting prevents blade deflection and vibration, which is critical for high-speed operations. The holder's flatness and parallelism ensure uniform force distribution across the blade, while surface roughness reduces friction and wear. The operating temperature range and material properties must be matched to the application to avoid premature failure.
Common Materials
Tool Steel, Hardened Alloy Steel
Technical Parameters
ParameterTypical rangeNotes & selection driver
Material Grade45#High-strength carbon steel for durabilityGB/T 699
Hardness38–42 HRCBalanced wear resistance and toughnessGB/T 230.1
Surface TreatmentNi-PCorrosion resistanceGB/T 13913
Overall Length120–200 mmCustomizable per blade assembly
Width50–80 mmMatches blade width
Height30–60 mmAffects stripping clearance
Mounting Hole Diameter10–16 mmFor M10–M16 boltsGB/T 5277
Mounting Hole Spacing80–120 mmEnsures stable mounting
Flatness≤0.05 mmCritical for blade alignmentGB/T 1184
Parallelism≤0.03 mmEnsures uniform stripping forceGB/T 1184
Surface RoughnessRa 0.8–1.6 μmReduces friction and wearGB/T 1031
Operating Temperature-20–80 °CBeyond range may affect material properties
Weight1.5–3.5 kgDepends on size

Ranges are indicative industry figures for RFQ preparation, not a supplier commitment. Confirm every value and standard with the legal manufacturer before ordering.

Components / BOM
  • Blade Clamp Plate Part
    Applies clamping force to secure the blade against the main holder body.
    Material: Hardened Steel
  • Mounting Flange Part
    Provides the interface with bolt holes for attaching the holder to the machine frame or actuator.
    Material: Steel
  • Alignment Pin Part
    Ensures precise positioning of the blade within the holder seat.
    Material: Hardened Steel
  • Holder Body
    The main body the blade seats against and the clamp plate presses onto.

Applied To / Applications

This component is essential for the following industrial systems and equipment:

Industrial Ecosystem & Supply Chain Structure

Complementary Systems
Downstream Applications
Specialized Tooling

Application Fit & Sizing Matrix

Operational Limits
pressure: Up to 10 bar
other spec: Slurry concentration: ≤40% solids by weight
temperature: -20°C to 150°C
Media Compatibility
✓ Metalworking coolants ✓ Industrial lubricants ✓ Water-based cleaning solutions
Unsuitable: Highly corrosive acids (e.g., hydrochloric acid, sulfuric acid)
Sizing Data Required
  • Blade thickness and width
  • Required clamping force
  • Stripping assembly mounting interface dimensions

Reliability & Engineering Risk Analysis

Failure Mode & Root Cause
Fatigue cracking
Cause: Cyclic loading from blade impacts and vibrations exceeding material endurance limit, often exacerbated by stress concentrations at fastener holes or geometric transitions.
Wear and galling at mating surfaces
Cause: Fretting and adhesive wear due to micro-motion between clamped surfaces, insufficient lubrication, or contamination from cutting debris.
Maintenance Indicators
  • Visible cracks or deformation around bolt holes or blade mounting area
  • Abnormal vibration or knocking sounds during operation indicating loose components or structural compromise
Engineering Tips
  • Implement torque verification procedures for all fasteners during reassembly and periodic checks to maintain proper clamping force
  • Apply anti-seize compound to mating surfaces and fasteners during installation to reduce fretting corrosion and ensure consistent clamping

Indicative industry ranges for design and RFQ preparation. Confirm the exact figures and applicable standard with the manufacturer before specifying.

Compliance & Manufacturing Standards

Applicable Standards
ANSI B94.50 - Cutting tools and holders DIN 69871 - Tool holders for automatic tool changers

Quoted from the published standard.

Manufacturing Precision
  • Bore diameter: +/-0.01mm
  • Surface flatness: 0.05mm
Quality Inspection
  • Dimensional verification with CMM
  • Hardness testing (Rockwell C scale)

Manufacturers of Upper Blade Holder

1 company lists this product among what they make. Company figures are quoted from each company's own website; every card states where the relationship came from.

Maxtor Metal
Nanjing, Jiangsu, CN
Listed on the company's own website · profile compiled by CNFX from public sources
Listed there as: “slitter upper blade & holder”
View source page ↗ maxtormetal.com · checked 2026-09-06

Manufacturer listings support early research and capability understanding. They are not certification, ranking, or transaction guarantees.

Share this page
Technical documentation
Request current drawings, revision history, and a signed specification sheet.
Manufacturing capability
Verify equipment lists, process limits, capacity, and representative production evidence.
Inspection readiness
Confirm test methods, calibrated equipment, sampling plans, and traceable reports.
Supplier transparency
Check the legal entity, factory address, ownership, certifications, and direct contacts.

CNFX does not score or rank suppliers. Buyers must verify all claims and documents with the legal manufacturer before ordering.

Supply Chain Compatible Machinery & Devices

Heavy-Duty CNC Plasma Cutting Machine

The Heavy-Duty CNC Plasma Cutting Machine is a standalone industrial device designed for cutting conductive metals such as steel, stainless steel, aluminum, and copper alloys.

Explore Specs →
Automated Powder Coating System

Integrated industrial system for applying dry powder coatings to metal substrates.

Explore Specs →
Centrifugal Pump Impeller

The centrifugal pump impeller is a critical rotating component that converts mechanical energy from the motor into kinetic energy in fluid systems.

Explore Specs →
High-Precision CNC Laser Cutting Machine

Computer-controlled industrial machine using focused laser beams to cut sheet metal with micron-level accuracy.

Explore Specs →

Frequently Asked Questions

What materials are used for the Upper Blade Holder?

The holder is typically made from tool steel or hardened alloy steel. A common material grade is 45# carbon steel per GB/T 699, with a hardness of 38–42 HRC per GB/T 230.1. Surface treatment is Ni-P per GB/T 13913 for corrosion resistance.

What are the key dimensional parameters?

Typical dimensions include overall length 120–200 mm, width 50–80 mm, height 30–60 mm, mounting hole diameter 10–16 mm (for M10–M16 bolts), and mounting hole spacing 80–120 mm. These are reference ranges; confirm exact values with the manufacturer.

What precision requirements apply?

Flatness must be ≤0.05 mm and parallelism ≤0.03 mm per GB/T 1184. Surface roughness is Ra 0.8–1.6 μm per GB/T 1031. These ensure proper blade alignment and uniform stripping force.

How should I verify the holder's suitability for my application?

Check the operating temperature range (-20 to 80 °C), weight (1.5–3.5 kg), and all dimensional parameters against your machine's requirements. Always consult the legal manufacturer or supplier for model-specific specifications and installation guidelines.

Data Basis

Editorial classification, named public sources where available, and source-reviewed manufacturer records.

Preliminary Technical Classification
This page supports structured research, RFQ preparation, and supplier evaluation. It does not replace buyer-led supplier qualification, standards review, or technical approval.
Buyer enquiry

Request manufacturing insight for Upper Blade Holder

Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.

Where it goes
Straight to the CNFX editorial desk, and to the manufacturer if this product is linked to a claimed profile. Nothing is broadcast to a supplier list.
Your details stay here
We do not sell or rent enquiry data, and we do not add you to a mailing list. Used only to answer this request.
No commission, no middleman
CNFX is a directory. We take no cut of any order and never negotiate on a supplier's behalf.
What we don't claim
A listing is not an endorsement. Qualify every supplier and verify every figure yourself before ordering.

Your business information is used only to process this request.

Thank you! Your message has been sent. We'll respond within 1–3 business days.
Sorry, we couldn't send your message. Please try again, or email us at [email protected].

Need to Manufacture Upper Blade Holder?

Compare manufacturer profiles with relevant product and process capability.

Previous Product
Z-axis Ram/Spindle
Last Product
Get QuotesChat