Magnesium alloy billets for extrusion and forging · AZ31B, AZ61A, AZ80A and ZK60A compositions and impurity limits, which alloys suit extrusion and forging, preheat temperature, forging speed and grain growth, and what to require on certificates
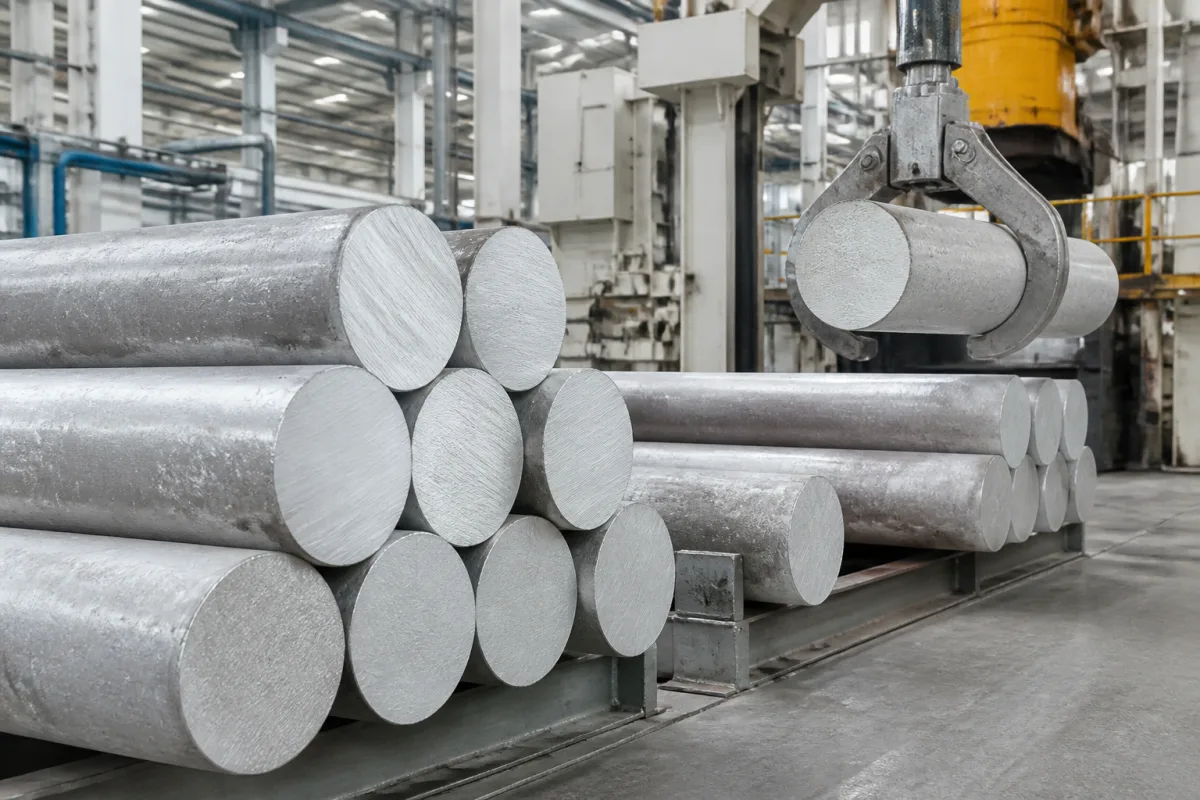
A magnesium alloy billet is a cast or extruded round bar (or slab) of a wrought magnesium alloy supplied as feedstock for extrusion, forging or rolling, chosen for its alloy, purity, structure and size. Ask three things first: which alloy the finished part's strength and the forming route require, which impurity limits and billet condition (cast, homogenised or extruded) the process needs, and what size, tolerances, certificates and handling come with each lot.
Magnesium alloy billets, logs and bar stock for extrusion and forging, cast or pre-extruded, in AZ, ZK, WE and similar wrought alloys. Pure magnesium ingot, magnesium die castings (see magnesium die casting), magnesium sheet and plate, finished forgings and extrusions are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Gontarz and co-authors (Lublin and Częstochowa Universities of Technology and ZOP forging plant, Materials 14:32, 2021) give compositions for three Mg-Al-Zn alloys: AZ31B with 2.5–3.5% Al, 0.6–1.4% Zn and 0.2–1.0% Mn; AZ61A with 5.8–7.2% Al, 0.4–1.5% Zn and 0.15–0.5% Mn; and AZ80A with 7.8–9.2% Al, 0.2–0.8% Zn and 0.12–0.5% Mn; each with at most 0.005% Fe, 0.10% Si, 0.05% Cu and 0.005% Ni. They describe AZ31B as suitable for hot working, at about 240 MPa tensile strength, 150 MPa yield, 9% elongation and 50–55 HB, and note that the alloys differ mainly in aluminium, which strongly affects workability. Round bars are the usual forging billet, with slabs or cast preforms for flatter parts. [1]
TMS (Materials Technology@TMS) charts list AZ31B, AZ61A, AZ80A, ZK60A and others among magnesium extrusion alloys and AZ31B, AZ61A, AZ80A, ZK60A, ZK31, WE43A and WE54A among forging alloys, with ZK60A given as 4.8–6.2% Zn and at least 0.45% Zr. [2]
Editorial note: name the alloy designation and the specification it must meet, because the impurity limits for iron, nickel and copper govern corrosion behaviour; ask for a cast or lot analysis covering every listed element.
For rare-earth alloys made as large billets, a 2026 study (Materials 19(2):282) cast a 330 mm diameter Mg-9.4Gd-5.8Y-1Zn-0.5Zr billet by semi-continuous casting with an electromagnetic vibration field, at 760–770 °C and 31–35 mm/min. Grain size across the billet ranged from 117 to 130 µm and Gd and Y segregation stayed below 3%. Homogenising at 520 °C for 5 h dissolved the grain-boundary eutectic and gave 208.4 MPa tensile strength with 24.4% elongation; the authors also tested 470 °C and holding times of 5–20 h. [3]
Editorial note: for large rare-earth billets, ask the supplier for grain size and Gd/Y segregation measured at the centre, mid-radius and edge, and for the homogenisation temperature and time applied before shipment. [3]
For a rare-earth wrought grade sold as feedstock, Luxfer MEL Technologies lists Elektron RotaMag 43 (UNS M18434, ASTM WE43C) with 3.7–4.3% yttrium, 2.3–3.5% rare earths and at least 0.2% zirconium, supplied as rolled plate, forging feedstock and extruded bar, section and profile under AMS 4485 and ASTM B107/B107M for extrusions. For extruded bar in the artificially aged T5 condition it gives longitudinal specification minima (A-basis) of 195 MPa 0.2% proof stress, 303 MPa tensile strength and 6% elongation, states that T5 properties depend on the extruded profile, and reports up to 300 MPa proof, 375 MPa tensile strength and 11% elongation demonstrated. Listed physical values are specific gravity 1.83, modulus 44.1 GPa, melting range 540–640 °C and Brinell hardness 70–90, with an axial fatigue value (ASTM E466, R=0.1) of 195 MPa at 50 million cycles for extruded bar; Luxfer rates the alloy for use up to 250 °C. [4]
Give the supplier the alloy designation and specification, forming route (extrusion, forging, rolling), billet condition (as-cast, homogenised, extruded), diameter or section and tolerance, cut length, surface condition (as-cast, scalped, machined), grain size or structure requirement, ultrasonic or other inspection, chemical and mechanical certificates, packing against moisture, and quantity per lot.
02
Set preheat, forging speed and structure
The same study notes that magnesium alloys are highly strain-rate sensitive with a narrow forging temperature window, so they are forged mainly on low-speed hydraulic presses with heated tools. Upset tests on 20 mm × 30 mm specimens preheated to 350, 410 and 450 °C, on a screw press at 0.5 m/s and a hammer at about 5 m/s with tools at about 300 °C, showed AZ31B workable at 410 °C on both machines, AZ61A satisfactory on the screw press but only for simple shapes on the hammer, and AZ80A unsuitable for either high-speed machine. Grain size grew with temperature: ASTM grain size number 12 at 350 °C and 8–11 at 450 °C. For alloys prone to grain growth forged in a sequence of operations, the cited guidance is to lower the forging temperature by about 15–20 °C in each successive operation and to water-cool forgings to stop recrystallisation. [1]
Editorial calculation: using the ASTM E112 values in the paper, grain size number 12 corresponds to an average diameter of 5.6 µm and numbers 8–11 to 22.5–7.9 µm, so raising preheat from 350 °C to 450 °C coarsened the grains up to about four times in diameter in these tests. [1]
Editorial note: if the billet will be forged, ask the supplier for the recommended preheat range for the alloy and condition supplied and whether the billet is homogenised, and plan press speed and die heating with the forger.
03
Find magnesium alloy billet manufacturers
No manufacturer record has been reviewed for this product yet. Send your specification and CNFX will match it against manufacturer records.
04
Compare the alloy options
Values from the sources cited; check the current specification for your market.
Extruded T5 minima 195 MPa proof, 303 MPa UTS, 6%; also forging feedstock. [4]
05
Fill the specification fields with values for your parts
A magnesium billet quotation needs values for your parts and process. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, cast house, certificates and scope for your order. How we source and review
· Page last updated 13 October 2026
Buyer questions
Which magnesium alloy is easiest to forge?
In one study AZ31B forged well at 410 °C on both a screw press and a hammer, while AZ80A could not be forged at those speeds. [1]
Why are iron and nickel limited in magnesium billets?
The AZ alloy compositions cited limit Fe and Ni to 0.005% and Cu to 0.05%; ask for certified analysis against your specification. [1]
Which magnesium alloys are used for extrusion and forging?
TMS lists AZ31B, AZ61A, AZ80A and ZK60A among both extrusion and forging alloys. [2]
How large can a cast magnesium alloy billet be?
A 2026 study cast a 330 mm diameter rare-earth magnesium billet with grain size 117–130 µm and Gd/Y segregation below 3%. [3]
What strength does an extruded rare-earth magnesium bar reach?
Luxfer gives longitudinal T5 minima of 195 MPa proof stress, 303 MPa tensile strength and 6% elongation for extruded Elektron RotaMag 43, and notes that properties depend on the extruded profile. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. The Materials papers report laboratory and plant casting and forging tests; TMS charts summarise alloy uses; the Luxfer MEL Technologies datasheet gives specification minima and physical data for one rare-earth wrought grade. Specifications and certified values for your order come from the applicable standard and the supplier.