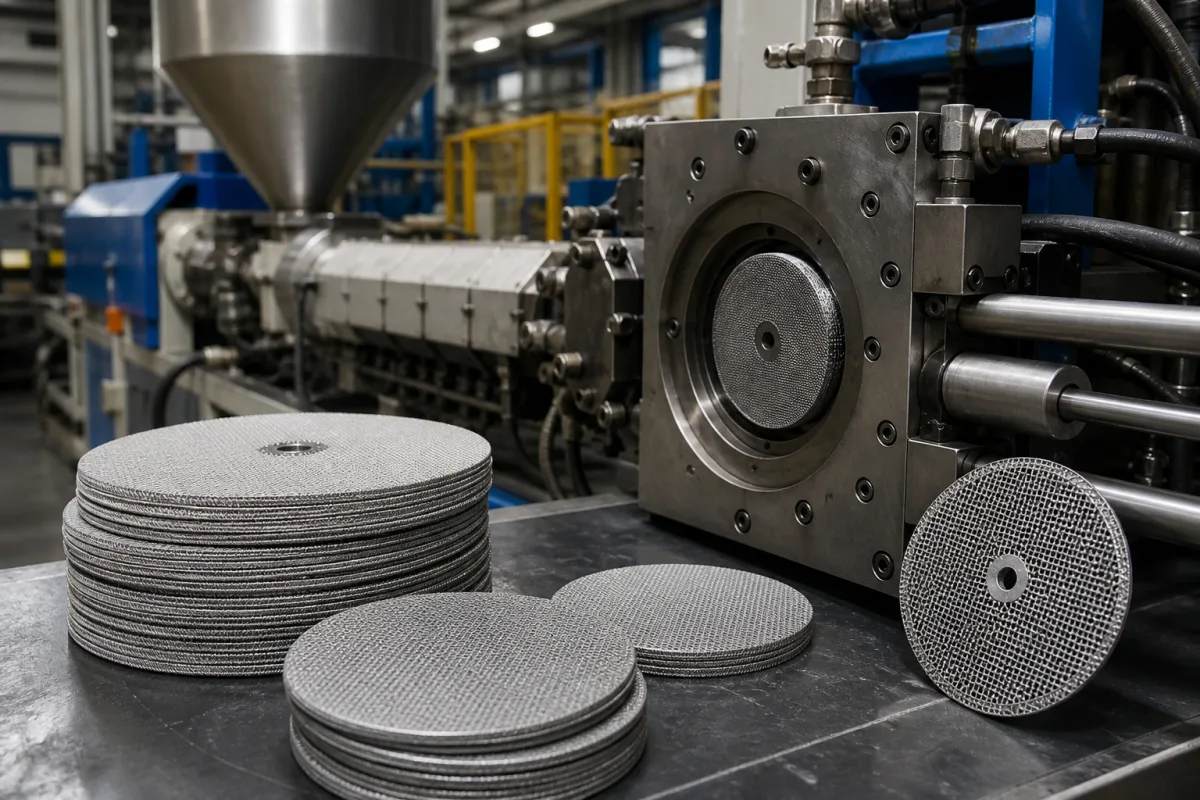
Extruder screen packs · Mesh count and micron rating, layer build-up, screen shapes and changers, back-flush re-use
An extruder screen pack is a stack of woven wire cloth, sometimes with sintered metal media, held in front of the breaker plate or in a screen changer to strain contaminants from the polymer melt before the die. Ask three things first: what filtration fineness and weave the filter layer needs, how the pack is layered and joined for your pressure, and which shape fits your screen changer and how often screens must be changed.
Woven wire screen packs, discs, ovals and filter elements for polymer melt filtration in extrusion. Screen changers as machines, gear pumps, hydraulic and oil filter elements, and screening machines for bulk solids are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Haver & Boecker, which makes woven wire cloth and extruder screens (W.S. Tyler in the USA), explains that screen packs are single- or multi-layer wire filters welded into shapes; layer configuration and micron rating are chosen for the decontamination needed, pressure and the material. "Square mesh is most widely used for its flow capability", with filter weaves such as Dutch twill for finer filtration, and typical square mesh runs from 18 mesh (1,000 µm) to 500 mesh (25 µm). [1]
Single-layer screens suit virgin material with few impurities; multi-layer packs — extruder screens "typically contain 2 to 5 layers" — suit regrind or recycled material or where absolute cleanliness is needed, with a coarse protection layer facing the melt and another coarse layer against the breaker plate so the fine mesh is not pushed into its holes. Stainless steel is preferred where a polymer could corrode mild steel or rust could contaminate the melt, and nickel-alloy mesh is used for fluoropolymers that could corrode stainless steel. [1]
Gneuss offers screen packs in nominal finenesses from 3 µm to 1,400 µm, combining square mesh with Dutch weave for stability and permeability, made from low-carbon stainless steel approved to 600 °C, with fabric tolerances that it says exceed DIN ISO 9044:2001. [3] Editorial calculation: 18 mesh is 18 wires per inch, a pitch of 25.4/18 ≈ 1.41 mm, so a 1,000 µm opening leaves about 0.41 mm for the wire; at 500 mesh the pitch is about 51 µm, so a 25 µm opening needs a wire of about 26 µm.
Give the supplier the polymer and melt temperature, contamination source (virgin, regrind, post-consumer recycled), required fineness, screen changer make and model or breaker-plate drawing, screen shape and dimensions, number and order of layers, mesh counts and weaves for each layer, joining method (spot weld, rim, loose), alloy, and expected change frequency.
02
Match the screen shape to the changer and change rate
Haver & Boecker describes round screens, used one at a time with the process stopped to change them, and kidney-shaped screens used in multiples around a screen-changer wheel that advances automatically when clogging or pressure rise is detected, so production continues. It gives round screens from under 1 in to over 16 in diameter and kidney shapes from about 2.5 × 3 in to over 3.5 × 6.5 in, and notes that clean melt may run days or weeks between changes while "dirty recycled material may need the Extruder Screen replaced several times per hour". [1]
Its guide to screen types lists slide-plate, hydraulic piston and continuous belt changers, and disk, oval, wrap-around, candle and belt screens; oval screens filter nearly twice the material of standard disks and wrap-around screens about four times, while candle packs give the best flow at the highest cost. It notes that clogged screens add back pressure and raise melt temperature through friction, reducing clean output. [2]
For automatic operation, Gneuss's RSFgenius back-flush screen changer keeps the active screen area constant so that pressure, temperature, viscosity and throughput stay constant, back-flushes each screen segment with filtered melt at about 30–80 bar, and reuses screens 100–400 times depending on fineness, with active screen areas of 55–2,800 cm² and filtration down to 1 µm. [4]
03
Compare what suppliers offer
Suppliers linked to this page list extruder screens or melt filter elements; each card links to the page reviewed.
Listings range from woven-mesh discs and filter leaves to sintered metal-fibre melt filter elements; ask each for mesh counts and weaves per layer, alloy, joining method, dimensional tolerance and cleanliness of the delivered screens.
04
Trace the screen pack layers
This is a functional reference built from the sources cited; it is not one maker's design.
Fill the specification fields with values for your line
A screen pack quotation needs values for your polymer and changer. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 13 October 2026
Buyer questions
What mesh counts are used in extruder screens?
Haver & Boecker gives typical square mesh from 18 mesh (1,000 µm) to 500 mesh (25 µm), with Dutch twill for finer filtration. [1]
How many layers does a screen pack have?
W.S. Tyler says extruder screens "typically contain 2 to 5 layers", with coarse layers on the melt side and against the breaker plate protecting the fine layer. [1]
Can extruder screens be reused?
W.S. Tyler says ordinary screens "typically are not able to be cleaned or reused", but Gneuss's back-flush changer reuses screens 100–400 times depending on fineness. [1][4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Haver & Boecker and Gneuss are a wire-cloth maker and a filtration-system maker describing their own products and practice; your fineness and change interval should be confirmed on your line.