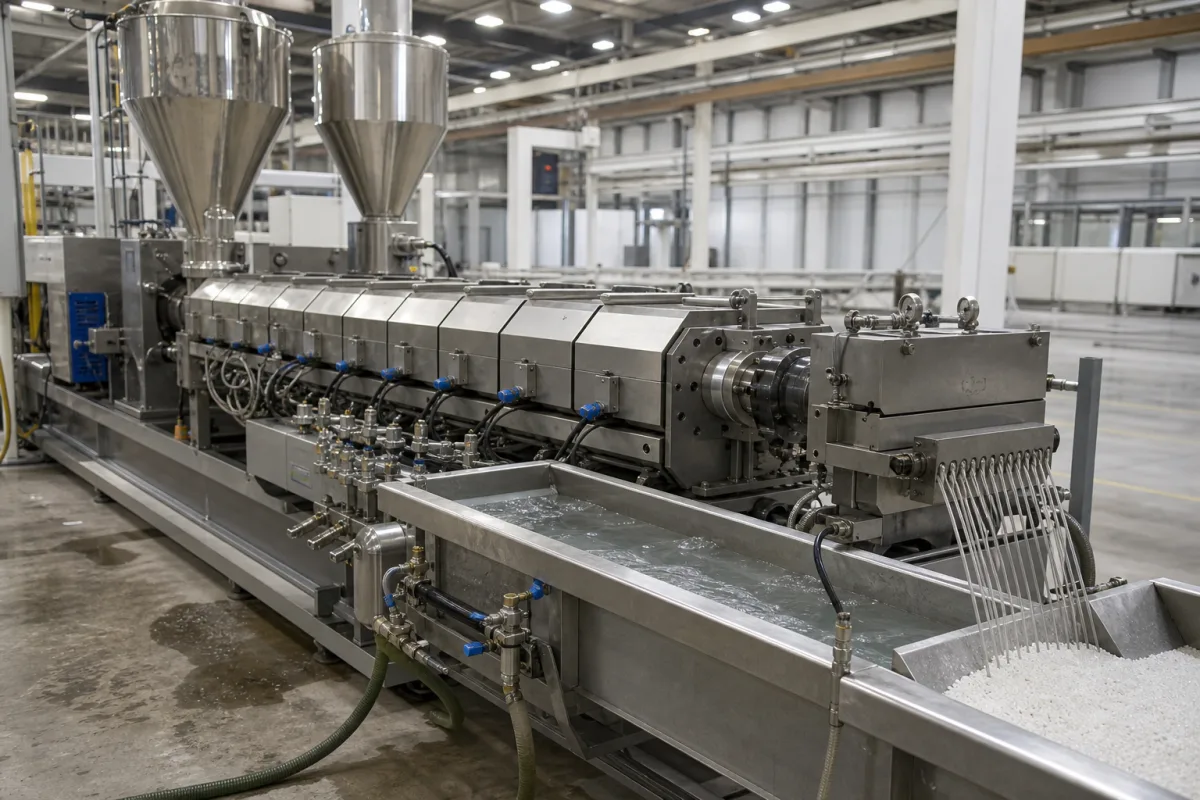
Co-rotating twin-screw compounding · Specific torque and free volume (Do/Di), torque- or volume-limited recipes, specific energy input, scale-up
A co-rotating twin-screw compounding extruder melts polymer and mixes in fillers, fibres, pigments and additives with two intermeshing screws built from conveying, kneading and mixing elements, then discharges the compound through a die to a strand or underwater pelletiser. Ask three things first: whether your recipe is limited by torque or by volume, what specific torque and diameter ratio the machine offers, and what specific energy input and throughput it has demonstrated on a comparable formulation.
Co-rotating intermeshing twin-screw extruders for polymer compounding and masterbatch. Single-screw extruders, counter-rotating extruders for PVC profile, individual screws and elements, and pelletisers are outside this page.
CNFX editorial research · Sources checked October 18, 2026 · 4 sources
Coperion's ZSK brochure defines the key design ratios: the diameter ratio Do/Di (outer to inner screw diameter) determines average shearing, devolatilisation and powder intake; the specific torque Md/a³ (torque over the cube of the centreline distance) determines power density and degree of fill; and screw speed determines shearing and mixing. [1]
Coperion's ZSK Mc18 is described at up to 18 Nm/cm³ with Do/Di 1.55, about 30% more torque than its predecessor, while its ZSK Mv PLUS pairs Do/Di 1.8, a very large free screw volume, with model-dependent specific torque up to 11.3 Nm/cm³ for processes with high volume requirements and specific energy below 0.13 kWh/kg. [1] Leistritz's ZSE MAXX combines up to 15 Nm/cm³ with OD/ID 1.66, which it describes as the optimum between high volume and effective energy input, aimed at volume-restricted processes such as dry blends, pigment preparations, fillers and additive concentrates. [2]
Editorial note: ask the supplier to state whether your recipe is limited by torque or by free volume and feed capacity at the throughput offered, and to show the torque utilisation it expects.
Give the supplier the polymers and their melt flow, fillers or fibres and their percentages and bulk densities, additives and liquid injections, target throughput and pellet form, devolatilisation needs, required dispersion or quality tests, current line data if any, utilities, and whether lab trials on a scale-up machine are required.
02
Check specific energy, throughput and feeding
Coperion's ZSK 45 comparison uses PBT with 30% glass fibres at 85% torque utilisation. It shows the ZSK Mc PLUS at 530 kg/h, 600 min⁻¹ and 0.146 kWh/kg against the ZSK Mc18 at 1,040 kg/h, 900 min⁻¹ and 0.147 kWh/kg, with melt temperature rising from 315 °C to 318 °C. The brochure labels this about 100% more throughput at nearly the same specific energy input (SEI); it is a named formulation comparison, not a rating for every compound. [1]
Coperion reports that its Feed Enhancement Technology doubled throughput of PP with 40% talc on a ZSK 45 Mc18, with torque utilisation rising from 54% to 85% and SEI falling from 0.134 to 0.129 kWh/kg, and that its ZS-EG side devolatilisation keeps the melt in the process section at maximum specific torque, allowing up to 30% more throughput. [1] In a Leistritz residence-time study, a machine with OD/ID 1.66 compounded at 0.253 kWh/kg against 0.276 kWh/kg for OD/ID 1.5 with the same screw geometry. [2]
Editorial calculation: assuming each published SEI and throughput describe the same steady operating point, their product is a power equivalent on that reported SEI basis: 0.147 kWh/kg × 1,040 kg/h = 152.88 kW, approximately 153 kW; 0.146 × 530 = 77.38 kW, approximately 77 kW. These values do not size the installed motor or total line supply: confirm torque, speed, gearbox/drive losses, heater demand and reserve separately. [1]
03
Find the specific-energy window for a filled recipe
The Leibniz-Institut für Polymerforschung Dresden compounded polycarbonate with 3 wt.% multiwalled carbon nanotubes on a co-rotating twin-screw extruder (KraussMaffei Berstorff ZE25, L/D 48, mean barrel temperature 260 °C), varying screw speed from 100 to 1,000 rpm and throughput from 5 to 15 kg/h, and testing hopper versus side feeding at L/D 14. It calculated specific mechanical energy (SME) from recorded torque as SME = 2πNτ/ṁ and related it to dispersion and nanotube length. [4]
The authors found that the higher the SME, the better the dispersion, but that SME beyond about 0.4 kWh/kg shortened the nanotubes without further dispersion gain, and that feeding position also changed the result. [4]
Editorial calculation: if a recipe trial establishes SME of 0.4 kWh/kg and that value can be maintained at a hypothetical steady throughput of 1,000 kg/h, SME × throughput = 400 kW on the same mechanical-energy basis. This is an assumed operating-point calculation, not an IPF production-machine result or an installed-motor specification. Confirm the recipe, screw configuration, torque convention, speed and losses in scale-up trials. [4]
Coperion states that the Do/Di ratio, which sets the free volume of the screws, is kept constant across all sizes of a ZSK series, which it presents as the basis for transferring processes between sizes. [1] Leistritz likewise describes a twin-screw series with a consistent OD/ID. [2]
Editorial note: run trials on a machine of the same series and diameter ratio as the production extruder, record SEI, melt temperature and torque utilisation, and use those values in the acceptance test of the production line.
05
Compounding machines listed by Advance, Kairong and Cowin
Advance lists its HPL65 co-rotating twin-screw compounder for compound and masterbatch production. Kairong lists co-rotating machines separately from its counter-rotating range. Cowin lists co-rotating machines and polymer-compounding applications. Obtain each offered machine’s screw configuration, torque basis and formulation trial results from that supplier.
06
Match residence time and specific energy when moving off the lab line
Thermo Fisher's application note LR70 reports a measured scale-up between two of its twin-screw compounders. On the 11 mm Process 11 at 1 kg/h and 200 rpm, the recipe ran at a specific energy of 559 kJ/kg with a residence time of about 55 s. For the 16 mm Process 16, the rule of Schuler gave a starting feed rate of 3 kg/h, but residence time and specific energy came out significantly lower than on the smaller machine; cutting the feed to 2.5 kg/h brought both back in line, at 566 kJ/kg. [3] The note concludes that the theoretical throughput factor must be adjusted, and that residence time is an important scale-up parameter. [3]
The note explains why: throughput has significant influence on residence time, with a higher throughput decreasing both the mean residence time and the width of its distribution, while the influence of screw speed on residence time is rather low; melt temperature rises with screw speed and feed rate through mechanical energy input in the mixing zones. Heat transfer limits scale-up because barrel volume increases by a power of three but surface area only by a power of two. [3]
Ask the supplier to show the measured residence time distribution and specific energy from the trial machine next to those predicted for the production size, and to state the feed-rate correction applied. Editorial unit conversion: 559 kJ/kg ÷ 3,600 kJ/kWh ≈ 0.155 kWh/kg. This converts the reported Process 11 energy value only; it does not establish comparable conditions with another maker’s test. [3]
07
Drive, mixing elements and process-zone interfaces
3 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Sichuan Advance technology Co.,Ltd
TBC
Lists the HPL65 self-cleaning co-rotating twin-screw compounding extruder for compounds and masterbatch.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 18 October 2026
Buyer questions
What is specific torque on a twin-screw extruder?
Torque divided by the cube of the centreline distance (Md/a³), in Nm/cm³; Coperion says it determines power density and degree of fill. [1]
What does Do/Di mean?
The ratio of outer to inner screw diameter, which sets free volume and affects shearing, devolatilisation and powder intake. [1]
How much energy does compounding take?
The reviewed Coperion ZSK 45 PBT + 30% glass-fibre test reports 0.147 kWh/kg for Mc18. Leistritz’s separate residence-time study reports 0.253–0.276 kWh/kg. These are different studies, not an energy comparison between brands; obtain a value on the intended formulation. [1][2]
Can I scale twin-screw throughput directly from a lab compounder?
Not without checking: in Thermo Fisher's LR70 example the Schuler rule predicted 3 kg/h on the 16 mm machine, but 2.5 kg/h was needed to match the 11 mm machine's residence time and specific energy. [3]
Is more mixing energy always better in twin-screw compounding?
Not for nanotube composites: IPF Dresden found dispersion in polycarbonate with 3 wt.% MWCNT stopped improving above about 0.4 kWh/kg, while nanotube length fell to about 44% of the original at 0.90 kWh/kg. [4]
Sources and what still needs a direct check
Sources checked 2026-10-18. Coperion, Leistritz and Thermo Fisher are twin-screw extruder makers describing their own machines and test results; the Leibniz-Institut für Polymerforschung Dresden study reports measured compounding results on another maker's extruder. Figures for another machine must come from its own trials.