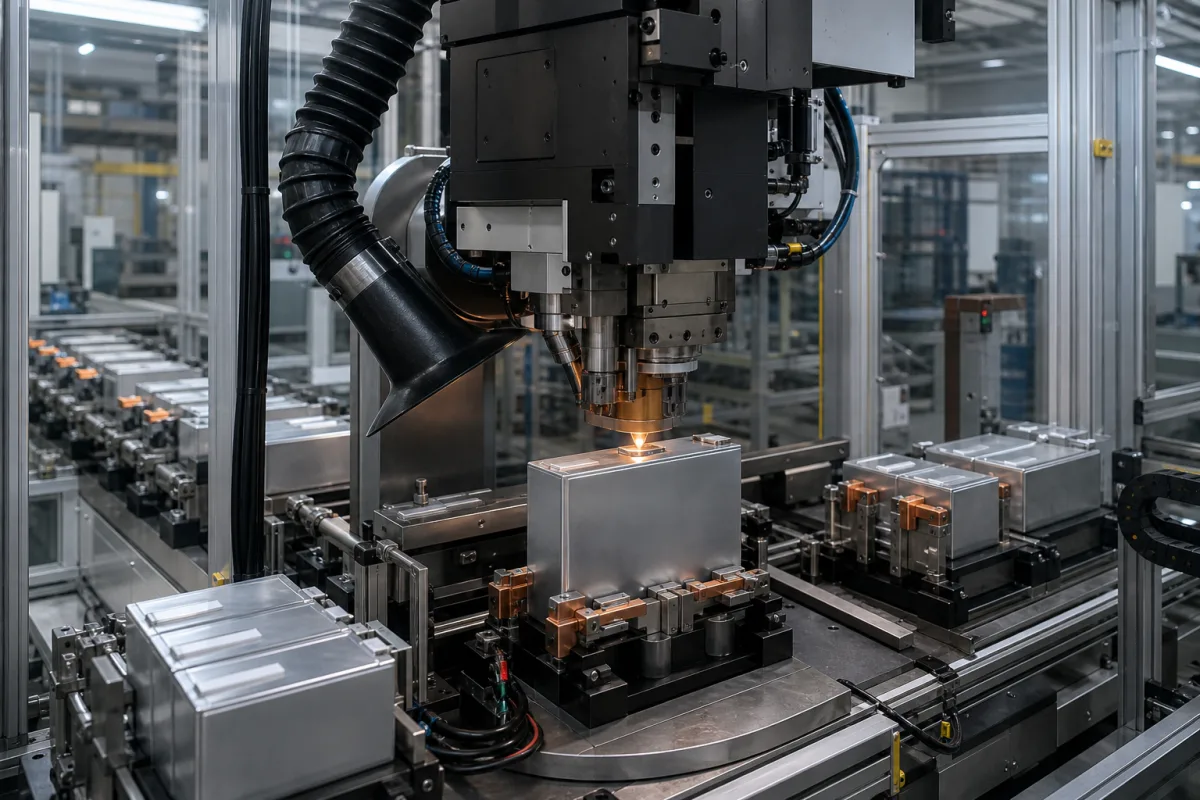
Final sealing station for prismatic lithium-ion cells: plugging and laser-welding the 1–2 mm electrolyte fill hole, then proving the seal by electrolyte-vapour leak test
The last opening in a prismatic lithium-ion cell · a 1–2 mm electrolyte fill hole closed with a plug and a laser weld after filling, with electrolyte on the rim working against the weld, and a leak test that can no longer use helium
A prismatic lithium-ion cell is closed in two welds. The lid is laser-welded to the aluminium can before any electrolyte goes in, while the joint is still clean. Electrolyte is then injected through a small hole in the lid, and that hole is the last opening in the cell. The final sealing station closes it: it places a sealing plug, holds it, and laser-welds it to the lid, working on a surface that has just had electrolyte pushed through it. Once that weld is made the cell is shut for its whole life, so the station is also where the leak test changes from helium blown into an open cell to tracing electrolyte vapour from a closed one.
Stations that close the electrolyte fill (injection) hole of prismatic and other rigid-case lithium-ion cells after filling: sealing plugs, balls or pins, the laser weld that fixes them to the lid, clamping and fume extraction, and the leak test of the sealed cell. Heated sealing jaws and bars, including those used to seal pouch cells, are covered on the Heat-sealing jaw page; filling machines and dosing on the Electrolyte filling systems page; electrolyte degassing on the Vacuum degassing chamber for lithium-ion battery electrolyte page; cylindrical cells closed by grooving and crimping on the Cylindrical lithium-ion cell assembly line page; and general laser welding heads on the Laser welding head page. Can-to-lid welding before filling is covered here only where compared.
CNFX editorial research · Sources checked October 13, 2026 · 3 sources
A 1–2 mm hole in a 0.8 mm aluminium lid, electrolyte on its rim, and a plug that has to be welded round its edge
Sanyo's European patent application EP 1 037 292 sets out the problem the station has to solve and one way around it. Its numbers describe the parts the station handles:
Sanyo notes that with an all-aluminium plug of the hole's own diameter, the weld must follow the plug's circumference precisely and the joint must be airtight, while pushing the plug in can drive electrolyte from the rim into the joint to be welded; it also asks for the laser axis to be perpendicular to the welded surface, with the height of that surface constant. [1]
Coherent, writing about the lid weld on prismatic cells, lists what both seals need: a hermetic seam with no gaps, enough penetration and low porosity to survive vibration and shock, and no spatter, which it calls a particular problem in aluminium because it melts at a low temperature and the melt pool can bubble. [3] The picture above shows a station of this kind: an aluminium prismatic cell clamped in a fixture with copper-coloured contact blocks under a laser head, with a fume-extraction hose beside the beam and further cells waiting on the conveyor.
Item
Value or arrangement in the patent
Fill (injection) hole
Diameter around 1–2 mm, in the lid's sealing plate [1]
Case and lid
Al-Mn alloy; casing about 0.5 mm (typ.) and sealing plate about 0.8 mm (typ.), the plate thicker so the terminal can be fitted without distortion [1]
Order of operations
Lid laser-welded to the can first; electrolyte injected through the hole with a nozzle; hole then closed with a sealing plug laser-welded to the lid [1]
Failure mode
Electrolyte on the edge of the hole causes spattering during welding and imperfect welds; the small plug is hard to handle and insert [1]
Patent's alternative
EP-rubber plug pressed into the hole by an aluminium plate whose edges are laser-welded at the lid rim, away from the wetted hole; external force applied to the plate while welding [1]
Give the lid material and thickness, the fill-hole diameter and any counterbore, the plug type (pin, ball, plate with insert), the time between filling and sealing, and how the rim is cleaned or kept dry before welding.
02
Leak test after sealing: helium for open cells and components at 10⁻⁵ to 10⁻⁷ mbar·l/s, electrolyte tracing once the hole is closed
Marposs divides cell leak testing by whether the cell still has an opening. That boundary is the final sealing station.
Marposs says the end-of-line test of the sealed fill hole can be run before or after formation, or after ageing and end-of-line testing, depending on the process; its AMU-scanning procedure finds the mass to monitor without knowing the solvent recipe, and its helium recovery system recovers up to 95 % of helium or He/N₂ mixtures. [2]
Editorial calculation: 1 mbar·l/s equals 0.1 Pa·m³/s, so Marposs's 10⁻⁵ to 10⁻⁷ mbar·l/s range is 10⁻⁶ to 10⁻⁸ Pa·m³/s. [2]
Stage
Method
What Marposs states
Housing and lid components
Helium tracer gas in a vacuum chamber
Leaks in the range 10⁻⁵ to 10⁻⁷ mbar·l/s must be found, which needs helium as tracer in a vacuum chamber [2]
Assembled cell before filling
Helium blown into the cell through the open fill hole, cell in a vacuum chamber
The lid seal is checked before the cell goes on; leaking cells in formation and ageing are a cost and a safety risk [2]
Cell after fill-hole sealing
Electrolyte-vapour tracing in a vacuum chamber, with a mass spectrometer
No opening is left for tracer gas; solvent vapour from a leak is extracted and measured, calibrated on master leaks for the electrolyte; cells can be tested in batches [2]
State the leak-rate limit for the sealed cell, the electrolyte, whether the test runs before or after formation, and the line rate the test must keep up with.
03
Line rate: the lid seam is 640 mm of weld, the fill-hole seal a few millimetres
Coherent gives a prismatic cell of around 20 mm by 300 mm (typ.), welded round its whole perimeter for the lid seal, and scanner welding faster than 350 mm/s with its adjustable ring-mode lasers. [3] Editorial calculation: that perimeter is 640 mm (2 × (20 + 300)), so at 350 mm/s the lid seam alone takes about 1.8 s of beam time; the fill-hole seal is a ring round a hole of 1–2 mm, so its weld time is a small part of the station cycle, which is then set by plug placement, clamping, cleaning and handling. [3][1]
Give the cell format, the target cycle time per cell, and whether plug placement, welding and inspection must run in one station or be split across stations.
04
Final sealing station data to send
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Cell format: [prismatic size; can and lid material and thickness]
Fill hole: [diameter; counterbore; position on lid]
Sealing part: [pin, ball, plate with elastic insert; material]
Weld: [laser type and power; weld path; shielding]
Rim cleaning: [method]
Leak test: [method; limit in mbar·l/s; before or after formation]
Cycle time and atmosphere: [s per cell; dry room dew point]
Fume extraction and safety: [ ]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How big is the electrolyte fill hole in a prismatic cell?
Sanyo's patent describes an injection hole of around 1–2 mm in the lid's sealing plate. [1]
Why is the fill-hole weld difficult?
Electrolyte on the rim of the hole causes spattering and imperfect welds, and the small plug is hard to handle; Coherent adds that spatter is a particular problem when welding aluminium. [1][3]
How is a sealed cell leak-tested?
Marposs traces electrolyte vapour in a vacuum chamber with a mass spectrometer, because the sealed cell has no opening left for helium. [2]
What leak rates matter for cell components?
Marposs states that component tests must find leaks in the range 10⁻⁵ to 10⁻⁷ mbar·l/s, using helium in a vacuum chamber. [2]
Sources and what still needs a direct check
Sources checked 2026-10-13. Three sources from three publishers: Sanyo's European patent application EP 1 037 292 on sealing the electrolyte injection hole, Marposs's brochure on leak testing in battery cell production, and Coherent's article on laser sealing of prismatic battery cans.