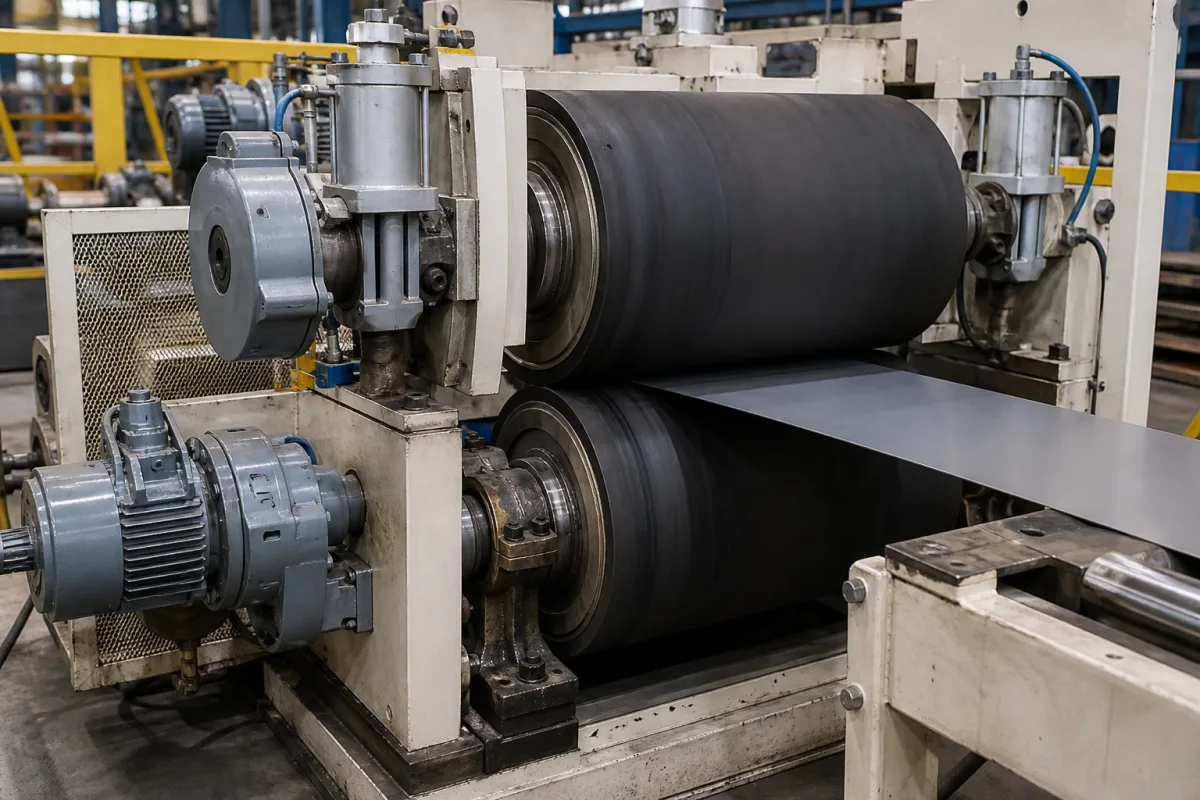
Pinch rolls with polyurethane covers (the driven roll pair that grips strip or web, and how its cover, pressure and alignment are checked)
Elastomer-covered pinch rolls that pull strip and web through a processing line · hard polyurethane covers at 65–95 Shore A for metal strip, measuring roll hardness to ASTM D2240, why hardness alone does not specify a cover, and tracing slip, tracking and marks back to cover, pressure or alignment
A pinch roll pair grips the strip or web between a driven roll and a pressure roll to pull, feed or hold it. The rolls can carry an elastomer cover such as polyurethane, which Hannecard lists for metal strip pinch rolls. The cover's compound and hardness, the nip pressure and the rolls' alignment together decide whether the material is pulled without slipping, drifting or being marked.
Elastomer-covered pinch roll pairs in strip and web processing lines: cover compound and hardness, hardness measurement, nip pressure and alignment. Web tension control as a system is covered on the Web tension control: follow the force and the feedback page; hot strip coiler pinch rolls on the Downcoiler page; run-out tables on the Run-out table for a hot strip mill: driven table rollers and water cooling banks between the finishing mill and the coilers page; caster withdrawal rolls on the Withdrawal and straightening unit of a billet caster: pinch-roll withdrawal force and stepwise straightening steps page; press-line loop control on the Loop control and dancer for coil-fed press lines: holding the strip loop between straightener and press feed page.
CNFX editorial research · Sources checked October 13, 2026 · 4 sources
Cover compound and hardness, and how hardness is measured
Hannecard (ASB Industries) describes its hard polyurethane roller coverings as "Featuring 65-95 Shore A", designed for mechanical forces, high loads and abrasion in humid and oily conditions, and lists "Excellent performances in metal strip processing (including pinch, snubber, hold-down and pressure rollers, tensioning, bridle, steering and traction rolls". [1]
American Roller measures roll hardness to ASTM D2240 and calls Shore A "the most widely used scale for the roller industry". Its notes for a reliable reading: condition the roll at room temperature or record the surface temperature, since some compounds soften when warm and harden when cold; keep the base of a hand-held durometer "parallel with the axis of the roller journals or support shaft"; and note that the reading can be instantaneous or taken up to 15 seconds after loading. [2]
Gallagher, a polyurethane moulder, warns that "Different polyurethane formulations can have the same hardness, yet have a very different set of performance properties", and that converting between hardness scales is not recommended. [3]
Give the cover supplier the material (painted, coated, bare, foil), strip width and speed, nip pressure, oils or solvents on the strip and the roll temperature, and ask for the compound, hardness with its measuring time and temperature, and cover thickness.
02
Tracing slip, tracking and marks before adding pressure
Hotion's troubleshooting guide for pinch rollers notes that "increasing roller pressure may temporarily improve traction in one system while causing marks or deformation in another", and maps each symptom to causes to check first. [4]
Hotion adds that a defect repeating at a fixed interval may indicate damage or contamination on a roller surface, and that tracking problems "should not automatically be treated as a roller-cover issue": rolls out of parallel, worn shafts, bearing play, uneven nip force across the face or upstream guide rolls can all steer the material. [4]
2 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Hotion Group
Manufacturing site to be confirmed for the order
Lists pinch rolls, including upper and bottom pinch rolls for strip lines, on its own website; ask whether covered rolls are supplied.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What hardness are polyurethane pinch roll covers?
Hannecard's hard polyurethane covers run 65–95 Shore A and are listed for metal strip pinch rolls. [1]
How should cover hardness be measured?
To ASTM D2240, with the durometer base parallel to the roll axis and the roll at room temperature, per American Roller. [2]
Is hardness enough to specify a polyurethane cover?
No; Gallagher notes formulations with the same hardness can perform very differently. [3]
Why do repeating marks appear on the strip?
Hotion points to surface damage, embedded debris, excess pressure or unsuitable cover texture; a fixed interval suggests a roll surface defect. [4]
Sources and what still needs a direct check
Sources checked 2026-10-13. Hannecard (ASB Industries) publishes its polyurethane roller covering range; American Roller and Gallagher publish notes on roll and polyurethane hardness; Hotion publishes a pinch roller troubleshooting guide.