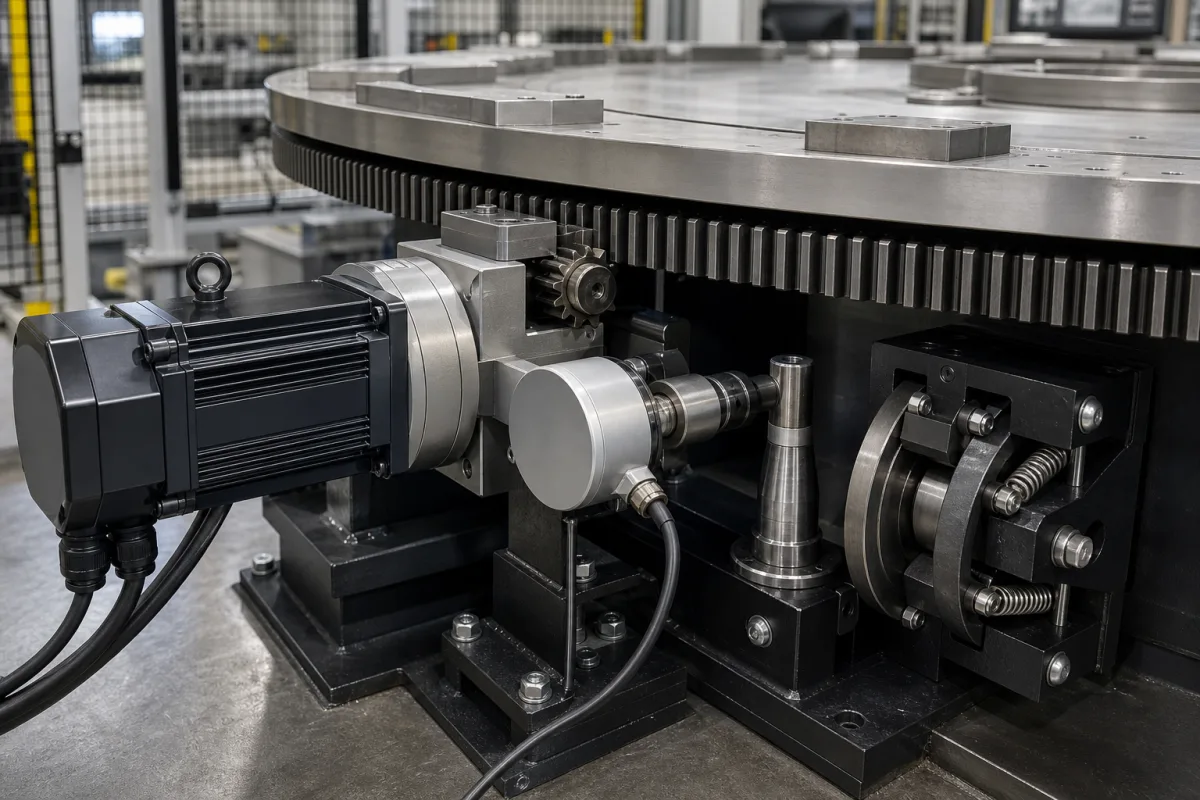
Station positioning system for indexing carousels (servo ring-gear drive, table-mounted angle encoder and station clamp)
Station positioning for indexing carousels and large turntables · ring-gear drive backlash, angle feedback on the table, holding the station with a clamp or brake, arc-seconds turned into millimetres at the station
On a carousel that indexes loads between stations, the motor and gearbox only move the table; whether a part arrives where the tooling expects it depends on three other things. The ring gear and pinion decide how much angle is lost to backlash, an encoder on the table (not only on the motor) decides how well the controller knows where the table really is, and a clamp or brake decides whether the table stays put while the station works on it. Settle the radius of the stations, the position tolerance at that radius, the torque the station process puts on the table, and how fast the table must lock.
Positioning equipment for indexing carousels and large turntables: zero-backlash ring-gear and pinion drives, absolute angle encoders mounted on the table, and rotary clamping elements and brakes that hold each station. CNC rotary tables, indexers and motorized rotary stages as complete units are covered on the Rotary table page; slewing-ring bearings, geared rings, base frames and decks of carousel platforms are covered on the Rotating platform for carousels page. Vision-guided, underwater and satellite positioning systems are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Ring gear without backlash: angle error turned into millimetres at the station
Nexen's Roller Pinion System geared bearing 967267 (RPS10, 160 mm bore, 378 mm outside diameter, external teeth) lists angular backlash of 0 arc-seconds, one-way positional accuracy of 34 arc-seconds and one-way repeatability of 5.6 arc-seconds, with 73 Nm maximum static torque, 48 Nm dynamic torque at maximum life and 200 rpm maximum output speed. [1]
Editorial calculation: one arc-second is π ÷ (180 × 3,600) ≈ 4.85 × 10⁻⁶ rad, so at a station 1,000 mm from the axis it is about 0.0049 mm. The 34 arc-second accuracy above is then about 0.165 mm at 1,000 mm and about 0.031 mm at the gear's own 189 mm outer radius; the 5.6 arc-second repeatability is about 0.027 mm at 1,000 mm. [1]
The same angle grows with radius, so a tolerance stated at the part must be divided by the station radius before it is compared with a drive or encoder rating in arc-seconds. Nexen rates the gear's life as more than 30,000,000 roller contacts per tooth at rated accuracy. [1]
Give the supplier the station radius and the position tolerance at the part, and ask whether accuracy figures are one-way (approaching from one direction) or bidirectional.
02
Angle feedback on the table: ring encoders up to 550 mm and tape scale for larger carousels
A motor encoder sees the motor, not the table; an encoder on the table measures the angle after the gearing. Renishaw's RESOLUTE absolute system offers RESA30 stainless-steel rings from 52 mm to 550 mm diameter, with typical installed accuracy of ±1.9 arc-seconds on the 550 mm ring, rising to ±12.7 arc-seconds on the 52 mm ring. [2]
Renishaw explains that typical installed values result from graduation and installation errors combining and partly cancelling. Resolution is set by the serial interface: 26-bit BiSS C gives 67,108,864 counts per revolution, about 0.019 arc-seconds. [2] Editorial calculation: ±1.9 arc-seconds is about ±0.009 mm at a 1,000 mm station radius, about one-eighteenth of the 34 arc-second gear accuracy above.
Carousels wider than the largest ring can carry RKLA30-S, a self-adhesive stainless-steel tape scale 0.15 × 6 mm, with ±5 µm/m accuracy, lengths up to 21 m and a minimum arc radius of 50 mm. [2] Editorial calculation: a 2 m diameter carousel has a circumference of π × 2 ≈ 6.3 m, inside that 21 m limit.
Ask where the encoder is mounted (motor, gearbox or table), its interface and resolution, and whether the controller closes the position loop on the table encoder.
03
Holding the station: normally-closed clamping elements, holding torque and closing time
Clamping the axis at each station takes the station's process torque off the drive. Zimmer's rotary clamping elements are normally closed: they clamp without pressure and open when pressure is applied. [3][4]
The hydraulic element states holding torque at a stated angular movement: 6,000 Nm while the axis moves no more than 1 arc-second, 8,000 Nm at 5 arc-seconds. Zimmer tests each element at its holding torque with a lightly oiled layer of ISO VG 68 and warns that other lubricants change the friction coefficient. [3]
Editorial calculation: a station tool pushing sideways at 1,000 mm radius with 6 kN applies 6,000 Nm, the DKHS1460's 1 arc-second rating; the pneumatic DKPS1140 at 770 Nm holds 0.77 kN at the same radius. The rated holding torque is 60% of the theoretical figure for the hydraulic element and 80% for the pneumatic one. [3][4]
Zimmer element
Holding torque
Opening / closing time
Pressure to open
Shaft Ø, weight, B10d
DKHS1460-00-A, hydraulic
6,000 Nm at 1 arc-sec; 8,000 Nm at 5 arc-sec; 10,000 Nm theoretical (µ = 0.1) [3]
State the largest torque any station puts on the table, the allowed angular slip while clamped, and the dwell time per station, so clamp opening and closing time can be set against the cycle.
04
Data for quoting a carousel positioning package
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Carousel: [diameter; number of stations; station radius; load and inertia]
Cycle: [index angle; index time; dwell per station]
Accuracy: [position tolerance at the part; repeatability; one-way or bidirectional]
Drive: [ring gear size; pinion; servo motor and gearbox; backlash limit]
Feedback: [motor encoder only or table encoder; ring or tape scale; interface and resolution]
Holding: [station process torque; clamp or brake; hydraulic or pneumatic supply; fail-safe on power loss]
Environment: [temperature; coolant, dust or washdown]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How do arc-seconds translate to millimetres on a carousel?
One arc-second is about 0.0049 mm at a 1,000 mm radius, so a 34 arc-second one-way accuracy, as Nexen lists for its 967267 roller-pinion gear, is about 0.165 mm at that radius. [1]
Can a ring encoder be fitted to a large turntable?
Renishaw's RESA30 rings go up to 550 mm (±1.9 arc-sec typical installed); beyond that its RKLA30-S tape scale runs up to 21 m with a 50 mm minimum arc radius. [2]
What holds a carousel at a station?
A normally-closed rotary clamping element; Zimmer's DKHS1460 holds 6,000 Nm at 1 arc-second and closes in 0.03 s, its pneumatic DKPS1140 holds 770 Nm. [3][4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Nexen, Renishaw and Zimmer publish these accuracy, torque and timing figures for their own products; the Nexen values are taken from a distributor listing of the part's catalogue data.