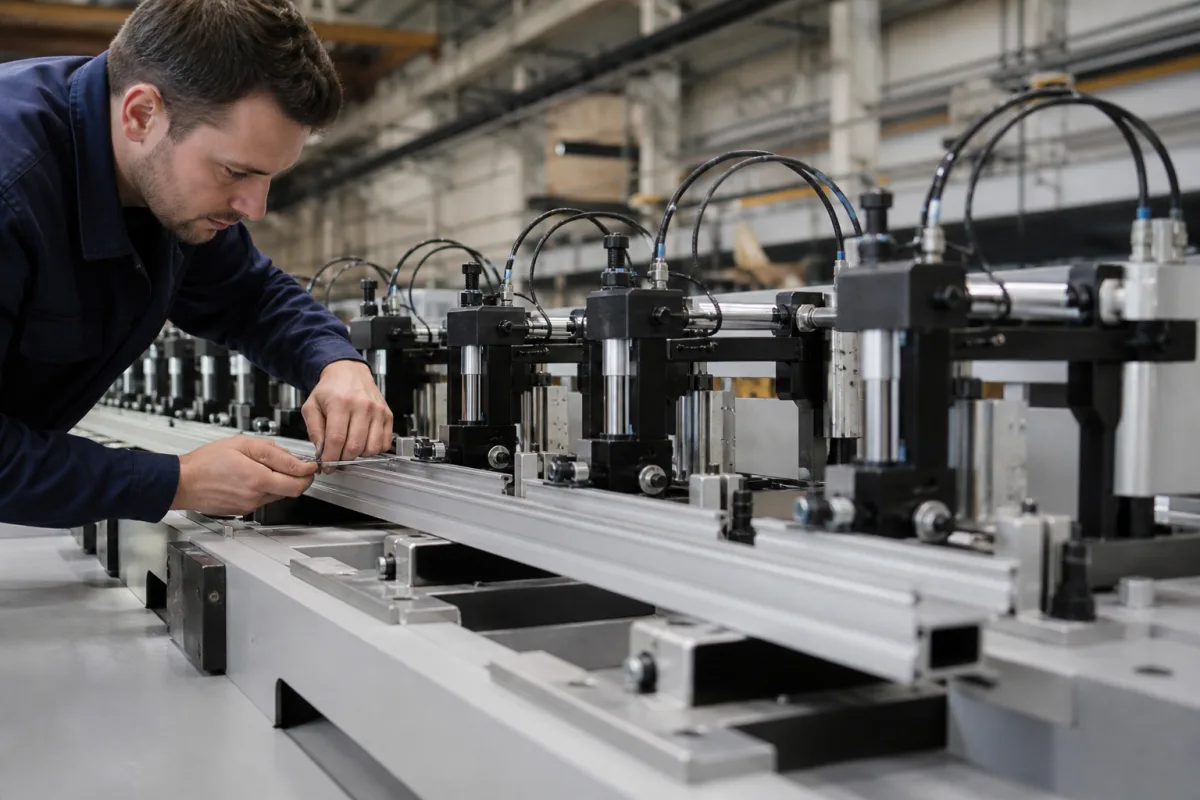
Profile clamping system on a bar-length profile machining centre: the row of pneumatic material clamps and how they are positioned along the X axis
Bar-length profile machining centres · pneumatic material clamps on the bed, how they are moved into position, clamp recognition, reference stops and double clamps
On a profile machining centre the bar lies along the bed and is held by a row of pneumatic clamps, which Elumatec describes as horizontal pneumatic material clamping units. The clamps slide along the bed so they can be set where the tool will not be working. How they get there separates one machine from another: an operator slides them by hand, the X-axis carriage drags each one into place, or each clamp has its own drive and moves while the spindle works. The clamp count, the positioning method and the stops at the bar ends decide how quickly a new part can be set up and how close to a clamp the spindle can work.
The material clamping system of bar-length CNC profile machining centres for aluminium, PVC and light steel profiles: the pneumatic clamps on the bed, their count and spacing, manual, X-axis-dragged and independently motorised clamp positioning, clamp recognition, reference stops and double clamps. The complete machine, its axes, spindle and tool magazine are covered on the Aluminium profile CNC machining centre page; the profile machine with a pneumatically tilted clamp beam on the Aluminium profile CNC milling machine page; machine vises on the Clamping jaws / vise page; hydraulic swing clamps and work supports for fixtures on the Hydraulic clamping system for machining fixtures page; dedicated fixtures for cast housings on the Workpiece fixture page.
CNFX editorial research · Sources checked October 13, 2026 · 9 sources
Clamps dragged by the X axis, independent motorised clamps, and clamps that are CNC axes
Mecal, an Italian profile machine maker, sells the same four-axis Ariel machining centre with two clamp positioning systems. With DPM, a single clamp positioning device, a pneumatic cylinder on the machine couples to one clamp at a time and moves it with the X axis, so the clamps are set sequentially; the machine has 8 clamps as standard. With MMI, the 8 clamps are independently motorised and are positioned automatically and simultaneously, which Mecal says cuts profile loading times. [4][5]
Mecal's five-axis Geos MTS goes further: its 8 standard motorised clamps are CNC axes in their own right, absolute so they need no homing after restart, and can reposition during machining (its MAM cycle) or while the spindle works in the opposite zone in pendulum mode. They also run cut-and-separate cycles on a full-length bar, and Mecal says the clamps are no longer restricted to fixed zones. It quotes a clamping capacity up to 550 mm on this machine and up to 500 mm on the Ariel DPM. [6][4]
Elumatec lists automatic clamp positioning with an absolute measurement system on its SBZ 140, and automatic clamp recognition and positioning on its SBZ 122/71, which it says prevents collisions. [2][1] Yilmaz states that its AIM 4420 and AIM 7420 position the profile clamps automatically from its CAMPROX programming software, and its AIM 3410 has automatic clamp recognition and positioning. [8][7]
Ask which method the machine uses (manual, dragged by the X axis, or motorised), whether the control knows each clamp's position, and whether clamps can move while the spindle is cutting.
02
Four to sixteen clamps along X strokes of 4.3 to 11.4 m, with stops at the bar ends
Elumatec offers its SBZ 140 with 4, 8 or 12 clamps, up to 16, on X traverses of 4,320, 7,720 and 9,820 mm, and fits the SBZ 122/71 with four horizontal pneumatic material clamping units as standard and up to eight, with a material stop on the left and an optional reference stop on the right for overlength machining. [2][1] Yilmaz fits 4 clamps on the AIM 4420 and 8 on the twin-station AIM 7420, adding that the number can be increased, with two pneumatic rests that reset the workpiece in the X direction. [8][9]
Editorial calculation: Mecal's Ariel has an X stroke of 7,420 mm in its shortest version; if its 8 clamps were spread evenly over that length there would be about 1,060 mm between neighbours (7,420 ÷ 7). [4] Mecal offers X strokes of 7,420, 9,420 and 11,420 mm on the same machine. [4] The figure only indicates scale; actual clamp positions are set for each part by the program or the operator.
Double clamps for two profiles per zone and pendulum loading
Mecal's MD double-clamp option gives each clamp two seats with independent clamping adjustment, so that with double clamps up to 8 profiles can be held, two in each of the four work zones, for pendulum machining. [4][5] Elumatec lists a clamping unit for double profile machining as an SBZ 140 option and double clamping on request for the SBZ 122/71. [2][1]
The Yilmaz AIM 7420 runs two stations: after finishing the part in station 1 it moves to station 2 while the operator unloads and reloads station 1. [9] Editorial note: for pendulum work, ask how the clamps in each zone are opened and closed independently and how the guarding keeps the spindle out of the zone being loaded.
04
Travelling roller tensioners and plate clamps on automatic pass-through lines
On fully automatic pass-through lines the bed clamps are replaced by other devices. Elumatec's SBZ 628 XL uses roller tensioners that clamp the profile automatically, can be moved over its whole length and adjusted during the machining cycle to compensate for profile tolerances, and servo-adjusted plate clamps whose narrow design reduces clamp spacing for sawing; the profile is advanced by a pusher X axis. [3]
Elumatec offers quick-change tension rollers and clamping plates for atypical profiles on the same line, and a mode for inserting and clamping non-stationary profiles by hand. [3]
05
Clamping details for a profile machining centre enquiry
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Profiles: [material; largest section W × H; wall thickness; bar length]
Clamps: [number; double clamps; jaw inserts for your profiles]
Positioning: [manual; dragged by X axis; motorised; repositioning during machining]
Recognition: [clamp position known to control; collision check]
Stops: [left and right reference stops; overlength machining]
Zones: [single or pendulum; zone guarding]
Air: [supply pressure; consumption]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How are the clamps moved on a profile machining centre?
By hand, by the X-axis carriage dragging each clamp in turn (Mecal's DPM), or by independent motorised clamps positioned simultaneously (Mecal's MMI). [4][5]
How many clamps does a profile machining centre have?
Elumatec offers 4, 8 or 12 on its SBZ 140, up to 16; Yilmaz fits 4 on the AIM 4420 and 8 on the AIM 7420. [2][8]
What is clamp recognition for?
Elumatec says automatic clamp recognition and positioning on its SBZ 122/71 prevents collisions between tool and clamps. [1]
What air pressure do the clamps need?
Elumatec asks for a supply over 7 bar, Mecal 7 bar and Yilmaz 6 to 8 bar for the machines reviewed. [2][4][7]
Sources and what still needs a direct check
Sources checked 2026-10-13. Product pages of three profile machine makers: Elumatec (SBZ 122/71, SBZ 140, SBZ 628 XL), Mecal (MC 304 Ariel 4A DPM and MMI, MC 302 Geos 5A MTS) and Yilmaz (AIM 3410, AIM 4420, AIM 7420).