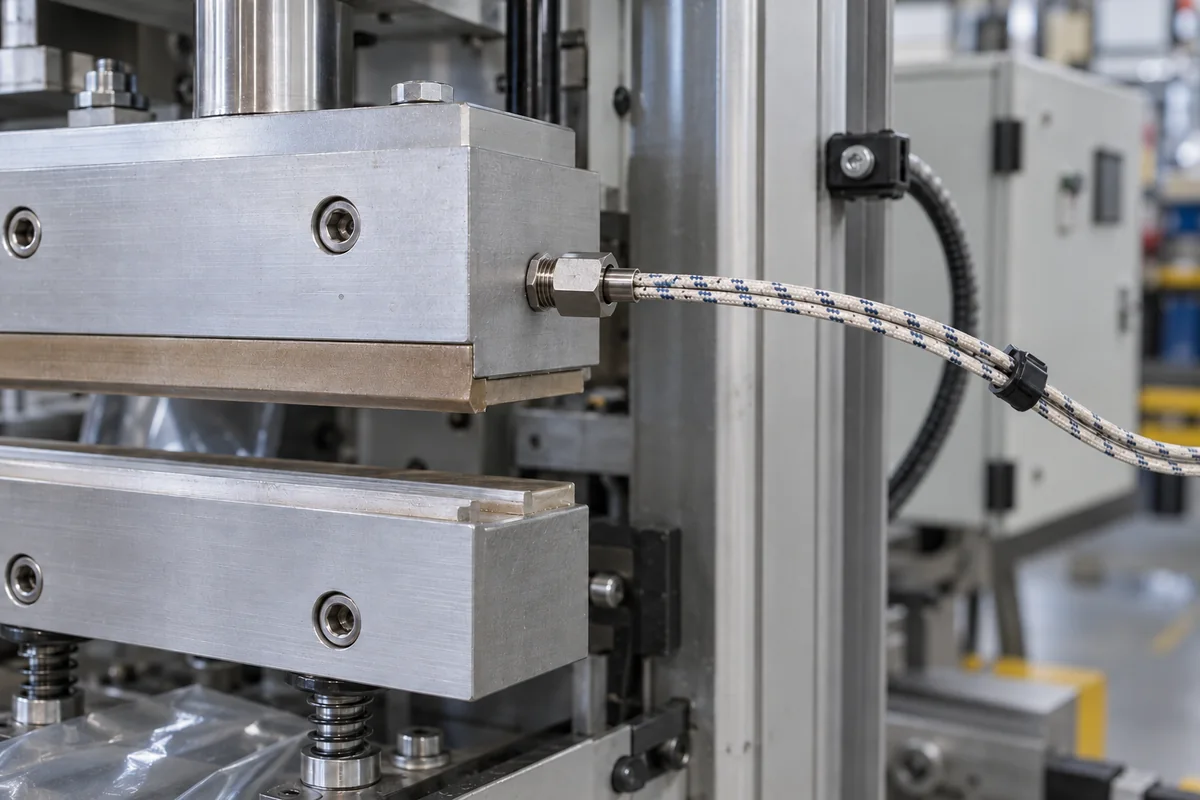
Thermocouple temperature sensor for heat-sealing jaws and sealing heads: where the junction sits, how slowly it settles, and the bayonet probes used
Sealing-jaw temperature sensing · Junction on the band centreline · 10 s to settle against a 400 ms heat-up · Zoned jaws · Bayonet probes in J, K and T · Class 1 tolerance
Every heated sealing jaw, bar or head that is run under temperature control needs a sensor, and on the sealers reviewed here that sensor is a thermocouple: a junction pressed into a bore in the jaw, held against its surface or slipped in as a spring-loaded bayonet probe. The reading drives the controller, so what it represents matters as much as its accuracy class. A buyer has to decide where the junction sits relative to the sealing face and across the jaw width, how the slow response of the probe compares with the heat-up of the jaw, and which probe build, sheath, junction and lead insulation suit the jaw temperature and the machine.
Thermocouple sensors fitted to heat-sealing jaws, sealing bars and sealing heads of packaging machines and laboratory heat sealers: junction position and contact, response compared with jaw heat-up, use as a control or a verification sensor, and bayonet, threaded and surface-mounted probe builds. The jaws themselves are covered on the Heat-sealing jaw page and lidding tools on the Sealing head for cup and tray lidding machines page; mineral-insulated thermocouples inserted through compression fittings on the Mineral-insulated thermocouple sensor page; process temperature probes with heads and thermowells on the Industrial temperature probe page; cartridge heaters with built-in thermocouples on their own page.
CNFX editorial research · Sources checked October 19, 2026 · 5 sources
Junction on the seal-band centreline, and one sensor per heated zone
In a Packaging South Asia feature on heat sealers, Brandon Hoser of PackworldUSA points out that "Traditional thermocouple technology measures at a single point about the size of a thumbnail", so material sealed on or off that point gives different results. The article states that "The most accurate recording is obtained when the thermocouple junction is placed in the centerline of the heat seal band width" (on an 8 mm band, 4 mm in from the edge), and that whether the thermocouple sits on the PTFE tape that contacts the material or directly on the band, the same arrangement must be used every time. [1]
Laboratory heat sealers show how sensors are arranged on jaws. Thwing-Albert's TA12-ASL/1 has upper and lower heated jaws, each independently controlled, with surface-mounted thermocouples, and lists a thermocouple among its replacement wear items. [2] Its 24 in CeraTek sealer divides the upper jaw into eight temperature zones, each 2 7/8 in × 1 in and independently controlled by its own controller, with 1/8 in between zones to minimise heat transfer from adjacent zones. [3]
Editorial calculation: eight zones of 2 7/8 in plus seven 1/8 in gaps make 23 + 0.875 = 23.875 in, close to the 24 in jaw length, so each zone's thermocouple stands for just under 3 in of seal. On a single-zone jaw of the same length, one junction stands for all 24 in. [3]
Ask the jaw or machine supplier where the control thermocouple is fitted (depth below the face, position along and across the jaw), how many zones are controlled, and whether a separate port or position is provided for a verification probe.
02
A thermocouple that settles in seconds on a jaw that heats in milliseconds
The same article reports that PackworldUSA's heat sealers reach sealing temperature from ambient within 400 ms, while "Even the quick response thermocouples take about 10 seconds to start stabilizing towards an accurate temperature reading". It recommends a 15–20 second dwell when validating temperature, and names recording temperature within a sealing time of 2–4 seconds as a mistake. PackworldUSA controls its sealers from the resistance of the whole heat seal band and uses NIST-calibrated thermocouples as a calibration instrument, not for running the machine. [1]
Editorial calculation: a 15 s validation dwell is 37.5 times the 400 ms heat-up, and a 2–4 s production seal is shorter than the 10 s settling time quoted, so a thermocouple reading taken during one production seal can lag the jaw. At a 300 °F setpoint, Thwing-Albert's ±2 % display accuracy is ±6 °F. [1][2]
Figure
Value
Source
Heat-up of the heat seal band, ambient to sealing temperature
Agree with the supplier whether the thermocouple is the control sensor or a verification probe, and record the dwell used when checking jaw temperature.
03
Bayonet probe build: sheath, junction, lead insulation, termination and tolerance class
Wuhan Global Metal Engineering (GME) lists a fixed bayonet-style thermocouple for the plastic and packaging industry with these options. [4]
ICS Schneider Messtechnik, summarising DIN EN 60584, gives the Class 1 tolerance for types K and J as ±1.5 °C or ±0.004 × t, and Class 2 as ±2.5 °C or ±0.0075 × t; the page does not state the temperature range for each term, so ask the supplier for the tolerance at the sealing temperature. Editorial calculation: at t = 200 °C, 0.004 × t = 0.8 °C, smaller than the fixed 1.5 °C term. [5]
Editorial note: the lead insulation ratings above sit close to sealing-jaw temperatures; a PVC lead at 105 °C or a plug at 350 °F (about 177 °C) has to be routed away from the hot jaw, while a fibreglass lead is rated to 510 °C. [4]
3 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Wuhan Global Metal Engineering Co., Ltd.
Manufacturing site to be confirmed for the order
Lists fixed and miniature adjustable bayonet thermocouples, types J, K and T, for plastics and packaging.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 19 October 2026
Buyer questions
Where should the thermocouple sit on a sealing jaw?
A PackworldUSA engineer advises the centreline of the heat seal band width, at the same layer (PTFE tape or band) every time. [1]
Why does the thermocouple read lower than the set temperature during a seal?
The same source says quick-response thermocouples take about 10 s to start stabilising while the band heats within 400 ms; it recommends a 15–20 s dwell for validation. [1]
Which thermocouple types are offered for packaging bayonets?
GME lists types J, K and T, Class I, grounded or ungrounded, in 304 or 316 sheaths of 1/8 to 1/4 in. [4]
Sources and what still needs a direct check
Sources checked 2026-10-19. A Packaging South Asia feature on heat sealers quoting PackworldUSA, Thwing-Albert laboratory heat sealer documents, GME's bayonet thermocouple page and ICS Schneider Messtechnik's summary of DIN EN 60584.