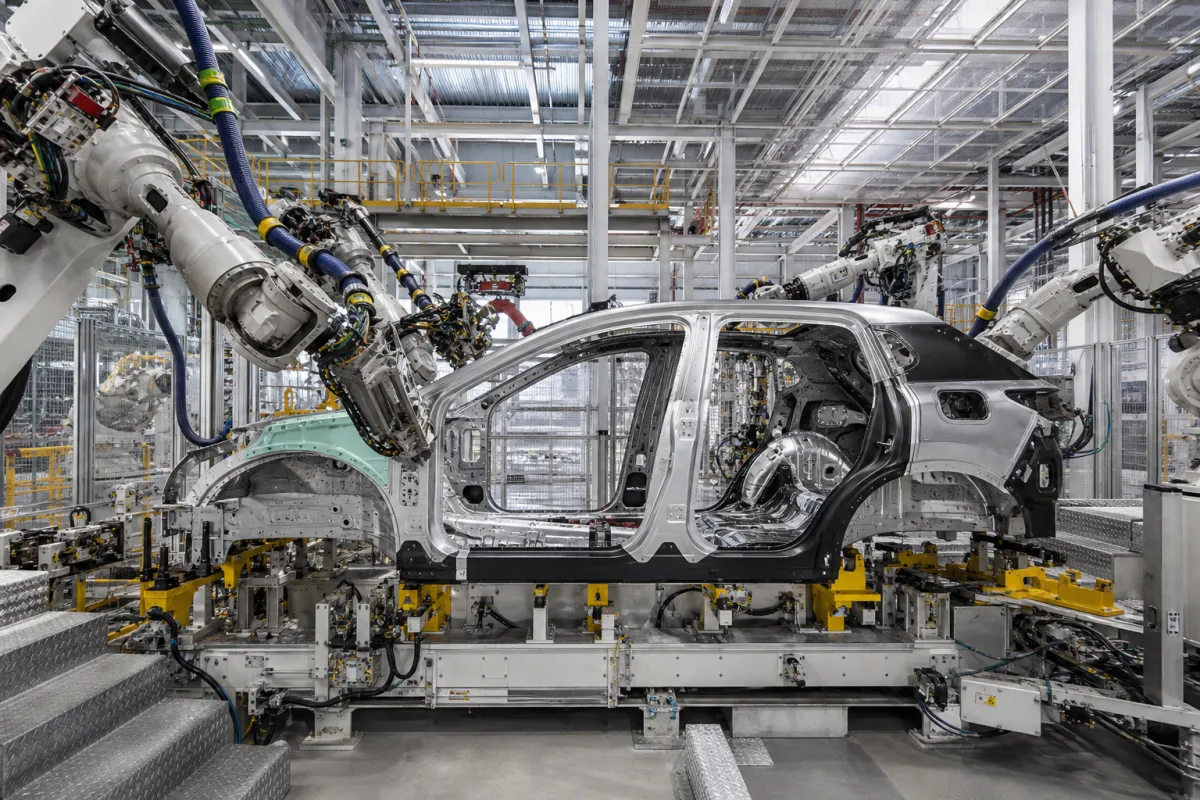
Mixed-material body-in-white joining line: riveting, screwing and bonding aluminium to steel
Body shops that join aluminium castings, extrusions and sheet to hot-formed steel · self-pierce rivets, flow-drill screws, resistance spot rivets, structural adhesive and hemming in one framing sequence
Once a car body mixes aluminium castings, extrusions and sheet with hot-formed steel, the body shop has to join material pairs that steel-to-steel spot welding was never set up for. The line then carries a set of cold and hybrid joining tools: self-pierce riveting guns fed from a rivet tape or loose feed, flow-drill screwdrivers, structural adhesive dispensed before the parts are clamped, and hemming rollers where an aluminium frame wraps a steel flange. Each tool brings its own consumable, feed system, die or electrode, and its own corrosion question at the joint.
Automated body-shop stations and lines that join dissimilar materials in a vehicle body structure: aluminium to steel, and aluminium to magnesium or carbon-fibre composite, by self-pierce riveting, flow-drill screwing, resistance spot riveting, structural bonding and roller hemming, with their rivet and screw feed systems and the corrosion protection at the joint. Robotic resistance spot welding of all-aluminium bodies with servo guns and electrode care is covered on the Robotic welding station for aluminium car bodies page; line PLCs, HMIs and fieldbus for welding lines on the Central control system for robotic body-in-white welding lines page; the robots themselves, sized by payload and repeatability, on the Assembly robot page; chassis marriage lines on the Chassis rigging and marriage line page; body panel stamping on the Automotive body panel stamping press page.
CNFX editorial research · Sources checked October 12, 2026 · 5 sources
Fourteen joining processes in one body shop: what the Audi A8 body required
The aluminium-intensive Audi A8 introduced for model year 2018 is a published example of how many separate joining tools a mixed-material body brings into the line. SAE's report on Audi's disclosure states that aluminium cast nodes, extruded profiles and sheets make up 58% of the body, alongside hot-formed high-strength steel, magnesium and CFRP, and that body assembly uses 14 different joining processes, including roller hemming, grip punch riveting and remote laser welding of aluminium. [1]
Where the aluminium side wall frame meets hot-formed steel at the B-pillar, roof line and sills, Audi pairs roller hemming with grip punch riveting that fixes the side wall frame in position, backed by structural bonding. [1] Light Metal Age, reporting the same release, quotes Audi's figure of up to 36 mm gained at the door cutouts compared with the previous A8, and describes the hemming as a mechanical, cold process. [2]
For the aluminium-to-aluminium seams, Audi's remote laser welding positions the beam relative to the weld edge to reduce hot-cracking risk and uses heat input to control penetration depth; Audi claims about one fourth lower CO2 emissions for that step and a 95% saving on recurring costs in series production, because the process control used with conventional laser welding is no longer needed. These are the carmaker's figures as reported, not independent measurements. [2]
Light Metal Age also reports Audi's figures for its new cast alloys: tensile strength over 230 MPa and yield strength over 180 MPa for heat-treated ultra-high-strength castings, and higher values for the profile alloys. [2] Those are the cast nodes that rivets and screws have to penetrate or anchor into, so the casting alloy and temper belong in the joining specification.
List every material pairing in the body by location (sheet, extrusion, casting, hot-formed steel, CFRP) and ask the line builder which joining process, consumable and access direction each pairing gets.
02
Self-pierce rivets: shank diameter, length steps and hardness levels against the stack
A self-pierce rivet is chosen for a particular stack of sheets, so a mixed-material line holds a rivet type for each family of stacks, fed to the gun that sets it. Atlas Copco's Henrob rivet catalogue codes every rivet by geometry, shank diameter, effective length, material, hardness level, head style, coating and packaging. [3]
The catalogue offers each family on sprocket tape spools or loose in bottles or bags, compatible with Henrob tape-feed and loose-feed systems, and lists zinc-tin and ALMAC base coats with optional top coats or lubricant. [3] It also notes that not every hardness, head and coating is available in every length and diameter, so the rivet matrix for a line is agreed with the rivet maker. [3]
Atlas Copco describes the process as driving a semi- or fully tubular rivet through the layers into a die that flares the rivet tail into the bottom sheet without piercing it, with no pre-drilled hole and no heat. [4] Because the die side must be reached, every self-pierce rivet location needs access from both sides of the flange.
Henrob rivet family
Stated application
Shank diameter
Lengths
Hardness levels
A
Automotive; thinner aluminium alloys and mild steel sheets [3]
For each rivet location give the stack order (punch side to die side), each layer's alloy, temper or steel grade and thickness, adhesive in the joint or not, and whether the gun is fed by tape or by blow feed.
03
Resistance spot rivets: feeding a steel or aluminium rivet through a standard spot-welding gun
A US Department of Energy-funded programme run by Arconic (now Howmet Fastening Systems) with Honda R&D Americas and The Ohio State University tested a third route: a rivet placed between the electrode and the aluminium sheet and welded to the steel underneath with conventional resistance welding equipment. Its final report states that RSR was tried because, in the team's assessment, self-pierce rivets, flow-drill screws and friction bit joining all have limitations with higher-strength materials and all need new joining equipment. [5]
The robotic pilot cell built by Howmet Fastening Systems and CenterLine used an off-the-shelf weld gun, transformer, robot, weld controls and electrode dressers, and added four new parts: a collet that holds the rivet against the electrode and retracts during the weld and for tip dressing, a J-Track magazine that swings into the gun loop between welds, a reload station where the robot docks the gun for a magazine refill, and a bowl feeder with checker and controller recording force and position signatures. [5] The report says rivets were fed and welded from above, below and the side on a double hat section, and that the feed system passed its feed-reliability evaluation without faulting. [5]
Production-condition tests in the report covered part angles up to 7 degrees and part gaps up to 2 mm; lap-shear tensile strength fell by no more than 25% against the baseline. Electrode life runs on two- and three-thickness stacks met the lap-shear and cross-tension targets for over 200 consecutive welds, and joining was shown on wrought and cast aluminium through 3.2 mm. [5]
On Honda's demonstrator, which joined two advanced high-strength steel pressings to an aluminium casting, a single RSR joint had to reach 10 kN in lap shear. The report gives a single-joint average above 10 kN, above 15 kN with structural adhesive added, and averages above 25 kN for two joints and above 30 kN for three in the offset-pull case. [5]
If the line already runs resistance spot welding for steel, ask whether spot rivets can share the guns and dressers, how the rivet magazine is refilled within cycle time, and which stacks have been qualified with weld-through adhesive.
04
Galvanic corrosion at riveted and screwed aluminium-steel joints: what the salt-spray comparison showed
The same programme exposed riveted and screwed aluminium-steel coupons in three cabinet tests: ASTM B117 constant 5% NaCl spray at 35 °C; ASTM G85 Annex 2, acidified to pH 3 with acetic acid and cycled through spray, dry purge and humidity at 45 °C; and the Japanese automotive cyclic test CCT-1 with salt fog at 35 °C, drying at 60 °C and humidity at 50 °C. [5]
The values are maximum sustained loads in the report; its authors say the two joint types are probably within the same scatter band and that comparison with unexposed samples is still needed. [5] Editorial calculation: the self-pierce riveted joint went from 9.19 kN to 8.84 kN between 2.7 and 32.4 days, a 3.8% fall. [5]
Honda's cyclic corrosion tests in the same report found that spot-riveted samples with no head or edge protection showed clear galvanic corrosion, samples with edge protection only at the material interface corroded around the rivet head, and samples with both head and edge protection showed no immediate signs of galvanic corrosion and kept strength similar to the controls. [5] Ohio State also found that test orientation (fastener head towards or away from the spray) can change how aggressive the galvanic pitting is, and the report warns that this needs care when technologies are compared. [5]
Joint (aluminium – steel)
After 2.7 days B117
After 10.7 days B117
After 32.4 days B117
Failure mode
Self-pierce rivet, AA6013 to 590 steel, no adhesive
Ask the supplier which sealer or adhesive isolates each aluminium-steel joint, whether the fastener head is coated or sealed, and which cyclic corrosion test and exposure time the joint was qualified to.
05
Joint list and station data for a mixed-material body-shop quote
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Body: [model; annual volume; jobs per hour]
Material pairings: [location; layers in stack order; alloy/temper or steel grade; thickness]
Joining per pairing: [self-pierce rivet; flow-drill screw; resistance spot rivet; adhesive; hemming; access from one or both sides]
Consumables: [rivet and screw types; tape or blow feed; adhesive type and bead size]
Corrosion: [sealing; isolation; cyclic test and exposure required]
Existing equipment: [spot-weld guns; robots; dressers; controls to reuse]
Acceptance: [lap-shear and cross-tension targets; cross-section checks]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How many joining processes can a mixed-material car body need?
SAE reports that the aluminium-intensive Audi A8 introduced for model year 2018 uses 14 different joining processes in body assembly, including roller hemming, grip punch riveting and remote laser welding. [1]
Which self-pierce rivet sizes does the Henrob catalogue list?
Shank diameters of 3, 5 and 5.5 mm, lengths from 3.25 mm up to 14 mm depending on the family, and hardness levels 1 to 6; level 2 is 410 HV and level 6 is 555 HV. [3]
Can a spot-welding robot set rivets in aluminium-to-steel joints?
In an Arconic-Honda programme funded by the US DOE, resistance spot rivets were fed by a collet and magazine into a conventional robotic spot-welding gun and the feed system passed a feed-reliability evaluation without faulting. [5]
Does an aluminium-steel rivet joint need corrosion protection?
In Honda's cyclic tests, spot-riveted joints without head or edge protection showed clear galvanic corrosion, while joints with both head and edge protection showed no immediate signs of it. [5]
Sources and what still needs a direct check
Sources checked 2026-10-12. The rivet sizes come from a rivet maker's catalogue; the spot-rivet cell, test limits and corrosion data from a final report to the US Department of Energy by the developer, a carmaker and a university; the Audi A8 figures are the carmaker's statements as reported by SAE and Light Metal Age.