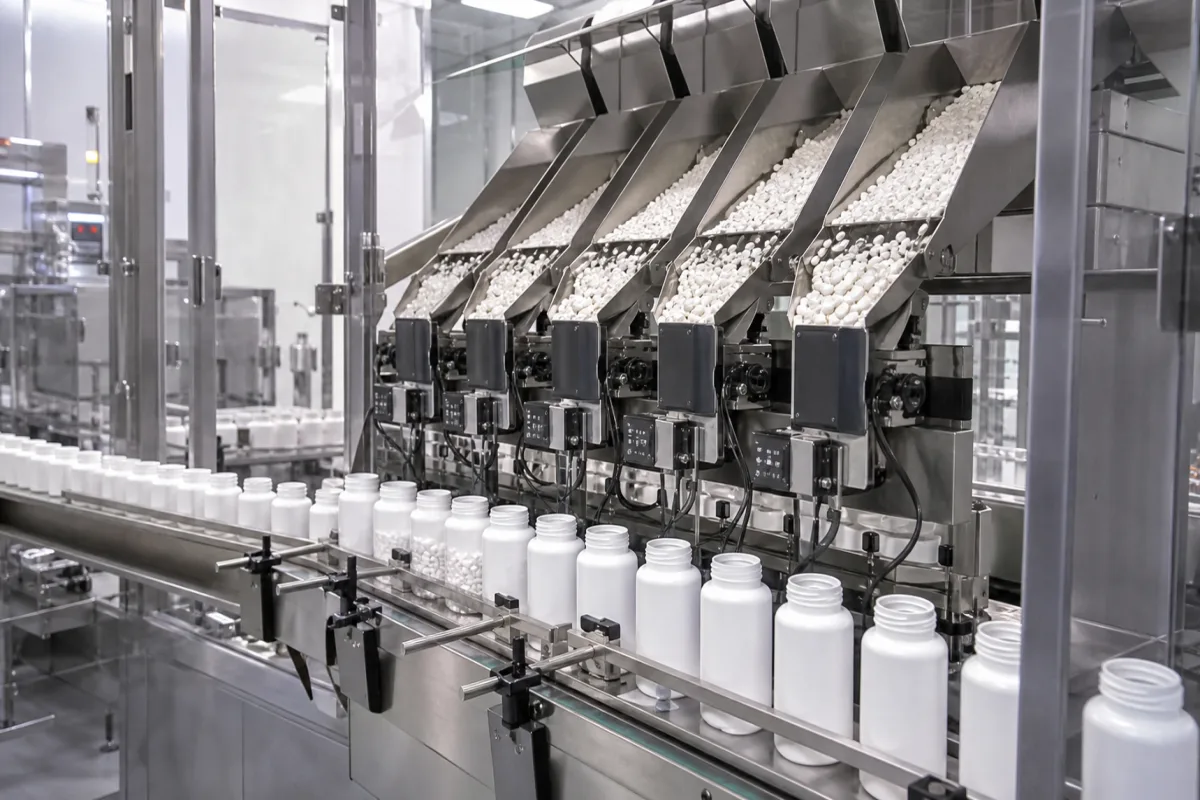
Pharmaceutical tablet counting and bottling machine
Electronic tablet and capsule counters that fill bottles · Vibratory multi-channel feed trays, light-beam or optical array counting, singulation and bunching errors, count accuracy targets, bottle indexing, and GMP calibration of automatic equipment
A tablet counting and bottling machine feeds tablets or capsules from a hopper onto vibrating channels that line them up, counts each one as it passes an optical sensor, and drops the counted fill into a bottle indexed beneath. Its accuracy depends on keeping tablets apart as they pass the sensor. Ask three things first: which products, sizes and counts per bottle it must handle, how it separates tablets and detects miscounts, and how its count accuracy is proven and kept under calibration.
Electronic (optical) tablet and capsule counters with vibratory feeders and bottle filling stations, from benchtop to multi-lane inline machines. Slat or disc counters, bottle unscramblers, cappers, cotton and desiccant inserters, labellers and pharmacy dispensing robots are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
US patent 3,958,687 (High-speed multi-channel feeder for tablets, 1976) explains that counters pass each tablet across a light beam aimed at a sensor, and each interruption triggers a count. At higher flow rates tablets falling freely through a counting channel (5 to 10 units per second) come together without separation, so a unique pulse may not be produced for each one; the patent puts the resulting probability of erroneous signatures at about 0.002, against new pharmaceutical accountability standards requiring a counting error below 1 part in 10⁴. Its feeder is an inclined vibrating tray with a spreading region and a multi-channel sorting region, each channel ending in an exit port above its own sensing channel, with wedge-shaped directing surfaces to put tablets into single file. [1]
US patent 10,524,985 B2 (Discrete object singulation, 2020) describes optical counters with a light source facing a sensor array and an image processor, and explains that accurate counts need singulated flow: two touching tablets risk a miscount and three together are almost impossible to resolve. Bunching can be vertical (stacked) or horizontal (side by side); its vibratory feeder uses a wiper above the pathway to push stacked tablets back to the reservoir and a chamfered edge to guide side-by-side tablets away from the exit. [2]
Editorial calculation: an error probability of 0.002 means about 20 miscounted events per 10,000 tablets, against no more than 1 per 10,000 at the 1-in-10⁴ target the patent cites, a twentyfold gap. [1]
Give the supplier the products (tablet and capsule shapes, sizes, coatings, friability), counts per bottle and bottle sizes, required bottles per minute, number of lanes, feed and singulation design, counting sensor type, reject and recount handling for miscounts, dust extraction, changeover and cleaning time between products, line integration (unscrambler, capper), data and audit trail requirements, and calibration and validation support.
02
Prove accuracy and keep it calibrated
US current good manufacturing practice rules for finished drugs (21 CFR 211.68) allow automatic, mechanical or electronic equipment, including computers, to be used in manufacturing, processing, packing and holding drug products, provided it is “routinely calibrated, inspected, or checked according to a written program designed to assure proper performance”, with written records kept. Changes to computerised master production and control records must be made only by authorised personnel, and inputs and outputs must be checked for accuracy. [3]
Editorial note: ask the supplier for the count accuracy it guarantees for each product and speed, the challenge test it proposes to prove it (for example counted reference lots), how the sensors are checked between runs, and what documentation it provides for your calibration and validation programme.
03
Choose line speed and in-line inspection
Countec, a maker of tablet counting and bottle packaging machines, lists complete automatic tablet and capsule bottle filling and packaging lines at 15, 30, 60, 120, 200 and 300 bottles per minute, and states that actual speeds vary with bottle neck diameter and the shape and size of the product. Its line includes tablet counters (it names the DMC60S and DMC120 models and its first counter, the DW-6), bottle unscramblers and cleaners, bottle printing and servo-driven rotary cappers with torque set from the touch screen. Its COVISS vision system inspects tablets and capsules on the counter's vibratory trays for broken or chipped tablets, black spots, wrong colour, size or shape, and removes the bottle containing a defective product from the line. [4]
Set this against the optical counting principle, singulation and GMP calibration requirements above. [1][2][3]
Editorial calculation: at 120 bottles per minute a line fills 7,200 bottles an hour; with 100 tablets per bottle that is 12,000 tablets counted per minute across the counter's channels.
Countec line point
Published value
Line speeds offered
15, 30, 60, 120, 200 and 300 bottles/min
What changes actual speed
Bottle neck diameter; product shape and size
Counter models named
DW-6 (first), DMC60S, DMC120
In-line inspection
COVISS vision on vibratory trays; rejects bottle with defective product
Defects detected
Broken/chipped tablets, black spots, wrong colour, size or shape
Give the supplier your bottle sizes, neck diameter, tablet or capsule dimensions and count per bottle, and ask for the guaranteed bottles per minute for each format and the defect types the vision system rejects.
04
Hopper, vibratory channel tray, wipers and guides, optical sensors, bottle indexing and controls
The tray, wipers and guides exist to stop bunching: US 3,958,687 puts the miscount probability near 0.002 when tablets fall freely at high rates, and US 10,524,985 counts on singulated flow for an accurate optical count. [1][2]
Counting speed, accuracy target, bottle and tablet range and line speed for a counter quotation
Speed and accuracy have to be quoted as a pair: the 1-in-10⁴ accuracy target the 1976 patent cites only means something at the counting rate and product it is proven on. [1]
Field
What it means and published values
Ask the supplier for
Maximum Counting Speed (tablets/minute)
Per lane free-fall 5–10 per s caused bunching in one patent. [1]
Find pharmaceutical tablet counting and bottling machine manufacturers
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Ruian Yongli Pharmaceutical Machinery Co., Ltd.
Manufacturing site to be confirmed for the order
Lists electronic tablet counters, including the YL-16S, YL-12S and YL-8 models.
Product scope checked 2026-10-12
Product page on own website · profile compiled by CNFX from public sources
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Why do tablet counters miscount?
When tablets bunch together they may pass the sensor as one; US 3,958,687 put the error near 0.002 at high free-fall rates. [1]
How do counters keep tablets apart?
Inclined vibrating multi-channel trays, wipers that return stacked tablets and guides for side-by-side ones (US 3,958,687; US 10,524,985). [1][2]
Must electronic counters be calibrated under GMP?
Yes; 21 CFR 211.68 requires a written programme of routine calibration, inspection or checks with records. [3]
How fast are tablet counting and bottling lines?
Countec offers complete lines at 15, 30, 60, 120, 200 and 300 bottles per minute, noting that actual speed depends on bottle neck diameter and product shape and size. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. The two US patents (1976, 2020) describe counting and feeding in their own terms; 21 CFR 211.68 is part of US drug GMP regulations; Countec, a counter maker, describes its own bottling lines.