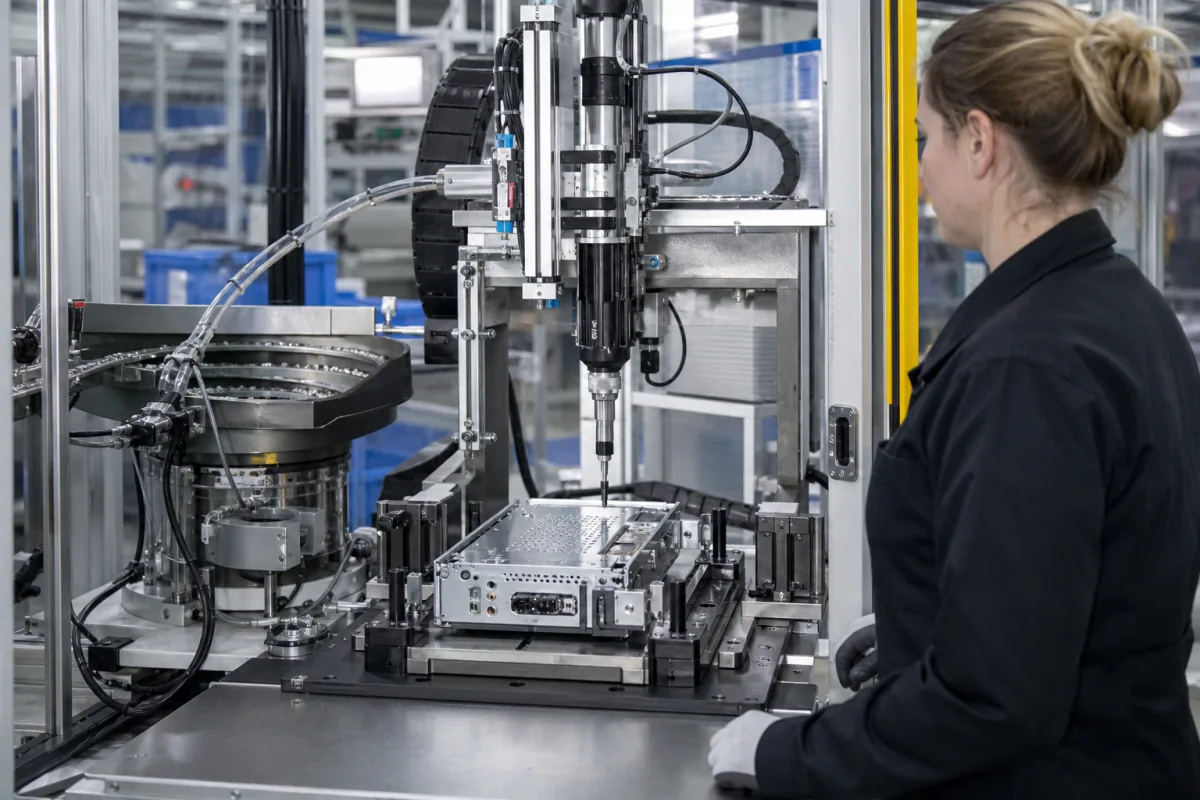
Fastener installation module: the blow-fed screwdriving head, feed tube and torque-controlled spindle of an automatic screwing station
The blow-fed screwdriving head of an automatic assembly station · bit-stroke or 48 mm head-stroke, a 10 Nm feeding head, 0.3–20 Nm spindles, and the screw geometry that decides whether hose feeding works
In an automatic screwing station the screw is not picked up by hand or by a gripper; it is blown through a hose from a feeder into a head that holds it in jaws while a motor-driven bit drives it home. This page is about that module: the two ways the head reaches the hole, how the spindle is matched to the joint, whether a given screw can be blown through a hose at all, and what to do when the hole is deep.
Blow-fed (hose-fed) automatic screwdriving modules for fixed stations, Cartesian slides and robots: the feeding head with its jaws and stroke, the feed tube and feeder that supply it, the torque-controlled driving tool, and the screw properties that decide feedability. Selection between vibratory bowl, centrifugal and vision-guided flexible feeders for parts of any kind is covered on the Feeding systems page; robots that carry screwdriving tools, among other tools, on the Assembly robot page; multi-station pallet lines that contain screwing stations on the Automated assembly line on workpiece pallets page; dedicated O-ring fitting machines on the Automatic O-ring assembly page. Hand-held torque wrenches and the screws themselves are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Bit-stroke for a robot, 48 mm head-stroke for a fixed station: Atlas Copco's fixtured screw feeding module
Atlas Copco's Fixtured Screw Feeding System consists of the tightening module, a driving tool, a Power Focus 6000 controller, a feeder, an external valve control unit, cables and hoses. [1] Its feeding head is built in two versions that differ in which part moves toward the screw location.
The screw travels by compressed air through the feeding tube to a swivel arm, which holds and loads the next screw while the previous one is being tightened and is swung out of the way by the bit; spring-closed aligning jaws hold the screw for the bit to engage. A ring sensor detects the screw at the end of the tube, an inductive sensor checks that the bit is fully retracted, and a stroke position sensor follows the bit stroke. [1] The feeding head can be set at −90°, −45°, 0°, 45° or 90°. [1]
Editorial note: for a robot-mounted head, the 4.3 kg of the bit-stroke version plus cable and hose loads count against the robot's payload at its wrist; the 1.7 kg saved against the head-stroke version is the difference between the two published weights.
Bit-stroke version
Head-stroke version
What moves
Only the bit, forward through the jaws; the robot or Cartesian slide supplies the Z motion to the part [1]
The feeding head, 48 mm toward the tightening location, while the motor stays stationary [1]
Tell the supplier whether the head goes on a robot, a slide or a fixed column, the approach direction and clearance around each screw location, the number of screws per part and the cycle time.
02
Spindle torque from 0.3–1.2 Nm to 4–20 Nm under a feeding head rated 10 Nm
The same module takes driving tools of different torque ranges, and Atlas Copco lists their speeds alongside. [1]
The QST34-20 tools reach 20 Nm, but the feeding head through which they drive is rated at a maximum of 10 Nm in both versions. [1] Editorial note: when a joint needs more than 10 Nm, ask the supplier which feeding head is rated for it, not only which spindle.
DEPRAG gives the span of its screwdrivers for manual and stationary use as 8 Nmm to 500 Nm, with sequence controllers (AST5-S, AST12, AST40) that supervise the screwdriving process and collect its data. [4] Editorial calculation: 8 Nmm is 0.008 Nm, so the DEPRAG span covers more than four orders of magnitude; the spindle for a given module is chosen from the joint's target torque and speed, not from the span of the range.
Give the target torque and tolerance, angle window if used, screw size, thread-forming or machine thread, and the data the controller must record for each screw.
03
Will the screw blow-feed? Length-to-head ratio, feeder type and screw purity
In an interview published by reinraum.de, DEPRAG describes hose feeding as offering the highest process reliability and the shortest cycle times, and explains how it checks whether a screw can be fed that way. [3]
DEPRAG's first check is an approximation formula on the ratio of screw length to head diameter, from which the possible tilt of the screw inside the feed hose is derived; borderline results are checked by CAD against the screw dimension sheet. If the answer is negative, a smaller head or a longer shank can make the screw feedable; if the screw cannot change, pick-and-place by vacuum, gripper or magnet is the alternative. [3]
DEPRAG notes that DIN screw quality allows 3 defective screws in 100, and that the purity level needed for the feeder's availability is calculated per application against VDI 3423. [3] Editorial calculation: if 3 in every 100 screws were defective and a part takes, for example, 10 screws, about 26% of parts would meet at least one defective screw if defects were spread at random (1 − 0.97¹⁰ ≈ 0.26); the example is an illustration, not a DEPRAG figure.
For feeding more than one screw position, simple distributors can only supply positions that use screws at the same rate, while twin vibratory bowl feeders with a double helix serve two positions independently; DEPRAG says its eacy feed bowl, available as a twin unit, saves up to 80% energy. [3] DEPRAG's feeding range covers standard fasteners from M1 to M16 by vibratory, sword (segment) or tape-on-reel systems, through a hose or by pick-and-place. [4]
Atlas Copco's SF36 step feeder sorts and blow-feeds M3 to M6 screws into the tightening module with 3 L of filling volume, and is described as quieter and less abrasive to sensitive screw coatings than conventional bowl feeders. [2]
Send the screw drawing (head diameter and height, shank length, thread, coating), the quality level the screws are bought to, the number of screw positions and the rate at each.
04
Deep screw locations and templates: keeping the screw from falling into the bore
Where the screw has to pass through a recess to a deep location, DEPRAG describes the risk it calls "free fall": the screw drops into the bore, misses the core hole, tilts and blocks the process. [3]
DEPRAG's answer is a feed module with a vacuum screw holder, a feed stroke and a guided vacuum tube that carries the screw down to the recessed location. The screw holder is otherwise a ball chuck, which centres in the area of the screw location, or a jaw chuck, which needs room to open its jaws. [3]
Screw templates with conical guide bushes stop the chuck slipping on inclined housing surfaces; DEPRAG says the time to place and remove the template can be recovered as the number of screw locations rises, and uses templates where sensitive electronics parts must not be damaged during positioning. [3]
05
What to send for a fastener installation module
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Screws: [drawing; size; head diameter; length; coating; quality level]
Joint: [target torque and tolerance; angle; material]
Part: [screw locations; depth; access angle; clearance]
Carrier: [robot, Cartesian slide or fixed station]
Rate: [screws per part; cycle time]
Feeding: [bowl, step or sword feeder; one or more positions]
Data: [results to record per screw]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What is the difference between bit-stroke and head-stroke screw feeding heads?
In Atlas Copco's module the bit-stroke version only moves the bit and relies on a robot or slide for Z motion (4.3 kg with tool); the head-stroke version moves the feeding head 48 mm toward the part while the motor stays put (6 kg with tool). Both are rated 10 Nm. [1]
How do you know if a screw can be blow-fed through a hose?
DEPRAG uses the ratio of screw length to head diameter to estimate how far the screw can tilt in the hose, then checks borderline cases by CAD; a smaller head or longer shank can make it feedable. [3]
Which screw sizes can a step feeder handle?
Atlas Copco's SF36 step feeder handles M3 to M6 screws with a 3 L filling volume. [2]
Why does screw quality matter for automatic feeding?
DEPRAG notes that DIN quality allows 3 defective screws in 100, which may not be enough for feeder availability; it calculates the needed purity per application against VDI 3423. [3]
Sources and what still needs a direct check
Sources checked 2026-10-12. Head versions, weights, sensors and spindle ranges come from Atlas Copco's system description of its fixtured screw feeding system; the step feeder from Atlas Copco's SF36 page; feedability, screw quality, multi-position feeding and deep locations from a DEPRAG interview on reinraum.de; DEPRAG's torque and fastener ranges from its screwdriving technology page.