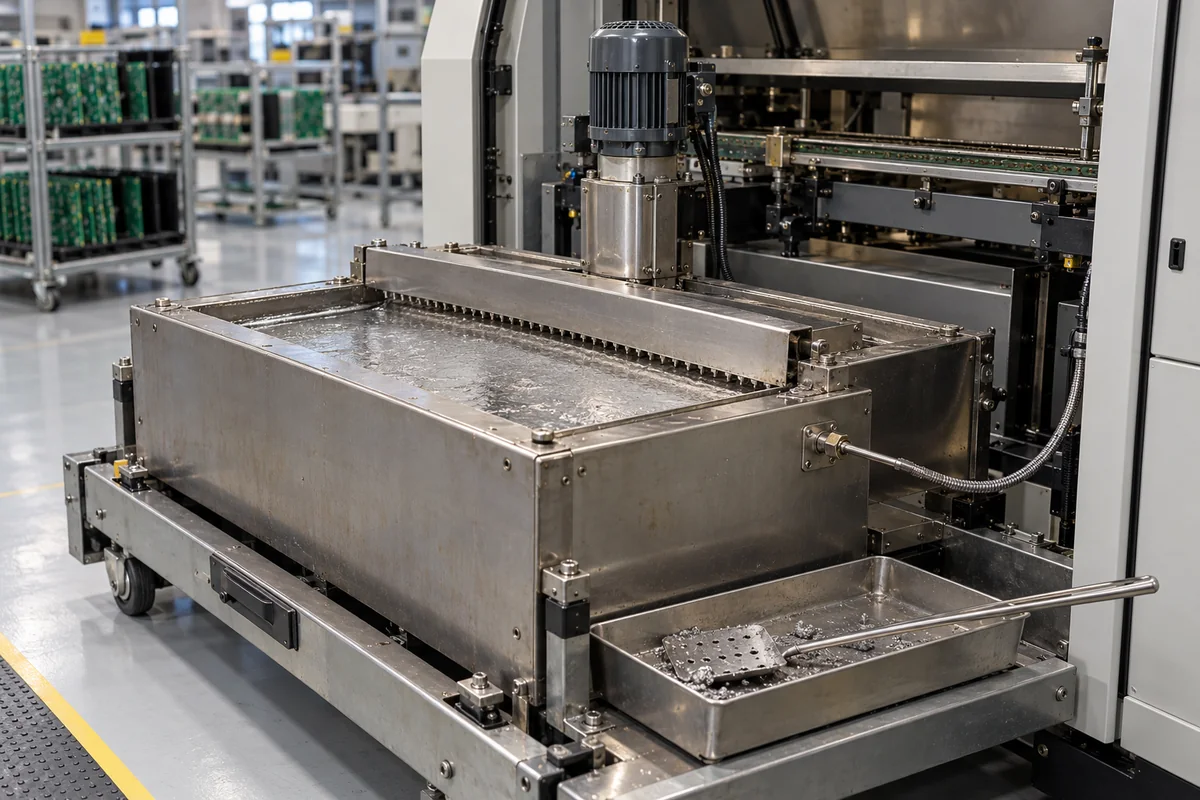
Wave soldering solder pots (solder baths) · the reservoir of molten solder that feeds the wave nozzles, solder content, alloy and pot temperature, copper pick-up and pot analysis, dross, and serviceability
In a wave soldering machine, the solder pot holds the molten solder from which the wave is pumped up through one or two nozzles to meet the underside of the board. Contamination of the solder in the pot affects wetting and joint quality. Ask three things first: which machine and working width the pot must fit, which alloy and pot temperature you will run, and how solder level, contamination and dross will be managed.
Solder pots (solder baths) and their solder wave modules in wave soldering machines for printed circuit boards. Small dip pots for wire and component tinning, selective soldering pots and the solder alloy itself are outside this page except where compared.
CNFX editorial research · Sources checked October 11, 2026 · 6 sources
Ersa, a wave soldering machine maker, describes its POWERFLOW soldering module as a solder wave module with one or two nozzles that match the conveyor width, so that the full surface of the board contacts the solder. Capillary and wetting forces draw the solder up the pins to the top of the board, where it solidifies as the wave breaks away. Ersa adds that its soldering pots can be moved out of the machine electrically for maintenance, and that preheating supplies up to 50% of the thermal energy so the board is not shock-heated on contact with the solder. [1]
Ersa lists a soldering module solder content of 525–630 kg depending on configuration for the POWERFLOW PRO, and 525–725 kg for the POWERFLOW ULTRA, which comes in working widths from 330 mm up to 610 mm (XXL version). Both are full-tunnel nitrogen machines. [2][3]
Editorial calculation: 525–725 kg is about 1,160–1,600 lb of solder in the pot.
Give the supplier the machine make and model or the working width, the alloy, the pot temperature range, the solder content, the number and type of nozzles, nitrogen or air operation, the heating power and heat-up time, the pot material, how the pot is moved for service, and the level-control and dross-handling arrangements.
02
Keep the solder in the pot within specification
Indium Corporation, a solder maker, explains that during wave soldering, molten solder contacting copper-containing boards such as OSP boards pulls copper into the wave and raises the copper content of the pot. As copper rises out of specification, wetting and joint appearance suffer. It says a pot that collects excess contaminants from boards and components, or too little of the important alloy elements, makes the solder sluggish. The result is overly large fillets, poor wetting and bridging. [4][5]
Indium recommends frequent analysis of wave soldering pots. It sells a replenisher bar, added to the pot rather than into the wave in a calculated amount, to bring copper back within specification. It also states that up to 50% of bar solder used in wave soldering becomes dross. [4][5]
Alloy choice changes the pot temperature. Indium states that its Indalloy 291 tin–copper–nickel alloy (melting point 227 °C) needs the pot about 10 °C hotter than SAC305. At 260 °C it lists dross rates of 54.30 g/h for Indalloy 291 and 65.44 g/h for SAC305 in its own test. [5]
03
Trace the pot and wave module parts
This is a functional reference built from the sources cited; it is not one maker's specification.
Part
Role
Fix in the order
Pot (solder bath)
Holds the molten solder: 525–725 kg in the cited machines. [2][3]
Solder content; material.
Wave nozzles
One or two nozzles matching the transport width. [1]
Bar or chips; replenisher bars go into the pot, not the wave. [4][6]
Level control; feeder.
04
Fill the specification fields with values for your line
A solder pot quotation needs values for your line. The table explains each field, gives published values where a reviewed source states them, and says what to ask the supplier for.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 13 October 2026
Buyer questions
How much solder does a wave soldering pot hold?
Ersa lists 525–630 kg for its POWERFLOW PRO and 525–725 kg for its POWERFLOW ULTRA, depending on configuration. [2][3]
Why does solder in the pot go out of specification?
Indium explains that copper from the boards is pulled into the wave and raises the pot's copper content, so it recommends frequent analysis. [4][5]
How much solder becomes dross?
Indium states that up to 50% of bar solder used in wave soldering is converted to dross. [4]
Sources and what still needs a direct check
Sources checked 2026-10-11. Ersa describes its own wave soldering machines. Indium Corporation describes its own solder bars and wave soldering practice; their figures are examples, not limits.