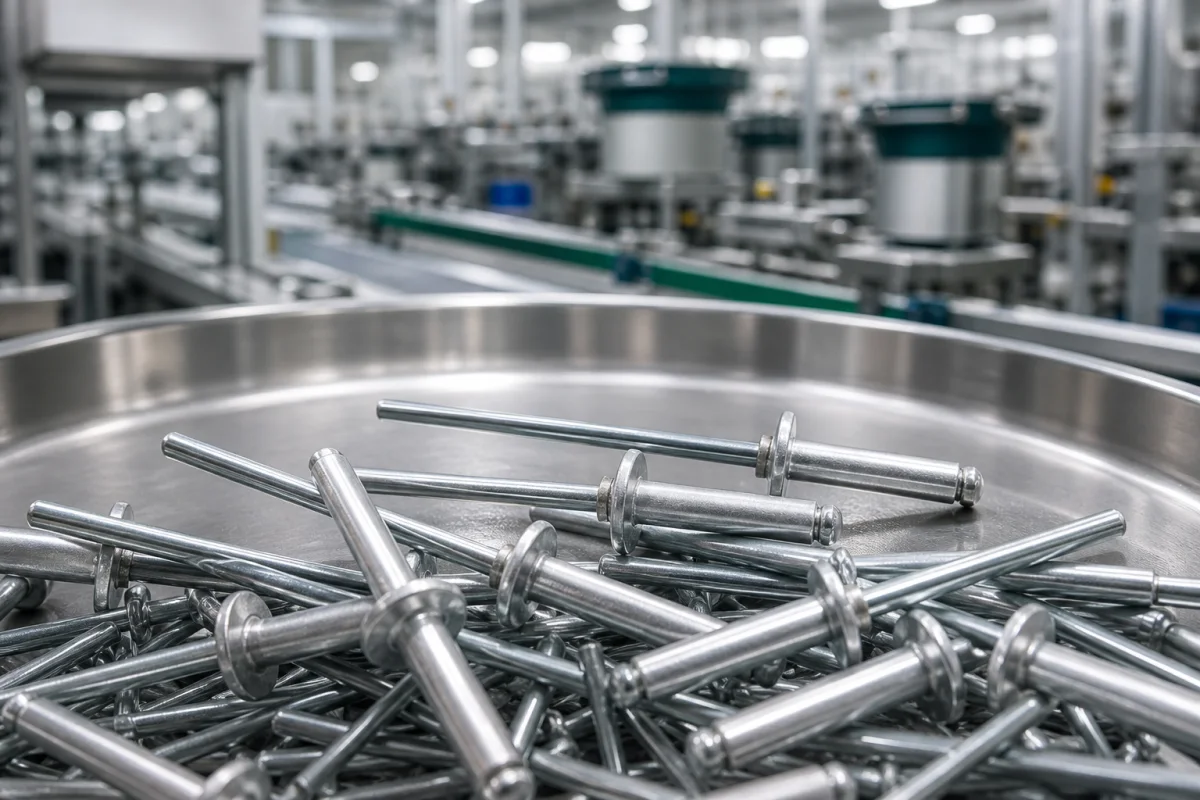
Blind rivets · break-mandrel and locked-stem types, DIN 7337 and similar standards, diameter, length and grip range, body and mandrel materials, edge distance and spacing, where blind rivets should not be used
A blind rivet is a tubular rivet with a mandrel through its centre, set from one side of the work: a tool pulls the mandrel, which expands the far end of the rivet into a blind head and clamps the sheets, then the mandrel breaks off. Ask three things first: which type and body and mandrel materials suit the joint, what diameter and length match the hole and total grip thickness, and whether a blind rivet is acceptable at that location at all.
Open-end and closed-end break-mandrel blind rivets and locked-stem structural blind rivets, with dome, countersunk or large flange heads, in aluminium alloy, steel, stainless steel and copper. Solid rivets, rivet nuts, drive rivets and riveting tools are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
FAA advisory circular AC 43.13-1B, on acceptable methods for aircraft repair, says blind rivets are used where there is access to only one side of the structure, and that their locking characteristics are not as good as a driven rivet's in its assessment, so it prefers driven rivets wherever they can be installed, and says blind rivets shall not be used in fluid-tight areas or on control surfaces and hinges. It describes self-plugging friction-lock rivets, whose stem is held only by friction and is sensitive to vibration, and mechanical-lock rivets such as Bulbed Cherrylock, which carry a lockring that locks the stem and can replace a solid rivet size for size; their lengths come in 1/16 in increments and must be chosen to match the grip length of the metal being joined. [1]
Haiyan Bolt, a linked fastener maker, lists DIN 7337 open-end blind rivets of 2.4 to 5 mm diameter and 6 to 25 mm length, with dome, countersunk or flange heads, in aluminium 5050/5154 or stainless steel, and aluminium-body blind rivets with steel large heads. [2]
Editorial note: give the supplier the total thickness of the parts being joined so it can choose the rivet length whose grip range covers it, and the hole diameter you will drill.
GESIPA's product pages show the strength and hole data to ask for. Its 4 × 8 mm aluminium-alloy dome-head rivet with a zinc-plated steel mandrel lists a 4.10 mm hole, 8.00 mm head and 2.10 mm mandrel, with shear strength of 1,400 N and tensile strength of 2,000 N. [4] The large-head aluminium/steel rivet of 4.8 × 12 mm sold through its parent SFS lists a 6–8 mm clamping (grip) range, a 4.9 mm drill, a 16 mm head on a 4.8 mm body with a 2.7 mm galvanised steel mandrel, shear strength of 1,800 N and tensile force of 2,700 N. [3]
Give the supplier the rivet type (open or closed end, structural locked-stem), standard (DIN 7337, ISO 15977 or other), diameter and length or grip range, head style, body and mandrel materials, finish, hole diameter, materials joined (to avoid galvanic problems), required shear and tensile strength, quantity and packing, and tool compatibility.
02
Place them at the right spacing and only where allowed
AC 43.13-1B defines edge distance as the distance from the hole centre to the nearest sheet edge and spacing as the distance between hole centres; where the original pattern cannot be copied, single-row rivets should have edge distance of at least 2 rivet diameters and spacing of at least 3 diameters. It says blind rivets shall not be used in fluid-tight areas, in air intakes where parts could be ingested, on control surfaces, hinges, flight-control actuating systems, wing attachment and landing-gear fittings, below the waterline on floats or hulls, or in other heavily stressed locations, and that for airframe metal repairs blind rivets need the manufacturer's or FAA's approval. [1]
Editorial calculation: for a 4.8 mm blind rivet in a single row, the minimum edge distance would be 2 × 4.8 = 9.6 mm and the minimum spacing 3 × 4.8 = 14.4 mm. The rivet size is an assumed example and the FAA figures are for aircraft repair; follow the design code or drawing for your product.
Editorial calculation: six 14.4 mm spacings fit within a 100 mm single-row seam, so it holds seven 4.8 mm rivets, giving 7 × 1,800 N ≈ 12.6 kN of catalogue shear before any design factor; confirm the joint allowable with the sheet bearing strength. [1][3]
03
Compare what suppliers offer
Suppliers linked to this page list blind rivets; each card links to the page reviewed.
Listings include DIN 7337 open-end blind rivets and large-head blind rivets from fastener makers, blind rivets alongside screws and pins, and blind rivets from fastener trading companies. Rivet tool and fastener-machine makers are hidden here. Ask each for standard, grip ranges, strength data and material certificates.
04
Trace the rivet parts
This is a functional reference built from the sources cited; it is not one maker's specification.
Fill the specification fields with values for your joint
A blind rivet quotation needs values for your joint. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 13 October 2026
Buyer questions
Are blind rivets as strong as solid rivets?
FAA AC 43.13-1B says their locking is not as good as driven rivets; locked-stem types such as Bulbed Cherrylock can replace solid rivets size for size. [1]
How do I choose blind rivet length?
Match the rivet's grip range to the total thickness being joined; FAA notes lengths in 1/16 in steps tied to grip length. [1]
What edge distance should blind rivets have?
AC 43.13-1B gives at least 2 diameters edge distance and 3 diameters spacing for single rows where the original pattern cannot be copied. [1]
How strong is a 4.8 mm aluminium blind rivet?
GESIPA's 4.8 × 12 mm large-head aluminium/steel rivet lists 1,800 N shear and 2,700 N tensile strength, set in a 4.9 mm drilled hole for a 6–8 mm grip. [3]
Sources and what still needs a direct check
Sources checked 2026-10-12. FAA AC 43.13-1B is US aviation guidance on acceptable repair methods, a demanding blind-rivet use; Haiyan Bolt is a fastener maker describing its own rivets; GESIPA is a blind-rivet maker whose product data is cited.