Workpiece Handling Mechanism
View system integration details
This page explains how Gripper or Fixture is classified within Machinery and Equipment Manufacturing. Technical values and manufacturer relationships are research references; confirm the current specification and supplier evidence for each order.
A mechanical device used to securely hold, position, or manipulate workpieces during manufacturing processes.
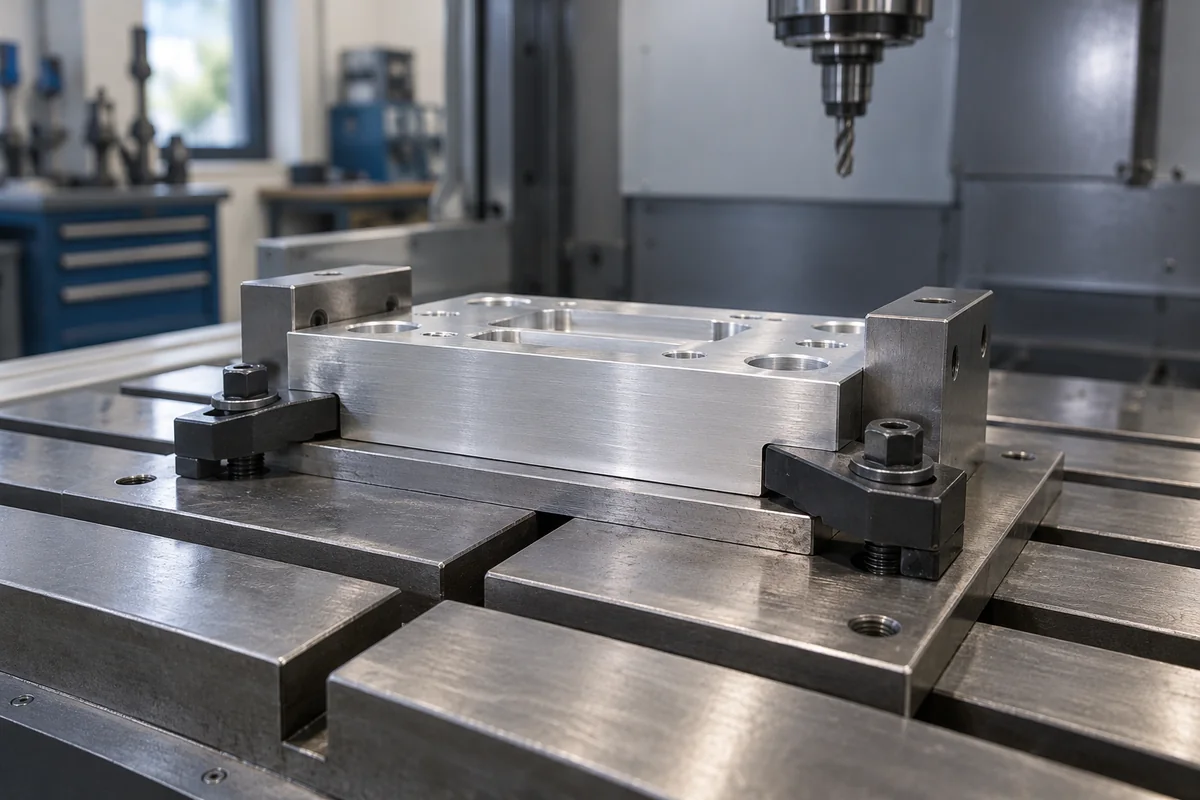
Technical details and manufacturing context for Gripper or Fixture
| Parameter | Typical range | Notes & selection driver |
|---|---|---|
| Clamping Force | 5–50 kN | Required to hold workpiece securely during machining |
| Operating Pressure | 0.4–0.8 MPa | Below 0.4 MPa insufficient clamping force |
| Repeatability | ±0.02 mm | Critical for automated processesISO 230-2 |
| Positioning Accuracy | ±0.05 mm | Ensures consistent workpiece locationISO 230-2 |
| Operating Temperature | -10–60 °C | Outside range may affect seal integrity |
| Ingress Protection | IP54–IP65 | Higher rating for coolant exposureIEC 60529 |
| Material | 6061-T6 | Aluminum alloy for lightweight and corrosion resistanceASTM B221 |
| Weight | 2–15 kg | Affects machine dynamics and handling |
| Footprint | 100×100–300×300 mm | Must fit within machine work envelope |
| Actuation Type | Pneumatic | Pneumatic for fast cycling; hydraulic for high force |
Ranges are indicative industry figures for RFQ preparation, not a supplier commitment. Confirm every value and standard with the legal manufacturer before ordering.
| pressure: | 0 to 10 bar |
| grip force: | 10 to 5000 N |
| temperature: | -20°C to 150°C |
| repeatability: | ±0.01 to ±0.1 mm |
Indicative industry ranges for design and RFQ preparation. Confirm the exact figures and applicable standard with the manufacturer before specifying.
Quoted from the published standard.
A practical evidence checklist for RFQ preparation and supplier evaluation.
Compare the published product scope and source details, then include your specifications and quantity in an enquiry.
Manufacturer profiles associated with Gripper or Fixture.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.
A gripper is a device that actively grasps and holds a workpiece, often used in automated handling. A fixture is a passive structure that locates and restrains a workpiece during processing, such as machining or assembly. Both ensure secure positioning but serve different roles in the production line.
The required clamping force depends on the workpiece weight, material, and process forces. The directory lists a reference range of 5–50 kN. For light-duty operations, lower force may suffice; for heavy machining, higher force is necessary. Always calculate based on your specific process and verify with the manufacturer.
Repeatability is typically specified as ±0.02 mm per ISO 230-2. To verify, perform repeated positioning tests under controlled conditions and measure the variation. Ensure the test method aligns with the standard and that the equipment is properly calibrated.
Common standards include for operating pressure, ISO 230-2 for repeatability and positioning accuracy, IEC 60529 for ingress protection, and ASTM B221 for aluminum alloy material. These are reference standards; confirm compliance with the supplier for the specific model.
This component is essential for the following industrial systems and equipment:
Editorial classification, named public sources where available, and source-reviewed manufacturer records.
Compare manufacturer profiles with relevant product and process capability.