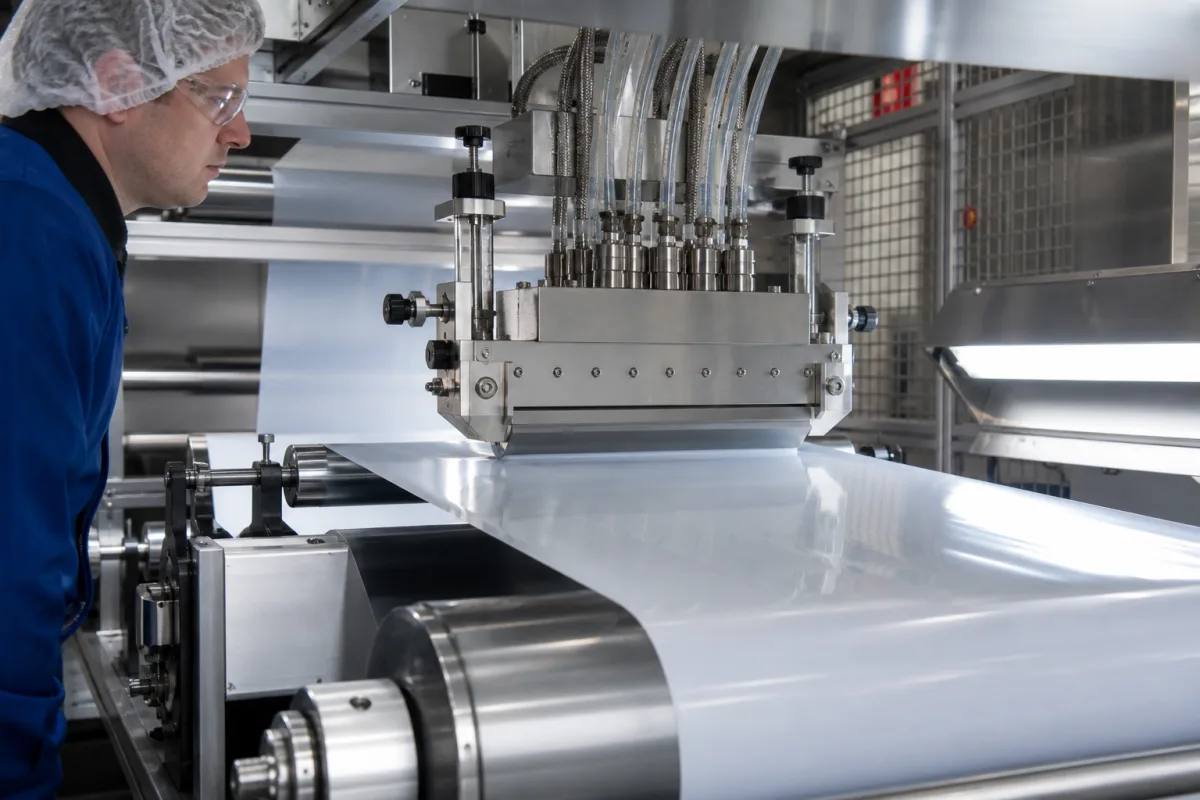
Slot-die coating heads · Pre-metered thickness, coating window and low-flow limit, vacuum on the bead, die lip configuration
A precision coating applicator of the slot-die type is a die that distributes coating liquid across its width through an internal cavity and a narrow slot, depositing it onto a moving web or substrate across a small gap, with the coated thickness set by the metered flow rather than by scraping. Ask three things first: what wet thickness, speed and width you need and what flow that implies, whether your liquid and gap sit inside the coating window, and how the die lips, gap and bead vacuum are set and held.
Slot-die and similar pre-metered coating heads for films, foils, battery electrodes, adhesives and functional coatings, with their pumps and positioning. Roll, gravure and knife coaters, spray valves for conformal coating and complete coating lines are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
A PUC-Rio study of slot coating presented at ENCIT 2006 describes the process: the liquid is pumped to a die whose elongated chamber distributes it across the width of a narrow slot, so the flow per unit width at the exit is uniform; exiting the slot it fills the gap between the die lips and the moving substrate, forming the coating bead between upstream and downstream menisci. It is a pre-metered method: the coated layer thickness is set by the flow rate fed to the die and the substrate speed, which makes it suited to high-precision coating. [1]
The same paper notes that bead flow, and so coating quality, is strongly affected by substrate speed, viscosity and the shape of the die lips just upstream and downstream of the slot, and lists operating parameters as gap, flow rate per unit width, web speed, die configuration, liquid and roll-cover properties. [1]
Editorial calculation: a 20 µm wet layer, 0.5 m wide, at 30 m/min (0.5 m/s) needs 20 × 10⁻⁶ × 0.5 × 0.5 = 5 × 10⁻⁶ m³/s, or 300 mL/min, from the metering pump. Ask the supplier how pump accuracy and pulsation are controlled.
Give the supplier the liquid (viscosity and its shear dependence, surface tension, solids, density), target wet and dry thickness and tolerance, coating width and edge requirements, web speed range, substrate and backing roll, stripe or intermittent pattern, gap range, vacuum box need, pump type, cleaning, and materials of construction.
02
Stay inside the coating window
The PUC-Rio paper defines the coating window as the region of operating parameters giving an acceptable uniform layer, bounded by three failure modes: too much vacuum on the upstream meniscus draws liquid into the vacuum chamber and destroys pre-metering; too little vacuum lets the upstream meniscus move to the feed slot and the bead turn three-dimensional; and below the low-flow limit the bead breaks into rivulets or droplets. Vacuum on the upstream meniscus is used to sustain the bead at higher speeds. [1]
The low-flow limit is the minimum thickness that a gap of given clearance can deposit at a given speed; seen from other directions it is the high-speed limit at a given flow, or the wide-gap limit, the largest gap that can deposit a given thickness at a given speed. In the paper's simulations with a 100 µm downstream gap, the upstream meniscus moved toward the feed slot as the film became thinner; with an underbite lip it sat closer to the slot and was less sensitive to thickness, while with an overbite lip it was more sensitive. [1]
Researchers at the University of New Mexico and Sandia National Laboratories describe the low-flow limit as the minimum uniform, defect-free film achievable for given liquid properties and die-substrate geometry, important for sub-micron wet films of costly inks, where start-up and shut-down transients matter more than speed. [2] Editorial note: ask suppliers to show the coating window measured with your liquid on their die.
The backup roll under the die is part of the window. A 2026 study by Konkuk University with the Korea Institute of Machinery and Materials and the Korea Textile Machinery Convergence Research Institute (Polymers, 2026) explains that eccentricity of the backup roll makes the effective radius rise and fall once per revolution, so web tension, web speed and the coating gap fluctuate periodically and the meniscus changes shape. Its roll-to-roll rig coated a 40 wt% silver nanoparticle ink (7.7 cP, 19 mN/m) onto 75 µm PET film 150 mm wide, at a 200 µm coating gap, 0.5 m/min web speed, 3 mL/min flow, 176.4 N/m web tension (set at about 10–25% of the film's yield strength) and a 90 °C drying zone, and imaged the meniscus at 10 Hz for eccentricities of 10, 20, 30 and 40 µm. Predicting eccentricity from meniscus images gave an RMSE of about 0.63 µm and R² above 0.93, outperforming predictions from web-tension signals. [4]
Editorial calculation: eccentricities of 10–40 µm are 5–20% of the 200 µm gap. If the ink were coated across the full 150 mm web width (an assumption; the coated width is not stated), 3 mL/min at 0.5 m/min gives a wet thickness of 3 × 10⁻⁶ m³ ÷ (0.15 m × 0.5 m) = 40 µm. Ask the coater supplier for backup roll runout and how gap variation is measured at your gap. [4]
03
A pilot slot-die head's published data, plus servo heads and hot-melt slot guns
One maker's data for a laboratory and pilot slot-die head (FOM Technologies, SD 200) show the fields a head is specified by: stainless steel, chemically passivated; coating width 1–200 mm, set by the shim; viscosity rating from 1 cP to more than 100,000 cP at 25 °C in standard and high-viscosity versions, with the practical upper limit also set by the pump and fluid; flatness 5 µm or better; stainless shims and meniscus guides from 50 µm to 500 µm; optional head heating to 80 °C; patterned shims for stripes; 240 × 40 × 70 mm and 4.06 kg. The maker offers a PEEK series for chemistries that attack stainless steel. [3]
Editorial note: shim thickness sets the slot gap the distribution cavity feeds, so ask the supplier which shim thickness it recommends for your viscosity and width, and for the flatness of the lips over your full coating width, not only over a short length. [3][1]
Listings include servo coating heads and continuous and intermittent hot-melt slot coating guns with adhesive melters.
04
Distribution cavity, slot and shims, die lips, gap positioning, vacuum box and metering pump
Thickness is set by the pump, not the die: the metering pump fixes flow and therefore wet thickness, while the cavity, slot, lips, gap and vacuum decide whether that flow lays down as a uniform layer. [1]
Coating width, wet thickness, web speed, viscosity, gap, lips and vacuum for a coating head quotation
The thickness, gap and speed rows are linked by the low-flow limit, the thinnest layer a given gap can lay down at a given speed, so ask for the coating window measured with your own liquid rather than single ratings. [1][2]
Field
What it means and published values
Ask the supplier for
Coating width (mm)
Die width and edges; e.g. 1–200 mm set by the shim on one head. [3]
Width and edge control.
Wet thickness range (µm)
Set by flow and speed; bounded by the low-flow limit. [1]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What sets the thickness in slot-die coating?
It is pre-metered: the flow fed to the die and the substrate speed set the coated thickness, per the PUC-Rio analysis. [1]
What is the low-flow limit?
The minimum thickness a gap of given clearance can deposit at a given speed; thinner flows break into rivulets or droplets. [1][2]
Why is vacuum applied to a slot-die bead?
To sustain the bead at higher speeds; too much draws liquid into the vacuum chamber, too little lets the meniscus reach the feed slot. [1]
What sets the coating width of a slot-die head?
The shim: one maker's 200 mm head coats from 1 to 200 mm with stainless shims of 50–500 µm. [3]
Does backup roll runout affect slot-die coating?
Yes. A 2026 Polymers study shows backup roll eccentricity makes tension, speed and the coating gap fluctuate each revolution; it tested 10–40 µm eccentricity at a 200 µm gap. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Two sources are research papers on slot coating flow (PUC-Rio, ENCIT 2006; University of New Mexico and Sandia, ISCST 2018 abstract) and a 2026 Polymers paper from Konkuk University and Korean research institutes measures the effect of backup roll eccentricity; FOM Technologies describes its own head. Windows for a given liquid and die must be measured.