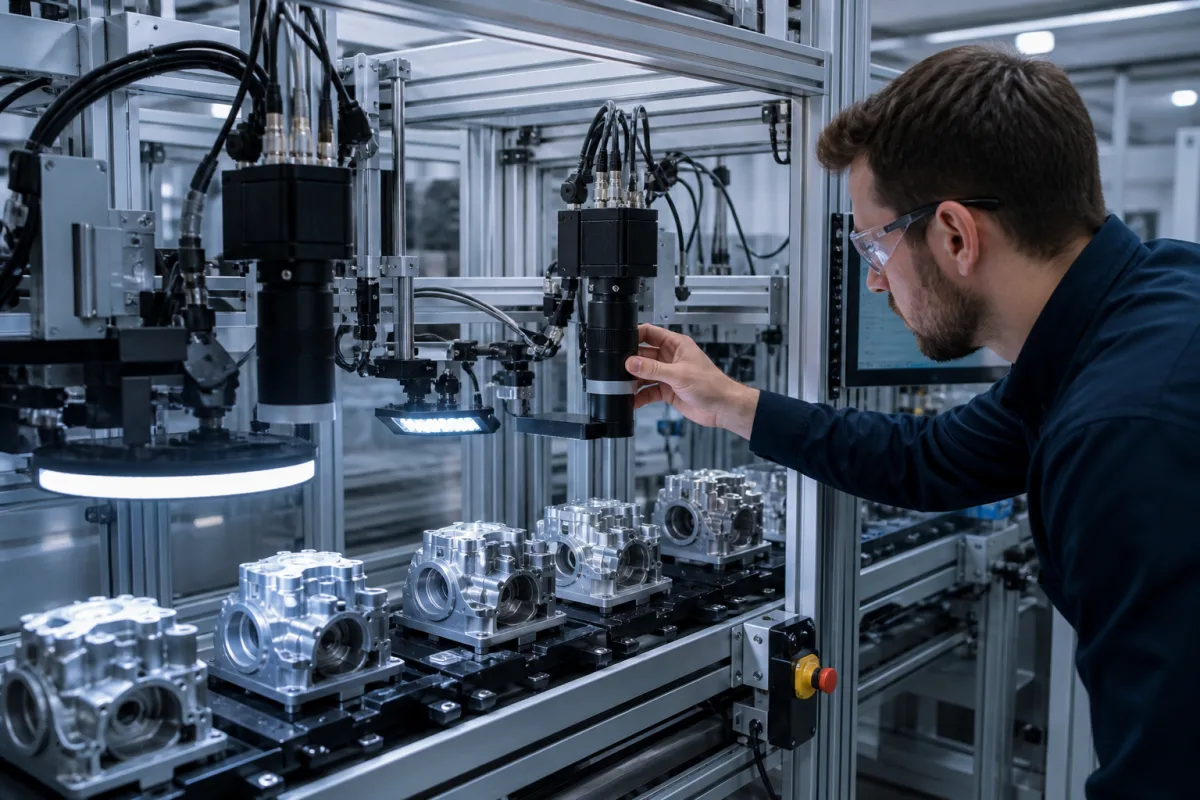
Vision system for cast and machined parts: a multi-camera inspection station that finds casting surface defects on the line
In-line vision inspection stations for cast and machined metal parts · Multi-camera cells with strobed multi-angle lighting, casting surface defect classes and depth thresholds, cycle time per part, and detector accuracy on casting datasets
This page covers in-line vision inspection stations for cast and machined metal parts: cells in which multiple cameras and strobed lights at different angles image each part on a conveyor and software flags casting and machining surface defects. Ask three things first: which defect classes and minimum depths the station must find on your parts, how long image capture takes against your cycle, and what detection and false-reject rates the supplier has measured on parts like yours.
In-line vision inspection stations for cast and machined metal parts, including multi-camera cells with strobed multi-angle or 3D lighting and the defect-detection software that runs them. Camera-based inspection, measurement and guidance systems for production lines, and their cameras, lenses and lighting, are covered on the Machine vision system page. X-ray and CT inspection of internal casting defects, vision measuring machines and pharmaceutical vial inspection machines are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
Eight casting surface defects and the depth at which each counts
A 2025 Scientific Data paper describing the Metal Surface Defect Dataset (MSDD) of aluminium alloy casting defects separates real defects from harmless surface features by depth: a low-reflectivity stain is not an inclusion, but a hole deeper than 0.5 mm is; tool-vibration lines are not cut marks, but marks deeper than 0.1 mm are. [1]
Give the supplier sample parts with each defect class you reject and good parts with the harmless features that must pass, the depth or size limits for each, the surfaces to inspect, the line rate and part presentation, and how rejects are to be marked or diverted.
02
Strobed lights from all around and cameras at different heights, inside a 300-parts-per-hour cycle
The MSDD acquisition method places multiple CCD cameras and light sources around the part at different heights, and a PLC strobes the lights in sequence with the cameras so each part is imaged under light from different angles; each camera runs at 30 frames per second and the whole capture takes 0.96 s, which the authors state meets the 300 parts per hour of an aluminium alloy casting line. Images from the different light angles are blended into pseudo-colour images for standard object detectors; the dataset holds 138,585 single-channel and 9,239 blended images, four detectors reached 86.1% mAP on it, and the authors report that the method struggles on highly reflective surfaces such as polished metal, where the lights produce reflections. [1]
Editorial calculation: 300 parts per hour leaves 12 s per part, so 0.96 s of image capture uses 8% of the cycle; at 30 frames per second each camera takes about 29 frames in that time. [1]
Hanchine lists bearing surface inspection machines, models HZ-VI-BB0515, HZ-VI-BB1530 and a 3060 model, integrating 2D and 3D vision, alongside bearing roller and ring inspection machines. [3]
03
Detector accuracy and speed on a casting surface defect dataset
A 2024 Sensors study of casting surface defect detection reports [email protected] on its casting dataset of 0.783 for RetinaNet, 0.827 for YOLOv5n, 0.832 for YOLOv8n, 0.835 for Faster R-CNN, 0.846 for Mask R-CNN, 0.854 for TOOD and 0.862 for its own SLGA-YOLO; the YOLO models need 2.5–3.0 million parameters and 7.1–10.9 GFLOPs, against 32–48 million parameters and 199–274 GFLOPs for Mask R-CNN, Faster R-CNN, TOOD and DINO. In its ablation, the baseline YOLOv8n ran at 105 frames per second and SLGA-YOLO at 133. [2]
Editorial note: an mAP near 0.86 means some defects are still missed or mislocated; ask the supplier for detection and false-reject rates per defect class, measured on your own parts across multiple shifts, rather than a dataset mAP.
04
Send the parts, defect limits and line timing together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Parts: [alloy; process; surfaces to inspect; finish]
Defects: [classes; depth or size limits; samples]
Line: [parts per hour; presentation; fixturing]
Imaging: [2D; multi-angle strobe; 3D]
Output: [reject signal; marking; data logging]
Acceptance: [detection rate; false-reject rate; trial parts]
Compare casting and machined-part inspection station suppliers
7 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Hanchine
Manufacturing site to be confirmed for the order
Lists bearing surface inspection machines (HZ-VI-BB0515, HZ-VI-BB1530) with 2D and 3D vision.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What casting defects can a vision system find?
The MSDD casting dataset covers inclusions, cut marks, stamp collapse, mould scuffing, dents, pockmarks, parting line cracks and misruns, counted as defects above 0.5 mm depth (0.1 mm for cut marks). [1]
How fast can a casting be imaged for inspection?
In the MSDD study, strobed multi-angle capture at 30 frames per second took 0.96 s per part, meeting a 300 parts per hour aluminium casting line. [1]
How accurate is AI defect detection on castings?
On one casting surface dataset, detectors scored 0.783 to 0.862 [email protected]; on the MSDD dataset four detectors reached 86.1% mAP. [2][1]
Sources and what still needs a direct check
Sources checked 2026-10-12. Two peer-reviewed studies report casting inspection data and detector results; Hanchine lists its own machines.