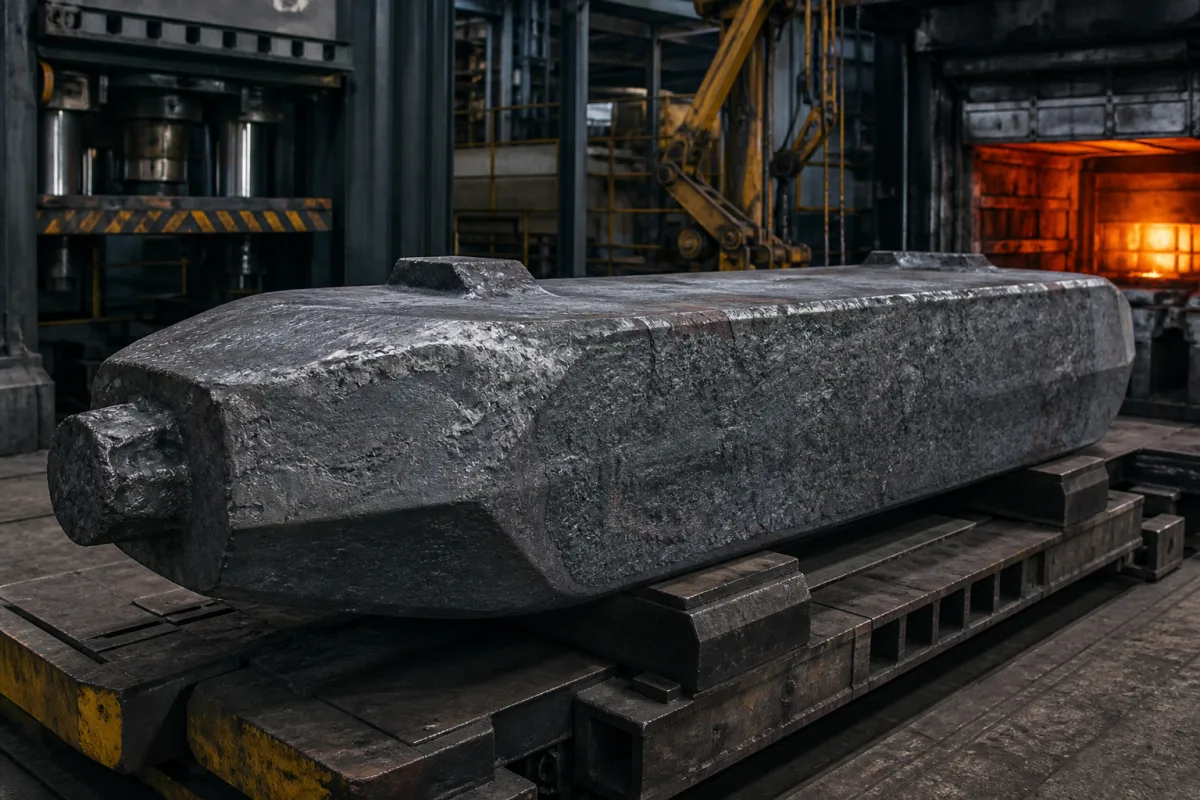
Cast steel ingots for heavy open-die forgings · Melting, ladle refining and vacuum degassing, bottom pouring into cast iron moulds, hot top design and macrosegregation, chemistry limits for rotor-quality steel, and what to ask for with each heat
A forging ingot is a large steel casting made to be hot forged into heavy parts such as shafts, rotors and dies. Its quality depends on the melting and degassing route, how it is poured, and how the mould and hot top control solidification, because chemical segregation and shrinkage in the ingot cannot always be removed later. Ask three things first: the grade, chemistry limits and ingot weight you need, the melting, degassing and pouring route, and how the hot top and discard are designed to keep segregation out of the forging.
Cast carbon and low-alloy steel ingots for open-die forging, from a few tonnes to heavy ingots, including their melting, refining, vacuum degassing, teeming, moulds and hot tops. Continuously cast blooms, forged bars and finished forgings, and non-ferrous ingots (see high purity aluminium alloy ingot) are outside this page except where compared.
CNFX editorial research · Sources checked October 11, 2026 · 4 sources
Set grade, chemistry and the melting and pouring route
A 2022 open-access paper in Metals (Ghodrati et al., with an industrial ingot producer) states that ingot casting is the primary process for heavy mono-block forgings of high-strength steels, and names the energy, transport and machinery industries as “the main users of such heavy blocks”, which are machined into power transmission shafts or forming dies. It describes a 12 t polygonal ingot of modified AISI 4130 Cr-Mo steel (0.32 C, 0.57 Mn, 0.015 P, 0.001 S, 0.27 Si, 0.23 Ni, 1.08 Cr, 0.34 Mo, 0.16 Cu wt.%) melted from scrap in an electric arc furnace, refined in a ladle furnace and vacuum degassed, then bottom-teemed for 26 min at 1580°C through a trumpet and runner into a cast iron mould. The ingot was about 2000 mm high with 1266 mm top and 1000 mm bottom diameters. [1]
US patent 3,907,547 (Method of preparing vacuum-treated steel for making ingots for forging) addresses forging ingots of great weight and high purity for rotors, turbine shafts, inductor shafts and other large steel parts, and targets vacuum-treated steel with phosphorus and sulfur each below 0.010 wt.% and carbon of 0.10 to 1 wt.%. [3]
Editorial calculation: the published heat had 0.015% P and 0.001% S, so it would meet the patent's sulfur target but not its phosphorus target; set phosphorus and sulfur limits to suit the forging, not by grade name alone. [1][3]
Give the supplier the steel grade and full chemistry limits (including P, S and residuals), ingot weight, shape and taper, the forging it will become, melting route (EAF, ladle refining, vacuum degassing), hydrogen limit, pouring method (bottom or top teeming) and temperature, mould and hot-top design, discard allowances, heat records and ladle analysis, and any ultrasonic or macro-etch tests on trial ingots.
02
Control macrosegregation with the hot top
The Metals paper defines macrosegregation as "the non-uniform distribution of alloying elements over several centimeters" and says it can be so severe that it cannot be removed even by long homogenising heat treatment, degrading the final part's properties. An ingot set-up comprises the mould, hot top, sideboards, riser, runner and trumpet; the hot top, at the top of the mould with sideboards and a topping compound, feeds the ingot during solidification, controls heat flow at the top, and gives a region where segregates and inclusions can gather. In the 12 t ingot the hot top was 381 mm high, lined with 177 mm insulating tiles, with two exothermic caps. [1]
Its model, validated on the sectioned ingot, found that raising the hot top by 165 mm lengthened solidification by up to 8 minutes and reduced negative and positive macrosegregation at two heights by up to 6.25% and 6.5%. [1] A 2024 follow-up in the Journal of Manufacturing and Materials Processing on the same ingot type found that changing hot-top heat capacity increased solidification time by about 2% to 31%, that a fully refractory-coated hot top reduced segregation in the hot top and upper half of the ingot, and that the new designs increased hot-top material yield by 10 to 29%. [2]
Editorial calculation: the 381 mm hot top is about 19% of the roughly 2000 mm ingot height in the published set-up; ask the supplier for the hot-top height and the top discard it plans for your ingot weight. [1]
03
Tie the ingot to the forging specification
The forging that will be made from the ingot sets which melting route is acceptable. ASTM A788/A788M, the general-requirements specification for steel forgings, says material shall be produced primarily by electric-furnace, basic oxygen, vacuum-induction (VIM) or open-hearth melting; the primary melting may include separate degassing or refining, and may be followed by secondary melting by electroslag (ESR) or vacuum arc remelting (VAR). Its scope applies to the forging product specifications it lists, and when a product specification conflicts with A788, the product specification prevails. Certification must state the number and year date of both A788 and the product specification. [4]
Editorial note: the 12 t Cr-Mo ingot in the Metals study followed an electric arc furnace, ladle furnace and vacuum degassing route, which fits the A788 primary-melting-plus-degassing wording; state the product specification and its year in the ingot enquiry so the heat records can support the forging certificate. [1][4]
Product specification listed in A788 scope
Title wording
What to tell the ingot maker
A469/A469M
Vacuum-Treated Steel Forgings for Generator Rotors [4]
Vacuum treatment required by the title.
A470/A470M
Vacuum-Treated Carbon and Alloy Steel Forgings for Turbine Rotors and Shafts [4]
Vacuum treatment; compare with the P and S targets in US 3,907,547. [3]
A508/A508M
Quenched and Tempered Vacuum-Treated Carbon and Alloy Steel Forgings for Pressure Vessels [4]
Vacuum treatment; heat records for certification.
A668/A668M
Steel Forgings, Carbon and Alloy, for General Industrial Use [4]
Grade and class of the forging.
04
Melting route, bottom-pour runner, mould, hot top and discard
Carbon, manganese, sulphur and phosphorus limits and ingot weight for a forging ingot
Chemistry rows carry the published values: 0.32% C and 0.57% Mn in the 12 t Cr-Mo heat studied, and sulphur and phosphorus each held below 0.010% in the rotor-ingot patent. Strength and hardness rows are set on the forging after heat treatment, not on the ingot. [1][3]
Field
What it means and published values
Ask the supplier for
Carbon Content (%)
E.g. 0.32% in one Cr-Mo heat; 0.10–1% in the patent. [1][3]
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Tongyu Heavy Industry Co., Ltd.
Manufacturing site to be confirmed for the order
Its website lists steel ingots, including double-vacuum and high-grade alloy steel ingots.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How are heavy forging ingots made?
In the published 12 t case: EAF melting, ladle refining, vacuum degassing, then bottom teeming at 1580°C into a cast iron mould with an insulated hot top. [1]
Why does the hot top matter?
It feeds the ingot and controls top heat flow; a taller or better insulated hot top reduced macrosegregation in two MDPI studies. [1][2]
What P and S limits apply to rotor forging ingots?
US 3,907,547 targets phosphorus and sulfur each below 0.010 wt.% for heavy rotor and turbine shaft ingots. [3]
Which melting routes does ASTM A788 allow for forging steel?
Electric-furnace, basic oxygen, vacuum-induction or open-hearth primary melting, optionally with degassing or refining and secondary ESR or VAR remelting. [4]
Sources and what still needs a direct check
Sources checked 2026-10-11. Two open-access peer-reviewed papers (2022, 2024) report one ingot type studied with an industrial producer; the US patent describes its own steelmaking process; ASTM A788 is read from its published abstract and scope only.