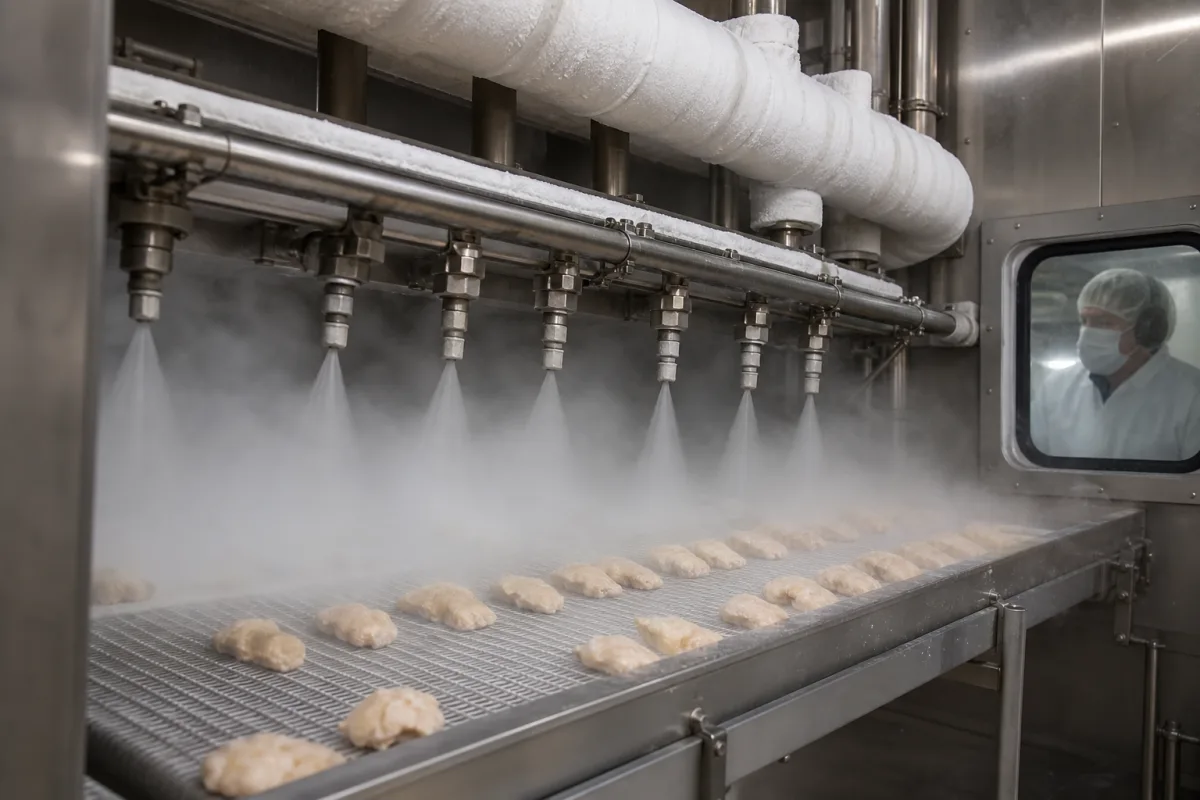
Liquid-nitrogen spray header and nozzle system for food freezers: nozzle pressure, flash-gas venting and on/off bank control
The liquid-nitrogen spray bar inside a food freezer · nozzle pressure that peaked near 2 bar gauge in Air Products tests, flash gas venting from the header, and banks of nozzles switched on and off instead of throttled
In a cryogenic freezer, the spray system is the part that decides whether the liquid nitrogen arrives on the product as liquid. Three things go wrong with it: the nozzles are run at a pressure where they transfer little heat, nitrogen that has flashed to gas in the supply line reaches the nozzles in slugs, and a single throttling valve drags every nozzle away from its best pressure as the load changes. The patents below come from freezer builders that tackled each of these.
The liquid-nitrogen delivery and spray assembly fitted inside a food freezer: supply valves, the spray header or manifold, gas relief or phase-separation at the header, the nozzles and how they are grouped and switched. Whole continuous freezing tunnels for fish and seafood, with their capacity, belt width, tunnel length, cryogen use per kilogram, oxygen safety and hygienic design, are covered on the Cryogenic tunnel freezers for fish and seafood page; bulk cryogen storage tanks and transfer lines up to the freezer are not covered here. Air-atomizing spray guns for tablet coating (Tablet coating spray system page), gas delivery control panels (Gas panel page) and press hydraulic pressure control (Hydraulic pressure control system for presses page) are different products despite shared terms such as manifold, valve and pressure.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Why the nozzles should see about 2 bar gauge, not the under-1-bar left after a throttling valve
Jeremy Miller of Air Products measured the heat transfer coefficient between liquid nitrogen leaving a Delavan ACM 10 nozzle, used in some of the company's conventional tunnel freezers, and a sheet of material beneath it, against the pressure just upstream of the nozzle. [1]
The patent also found that a nozzle's effectiveness, the share of the cryogen's available refrigeration that reaches the product, peaks at a slightly different pressure from its heat transfer coefficient, and recommends operating between the two; for rapid cooling it gives a preferred pressure at which the nozzle reaches at least 50 %, better 75 % and better still 90 % of its maximum heat transfer coefficient. Its tests indicated that nozzles with a swirling device upstream of the orifice may be preferable to plain ones. [1]
Editorial note: each nozzle model in those tests had its own curve, so the operating pressure belongs to the nozzle chosen, not to the freezer; ask the supplier for the curve of the nozzle it fits.
Pressure upstream of the nozzle (bar gauge)
What the patent reports
0 to 1
Range a continuously throttled freezer works in after cooldown, with 0 to 1.4 × 10⁻² l/s per nozzle; heat transfer described as extremely poor. [1]
0.5 to 0.9
Heat transfer coefficient rises only marginally. [1]
Range in which tests on commercially available nozzles found the optimum. [1]
Ask for the nozzle model, its tested pressure for peak heat transfer, the supply pressure at the header inlet, and the pressure drop between supply and nozzle.
02
Flash gas in the supply line: slug flow at the nozzles and a header that vents its own vapour
Air Products' phase-separator patent explains that warming and pressure drop in transfer lines and control valves turn a substantial volume of the liquid nitrogen into vapour before it reaches the spray header. The two-phase mixture then arrives as small slugs of liquid between large slugs of gas, so the product is sprayed alternately with liquid and gas. Liquid nitrogen, the patent notes, has about twice the available refrigeration of the gas, so the frozen product's temperature varies. [2]
Formax's 1979 freezing-tunnel patent addressed this inside the header itself: large-diameter tubes carry liquid spray nozzles along the bottom, and optionally the sides, with one or more gas relief nozzles on top, so the header acts as a phase separator and the liquid leaves evenly from below. [3] Air Products later pointed out that a relief nozzle of fixed diameter lets out only a fixed amount of gas per unit time, which would have to be resized whenever the flow rate or the share of flashed cryogen changed. [2]
Its answer was a temperature-actuated valve on the header: a PTFE stem that contracts more than its housing, closing a UHMW polyethylene seat when liquid at about -192 °C fills it and cracking open as gas warms it. In the example the vent was sized for 54.6 kg/h of nitrogen gas at 7 psig, the gas produced when 1,135 kg/h of liquid nitrogen is expanded from 25 psig to 7 psig. With storage at 37 psig, the spray header then held 6 ± 1/4 psig and the temperature next to the nozzle outlets read -193 °C. [2] Editorial calculation: 54.6 ÷ 1,135 ≈ 4.8 % of the liquid flow flashing to gas over that pressure drop.
Ask how the header separates gas from liquid (relief nozzles, a separator valve or a separate vessel) and what flash-gas flow it is sized for at your supply pressure.
03
Solenoid banks at constant pressure against spring-loaded nozzles on a modulating valve
The two patents take opposite routes to matching nitrogen flow to a changing heat load.
Lewis Tyree's 1982 patent keeps a single modulating pressure-reducing valve and makes the nozzles follow it: each injection device is spring-biased closed and, with nitrogen, can be set to close at about 30 psia, opening its orifice wider as pressure rises. In one arrangement one array opens at about 40 psia and the other at 30 psia, so an intermediate pressure sprays from only one array and lengthens the pre-cooling zone. For a tunnel about 40 inches wide, each group might carry five devices facing upstream on one header and five facing downstream on another, with inducers around the devices that draw in surrounding vapour, though some may be fitted without one. Depending on pressure and flow, the patent says, the nitrogen may all vaporise at the nozzle or leave as a mist of small drops. [4]
Air Products' patent cites Tyree's continuously varied flow as the approach it replaces. [1] It supplies all banks from a source held at 2.2 bar gauge, so every nozzle in use runs near 2 bar, and meets the load by switching solenoid valves: in the example, two banks of three nozzles and a third bank of six. The small first bank trims the load by cycling, for instance five seconds of flow in every thirty at low load and fifteen in every twenty at normal load; the second and third banks stay on or off for long periods, and the first opens again when the tunnel sensor is 5 °C above set point. [1] Editorial calculation: those duty cycles are 17 % and 75 % open.
Whichever route is used, the spray bar works with the tunnel's fans and exhaust. In Tyree's design a vent blower near the entrance draws off about 90 % of the vapour so that about 10 % leaves at the exit, which keeps humid room air from entering. [4] Air Products notes that gas passing through the nozzles at a lower mass flow than liquid lets room air in at the discharge opening, adding frost and heat load. [2]
State whether the freezer meters nitrogen by a modulating valve or by switched nozzle banks, how many banks and nozzles each has, and which valve cycles to trim the load.
04
Data to give a supplier of a liquid-nitrogen spray system
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Freezer: [type; width; product and line rate; set temperature]
Supply: [storage pressure; pressure available at the header inlet; transfer line length and insulation]
Nozzles: [model; number; spacing; pressure for peak heat transfer; swirl insert or plain orifice]
Header: [tube size; gas relief or phase separator; flash-gas flow it is sized for]
Control: [modulating valve or switched banks; banks and nozzles per bank; valve type and cycle rate]
Materials: [header, nozzle and seal materials rated for -196 °C]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
At what pressure should liquid-nitrogen spray nozzles run?
In Air Products' tests the heat transfer of a Delavan ACM 10 nozzle peaked at about 2 bar gauge and fell off by 2.3 bar; across the commercially available nozzles tested the optimum lay between 2 and 4 bar gauge, against under 1 bar in throttled freezers. [1]
Why does a spray header need to vent gas?
Liquid nitrogen partly flashes to gas in the supply line and reaches the header in slugs, so product is sprayed alternately with liquid and gas; relief nozzles or a separator valve let the gas out so liquid flows evenly from the nozzles. [2][3]
How much nitrogen flashes to gas before the nozzles?
In one Air Products example, 1,135 kg/h of liquid expanded from 25 to 7 psig produced 54.6 kg/h of gas, about 4.8 % by an editorial calculation. [2]
Can nozzles be switched instead of throttled?
Yes; one Air Products design feeds banks of nozzles from a 2.2 bar gauge source and switches them with solenoid valves so each runs near its best pressure. [1]
Sources and what still needs a direct check
Sources checked 2026-10-12. All four sources are patents from freezer builders or their inventors: Air Products (nozzle pressure tests, bank switching and a header phase-separator valve), Formax (a spray header that vents its own gas) and Lewis Tyree, whose patent was later assigned to Liquid Carbonic (spring-loaded nozzles on a modulating valve). Patent examples describe the inventors' test equipment, not a guaranteed product rating.