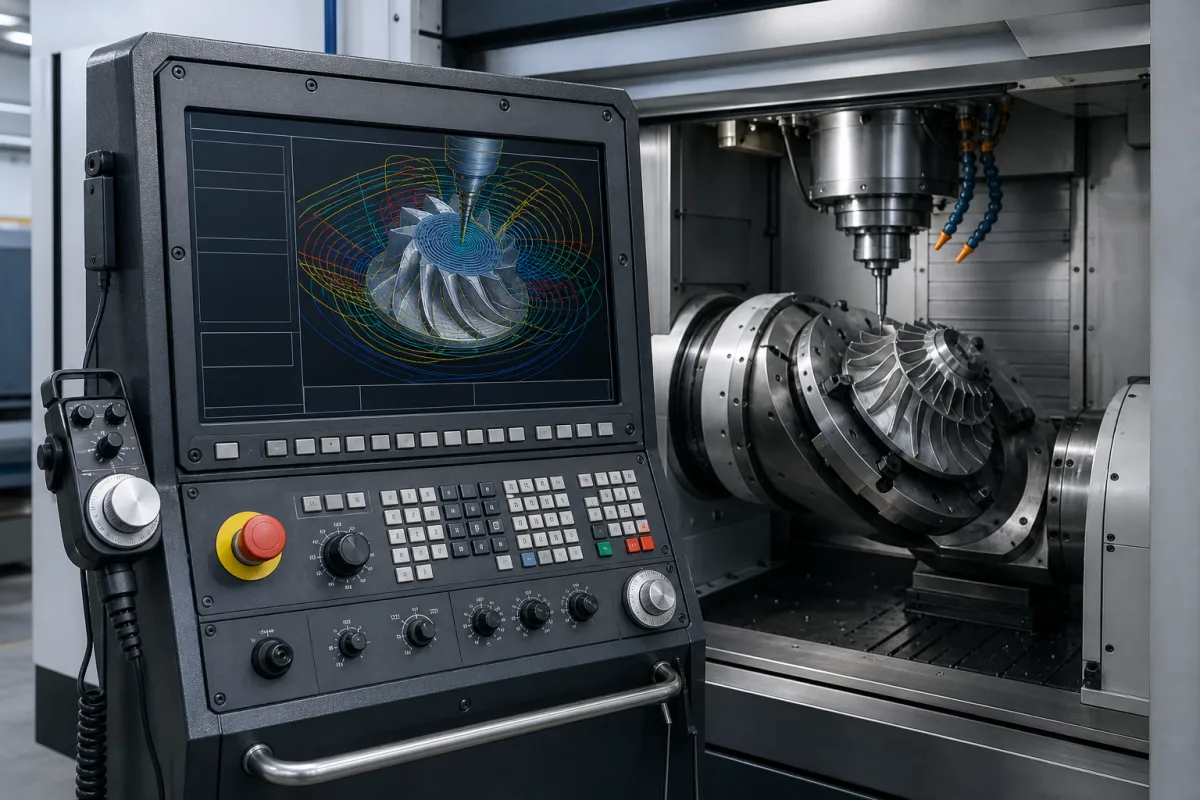
5-axis CNC controller: simultaneous five-axis control with RTCP and machine kinematics
Five-axis simultaneous CNC control · RTCP and kinematic transformation for table-tilting and head-tilting machines, rotary-axis offsets, inclined-plane machining, channels and bus axes
This page covers CNC controllers for five-axis simultaneous machining: they take tool tip position and orientation from the CAM system and, through a kinematic model of the machine, move three linear and two rotary axes together in coordinated moves. Ask three things first: which machine configurations the RTCP kinematics support and how rotary-axis offsets are calibrated, how many axes, channels and spindles the controller runs, and how inclined-plane and simulation functions are provided.
CNC controllers and controller kits for five-axis simultaneous milling and machining centres, including RTCP, kinematic transformation and inclined-plane functions. CNC controls for milling machines, machining centres and lathes as a whole are covered on the CNC controller page. CAM software, standalone motion cards and servo drives sold alone are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
LinuxCNC's documentation explains that coordinated multi-axis machines need a kinematics component for each machine type: a five-axis milling machine has three linear and two rotary axes that set tool orientation, the CAM system supplies cutter location data as tool tip position and orientation vectors, and the controller computes forward and inverse transformations between work and joint coordinates. In table rotary/tilting (trt) machines, a rotary table about Z (C) sits on a tilting table about X or Y (A or B); LinuxCNC develops transformations for xyzac-trt machines with and without rotary-axis offsets and for xyzbc-trt machines with offsets Dx and Dz, where the tilting and rotary axes do not intersect at one pivot point. [2]
LinuxCNC defines A, B and C as rotations about lines parallel to X, Y and Z, and notes that its own kinematics components rotate opposite to that convention, so direction conventions must be checked when posts are moved between controls. [3][2]
Huazhong states that the HNC-848Di's RTCP function supports up to three linear plus four rotary axes and covers 21 five-axis machine tool types, with two programming methods, and lists five-axis auto calibration among its features. [1] Editorial note: ask the supplier to name the configuration (for example head-head, head-table or table-table) its kinematic model uses for your machine and how the rotary-axis offsets are measured and stored.
Give the supplier the machine configuration and rotary-axis layout, axis strokes and rotary ranges, spindle data, drive bus and motors, required functions (RTCP, inclined plane, simulation), and the CAM system and post-processor you use.
02
Axes per channel, drive bus and inclined-plane programming
Huazhong lists the HNC-848Di at 5–32 axes over NCUC or EtherCAT, a 17-inch 1280 × 1024 touch screen, an on-board i7-5550U dual-core 2.0 GHz CPU, 8 GB memory expandable to 16 GB, a 128 GB SSD and two LAN ports, with external PLC and I/O modules and optional dual-channel control. Its specification table gives the HNC-848DM up to 9 simultaneously controlled axes in a channel, 32 feed axes, 4 spindles per channel, 1 standard and 10 maximum channels and up to 4,096 inputs and 4,096 outputs, with gantry axis synchronisation standard. [1]
For inclined surfaces, Huazhong describes establishing a tool coordinate system on the inclined surface and programming in it, and offers 3D simulation of the NC program before machining and real-time graphical simulation during machining. [1]
Editorial calculation: RTCP over 3 linear and 4 rotary axes is 7 kinematic axes; a five-axis machine uses 5 of them in one channel, inside the 9 simultaneously controlled axes per channel listed for the HNC-848DM. [1]
03
Compare machine configurations the kinematics must cover
Configurations below are those LinuxCNC develops in its documentation.
Axis count, resolution and RTCP calibration values to state in the controller order
Of these values, only the axis and channel counts are published for the controller itself; accuracy and repeatability belong to the finished machine, and with RTCP active the tool tip position also depends on how well the rotary-axis offsets were measured. [1][2]
Field
Published value or dependency
Ask the supplier for
Number of Controlled Axes (axes)
5–32 axes; 9 simultaneous per channel; up to 10 channels (HNC-848DM). [1]
Axes, spindles and channels for your machine.
Positioning Accuracy (mm)
Machine property; RTCP results depend on calibrated rotary-axis offsets. [2]
Offset calibration method and probe.
Repeatability (mm)
Machine property.
Value measured on the finished machine.
Control Resolution (mm)
Command resolution of the NC kernel.
Linear and rotary resolution.
Spindle Speed Range (rpm)
Set by the spindle and its drive; up to 4 spindles per channel (HNC-848DM). [1]
Spindle interface and drive.
Rapid Traverse Rate (m/min)
Set by the machine's feed drives.
Rates supported on the bus.
05
Send the machine, kinematics and functions together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
HuazhongCNC
Manufacturing site to be confirmed for the order
Lists the HNC-848Di closed-loop five-axis CNC controller kit with RTCP, five-axis auto calibration and 5–32 axes.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Which machines can a five-axis controller's RTCP cover?
Huazhong states that the HNC-848Di's RTCP supports up to 3 linear plus 4 rotary axes and covers 21 five-axis machine tool types, with two programming methods. [1]
Why does the controller need to know rotary-axis offsets?
Where tilting and rotary axes do not meet at one pivot point, the kinematic transformations include offsets such as Dx, Dy and Dz, as LinuxCNC's five-axis documentation shows. [2]
How many axes can a five-axis CNC controller run?
Huazhong lists 5–32 axes for the HNC-848Di, with up to 9 simultaneously controlled axes per channel and up to 10 channels on the HNC-848DM. [1]
Sources and what still needs a direct check
Sources checked 2026-10-12. Huazhong describes its own controller; the LinuxCNC documentation describes five-axis kinematics as implemented in that open-source control.