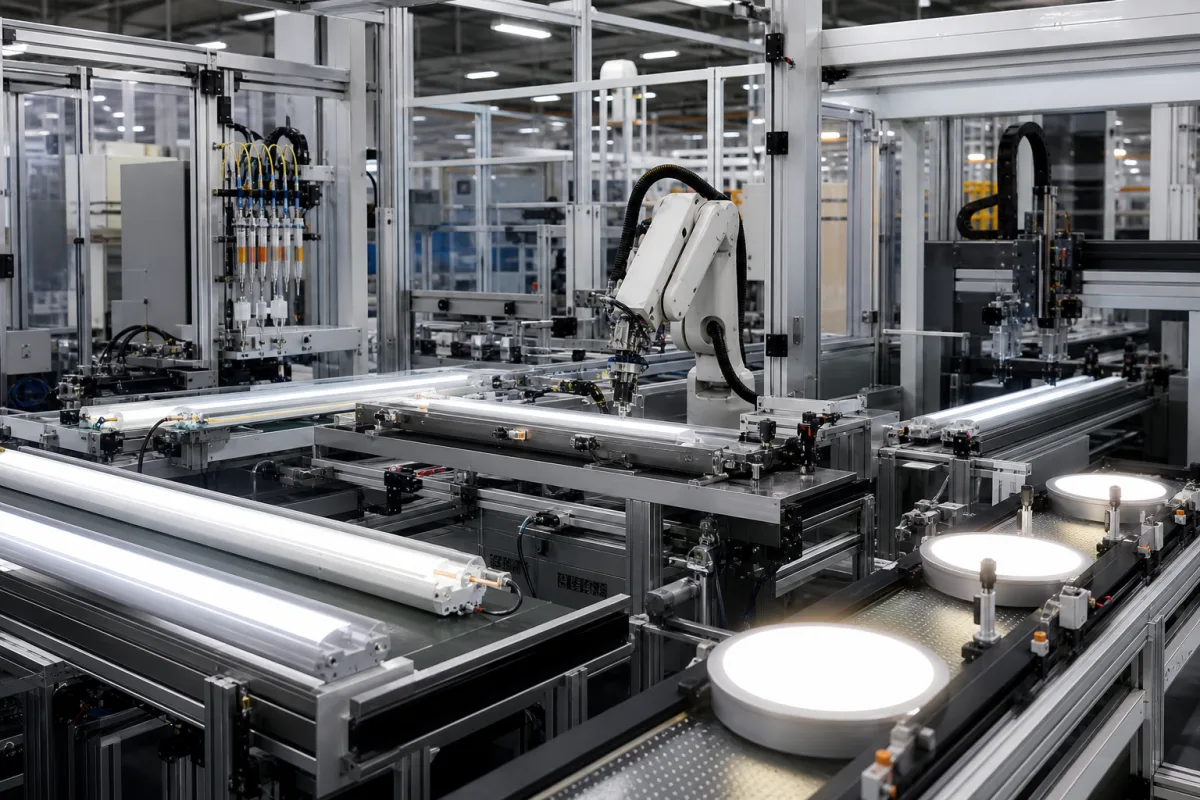
Automated LED luminaire assembly and end-of-line test line: gasket dispensing, lit check and hipot on complete linear and round fittings
Final assembly of complete LED fittings · foam gasket dispensed into the housing groove, driver wired in, then a lit check and an electrical safety test on every unit
The LED module is a bought-in part by the time a luminaire reaches this line. What the line adds is the enclosure and the wiring around it: a gasket laid into the housing groove, a driver connected to the mains terminal and to the module, a cover or diffuser closed over both, and labels. Two stations decide whether a finished fitting can ship. One is the gasket dispenser, because its material sets how long a housing must wait before the cover can be closed. The other is the end-of-line electrical test, because a high voltage applied the wrong way can pass the fitting and still damage the driver inside it.
Lines that assemble and test complete LED luminaires: linear and damp-proof fittings, round ceiling and downlight fittings and similar housings, with gasket dispensing or potting, driver and module wiring, cover closing, a lit operating check and production electrical safety tests. LED modules and light engines themselves (boards, packages, optics and heatsinks) are covered on the LED light module page; LED lights for machine vision on the LED lighting system for machine vision page; reflector cup sub-assemblies on the Precision reflector assembly page. Built-in drivers on the Built-in LED driver module page, appliance lines such as the Automated dishwasher production line page, LED package production and photometric type testing in a laboratory are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Foam gasket in the housing groove: pot life, tack-free time and how long a housing waits for its cover
In a damp-proof linear luminaire the transparent cover is pressed onto a soft foam gasket that a mixing head lays into the housing groove while the material is still liquid; the foam rises in the groove and cures at room temperature. [1] Henkel's Sonderhoff brochure gives the reaction times of the materials it sells for this job.
Editorial calculation: if one housing leaves the dispenser every 30 s (an assumed rate, not a published one), housings sealed with the 8 min indoor foam need 8 × 60 / 30 = 16 places on a buffer conveyor before the cover-closing station, against 7 places for the 3.5 min outdoor foam. [1] The table in the brochure lists the times without the temperature at which they were measured, so ask for them at the hall temperature of the line.
Sonderhoff's reference cell for linear luminaires pairs a DM 502 mixing and dosing unit with a three-axis linear robot and a shuttle table carrying two pick-up plates used alternately, so one housing is loaded while the other is foamed; the mixing head follows the groove and closes the bead with a dosing loop at the joint. [1] For plastics such as PP or PE the brochure names CNC-guided plasma activation of the groove to improve adhesion, and the material table lists plasma, corona or primer pre-treatment. [1] It states protection up to IP 68 with its outdoor polyurethane foam and up to IP 69K or NEMA 4-6p with its silicone foam on street-light housings, for the whole construction of housing, cover and seal. [1]
Send the groove section, housing material, cover clamping force and target IP rating; ask for the gasket's tack-free time at your hall temperature and the number of buffer places this sets before cover closing.
02
Hipot, insulation resistance and earth continuity on a finished fitting without damaging the driver
The production tests in the informative Annex I of the 2018 CSA C22.2 No. 250.0 / UL 1598 luminaire standard show what the electrical station has to do and where it may depart from a plain AC hipot. [2]
The annex allows solid-state components that are not relied on to reduce the risk of electric shock, and that the test voltage could damage, to be disconnected, and the circuit to be rearranged so that the dielectric stress stays representative. [2] Fulham, a maker of LED drivers, advised in a 2016 notice against applying AC hipot to LED products because it may damage or degrade the unit, and pointed users to the DC exceptions in UL's factory follow-up inspection instructions where the test is required. [4]
In Europe the routine tests that certification bodies under the ENEC scheme expect on 100% of EN 60598 luminaires are a visual and completeness check against a product checklist, an operating check with the intended lamps or a circuit that gives equal assurance, the electric strength or insulation resistance test, and earth continuity for class I luminaires, with the minimum values taken from Table Q.1 of EN 60598-1 Annex Q. [3] Editorial note: earth continuity is therefore a per-unit test for a class I fitting certified under ENEC, while the UL 1598 annex sets a per-run or per-quarter frequency; a line building for both markets has to run it at the stricter frequency. [3][2]
Check
Condition in UL 1598 (2018) Annex I
How often
Dielectric voltage-withstand
1200 V ac for 1 s between primary wiring and accessible metal parts that can become energized, and between primary wiring and accessible live parts of an isolating-transformer secondary rated at no more than 30 V rms or 42.4 V peak [2]
100% of production where conductors are hidden after assembly or enclosed more than 38 mm in a stem, arm, tubing or unlisted conduit [2]
Insulation resistance (alternative)
500 V dc for at least 1 s, at least 2 MΩ, with the luminaire disconnected from the supply [2]
100%, accepted as representative of the dielectric test [2]
Grounding continuity
Not more than 0.10 Ω from the grounding connection to accessible metal parts [2]
At least once per production run per design for temperature-test-exempt luminaires; at least once per quarter per design for others [2]
One sample per design at least once per quarter [2]
Ask which test the electrical station runs (AC withstand, DC withstand or DC insulation resistance), at what voltage and dwell, with which parts disconnected, and whether the driver maker has approved that test for its product.
03
Yearly verification tests and test records kept outside the line
Some checks are done on samples away from the line, so the line has to keep a record that ties each shipped fitting to them.
Editorial note: because the IP test on sample fittings follows any IK impact test, a gasket that passes when new may still be challenged after impact; keep gasket batch and dispense parameters in the same record as the sample's IP result.
Item
Published requirement
ENEC product verification tests
At least once a year: endurance test under Clause 12.3 for each range of luminaires (applicable to luminaires with an IP class of 20 or above), enclosure protection, screws and nuts, protection against electric shock with creepage and clearance, and photobiological blue-light assessment for LED luminaires not classified RG0 or within unlimited RG1 [3]
Order of IP and IK tests
If the luminaire carries an IK rating under ENEC, the IP test is done after the IK tests [3]
UL 1598 Annex I records
Kept at least 6 months, with test quantity, dates, catalogue or model numbers, results and disposition of non-complying products [2]
04
What to send when asking for a luminaire assembly line
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Fittings: [linear / damp-proof / round ceiling / downlight; lengths or diameters; housing material]
Rate: [fittings per hour; shifts; changeover between lengths]
Sealing: [gasket or potting; groove section; IP and IK target; hall temperature]
Wiring: [driver type; terminal; class I or class II]
Test: [lit check; AC or DC withstand or insulation resistance; voltage and dwell; earth continuity per unit or per run; ENEC and/or UL markets]
Records: [per-unit serial, test result, retention period]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How long must a foam-gasketed luminaire housing wait before the cover goes on?
Sonderhoff lists tack-free times of 8 min, 3.5 min and 5 min for its indoor, outdoor and Ex luminaire gasket foams; the wait depends on the material and the hall temperature. [1]
Can the end-of-line hipot damage an LED driver?
Fulham advised against AC hipot on LED products for that reason; UL 1598 Annex I lets parts at risk be disconnected and accepts a 500 V dc insulation resistance test of at least 2 MΩ as an alternative. [4][2]
Is earth continuity tested on every luminaire?
For class I luminaires under ENEC it is one of the 100% routine tests; the 2018 UL 1598 annex sets it per production run or per quarter, with a 0.10 Ω limit. [3][2]
Sources and what still needs a direct check
Sources checked 2026-10-12. The gasket figures come from the gasket maker's own brochure; the test requirements from the 2018 bi-national luminaire standard published as a public-safety copy and from the ENEC routine-test annex; the hipot warning from a driver maker's notice.