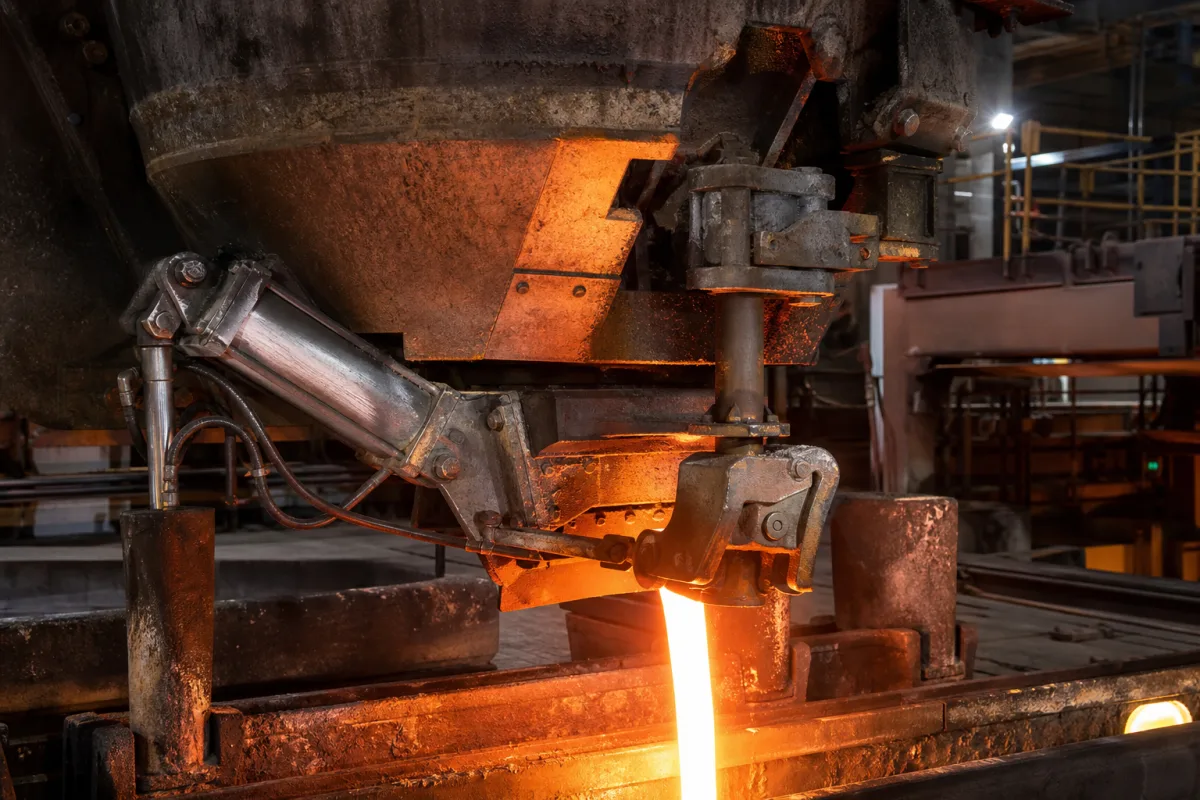
Slide gate flow control for molten steel ladles and tundishes
Molten steel flow control · ladle and tundish slide gates, hydraulic drive, well filler sand, refractory plates and cost per ton
A slide gate is a refractory valve under the nozzle of a steel ladle or tundish: refractory plates with bore holes, clamped in a steel mechanism, slide across each other under a hydraulic cylinder so that the holes line up to open, partly overlap to throttle, or close to stop the stream. Ask three things first: how the gate will open freely at the start of each heat, what refractory plates and nozzles it uses and how often they are changed, and what it costs per ton of steel cast.
Slide gate (sliding gate) systems for steel ladles and tundishes: the gate mechanism, hydraulic drive, refractory slide plates and nozzles, and the well filler sand that keeps the nozzle open. Process control valves for liquids and gases in pipelines are covered on the Pneumatic globe control valve page. Stopper rods, electromagnetic flow control and the ladle itself are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
Before tapping, the ladle nozzle above the slide gate is filled with stuffing (well filler) sand that isolates the liquid steel from the gate; when the gate opens, the sand should run out and let the steel follow. In a 2025 study published in Materials, the authors report about 70 kg of sand per 220 t ladle, and that the conventional chromite (Cr2O3-based) sand is used for its low cost and high self-opening rate. [1]
The same study found the chromite sand, about 76% Cr2O3, SiO2 and FeO, reoxidized interstitial-free steel: thermodynamic calculation put the aluminium loss at up to 92 ppm for 70 kg of sand in 220 t of steel. A new alumina-based sand (over 80% Al2O3) had a refractoriness of 1,740 °C against 1,610 °C for the chromite sand, gave a 100% self-opening rate over 100 industrial heats, and lowered total oxygen in the tundish from 30.1 to 19.5 ppm, with aluminium and titanium losses down 41.3% and 24.2%. [1]
Editorial calculation: 70 kg of sand in a 220 t heat is 70 ÷ 220,000 ≈ 0.032% of the steel weight, small by mass but in direct contact with the first steel to pass the gate.
Give the supplier the vessel (ladle or tundish), steel capacity, steel grades, nozzle bore, number of plates, drive (hydraulic stroke and force), plate and nozzle refractory, filler sand used, sequence length, and how the plates are changed.
02
Count capital and refractory cost per ton
A report to the US Department of Energy by Concept Engineering Group lists a tundish slide gate and level-control system as the slide gate, hydraulic cylinders, hoses, control valves, pumps, motors, reservoirs, racks, mounting plates, tools, tube changers, argon units, process sensors and computer interfaces. It gives costs of about $100,000 per strand for a billet caster slide gate and $175,000 to $250,000 per strand for a bloom or slab machine, against about $50,000 per strand for a stopper rod system. [2]
The report puts operating cost at about $1 per ton for a stopper rod system and up to $4 to $5 per ton for a slide gate system, much of it for refractory replacement. [2] Editorial calculation: at $4.50 per ton, a strand casting 500,000 t a year would spend about $2.25 million a year; these are 2004 US figures and should be used only to compare options, not as prices.
The same report cites Inland Steel's 1991 finding that a slide gate creates recirculation loops in the submerged entry nozzle below it, through its sharp geometry change, worsening alumina clogging with aluminium-killed steels. [2] Editorial note: ask the supplier for argon injection options and the clogging record on grades like yours.
03
Match the gate to the shroud below it
Below a ladle gate the stream runs through a ladle shroud into the tundish. In a 2026 physical and numerical study of a two-strand slab tundish, a standard shroud was a straight pipe of 0.09 m internal diameter, with inlet velocities of 1.35 m/s at 1.0 m/min casting speed and 2.16 m/s at 1.6 m/min. [3]
The study's alternative umbrella-type shroud reduced shear stress on the tundish walls and bottom in the pouring zone from 26–63 Pa to 1.5–5.1 Pa and dynamic pressure from 5,235 Pa to 252 Pa at 1.6 m/min. [3] Editorial note: confirm the collector nozzle and shroud connection, and the shroud manipulator, with the gate supplier.
04
Gate model, plate count, stroke, refractory life and references to request
Ask each supplier for the gate model, plate count and stroke, hydraulic unit, plate and nozzle refractory and their life in heats, and references on comparable vessels.
05
Well block, filler sand, slide plates, gate mechanism, hydraulics, shroud and argon
Bore, stroke time, plate refractory and hydraulic pressure for a ladle or tundish slide gate
A valve-style flow coefficient does not apply to molten steel: throughput is set by bore, ferrostatic head and plate opening, so ask for throughput at full open for your bore.
Field
What it means and published values
Ask the supplier for
Nominal Diameter (mm)
Nozzle and plate bore; one shroud studied at 90 mm ID. [3]
Bore of each refractory.
Operating Pressure (MPa)
Hydraulic pressure of the drive.
Pressure and cylinder force.
Operating Temperature (°C)
Molten steel; sand refractoriness 1,610–1,740 °C reported. [1]
Refractory limits.
Flow Coefficient (Cv) (US gal/min)
Not used for molten steel; flow set by bore, head and opening.
Throughput at full open.
Leakage Rate (% of rated flow)
Steel or air leakage between plates.
Sealing and argon practice.
Actuation Time (s)
Time to open or close.
Stroke time.
Control Accuracy (% of span)
Plate position control for level.
Position sensor and resolution.
Supply Voltage (V DC)
Valves and sensors.
Voltage.
Enclosure Rating
Hydraulic and electrical parts near heat.
Rating and heat shielding.
Body Material
Gate frame.
Material.
Seat Material
Slide plate refractory.
Grade and life in heats.
Weight (kg)
Mechanism for handling.
Weight.
07
Send the vessel, steel and refractory data together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What does the well filler sand do?
It fills the ladle nozzle above the slide gate and isolates the steel from the gate so the gate can open freely; a 2025 study reports about 70 kg per 220 t ladle. [1]
Can the filler sand affect steel cleanliness?
Yes; the study found chromite sand reoxidized IF steel, and an alumina-based sand cut tundish total oxygen from 30.1 to 19.5 ppm with 100% self-opening over 100 heats. [1]
How does slide gate cost compare with a stopper rod?
A 2004 DOE-funded report gives about $1 per ton operating cost for stopper rods and up to $4–5 per ton for slide gates, much of it for refractory replacement. [2]
Sources and what still needs a direct check
Sources checked 2026-10-12. The filler sand and ladle shroud studies are peer-reviewed articles in Materials (MDPI); the cost figures come from a 2004 final report by Concept Engineering Group to the US Department of Energy, available from OSTI. Costs are historical US figures.