Continuous casting refractories · Nozzle clogging types and causes, argon and calcium practice, nozzle material and geometry, slide-gate signals
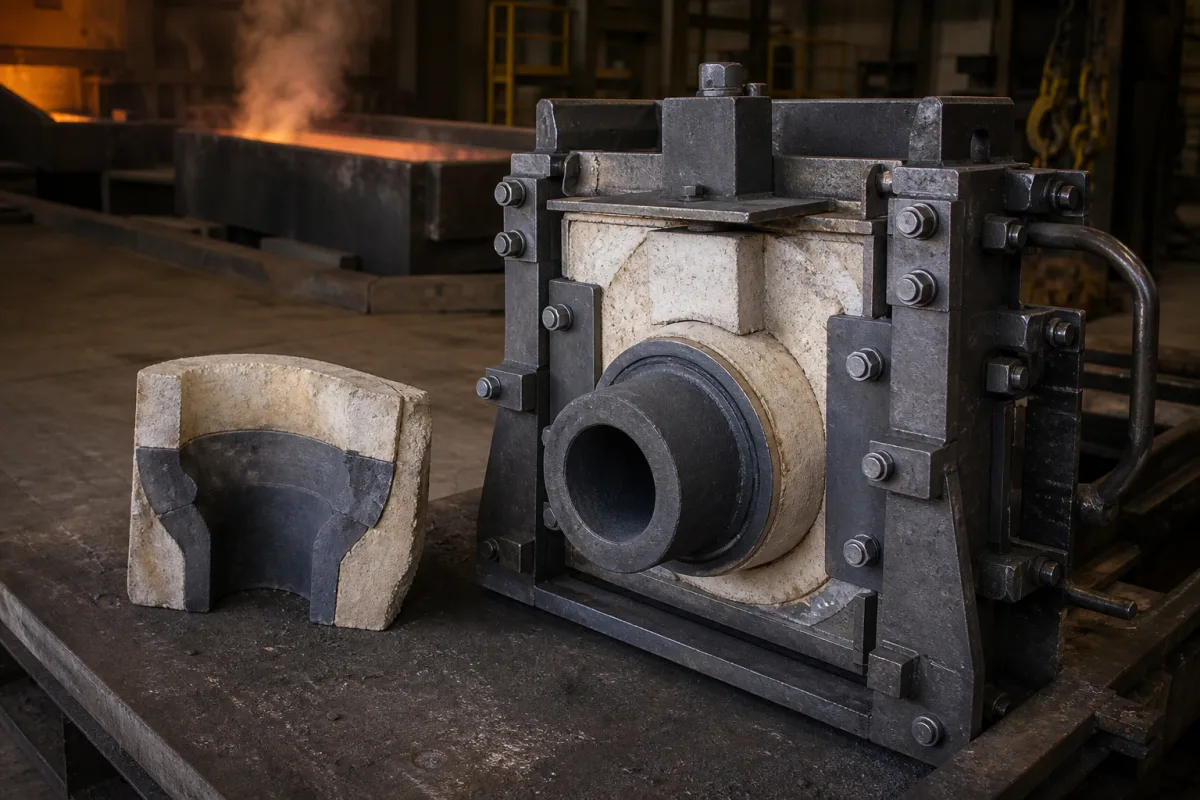
A molten metal flow control nozzle is the refractory channel that carries liquid steel from ladle or tundish towards the mould, working with a slide gate or stopper rod that sets the flow. Ask three things first: how the nozzle will resist clogging with your steel grades and deoxidation practice, which refractory, insert and argon arrangement the supplier proposes, and how bore erosion, joints and preheat will be managed over a sequence.
Refractory nozzles for steel continuous casting and teeming: ladle and tundish upper and lower nozzles, metering (sizing) nozzles, slide-gate nozzles and submerged entry nozzles. Slide-gate plates and mechanisms as stand-alone products, tundish linings, aluminium casting launders and spray nozzles are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Rackers and Thomas's 1995 review of nozzle clogging, presented at the 78th Steelmaking Conference, describes clogging as buildup in the flow passage between tundish and mould that cuts productivity, raises cost and harms quality. It cites one case where clogging cut a tundish's run from twelve heats to six, and notes that dislodged clog particles cause cleanliness defects in deep-drawn products that need oxides below 50 µm. [1]
The review classifies clogs as: sintered networks of deoxidation products such as alumina, reported as 1–20 µm particles; solid steel, especially at start of cast with low superheat or inadequate nozzle preheat; complex oxides such as mould flux drawn into submerged-entry-nozzle ports, or calcium aluminates and sulfides on calcium-treated heats; and reaction-product films from deoxidants reacting with air aspirated through porous refractory or joints, with oxygen from the cooler steel or with silica in the refractory. [1]
Its flow model shows that very little slide-gate travel is needed until a clog reaches a critical thickness, after which a small increase demands a large change in gate position, because turbulent pressure drop at fixed casting rate scales inversely with the fifth power of the bore radius. Slide-gate position is therefore a poor indicator of early clogging. [1] Editorial calculation: a clog 5 mm thick on each side of an 80 mm bore raises that pressure drop by (80/70)⁵ ≈ 1.95 times.
Give the supplier the caster type (billet, bloom or slab), steel grades and deoxidation practice, calcium treatment, casting speed and sequence length, flow control (slide gate or stopper), current nozzle materials, bore sizes and failure modes, argon practice, and preheat equipment.
02
Reduce clogging with practice, material and geometry
Rackers and Thomas report argon injected through the nozzle wall or stopper rod as an anti-clogging practice, at a rate of 5 L/min (STP), via porous refractory or machined or laser-cut holes. Suggested benefits include a gas film on the wall, flushing and flotation of deoxidation products, and higher pressure in the nozzle that reduces air aspiration; drawbacks include mould-level fluctuation and slag-line erosion, bubble entrapment, nozzle cracking, and the clog moving elsewhere. [1]
Calcium treatment can liquefy alumina inclusions: at 1550 °C, calcia–alumina mixtures with 40–60% alumina are liquid. But too little calcium forms CaO·6Al₂O₃ and increases clogging, calcium erodes refractories, and it fails in high-sulfur steels: for steel at 0.04% total aluminium, the review puts the sulfur needed below 0.007%. [1]
The review lists nozzle-side measures: calcia additions to the refractory, boron nitride and other coatings, oversize bores and replaceable submerged entry nozzles, better joint sealing and stronger holding steelwork against air aspiration, rounded and aligned nozzle entrances, a 5 mm internal step in the submerged entry nozzle, a wider bore below the stopper seat, flat-bottomed nozzles without a well, and insulation, preheat or heating around the clogging location. [1]
The Continuous Casting Consortium's flow modelling of bifurcated submerged entry nozzles found a recirculation zone at the top of oversize outlet ports, where steel flows back into the nozzle, making that region prone to clogging buildup. [2]
A bore liner is another material route. Vesuvius Crucible Company's US patent 5,370,370 A starts from a carbon-bonded alumina-graphite nozzle body (its example composition by weight is 32% C, 52% Al₂O₃, 14% SiO₂ and 2% other additions), glazes the outside with a frit up to about 5 mm thick (3 mm preferred), and fires it in an oxidising atmosphere at about 1,000 °C for about two hours so that the unglazed bore loses its carbon to a depth of about 2–3 mm. That porous, carbon-free zone is then infiltrated with a refractory slurry, preferably 50–65% by weight alumina powder of 0.1–1.0 µm average particle size, giving a bore surface that the patent states resists alumina buildup; it cites earlier CaO–MgO–Al₂O₃ liners that form low-melting eutectics at 1,350–1,600 °C and wash out as alumina deposits. [4] Editorial note: ask the supplier whether the bore of the offered nozzle is carbon-free, glazed or lined, and to what depth.
03
Submerged entry nozzles in brief
The submerged entry nozzle carries steel from the tundish into the mould below the meniscus. US patent 7,757,747 B2 describes one built in zones — alumina graphite for the body and zirconia graphite at the mould slag line — pressed isostatically at up to or above 4,000 psi. [3]
Submerged entry nozzles are covered in detail on the CNFX page “Submerged entry nozzle (SEN) for continuous casting”, including zone compositions, bore profile, slag-line erosion and port design; this page keeps to the nozzle system as a whole.
04
Ladle, tundish and metering nozzles on supplier lists
Listings include ladle and tundish upper and lower nozzles, metering or sizing nozzles, long nozzles (shrouds), submerged entry nozzles and slide-gate plates.
05
Nozzle train from well block to mould
Part
Role
Fix in the order
Upper (well) nozzle
Takes steel from ladle or tundish; entrance shape matters. [1]
Refractory and entrance profile.
Slide gate or stopper
Throttles flow; position reflects clogging only late. [1]
Bore and refractory data to put on a nozzle drawing
Check the bore rows first: Rackers and Thomas show pressure drop scaling with the fifth power of bore radius, so a 5 mm clog on each side of an 80 mm bore nearly doubles it. [1]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What causes nozzle clogging in continuous casting?
Rackers and Thomas classify clogs as deoxidation-product networks, solid steel, complex oxides and reaction-product films from air or refractory reactions. [1]
How much argon is injected to prevent clogging?
The 1995 review gives a rate of 5 L/min (STP), through porous refractory or drilled holes. [1]
Can slide-gate position show clogging?
Only late: little gate travel is needed until the clog reaches a critical thickness, because pressure drop scales with the fifth power of bore radius. [1]
Can the nozzle bore itself be made to resist alumina buildup?
Vesuvius' US 5,370,370 A oxidises the bore of an alumina-graphite nozzle to a carbon-free zone about 2–3 mm deep at about 1,000 °C and infiltrates it with fine alumina, which the patent states resists alumina buildup. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Rackers and Thomas's review (1995) and the Continuous Casting Consortium pages are academic research; practice has developed since, so confirm current materials and argon practice with suppliers and your own trials. The two US patents (US 7,757,747 B2 and Vesuvius' US 5,370,370 A) are primary design documents for specific nozzle constructions.