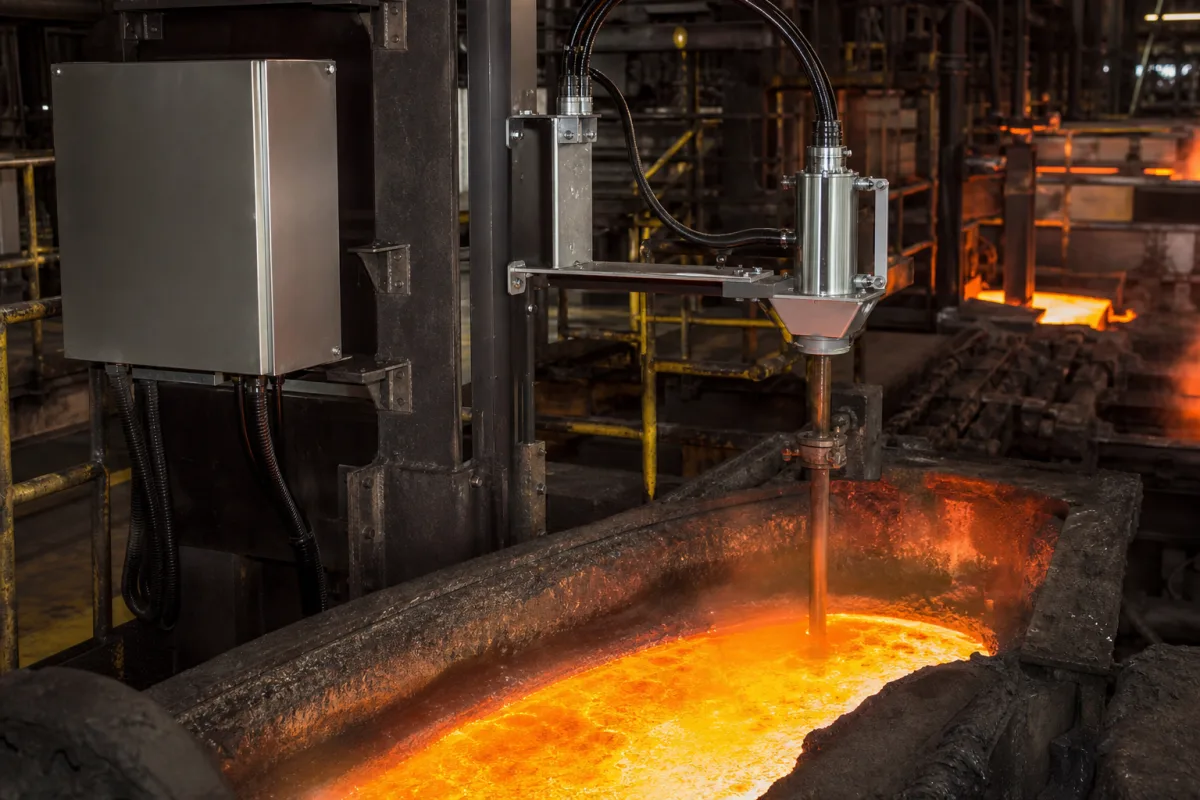
Molten metal (mould) level control for continuous casting · Radiometric, eddy-current and optical level measurement, measuring range, filter time constant and precision, Co-60 versus Cs-137 sources, casting powder and electromagnetic stirrer effects, stopper-rod or speed actuation
A molten metal level control system measures the height of liquid steel or other metal in a continuous casting mould, without contact, and drives a stopper rod, slide gate or the strand withdrawal speed so the level stays at its set point; the same loop also handles the automatic start of casting. Ask three things first: which measuring principle suits the mould format, casting powder and any electromagnetic stirrer or brake, what measuring range, precision and response time the casting speed demands, and how the controller connects to the actuator and the caster automation.
Mould level measurement and control systems for continuous casting of steel and other metals, including radiometric source-and-detector sets, eddy-current and optical sensors, evaluation units and level controllers driving stopper rods, slide gates or strand speed. Tundish weighing, furnace bath-level gauges, stopper-rod mechanisms sold alone and level sensors for cold liquids are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Berthold's white paper on mould level measurement explains that the level in a continuous casting mould must be kept at a metallurgical optimum: too high risks overflow or burning the sealing elements at the mould head, too low gives a shell thin enough to break out below the mould. Flow from the tundish varies as the ceramic outlet wears or builds up slag or alumina and as tundish level changes, so online level measurement drives an actuator — a stopper rod or slide valve on the tundish, or the strand withdrawal speed. It states that radiometric and electromagnetic technologies dominate the application and that more than six thousand strands use radiometry. [1]
A radiometric system has three main parts: a rod-shaped gamma source on one side of the mould, a scintillation detector on the other and an evaluation unit that converts the pulse rate into a level using a stored calibration curve; sources may be fitted outside the water jacket in a lockable shield (preferred for tubular billet moulds), inside the water jacket or frame (bloom and slab), or in a dip tube for retrofits. Detectors handle continuous operating temperatures of up to 70 °C and can be water-cooled from the mould water. Silicon photomultiplier (SiPM) detectors are virtually immune to electromagnetic fields, and the paper says moulds with electromagnetic stirrers or brakes call for them. [1]
Endress+Hauser's US patent 4,420,250 (1983) describes the radiometric arrangement of a Co-60 or Cs-137 rod source of about 100 mm with a scintillation counter, and lists its drawbacks as averaging times of about one second for spreads of up to 5% of range, a control range limited to the rod length so that casting start needed manual control, and gamma-radiation safety measures; it proposes instead an electro-optical range meter that sends light pulses vertically onto the bath and measures their travel time. [2]
Editorial note: radiometric gauges need a radioactive-source licence and radiation protection under national law; agree with the supplier who holds the licence, how sources are handled during mould changes and what dose rates apply at the mould cover.
Give the supplier the casting format and mould type (tube or plate), casting speeds including start-up, actuator (stopper rod, slide gate, speed), measuring principle preferred, required range, precision and response time, casting powder practice, electromagnetic stirrer or brake, mould oscillation frequency, cooling water available, radiation permit situation, interface to caster automation, and number of strands.
02
Set range, precision, filtering and source
The white paper gives measuring ranges of 100 to about 200 mm. Because radioactive decay is random, the level signal fluctuates statistically; precision improves with higher count rate (source activity or detector sensitivity), longer filter time constant and a higher set point. In its worked example for a small-section caster — 10,000 counts/s with an empty mould, a 0.8 s time constant, a 150 mm range and a set point of 112.5 mm — the standard deviation is 0.6 mm, giving ±1.2 mm for 95% and ±1.8 mm for 99.7% of the time; doubling the count rate to 20,000 counts/s reduces these to 0.4, 0.8 and 1.3 mm. [1]
With casting speeds of about 100 mm/s for small sections the full range is passed in 1–2 s at start-up, so time constants of 0.2–0.5 s are used then. The paper describes an RC filter that passes 63% of a step change in one time constant and about 95% in three, an output update about every 5 ms, and digital filtering of the mould-oscillation signal for formats below about 180 strokes per minute. It compares sources: Cs-137 at 660 keV needs up to five times the activity of Co-60 (1,173/1,332 keV), is more affected by casting powder and gives a non-linear calibration, with half-lives of 30.18 and 5.27 years and a designed source life of 10 (–15) years. [1]
Editorial calculation: with the paper's 0.8 s time constant, the signal shows about 95% of a sudden level change after 3 × 0.8 = 2.4 s; at the start-up rate of 100 mm/s, a 150 mm range fills in 1.5 s, which is why a shorter start-up time constant is needed. [1]
03
Ask where the sensor sits and which wave frequencies the loop sees
A Nippon Steel Technical Report (No. 89, 2004) describes the loop: a sensor monitors the mould level, a controller compares it with the target, and a cylinder adjusts the sliding nozzle. Disturbances come from nozzle clogging with non-metallic inclusions and from periodic fluctuation caused by strand bulging in the water-cooling zone. [4]
Its simulation used a 1,500 × 240 mm slab mould at 2.1 m/min, a −5 mm reference level, PI control and an imposed 10 s (0.10 Hz) bulging disturbance. A flow-analysis model showed extra ripple of about 0.70 Hz, close to the 0.71 Hz standing wave calculated for a 1,500 mm wide mould; a commercial caster chart showed roughly 1.00 Hz. Fluctuation was well controlled near the sensor but large on the opposite side, where no sensor was fitted. [4]
Editorial calculation: at 2.1 m/min (0.035 m/s) the 0.36 m² mould section withdraws about 0.0126 m³/s; a 10% inflow mismatch moves the level 0.1 × 0.035 = 0.0035 m/s, or 3.5 mm/s, beyond the ±1.2 mm precision quoted above within one second. Ask where the sensor sits relative to nozzle and narrow faces, and how the loop responds between 0.1 and 1 Hz. [4][1]
04
Tune the control loop against disturbances
A JFE Steel technical report (No. 26, 2021) describes mould level control on the six-strand round-billet No. 5 continuous caster at East Japan Works (Keihin): the level is detected by an eddy current sensor, a DCS calculates the discharge rate from the tundish, and commands go to a stepping cylinder driving the tundish stopper. Mould level fluctuation was the largest cause of billet scrap there, at 55%. [3]
The report gives two causes of fluctuation: dummy bar disturbances spread over a wide frequency band, and changes in the flow characteristic because the stopper and refractory wear or warp. It notes that slab casters controlled by a sliding nozzle show smaller system model changes. [3]
Item reported by JFE
Value or finding
Level sensor
Eddy current sensor
Actuator
Stepping cylinder on tundish stopper
Share of scrap caused by level fluctuation
55%
Manual gain re-tuning after model change
About 5 minutes, with fluctuation uncontrolled meanwhile
Control method introduced
Variable sliding mode control
Result on the caster
Fluctuation within ±30% of target rate; amount reduced by about 50%
Result on quality
Scrap in billet trimming reduced by about half
Tell the supplier whether the caster uses a stopper or a slide gate, what disturbances you see (bulging, dummy bar, clogging), and ask for the controller's adaptive or disturbance-rejection functions and a fluctuation target.
05
An eddy-current mould level system for stopper-rod casters
The maker listed below shows an eddy-current detector rather than a radiometric one, with a stated 0–150 mm range; compare that with the 100 to about 200 mm radiometric ranges above and the eddy-current sensor JFE used on its billet caster. [1][3]
06
Gamma source, detector, evaluation unit, controller and stopper or slide-gate actuator
Measuring range, precision, time constant and source isotope for a mould level order
Range, time constant, update rate, source and detector rows come from Berthold's white paper; its ±1.2 mm precision comes from one worked case at 10,000 counts/s, so ask for the precision guaranteed at your own count rate and set point. [1]
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Shanghai Hinner Information Technology Co., Ltd.
Manufacturing site to be confirmed for the order
Lists an eddy-current mould level detection system used with stopper-rod control on slab, bloom and round-bloom casters, stating a 0–150 mm measuring range.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How precise is radiometric mould level measurement?
In one worked example at 10,000 counts/s and a 0.8 s time constant, ±1.2 mm for 95% of the time and ±1.8 mm for 99.7%. [1]
Is Co-60 or Cs-137 better for mould level?
Berthold's paper favours Co-60: Cs-137 needs up to five times the activity, is more affected by casting powder and gives a non-linear calibration. [1]
Are there alternatives to radioactive sources?
Electromagnetic (eddy-current) systems are the other main technology, and a 1983 patent proposed optical pulse ranging from above the mould. [1][2]
How much can better mould level control reduce fluctuation?
JFE Steel reports that variable sliding mode control on a billet caster held fluctuation within ±30% of target and cut it by about 50%, halving billet trimming scrap. [3]
Does mould level control steady the whole meniscus?
No. Nippon Steel's Technical Report No. 89 found fluctuation well controlled near the sensor but large on the opposite side of the mould, concluding that mould level control suppresses local level fluctuations only. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Berthold's white paper is written by a radiometric gauge maker and the Endress+Hauser patent argues for an alternative; read both as one side's view. Performance for your caster must come from the supplier's guarantees and your radiation-protection authority.