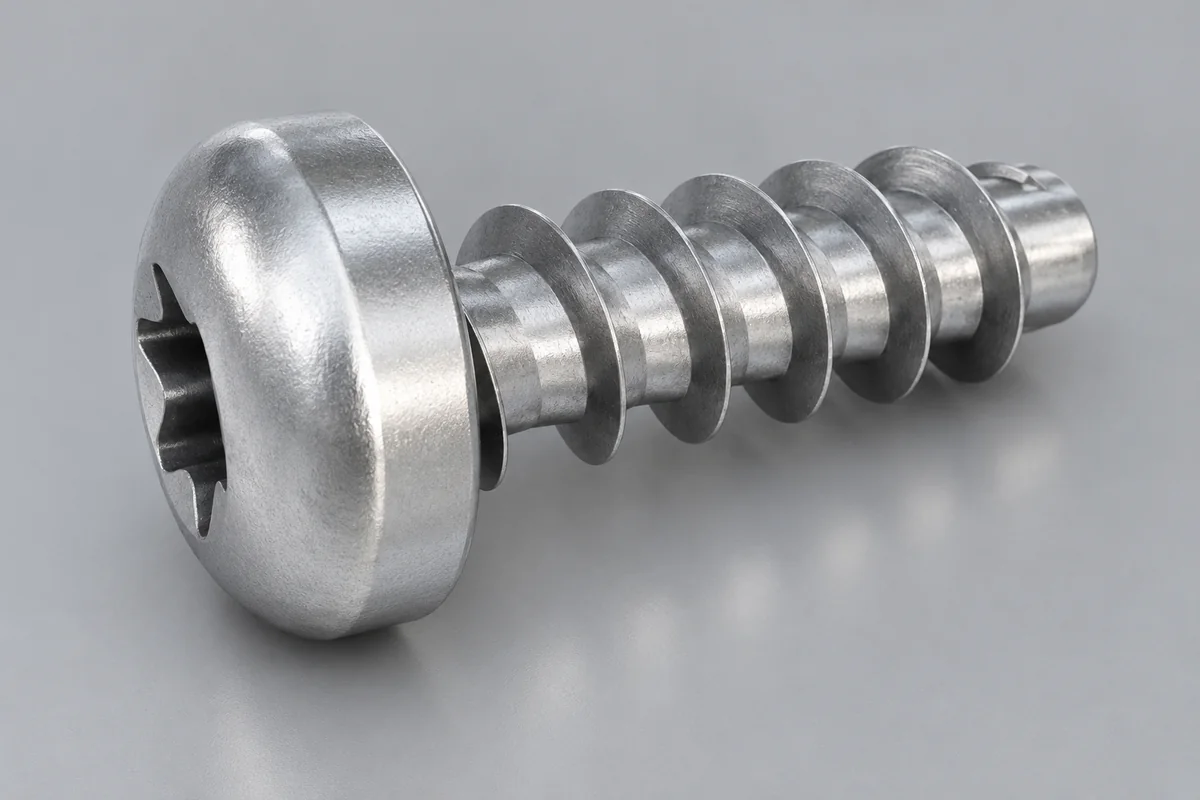
Self-tapping screws · Insertion, tightening and stripping torque, thread geometry, pilot-hole ratios for plastics, driver speed, torque cut-off, plating and hydrogen embrittlement
A self-tapping screw is a hardened fastener with a tapered or pointed threaded shank that forms or cuts its own mating thread as it is driven into a pilot hole in plastic, sheet metal or wood, so no tapped hole or nut is needed. Ask three things first: which thread geometry suits the material it will be driven into, which pilot-hole size and engagement depth give a safe gap between insertion and stripping torque, and which material and finish suit the load and environment.
Thread-forming and thread-cutting self-tapping screws for plastics, sheet metal and similar materials. Self-drilling screws, drywall and chipboard screws, wood screws, machine screws and threaded inserts are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Set the torque window between insertion and stripping
Covestro's technical information on self-tapping screws for thermoplastics defines the insertion torque as the maximum torque reached before the screw head seats, and the stripping torque as the torque that strips the formed thread. It sets the tightening torque at least 1.2 times the insertion torque but not more than 0.5 times the stripping torque, says both should be measured experimentally, and states that the higher the ratio of stripping to insertion torque, the more reliable the joint. [1]
It lists causes of joints damaged in assembly: the kinetic energy of nut-runner masses that cannot be braked fast enough (especially at high speed with small screws), an unknown or misjudged stripping torque, and too small a screw-in depth; increasing screw-in depth raises stripping torque considerably with only a slight rise in insertion torque. [1]
Editorial calculation: if trials give an insertion torque of 0.5 N·m and a stripping torque of 2.0 N·m (assumed values), Covestro's rule allows tightening between 0.6 and 1.0 N·m; if the stripping torque were only 1.1 N·m, the window would shrink to 0.6–0.55 N·m and close. [1]
Give the supplier the material to be fastened (resin grade, glass content, or sheet thickness and grade), pilot-hole size, screw-in depth, thread form (thread-forming or thread-cutting), head and drive, required pull-out or clamp load, reuse cycles, screw material, hardness and finish, any baking requirement, driving equipment and quantities.
02
Size the screw, pilot hole and driving speed
For thermoplastics Covestro recommends screws with a sharp thread angle below 40°, a small core diameter below 0.65 × D, a high pitch above 0.35 × D and tight tolerances, and says countersunk heads are unsuitable because of their expanding effect. For screws without cutting notches of D = 2.9 to 5.1 mm its pilot-hole diameters are 0.86–0.89 × D for Bayblend PC+ABS, 0.90 × D for unreinforced Makrolon PC and Apec, and 0.92 × D for glass-fibre-reinforced Makrolon. [1]
Screws with a cutting notch cut the thread and suit single or few assemblies; reducing the hole diameter to meet repeated-assembly requirements raises boss expansion and the risk of long-term stress cracking. Screw circumferential speeds of 3–6 m/min have proved successful, about 250–500 rpm for a 4 mm screw; too much frictional heat lowers the stripping torque. Screws should be free from cutting oil or rust-protection residues that can cause stress cracking. [1]
NASA's Fastener Design Manual notes that plating processes can generate hydrogen, so plated steel fasteners must be baked after plating to prevent hydrogen embrittlement, and that dissimilar metals in contact can cause galvanic corrosion. [2]
A patented thread-forming screw for harder plastics from Illinois Tool Works takes a different route: an asymmetric thread with a flank angle of about 30°, split into a leading angle of 20° ± 2° and a trailing angle of 10° ± 1°, and a smaller pitch for more threads per inch. For an M5.0 screw the patent gives a pitch of 1.15–1.35 mm (1.25 mm preferred, ±0.10 mm) against conventional pitches of about 2.25 mm, a thread outside diameter of 5.0–5.25 mm and a core diameter of 3.80–4.00 mm, an outside-to-core ratio of about 1.30:1; M4.0 examples have a 0.90–1.10 mm pitch and a 3.0–3.20 mm core. [4]
Editorial calculation: the patent's M5.0 example has a core of about 3.9 / 5.1 ≈ 0.76 × D and a pitch of 1.25 / 5.0 = 0.25 × D, outside Covestro's general guidance of a core below 0.65 × D and a pitch above 0.35 × D; the patent trades the larger core and finer pitch for pull-out resistance, so ask which design rule a quoted screw follows. [1][4]
Editorial calculation: for a 3.5 mm screw in unreinforced Makrolon, the pilot hole is 0.90 × 3.5 ≈ 3.15 mm; at 250 rpm a 4 mm screw's thread moves π × 4 mm × 250 ≈ 3.1 m/min, matching Covestro's lower speed limit. [1]
03
Pick a pilot hole from a screw maker's material factors
TR Fastenings' installation guide for its Plas-Tech 30 screw for plastics (a 30° flank angle and 8° pitch angle, with a profiled thread root) sizes the hole by multiplying a material factor by the nominal thread diameter d: for example 0.80d for ABS, so a 3.0 mm screw in ABS takes a 2.4 mm guideline hole. It recommends a counterbore 0.2 mm larger than the published head diameter to protect the top of the boss and relieve extruded material, and says the screws can go into moulded holes with a 1° inclusive taper or into drilled holes. [3]
The factors show glass-filled grades taking a larger hole than the same unfilled resin (0.80d for PA6 GF30 against 0.75d for PA6). [3] Compare these with the pilot-hole table and torque window from Covestro and the fastener design data from NASA above, and confirm by trials on your boss. [1][2]
Editorial calculation: hole diameters in the table are factor × 3.0 mm; for a 4.0 mm screw in PC the 0.85d factor gives 3.4 mm.
Material (TR Plas-Tech 30)
Hole factor A
Hole for d = 3.0 mm (editorial)
ABS; ABS/PC
0.80d
2.40 mm
PA6; PA6.6; PBT; PP; POM
0.75d
2.25 mm
PA6 GF30; PBT GF30
0.80d
2.40 mm
PA6.6 GF30
0.82d
2.46 mm
PC; PC GF30; PMMA; PVC
0.85d
2.55 mm
LDPE
0.70d
2.10 mm
Give the screw supplier your resin grade, filler content and boss drawing, and ask for its hole factor and recommended counterbore for that grade.
04
Compare what suppliers offer
Suppliers linked to this page list self-tapping screws; each card links to the page reviewed.
Listings include pan, hex and other head self-tapping screws among machine, drywall, chipboard and self-drilling screws.
05
Trace what defines the screw
This is a functional reference built from the sources cited; it is not one maker's design.
Fill the specification fields with values for your joint
A self-tapping screw quotation needs values for your joint. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Field
What it means and published values
Ask the supplier for
Thread
Flank angle below 40°, core below 0.65 × D for plastics. [1]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory, certificates and scope for your order. How we source and review
· Page last updated 12 October 2026
How tight should a self-tapping screw be in plastic?
Covestro sets tightening torque at least 1.2 times the insertion torque and no more than half the stripping torque. [1]
What pilot hole should be used in plastic?
Covestro recommends 0.86–0.92 times the screw diameter depending on resin, for D = 2.9 to 5.1 mm. [1]
Can countersunk self-tapping screws be used in plastics?
Covestro says countersunk heads are unsuitable for thermoplastics because of their expanding effect. [1]
What pilot hole does a self-tapping screw for plastic need?
TR Fastenings multiplies a material factor by the screw diameter: 0.80d for ABS (2.4 mm for a 3.0 mm screw), 0.75d for PA6 or PP, 0.85d for PC. [3]
Does a finer pitch help a thread-forming screw hold in plastic?
Illinois Tool Works' patent US 6,702,537 B2 uses a 1.15–1.35 mm pitch on an M5.0 screw, against about 2.25 mm for conventional screws, to raise pull-out resistance, with a flank angle of about 30° to reduce cracking in harder plastics. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Covestro is a plastics maker giving guidance for its own resins; TR Fastenings publishes hole factors for its own screw; Illinois Tool Works' patent describes one thread-forming design; NASA's manual is general fastener guidance. Values for your joint must come from trials and the supplier.