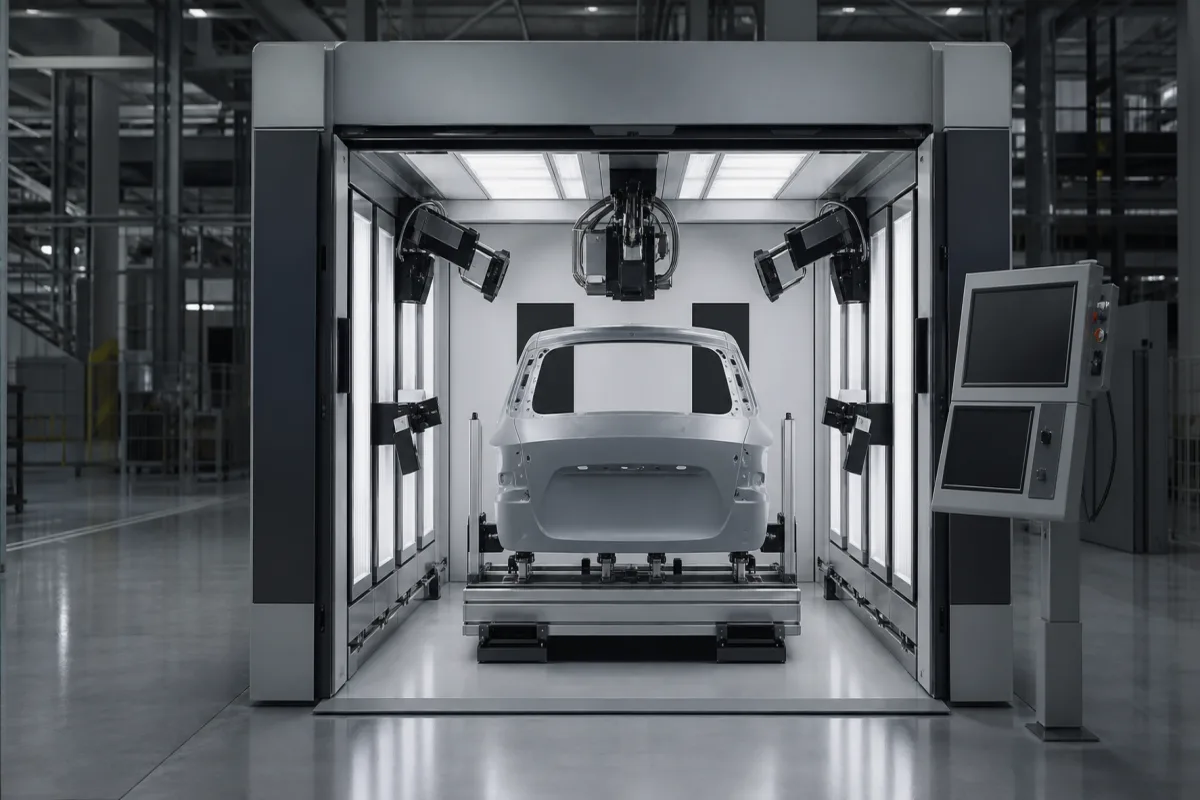
Body-in-white quality inspection station: robot-carried sensors that gauge holes, studs and edges and look for dents on every body before paint
Body shop, before paint · the station that checks every body-in-white for feature position and sheet-surface defects, and the measuring cell that backs it up
Once the body-in-white leaves the last framing and closure stations, it is the last chance to catch a misplaced hole, a missing stud, a hem edge out of position or a dent in the sheet before paint makes every repair dearer. A quality inspection station at that point is a cell in which robot- or structure-mounted sensors measure the body's features and scan its panels within the line cycle, flag parts out of tolerance, and send the data back up the line. Its buyer has to settle three things: how the measured points are made accurate when a robot carries the sensor, which surface defects the cell must find, and what reference measurement backs up the in-line results.
In-line and at-line inspection stations for car bodies-in-white and their closures before paint: robot- or structure-mounted laser-line gauging sensors for holes, slots, studs, edges and gap and flush, optical trackers that locate the sensor in space, surface-defect sensors for dents, sink marks, cracks and residues, the software that compares results to tolerances, and the robot-based scanning cells used as the offline reference. Camera-based inspection, measurement and guidance systems for production lines are covered on the Machine vision system for inspection page; fixed 3D cameras that find the pose of a body so a robot can correct its path on the 3D vision guidance for robot cells on car bodies page; and end-of-line toe, camber and headlamp setting on the finished car on the End-of-line wheel alignment and headlamp aiming station page. Laser line profile sensors as components are covered on the Laser scanner modules (laser line profile scanners) page, vision measuring probes on the Vision camera system for coordinate measuring machines page, reference bridge CMMs on the High-accuracy reference bridge CMM page, multi-camera defect inspection of cast and machined parts on the Vision system for cast and machined parts page, handheld and fixed 3D scanners as instruments on the Optical 3D scanner for dimensional inspection page, and the panels themselves on the Automotive body panels page.
CNFX editorial research · Sources checked October 13, 2026 · 5 sources
Gauging holes, studs and hem edges on every body: laser-line sensors on robots, and an optical tracker that takes the robot's error out
ISRA VISION's Perceptron metrology flyer describes the in-line approach: every part is measured without removing it from the line, with HelixHD non-contact sensors mounted on robots, on fixed structures or both, and the software can stop the line, alert line staff or route a part out through the PLC when a critical feature falls outside its limits. [3] The sensor data sheet gives the hardware choice as a family of standoffs.
The same data sheet lists laser line triangulation with a green 520 nm laser in Class 2M or 3R under IEC 60825-1:2014, IP67, PoE Class 4 on a single cable, operation from 10 to 45 °C, and factory calibration so that each sensor arrives ready to measure; its thin laser line is offered for threaded holes, studs and hemmed edges. [1] Editorial calculation from the table: the X1400 is 3.8 times the length and 2.7 times the weight of the X200, so a longer standoff adds length and payload at the robot wrist. ISRA's body-shop page lists holes and slots, surfaces, threaded studs and feature relationships as measured features and quotes measurements in 2.5 s, without saying whether that is per feature or per part. [3]
Where the sensor rides on a robot, the robot's own positioning error enters the result. ISRA says its AccuSiteHD optical tracking option cancels out the influence of the robot, and mechanical drift and temperature, in this way: a receiver locates emitters on the sensor and records its position and orientation while it scans, in less than 0.1 s, so that the robot becomes a mover only. ISRA states a system-level accuracy of less than 0.150 mm, validated to DIN/ISO 10360-8, and up to 10 trackers per system for large parts. [2] Each tracker measures 1,174 × 132 × 86 mm and weighs 8.3 kg, with IP67 and operation from 10 to 45 °C. [2]
For gauging, give the supplier the feature list with tolerances (holes, slots, studs, edges, gap and flush), the cycle time available, the robots and structures available for mounting, whether results must be absolute (CAD-referenced) or relative to a master body, and what the line should do when a feature fails.
02
Dents, sink marks, cracks and weld or adhesive residues on bare sheet: a multi-light surface sensor inside the cycle
Dimensional gauging does not find a dent. ZEISS describes the alternative to grindstone checks in its ABIS III surface inspection system, which it offers for press shops and body shops, in-line or at-line, and for moving or stationary parts. [4]
In the BMW application ZEISS describes, four robots inspect the entire surface of each body before it is transferred to the paint shop, within the available cycle time, and the results are ready before the body leaves the station; they are used for rework, for tracking defect hot spots and for closing quality loops between press shop and body shop. [4]
Editorial calculation: one 300 × 225 mm field covers 0.0675 m², so at 20 frames a second a single sensor could at best pass over 1.35 m² per second; the figure assumes no overlap between frames and no robot travel between them, neither of which holds in a real path, and is only a way to compare surface area against cycle time. [4] An 11.5 kg sensor at a 460 mm working distance also sets the robot payload and the clearance it needs around the body. [4]
For surface inspection, give the supplier the panel areas to be covered, the defect types and their acceptance limits or limit samples, the cycle time, whether the body is moving or stopped in the station, and how defects should be reported for rework.
03
Behind the line station: full-field scanning of a complete body in a measuring cell, and what the comparison buys
A line station measures a chosen set of features on every body; a measuring cell digitises the whole body on a sample. ZEISS's ScanBox Series 8 data sheet describes a cell in which complete vehicles are digitised from outside and inside in less than 30 minutes, with more than 1,000 measurement features such as bolts, surface and edge points and holes. [5]
ZEISS's product page adds that two 8-axis kinematics can scan in a shared coordinate system or work on two parts independently, that the 8160 model handles parts up to 6,000 × 2,500 mm, that the 8260 and 8360 add rotation-table areas for doors and trunk lids while a body is measured in the centre, and that bodies can be loaded by a driverless transport system or by cart, truck, crane or forklift. Its laser-light ATOS 5X sensor scans measuring areas up to 1,000 mm. [5]
The two do different jobs: the line station measures a set of features on every body inside the cycle [3], while the scanning cell takes up to half an hour to cover all of one body [5]. ISRA presents its tracked in-line gauge as delivering CMM-level accuracy on the plant floor without moving the part to the quality room. [2]
Ask how in-line results will be checked against the reference cell or CMM, how often a body is pulled for full scanning, and whether both systems report against the same CAD datum and feature names.
04
What a body-shop inspection station enquiry should state
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Body: [models and variants; materials; size]
Features to gauge: [holes, slots, studs, edges, gap and flush; tolerances]
Surfaces to inspect: [panels; defect types; limit samples]
Cycle: [line cycle time; stop-and-go or moving]
Mounting: [robots available; fixed structures; enclosure]
Accuracy: [absolute or relative to a master; acceptance test]
Outputs: [line stop, alerts, part routing, data to SPC]
Reference: [CMM or scanning cell used for correlation]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How can a robot-carried sensor give accurate absolute results?
ISRA's AccuSiteHD tracks emitters on the sensor and records its position and orientation in less than 0.1 s, and ISRA states a system-level accuracy below 0.150 mm validated to DIN/ISO 10360-8. [2]
What standoff can a body-shop gauging sensor work at?
ISRA lists HelixHD sensors from the X200 to the X1400, for standoffs of 200 to 1,400 mm, with depth of field from 175 to 300 mm and fields of view from 150 × 140 mm to 220 × 180 mm. [1]
Which surface defects can be found before paint?
ZEISS names dents, sink marks, neckings, cracks, pressure marks, scratches and welding and adhesive residues for its ABIS III sensor, which uses 8 cameras and 200 light sources at up to 20 Hz. [4]
How long does a full-body scan take?
ZEISS states that its ScanBox Series 8 digitises complete vehicles from outside and inside in less than 30 minutes, covering more than 1,000 measurement features. [5]
Sources and what still needs a direct check
Sources checked 2026-10-13. Gauging figures come from ISRA VISION's Perceptron flyers and body-shop page (sensor data sheet, optical tracker, in-line metrology); surface inspection and offline scanning figures from ZEISS product pages, a brochure and a data sheet.