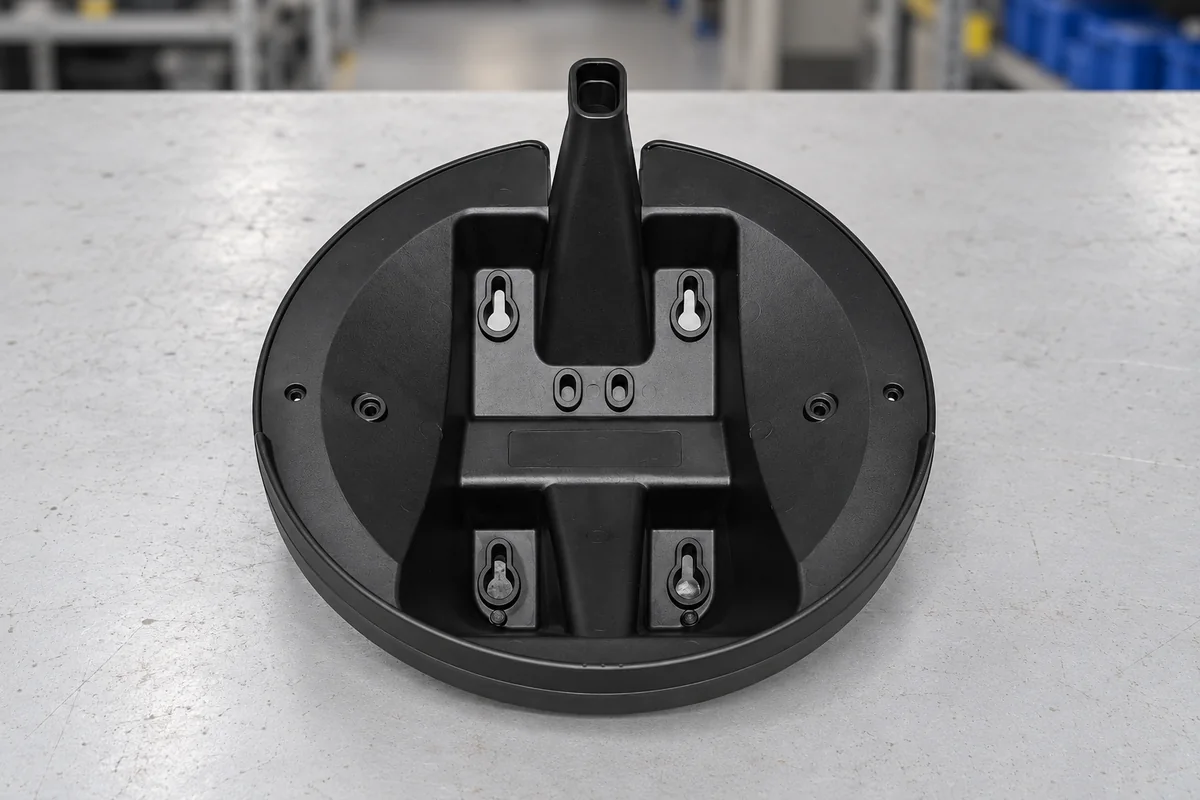
Custom plastic injection-moulded parts · Recommended wall thickness by resin, draft angles, size and side-action limits, achievable tolerances, finishes, and inspection reports from FAI to PPAP
A plastic injection-moulded part is a custom component made by injecting molten thermoplastic into a machined mould, giving repeatable parts for housings, clips, medical and packaging components. Ask three things first: which resin and wall thickness the part uses, since resin sets the recommended walls and shrinkage; whether the geometry has draft, even walls and moldable undercuts; and what tolerances and inspection reports the supplier will commit to.
Custom thermoplastic injection-moulded parts, from prototypes to production, including insert-moulded and overmoulded parts. Injection moulds and machines, rubber and silicone moulded parts, and liquid silicone rubber parts (covered separately) are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Protolabs' injection moulding guidelines list recommended wall thicknesses by resin: ABS 1.143–3.556 mm, acetal 0.762–3.048 mm, acrylic 0.635–12.7 mm, liquid crystal polymer 0.762–3.048 mm, long-fibre reinforced plastics 1.905–25.4 mm, nylon 0.762–2.921 mm, polycarbonate 1.016–3.81 mm, polyester 0.635–3.175 mm, polyethylene 0.762–5.08 mm, PPS 0.508–4.572 mm, polypropylene and polystyrene 0.889–3.81 mm and polyurethane 2.032–19.05 mm. It recommends draft of 0.5° on vertical faces, 2° for "most situations", 3° minimum for shut-offs and light texture, and 5° or more for medium texture. [1]
Its maximum part size is 18.9 × 29.6 × 8 in (480 × 751 mm footprint), 59 in³ volume, 4 in depth from the parting line (up to 8 in if the parting line passes through the middle) and 175 in² projected mould area; side actions are limited to about 8.4 × 2.4 in with 2.9 in pull. Standard finishes run from non-cosmetic PM-F0 through SPI-C1 (600 stone, 10–12 Ra) and SPI-B1 (600 paper, 2–3 Ra) to SPI-A2 (diamond buff, 1–2 Ra), with texturing, threaded inserts, pad printing, laser engraving and basic assembly as options. [1]
Editorial calculation: ABS's 0.045–0.140 in recommended range means the thickest recommended wall is about three times the thinnest; a 2.5 mm ABS wall sits inside the range, while a 4 mm wall would exceed it. [1]
A resin maker's design guide ties draft and venting to the material. Covestro's Engineering Polymers Part and Mold Design guide for thermoplastics says Makrolon PC, Bayblend PC/ABS and Makroblend PC/PET need at least 1° of draft for easy ejection, Apec high-heat PC ejects best with 3° or more, and Texin and Desmopan TPU need at least 5° plus a 0.5–0.6 µm surface roughness. For parting-line vents it keeps the first 0.150 to 0.300 in of vent land shallow — less than 0.0020 in deep for amorphous resins and less than 0.0015 in for semi-crystalline resins — and places vents at the last areas to fill, farthest from the gate, adding ejector pins with flats where air traps persist. [3]
Editorial calculation: on a 50 mm deep wall, 1° of draft opens the opening by about 0.87 mm per side (50 × tan 1°), 3° by about 2.6 mm and 5° by about 4.4 mm, so a TPU part designed to the 5° minimum needs noticeably more taper than a PC part at 1°; and a 0.0020 in vent depth is about 0.05 mm. [3]
Wall thickness also limits how far the melt can travel. A Turkish university and seat-supplier team moulded polypropylene (MFR 11 g/10 min, density 0.99 g/cm³) into a centre-gated spiral at 240 °C melt and 40 °C mould temperature, and simulated walls of 0.50, 1.50, 2.70 and 3.00 mm at injection pressures from 20 to 180 MPa. At 20 MPa the fill stopped at 0.43 s for the 0.50 mm wall because the melt froze early, against 1.61 s, 5.03 s and 6.13 s for 1.50, 2.70 and 3.00 mm. The 0.50 and 1.50 mm spirals could not be filled even at maximum pressure, the 3.00 mm spiral filled its full length at 140 MPa, and the measured 2.70 mm parts agreed with the simulation to about 90%. [4] Ask the moulder for a fill (mould-flow) check when a wall sits near the thin end of the resin's recommended range.
Give the supplier the 3D CAD and 2D drawing with critical dimensions and tolerances, resin grade and colour, annual and batch quantities, cosmetic finish or texture, inserts or overmoulding, secondary operations (printing, engraving, assembly), mould life and cavity expectations, inspection level (FAI, CTQ, capability study, PPAP), certifications (ISO 9001, ISO 13485, IATF), packaging and delivery.
02
Agree tolerances and inspection evidence
Protolabs states that "typically, Protolabs can maintain a machining tolerance of +/- 0.003 in. (0.08mm)", plus a resin tolerance of no less than ±0.002 in/in, which can be larger depending on resin. [1] It describes scientific (decoupled) moulding — a documented, optimised fill, pack and hold process with tracked changes — DFM analysis that flags thick walls and insufficient draft with mould-flow, gate and ejector-pin selection, and certifications including ISO 9001:2015, ISO 13485:2016 and AS9100D. [2]
Its inspection options include critical-to-quality partial first-article inspection, a CTQ dimensional report with capability study, full FAI or digital inspection report, PPAP and custom inspection; standard checks measure up to four plane-to-plane and outside-diameter dimensions on a sample of parts using CMMs, calipers and pin gauges, and capability reports sample parts at an equal cadence of n/30 of the order quantity and give the mean, standard deviation and Cpk for critical dimensions. [2]
Editorial calculation: for a 100 mm (3.94 in) dimension, ±0.003 in + 0.002 in/in × 3.94 in is about ±0.011 in, or ±0.28 mm; for an order of 3,000 parts, n/30 sampling measures every 100th part. [1][2]
03
Compare what suppliers offer
Suppliers linked to this page list plastic injection-moulded parts; each card links to the page reviewed.
Listings include custom injection plastic parts from rubber-and-plastic moulders, medical plastic components, vent and breather plastic parts, and injection moulding with in-house mould making; ask each for resin traceability, tolerance capability, inspection reports and mould ownership terms.
04
Trace the part specification
This is a functional reference built from the sources cited; it is not one maker's specification.
Fill the specification fields with values for your part
A moulded-part quotation needs values for your part. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 12 October 2026
What wall thickness should an injection-moulded part have?
It depends on the resin: Protolabs recommends, for example, 1.14–3.56 mm for ABS and 0.89–3.81 mm for polypropylene. [1]
How much draft does an injection-moulded part need?
Protolabs recommends 0.5° on vertical faces, 2° for "most situations", and 3° or more for shut-offs and textured surfaces. [1]
What inspection can a moulder provide?
Protolabs offers first-article inspection, CTQ reports with capability studies (Cpk) and PPAP, measured with CMMs at n/30 sampling. [2]
Does draft depend on the resin?
Yes; Covestro's design guide asks for at least 1° on Makrolon PC and PC blends, 3° or more on Apec high-heat PC and at least 5° on TPU. [3]
Sources and what still needs a direct check
Sources checked 2026-10-12. Protolabs pages describe its own design rules, tolerances and inspection services, Covestro's guide gives draft by resin, and an open-access Polymers paper reports measured fill lengths for thin polypropylene walls; other moulders' capabilities differ.