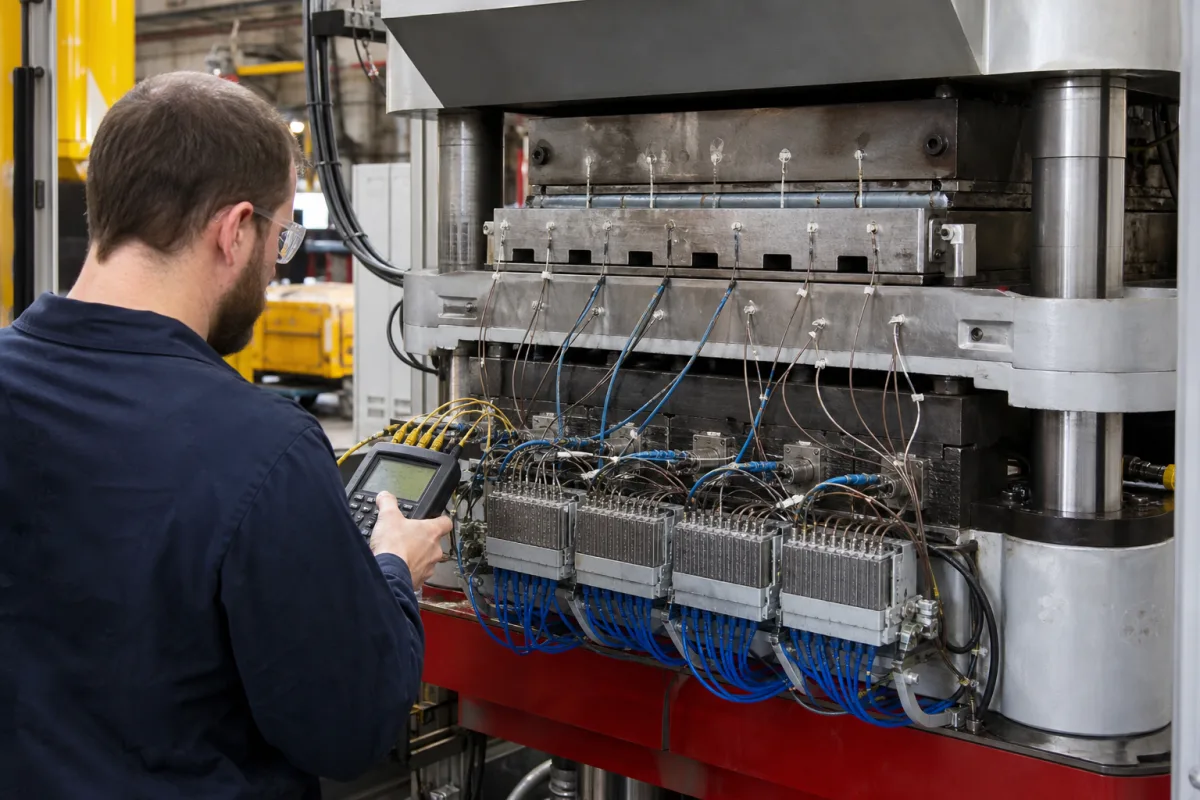
Temperature sensor array in a mould cavity: flush, fast-response thermocouples along the flow path that time the melt front and compare cavities
A set of fast thermocouples set flush in the cavity wall of a mould · placed along the flow path to see the melt arrive, wired out through multi-channel connectors, with fronts that are machined, textured or hardened
A single probe in a mould plate reports how warm the steel is. An array of cavity temperature sensors does something else: each sensor sits flush with the cavity surface at a chosen point along the flow path, and the sharp temperature rise when hot melt touches it marks the moment the flow front passes. Two or more such points show how far the cavity has filled and whether the cavities of a multi-cavity mould fill together. Buying one means choosing sensors fast enough for that job, routing every sensor's signal out of the mould, and matching the sensor face to the cavity surface.
Arrays of cavity temperature sensors, and combined cavity pressure-and-temperature sensors, mounted flush in injection mould cavities to detect melt-front arrival and compare cavities, with their cabling, multi-channel connectors and sensor fronts. Pt100 RTD probes for process and machinery are covered on the Temperature sensor probes (Pt100 RTD assemblies) page; sheathed thermocouples inserted through fittings on the Mineral-insulated thermocouple sensor page; thermocouples in heated press platens on the Heated press platen page; mould temperature controllers on the Mould temperature controller page; PLC temperature input cards on the Temperature input module page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Timing the melt front: why response speed, not steady accuracy, decides the sensor
Priamus explains that cavity temperature sensors are used, besides measuring temperature, to detect the position of the plastic melt in real time, that a very short reaction time is crucial for this, and that conventional thermocouples are too slow; each of its sensors is checked for reaction speed before delivery, and because no standards apply to dynamic behaviour, it uses specially developed test procedures. [4]
RJG's own framing is that melt and mould temperature are two of the four plastic variables that determine how a part is formed, and that its sensors work with its process control systems to diagnose temperature-related problems. [3]
Editorial calculation (illustrative, with an assumed flow-front speed): if the melt front moves at 0.5 m/s past a sensor, 1 ms of sensor response corresponds to 0.5 mm of flow travel. The real flow-front speed depends on the part and the injection profile; use it to judge whether a sensor's stated response is fine enough for the distance between array positions.
±1.1 °C from 0 to 275 °C; 0.4% of reading from 275 to 450 °C [3]
Kistler 6188A temperature response
Short response time owing to the small sensor dimensions (no figure given) [1]
Priamus dynamic test
Every sensor checked for reaction speed; no applicable standard for dynamic behaviour [4]
Mark on the part drawing where each sensor should sit along the flow path (near the gate, mid-flow, end of fill, and in each cavity of a multi-cavity mould), and ask each supplier for a stated dynamic response, not only static accuracy.
02
Front diameter, pressure rating and thermocouple type across three makers
The sensors used in such arrays differ in size, in whether they also measure pressure, and in thermocouple type. Kistler's Types 6188A and 6190C measure cavity pressure across the whole front with a piezoelectric crystal and the melt's contact temperature with a Type K (NiCr-Ni) thermocouple pair on the front; the pressure charge is converted to 0–10 V in an amplifier. [1][2]
Editorial calculation: 30,000 psi is about 2,068 bar, close to Kistler's 2,000 bar range; 400 °F is about 204 °C. RJG's page lists the sensor at +450 °C while limiting the Teflon-coated wire to moulds up to 400 °F; ask which limit governs the installed sensor in your mould. [3]
Priamus says it chose Type N because, compared with other thermocouples, it shows no corrosion and no irreversible temperature shifts. [4] Editorial note: Type K and Type N need different input settings on the evaluation electronics; an array should not mix types unless every channel is configured for its sensor.
Getting every sensor signal out of the mould: sensors without connectors, multi-channel plugs and colour coding
With a sensor at each chosen position in each cavity, wiring becomes part of the product. Kistler offers 6188A and 6190C sensors without connectors (types 6188AAG and 6190CAG) for multi-cavity moulds: the charge cables go to multi-channel connectors Type 1708 or 1710, and the two temperature conductors to the Type 2205B temperature amplifier. [1][2]
Priamus colour-codes plugs — red for cavity temperature sensors and black for cavity pressure sensors — on all connecting and extension cables; offers compact sensors whose rigid housing is installed axially in cavity inserts without a connection cable and transmits through a quick disconnect; and does not use open cable ends, preferring grounded signal lines with connectors to avoid noise from grounding problems. [4] RJG supplies its press-fit sensor with 1.8 m or 2.5 m cables. [3]
Editorial note: count channels before ordering — sensors per cavity times cavities — and check that the mould's connector plate, the multi-channel connectors and the amplifier or monitoring system have one temperature input per sensor, set for the right thermocouple type.
List sensor positions and count, cable routing through the mould, connector type and channel count, and the monitoring system the array will feed.
04
The sensor face in the cavity: flush, contoured or hardened against abrasive melts
Each sensor face becomes part of the moulding surface. RJG installs its sensor by drilling a small hole for the wire and a flat-bottomed pocket at press-fit tolerance from the cavity face, and states that the sensor head can be textured or contoured to the part; it claims installation costs cut by over 50%. [3] Kistler's 6188A and 6190C fronts cannot be machined. [1][2]
Priamus offers both: machinable fronts, which can be adapted to the cavity contour but wear faster with abrasive plastics, and hardened fronts for ceramic melts and highly filled materials; it shows fronts after about 2,000,000 cycles with abrasive plastics, where the machinable front had worn significantly more than the hardened one. [4]
Editorial note: on a visible surface the sensor face leaves a witness mark; agree with the part owner where marks are acceptable before fixing the array layout, and choose hardened fronts for glass- or mineral-filled grades.
05
What to send for a mould cavity temperature sensor array
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Mould: [number of cavities; part drawing with sensor positions; surface finish or texture at each position]
Material: [polymer grade; filler type and content]
Sensors: [temperature only or pressure plus temperature; front diameter; machinable or hardened]
Range: [mould temperature; melt temperature; cavity pressure]
Response: [required dynamic response; test method]
Wiring: [cable length; connector type; channel count; thermocouple type]
System: [monitoring or process control unit the array connects to]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Why use more than one temperature sensor in a mould cavity?
Priamus states cavity temperature sensors detect the position of the melt in real time, which needs a very short reaction time; positions spread along the flow path show how the cavity fills. [4]
How fast does a cavity temperature sensor respond?
RJG states 1 ms for its press-fit sensor to see a 1–2 °C rise; Priamus checks every sensor's reaction speed because no standard covers dynamic behaviour. [3][4]
What thermocouple types are used in cavity temperature sensors?
Kistler's 6188A and 6190C and RJG's TS-PF03-K use Type K; Priamus uses Type N, citing no corrosion and no irreversible temperature shifts. [1][3][4]
How small can a cavity pressure-and-temperature sensor be?
Kistler's 6188A has a 1 mm front, rated to 2,000 bar and 0–200 °C. [1]
Sources and what still needs a direct check
Sources checked 2026-10-12. Sensor sizes, ratings and multi-cavity wiring come from Kistler's 6188A and 6190C product pages; press-fit installation, response and accuracy from RJG's TS-PF03-K product page; thermocouple type, dynamic testing, colour coding and front wear from Priamus's sensors and electronics page.