High-temperature thermocouple assemblies · IEC 60584 classes vs ASTM E230 tolerances, ceramic thermowell limits, preheating and insertion speed, wire diameter, support tube, head and transmitter
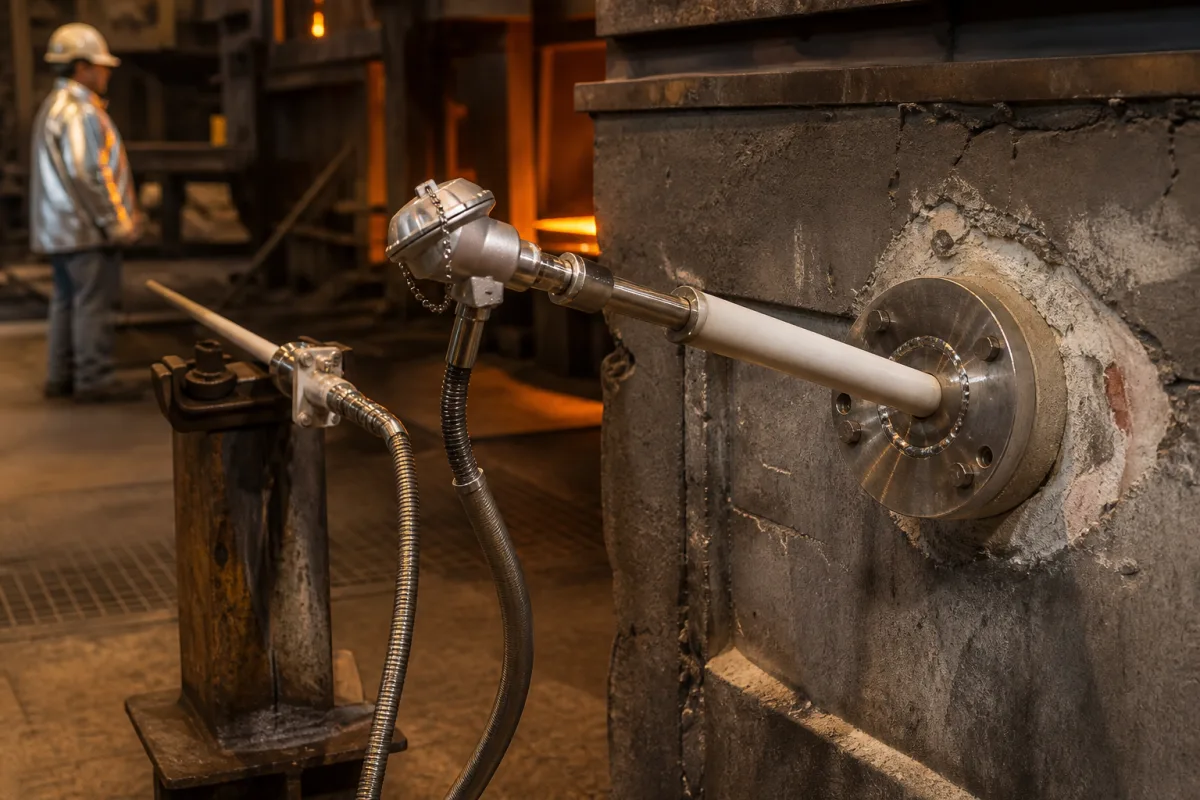
A high-temperature thermocouple assembly measures furnace, kiln or molten-metal process temperatures with a thermocouple insert inside a ceramic or metal thermowell, fixed through the furnace wall with a terminal head, like the ceramic-sheathed assembly pictured entering a refractory wall. Ask three things first: which thermocouple type and tolerance class the measurement needs at your temperature, which thermowell material and construction will survive the atmosphere and thermal shock, and how fast the assembly responds and how it must be installed.
Thermocouple assemblies with ceramic or high-temperature metal thermowells for furnaces, kilns, ladles, tundishes and combustion processes, including the inserts and head transmitters. Resistance thermometers (see temperature sensor probes), disposable immersion tips, pyrometers and temperature controllers are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 5 sources
Endress+Hauser's technical information for its TAF11, TAF12x and TAF16 high-temperature thermometers lists IEC 60584 tolerances. For Type K (NiCr-NiAl), Class 2 is ±2.5 °C from −40 to 333 °C and ±0.0075|t| from 333 to 1,200 °C, Class 1 ±1.5 °C to 375 °C and ±0.004|t| to 1,000 °C. For Types R and S (platinum-rhodium), Class 2 is ±1.5 °C from 0 to 600 °C and ±0.0025|t| from 600 to 1,600 °C, Class 1 ±1 °C to 1,100 °C and ±[1 + 0.003(|t| − 1,100)] to 1,600 °C. Type B (PtRh30-PtRh6) Class 2 is ±1.5 °C or ±0.0025|t| from 600 to 1,700 °C. [1]
The assemblies accept J, K, N, R, S and B thermocouples, with process temperatures up to 1,600 °C for TAF11 (steel heat treatment, concrete and non-ferrous furnaces) and 1,700 °C for TAF12x (ceramic kilns, brickworks, glass) and TAF16 (cement, steel processing, combustion and fluidised bed furnaces). [1]
Editorial calculation: at 800 °C a Type K Class 2 thermocouple may deviate ±0.0075 × 800 = ±6 °C (±3.2 °C in Class 1); at 1,200 °C a Type S Class 2 allows ±3 °C and Class 1 ±1.3 °C. The tolerance is for the thermocouple itself; installation, drift and the transmitter add further error.
IEC 60584-1:2013 (edition 3.0, published 28 August 2013) specifies reference functions and tolerances for Types R, S, B, J, T, E, K, N, C and A on ITS-90, merges IEC 60584-1:1995 with IEC 60584-2:1982, restricts the Type K reference polynomial to 1,300 °C and gives guidance on upper temperature limits and environmental conditions in Annex C. [5]
WIKA's TC80-H furnace thermocouple sheet lists operating ranges per IEC 60584-1 of −40 to +1,000 °C (Class 1) and −40 to +1,200 °C (Class 2) for Types K and N, 0 to 1,600 °C for R and S and 600 to 1,700 °C for B, and states that the actual limit is set by both the thermocouple and the thermowell material. [2]
Give the supplier the process and maximum temperature, atmosphere (oxidising, reducing, sulphur, alkali, fluorine), molten metal or gas contact, thermocouple type and class, single or double element, thermowell material and dimensions, immersion length and orientation, process connection and pressure, response time needed, head or transmitter output, and the planned replacement interval for the assembly.
02
Compare IEC 60584 classes with ASTM E230 tolerances
ASTM E230/E230M-23a gives temperature-emf reference tables for Types B, C, E, J, K, N, R, S and T and, in its Table 1, standard and special tolerances on initial values of emf versus temperature. Those tolerances apply only to the temperature ranges in Tables 1 to 3, recommended upper temperature limits are in Table 6, and ordering, physical and mechanical properties, workmanship, testing and marking are left to other standards such as E235, E574, E585/E585M, E608/E608M, E1159 and E2181/E2181M. [3]
Pyromation's reproduction of ASTM E230 Table 1 (reference junction 0 °C) gives: Type K and N standard ±2.2 °C from 0 to 293 °C and ±0.75% from 293 to 1,260 °C, special ±1.1 °C from 0 to 275 °C and ±0.4% from 275 to 1,260 °C; Types R and S standard ±1.5 °C from 0 to 600 °C and ±0.25% from 600 to 1,480 °C, special ±0.6 °C and ±0.1%; Type B standard ±0.5% and special ±0.25% from 870 to 1,700 °C. The values apply to new, essentially homogeneous wire from 30 AWG to 8 AWG used within the recommended limits. [4]
WIKA's sheet lists the ASTM E230 ranges as 0 to 1,260 °C for K and N, 0 to 1,480 °C for R and S and 870 to 1,700 °C for B, so the ASTM tolerances for R and S stop below the 1,600 °C IEC range. [2][4]
Editorial calculation: at 1,200 °C, Type K ASTM standard ±0.75% and IEC Class 2 ±0.0075|t| both give ±9 °C; ASTM special ±0.4% gives ±4.8 °C (IEC Class 1 for K stops at 1,000 °C). For Type S at 1,200 °C, ASTM special ±0.1% gives ±1.2 °C against ±1.3 °C for IEC Class 1. For Type B at 1,500 °C, ASTM standard ±0.5% allows ±7.5 °C while IEC Class 2 ±0.0025|t| and ASTM special ±0.25% allow ±3.75 °C. State which standard and class or tolerance the certificate must show. [4][1]
Terminal colour codes also differ: at WIKA's terminal block Type K is green (+) and white (−) under IEC 60584-1 but yellow (+) and red (−) under ASTM E230; Type S is orange/white and black/red. [2]
03
Choose the thermowell and install it without thermal shock
Endress+Hauser lists ceramic thermowell materials to DIN VDE 0335: C530 (about 73–75% Al₂O₃) to 1,400 °C, porous, very resistant to temperature shocks and used as an outer thermowell; C610 (about 60% Al₂O₃) to 1,500 °C, non-porous and resistant to hydrofluoric acid, thermal shock and mechanical stress; and C799 (about 99.7% Al₂O₃) to 1,800 °C. Where a porous ceramic is the outer sheath, a non-porous inner sheath is needed to protect the elements from contamination that would cause drift; metal alloys are stronger but less resistant to high temperatures and abrasion. [1]
Gas-tight ceramic thermowells and inserts are sensitive to rapid temperature change: for process temperatures of 1,000 °C or more the ceramic part must be preheated from room temperature to 400 °C before installation. For horizontal installation the recommended maximum immersion length is 1,500 mm for diameters over 20 mm and 1,200 mm below 20 mm, as hot thermowells can bend or break under their own weight; process connections are gas-tight up to 1 bar, and a thermowell load calculation is recommended at 1 bar and 1 m/s or more. [1]
Protection costs response speed: a TAF12T with a triple ceramic thermowell (26/14/9 mm) takes t50 = 195 s and t90 = 500 s for rapid temperature changes around 1,000 °C in still air. Insulation resistance between terminals and neck is at least 1,000 MΩ at 25 °C and 5 MΩ at 500 °C, measured at 500 V DC. [1]
Endress+Hauser's installation method: with preheating, insert the hot ceramic at 100 mm/min, or 30 mm/min if it cools during transport from a preheating point away from the plant; without preheating, hold the sheath at a depth equal to the wall and insulation thickness for 2 hours at process temperature and then insert at 30 mm/min. Avoid direct flames on the sheath. [1]
WIKA rates the same grades differently: gas-tight C 610 usable up to 1,500 °C and gas-tight, high-purity C 799 up to 1,600 °C, both not resistant to alkali vapours, with C 799 only partially resistant to temperature changes and therefore preheated and inserted slowly. Ask which temperature limit the supplier applies to its ceramic, since Endress+Hauser gives 1,800 °C for C799. [2][1]
Above 1,200 °C only precious-metal thermocouples (Types R, S and B) can be used, their risk of poisoning by contamination rises with temperature, and WIKA recommends gas-tight ceramics, preferably high-purity C 799, there. It also notes that ceramic thermowells are treated as gas-tight to DIN EN 50446 but that diffusion of process gas into the sensor cannot be ruled out at high temperature. [2]
For the metal support tube, WIKA lists use in air up to 550 °C for DIN 1.0305 and up to 1,150 °C for DIN 1.4841, AISI 446 and AISI 310. [2]
04
Build the assembly: wire, support tube, head and transmitter
In WIKA's TC80-H design the ceramic thermowell (outer Ø 24 mm, hemispherical closed tip) is cemented into a metal support tube of Ø 32 mm and 200, 150 or 100 mm length, because of the ceramic's low mechanical strength. Nominal lengths are 500, 710, 1,000, 1,400 and 2,000 mm; the 2,000 mm length is not suitable for vertical installation with a precious-metal element. [2]
Thermowire: base-metal Types K and N use Ø 1 mm or Ø 3 mm wire in ceramic insulation tubes; Types S, R and B use Ø 0.35 mm or Ø 0.5 mm wire in ceramic insulation rods, and WIKA states that long-term stability of precious-metal thermocouples rises with wire diameter. Single or dual elements are offered, with an ungrounded measuring point. [2]
Process connection: an adjustable stop flange, or a threaded bushing G 1 1/4 for the 32 mm support tube, gas-tight up to 1 bar with sealing up to 200 °C. With toxic or safety-critical gases WIKA recommends extra measures, such as a pressure-sealed feed-through in the head, against leakage after a thermowell fracture. [2]
Head and transmitter: the aluminium heads have M20 × 1.5 cable entry and IP53. A built-in transmitter (T16, T32 with HART, T53 with FOUNDATION Fieldbus or PROFIBUS PA) needs the high ASZ-H cap; heat carried along the thermowires can overheat the transmitter terminals, so a short piece of thin compensating cable may connect them. After the transmitter, copper cable replaces thermocouple and compensating cable, and the transmitter includes the cold junction. [2]
Endress+Hauser notes that sleeve length, between process connection and terminal head, sets the head temperature, which must stay within the head's operating limits. [1]
05
Thermocouple assemblies listed by Silver Automation, and the certificate questions to settle
Silver Automation lists thermocouple assemblies alongside RTD sensors and industrial thermocouples; the questions below are what to settle with it, or any other supplier, before ordering.
Ask any supplier for the thermocouple type and tolerance class with test certificate, the thermowell material and its temperature limit, insulation resistance at temperature, response time as assembled, and spare insert availability.
Also ask whether the tolerance is certified to IEC 60584-1 class or to ASTM E230 standard or special limits, the thermowire diameter, and the ceramic grade with the temperature limit the supplier applies to it. [2][3]
06
Insert, ceramic insulator, outer thermowell, support tube, process connection, head and transmitter
WIKA's TC80-H shows how the rows fit together: a Ø 24 mm ceramic thermowell cemented into a Ø 32 mm metal support tube, with the cold junction inside the head transmitter. [2]
Part
Role
Fix in the order
Thermocouple insert
Generates the EMF; type, class, wire diameter. [1][2]
Type, class, single or double, wire Ø.
Inner ceramic insulator
Insulates wires; tubes for K/N, rods for R/S/B. [2]
Carries the ceramic; 1.0305 to 550 °C, 1.4841/446/310 to 1,150 °C in air. [2]
Length and material.
Process connection
Stop flange or fitting; gas-tight to 1 bar. [1][2]
Type and pressure rating.
Head and transmitter
Terminal or 4–20 mA/HART/fieldbus; cold junction in transmitter. [1][2]
Head, transmitter, cable.
07
Temperature range, tolerance class, sheath, immersion length, response time and insulation for a furnace thermocouple
Read the sheath material row with the ceramic limits above: Endress+Hauser gives C799 1,800 °C and WIKA 1,600 °C, so ask which limit applies to the thermowell quoted. [1][2]
1 company lists this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
Silver Automation Instruments
Manufacturing site to be confirmed for the order
Lists thermocouple assemblies with RTD temperature sensors and industrial thermocouples.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How accurate is a Type K thermocouple at 800 °C?
IEC 60584 Class 2 allows ±0.0075|t|, about ±6 °C at 800 °C (editorial calculation), per the table in Endress+Hauser's TAF information. [1]
Which ceramic thermowell suits the highest temperatures?
Endress+Hauser rates C799 (about 99.7% alumina) to 1,800 °C, C610 to 1,500 °C and C530 to 1,400 °C. [1]
Do ceramic thermowells need preheating?
Yes; for processes at 1,000 °C or more Endress+Hauser requires gas-tight ceramics to be preheated to 400 °C before installation. [1]
Is ASTM E230 special tolerance the same as IEC 60584 Class 1?
Not always: for Types R and S ASTM special is ±0.6 °C or ±0.1%, while IEC Class 1 is ±1 °C to 1,100 °C and ±[1 + 0.003(|t| − 1,100)] above; for Type K both standard grades are 0.75%. [4][1]
Which thermocouple types work above 1,200 °C?
WIKA states only precious-metal Types R, S and B can be used above 1,200 °C, preferably in gas-tight high-purity C 799 ceramic. [2]
Sources and what still needs a direct check
Sources checked 2026-10-12. Endress+Hauser and WIKA are process instrument makers whose data describe their own high-temperature thermometers; the IEC and ASTM pages are publisher summaries, and the ASTM E230 tolerance values are from Pyromation's reproduction of its Table 1.