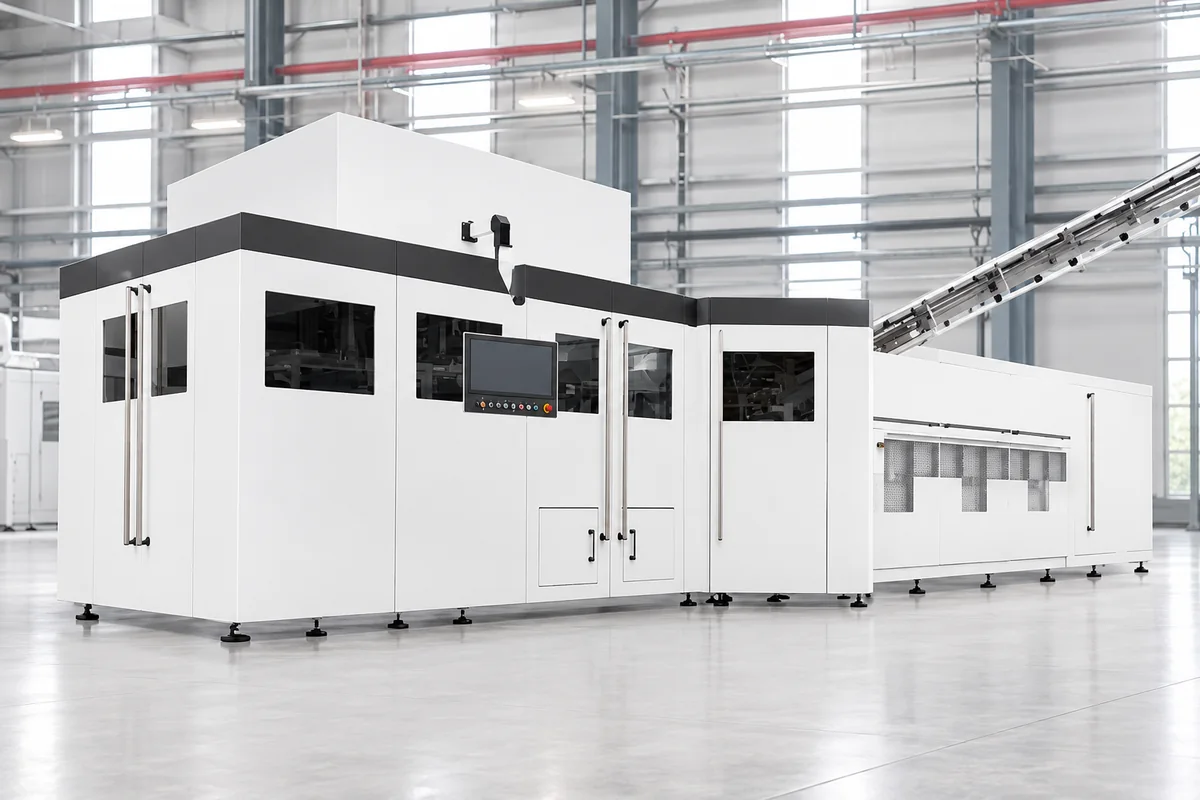
Blow moulding machines for bottles and containers · PET stretch blow vs extrusion blow, output in bottles per hour, preform heating, rPET, hot-fill, container size and energy use
A blow moulding machine forms hollow containers by inflating hot plastic inside a mould: stretch blow moulders reheat PET preforms and stretch-blow them into bottles, while extrusion blow moulders extrude a molten parison and blow it into containers such as canisters and jugs. Ask three things first: which material and container — PET bottles or extruded polyolefin containers, and what size; what output in containers per hour the line needs; and whether the bottle is for still, carbonated, hot-fill or aseptic products, since that changes the process and mould heating.
Stretch blow moulders for PET and rPET bottles (rotary and linear, stand-alone or blow-fill-cap blocks), and extrusion and injection blow moulding machines for plastic containers. Film blowing lines, preform injection moulding machines and complete filling lines are outside this page except where compared.
CNFX editorial research · Sources checked October 11, 2026 · 4 sources
SMI's rotary stretch blow moulders produce PET, rPET and PP containers at up to 55,000 bottles per hour and can be integrated with fillers and cappers in a single ECOBLOC block. [1] Sidel's EvoBLOW stretch blow range covers transparent and opaque PET, up to 100% recycled PET and refillable PET, with over 200 configurations, an aseptic version with dry preform sterilisation, an eHR version with electrical mould heating for hot-fillable and pasteurisable bottles, a preferential-heating version for food, home and personal care containers, and an XL version for PET bottles up to 10 L. [2]
For extruded containers, Bekum's all-electric EBLOW 508–708 extrusion blow moulders make containers up to 10 L such as canisters and large pharmaceutical or cosmetic packs, with mono- or multilayer spiral-mandrel heads for EVOH barrier, view stripes or recycled (PCR) content, including a three-layer construction for recycled material or fillers such as chalk. Bekum says IE5 motors and its HiPEx 36D extruder cut energy use by up to 20%. [4]
Editorial calculation: 55,000 bottles per hour is about 917 per minute, or roughly 15 every second. [1]
Give the supplier the container drawings (volume, neck finish, weight, shape), material (PET, rPET, HDPE, PP; layers), product filled (still, carbonated, hot-fill, aseptic), target output per hour, number of moulds and format changes, preform supply or integrated preform/parison production, integration with filling and capping, compressed-air supply and recovery, power supply, floor space, and quantity of moulds and machines.
02
Control preform heating, weight and rPET
Sidel says its EvoBLOW Laser oven replaces halogen heating with up to 36 heating lines against 10 heating zones for halogen, placing material only where needed for an average 10% container weight reduction, and cites 16 g for a 1.5 L bottle and 4.8 g for a 0.5 L concept bottle. It claims 50% less preform waste from a shorter oven, no warm-up or cool-down time, about one minute less downtime per stop and start, consistent quality regardless of surrounding temperature, one intensity setting per heating line for rPET variation, and laser diodes with an estimated 20-year life. [3]
Editorial calculation: 16 g for a 1.5 L bottle is about 10.7 g per litre of capacity; a 10% weight reduction on a 20 g bottle would save 2 g per bottle, or about 110 kg an hour at 55,000 bottles per hour. [3][1] Editorial note: lightweighting figures are the maker's claims for its own process and bottle designs; ask for trials on your preform and bottle.
03
Compare what suppliers offer
Suppliers linked to this page list blow moulding machines; each card links to the page reviewed.
Listings include automatic and semi-automatic PET stretch blow moulders, multi-cavity servo blowers, 5-gallon bottle blowers, blow-fill-cap blocks, extrusion blow moulders and injection blow moulders for LED bulb housings; ask each for output per cavity, maximum container volume, air consumption at your blow pressure, and power use.
04
Trace the machine construction
This is a functional reference built from the sources cited; it is not one maker's specification.
Fill the specification fields with values for your line
A blow moulding machine quotation needs values for your containers. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 11 October 2026
SMI lists rotary stretch blow moulders for PET, rPET and PP containers at up to 55,000 bottles per hour. [1]
What size containers can blow moulders make?
Sidel's EvoBLOW XL makes PET bottles up to 10 L, and Bekum's EBLOW 508–708 extrusion blow moulders make containers up to 10 L. [2][4]
Can a blow moulder run 100% recycled PET?
Sidel says its EvoBLOW range handles up to 100% rPET. [2][3]
Sources and what still needs a direct check
Sources checked 2026-10-11. SMI, Sidel and Bekum build blow moulding machines and describe their own ranges; lightweighting and energy figures are their claims. The Bekum page reviewed is in German.