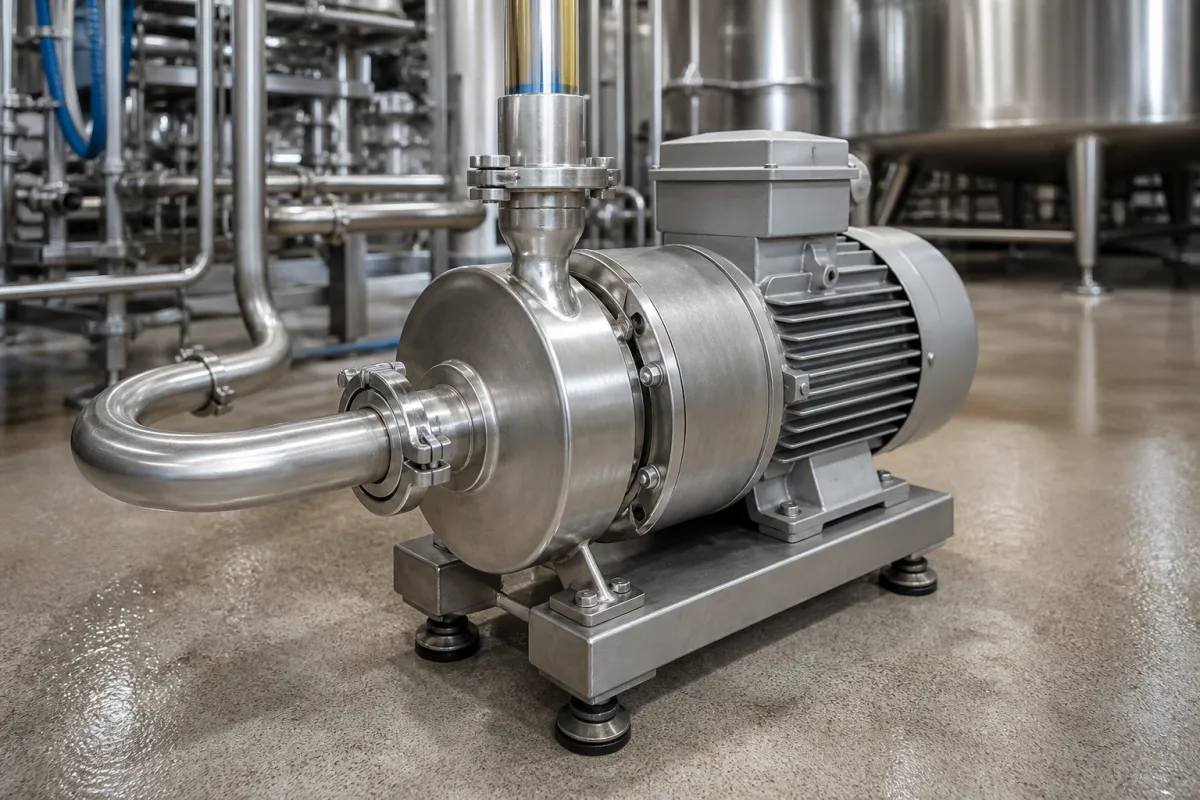
CIP supply pump on hot caustic duty: suction head lost to vapour pressure at 80–95 °C, wash temperatures it must deliver, and the ratings to check
The hygienic centrifugal pump that pushes hot caustic and acid from the CIP tanks out to the circuits · checked less on flow, which the circuits set, than on whether its suction still works when the solution is at 80 °C and on its temperature, pressure and SIP ratings
The supply pump on a CIP set draws solution from an atmospheric tank and pushes it through the plant: pipework, heat exchangers and tank spray devices. Its flow is set by the velocity the largest line needs and its head by the circuit and spray devices. What is easy to miss is the suction side. A pump that runs quietly on cold rinse water can cavitate on the hot caustic step of the same cycle, because between 80 and 95 °C half or more of the atmospheric pressure that pushes liquid into the impeller is used up by the solution's own vapour pressure.
Hygienic centrifugal pumps used as CIP supply pumps on hot detergent duty: suction head available at wash temperature, wash temperatures and caustic strengths by equipment type, and the pump's operating, sterilisation and pressure ratings. Sizing CIP supply flow from line velocity and choosing self-priming return pumps are covered on the CIP circulation pump page; complete CIP skids on the CIP (clean-in-place) system page; combined CIP and SIP units on the Automated CIP/SIP system for beverage lines page; and large bare-shaft hygienic pumps on the High-flow hygienic centrifugal pump on a baseplate page.
CNFX editorial research · Sources checked October 13, 2026 · 3 sources
Vapour pressure eats the suction head: 2.3 kPa at 20 °C, 51 kPa at 82 °C and 85 kPa at 95 °C
NIST lists Antoine equation parameters for water, log10(P) = A − B/(T + C) with P in bar and T in kelvin, from Bridgeman and Aldrich's data: A = 5.40221, B = 1838.675, C = −31.737 for 273–303 K and A = 5.08354, B = 1663.125, C = −45.622 for 344–373 K. [1]
Editorial calculation: head = (101.3 kPa − vapour pressure) ÷ (ρ × g), taking densities of about 998, 970 and 962 kg/m³ at the three temperatures (assumed values, not from the cited sources) and a sea-level atmosphere; the last column adds a 1.5 m liquid level and subtracts 0.5 m of suction pipe loss, both assumptions for illustration. Treating detergent as water is also an assumption; dissolved caustic and entrained air change the figures. [1]
Editorial note: the NPSH a pump needs rises with flow, so the hot caustic step at full CIP flow is the point to check on the pump curve. Keeping the tank outlet short and wide, keeping a liquid level above the pump, or lowering the wash temperature where the cleaning guide allows are the levers; a pump selected only on the cold-water duty point may not have that margin.
Solution temperature
Vapour pressure of water (Editorial calculation from the NIST parameters)
Head from atmospheric pressure less vapour pressure (Editorial calculation)
With 1.5 m of liquid above the pump and 0.5 m of suction loss (assumed)
Give the hottest step temperature, the minimum liquid level in the CIP tank above the pump, the suction pipe length and diameter, the site altitude, and ask for the pump's NPSH required at the full CIP flow.
02
The washes the pump has to deliver: 135–150 °F on cold surfaces up to 1.5–4.0 % caustic in evaporators
Hydrite's cleaning guide ties caustic strength, flow, temperature and time to what the equipment does to the soil; heat-treated product is harder to remove than soil from cold surfaces. [2]
For a milk evaporator Hydrite warns that the first caustic wash should not exceed 0.75 %, because a stronger first wash can turn the milk protein into an orange rubbery gel; the second wash then goes to 1.5–4.0 %. [2] Editorial calculation: the pasteuriser flow rule of process flow plus 10 % means a CIP supply pump serving a 20 m³/h HTST has to deliver at least 22 m³/h through that circuit, at 77–82 °C, which is the hot-suction case in the section above.
Equipment
Caustic
Flow
Temperature (°C by Editorial calculation)
Time
Cold or ambient surfaces: silos, transfer lines
0.40–0.75 oz/gal of caustic CIP cleaner
At least 5 ft/s through the largest flow path, or the equipment maker's minimum
List each circuit the pump serves with its equipment type, required CIP flow, hottest wash temperature and caustic strength.
03
Ratings to check against the cycle: 95 °C in operation, 140 °C for SIP, PN 16, and 77 m at 50 Hz becoming 110 m at 60 Hz
GEA lists the HYGIA single-stage hygienic centrifugal pump, which it describes as CIP and SIP capable and self-draining when installed vertically, with these limits: [3]
Editorial calculation: 110 ÷ 77 ≈ 1.43, close to (60 ÷ 50)² = 1.44, which is what the pump affinity laws predict when the same pump runs 20 % faster on 60 Hz supply; a frequency converter uses the same relation to trim one supply pump to circuits that need different flows and heads. [3]
Editorial note: the 95 °C operating limit sits just above the hottest washes in Hydrite's table, and the 140 °C rating applies to sterilisation, not to continuous pumping; if the cycle includes hot water or steam sterilisation through the pump, state its temperature and duration. [3][2]
Close-coupled with plug-in shaft (K, up to 22 kW), with bearing bracket and coupling (Adapta), stainless motor shrouds (SUPER), built-in frequency converter (tronic, up to 22 kW), ATEX categories 2 and 3 [3]
State supply frequency or whether a frequency converter is wanted, the maximum pressure in the circuit, the hottest CIP step, and any SIP step through the pump with its temperature and time.
04
What to send for a CIP supply pump
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Circuits: [each circuit's flow and head; largest line size]
Washes: [caustic and acid strength; hottest temperature]
Suction: [tank type; minimum level above pump; suction line; altitude]
Ratings: [operating temperature; SIP temperature and time; pressure class]
Drive: [50 or 60 Hz; frequency converter]
Hygiene: [certificates; self-draining installation; seal type]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Why does a CIP supply pump cavitate on the hot caustic step?
Water's vapour pressure rises from 2.3 kPa at 20 °C to about 51 kPa at 82 °C on NIST's Antoine parameters, so the suction head available from atmospheric pressure falls from about 10 m to about 5 m (Editorial calculation). [1]
How hot are caustic CIP washes for pasteurisers?
Hydrite's guide gives 1.0–2.0 % caustic as NaOH at 170–180 °F (77–82 °C), 10 °F above processing temperature, for 45–60 minutes. [2]
What temperature can a hygienic CIP pump take?
GEA rates its HYGIA pump to 95 °C in operation (150 °C on request) and 140 °C for SIP, at PN 16. [3]
Sources and what still needs a direct check
Sources checked 2026-10-13. Vapour pressure parameters are from the NIST Chemistry WebBook; wash parameters from Hydrite's 'Are You Aware' guide on caustic concentrations (May 2023); pump ratings from GEA's HYGIA product page.