Aluminium fabrication · Single or double head, blade diameter, tooth pitch and rake, cutting speed and clamping
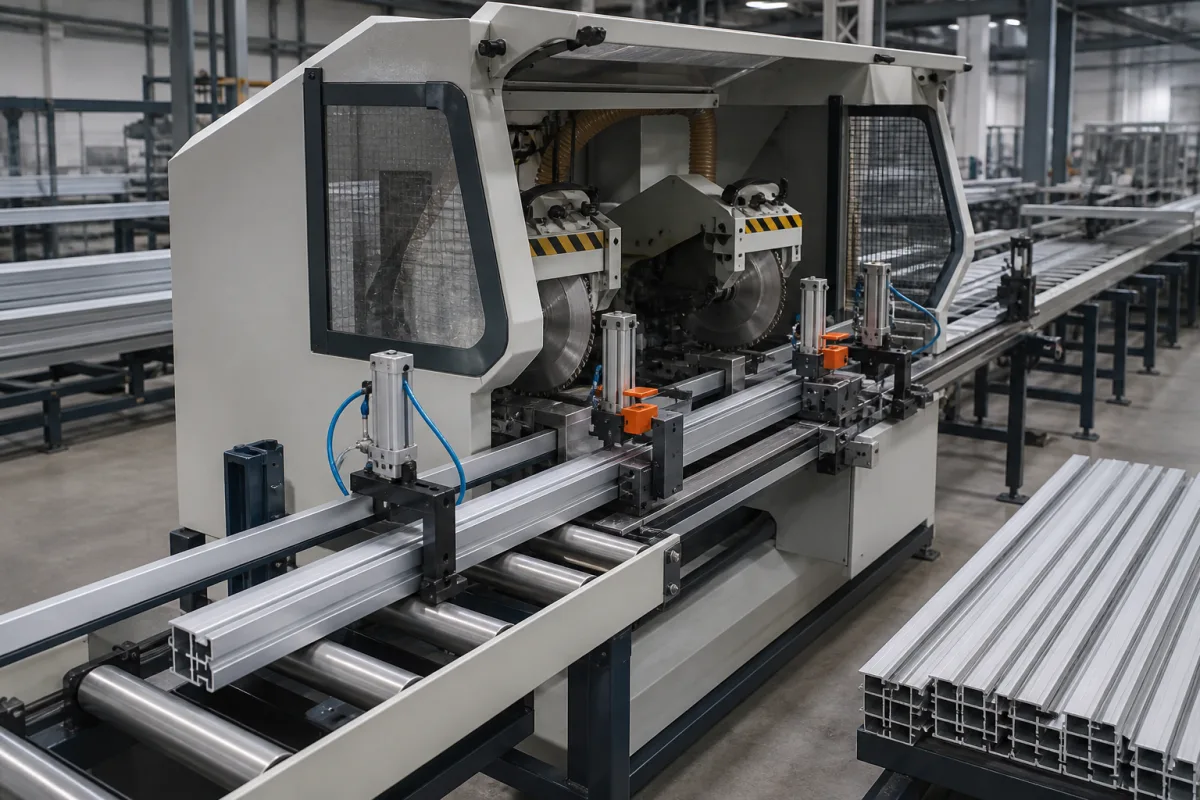
An aluminium profile cutting machine saws extrusions to length and angle with a carbide-tipped circular blade, on one saw head or two. Ask three things first: the profiles, lengths and angles you cut, the blade diameter, tooth pitch and spindle speed it runs, and the clamping, feeding and length measurement that set accuracy.
Circular saw machines for aluminium and other non-ferrous profiles: single-head, double-head mitre, up-cut, corner-connector and CNC automatic saws for windows, curtain walls and industrial profiles. Band saws for steel, punching machines and CNC profile machining centres are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 4 sources
Choose single-head or double-head, and the blade size
DEMAC's aluminium cutting range describes double-head machines with 450–600 mm blades in what DEMAC calls CNC, precision and “Common” types, cutting at 45° and 90° or by up-cutting, and single-head saws with 420–600 mm blades that can cut any angle, 90° or 45°/90°, which can be combined with automatic or CNC stoppers for feeding and positioning. Blades are special carbide-tipped (TCT) or diamond blades for aluminium profiles. [2]
Single-head saws can be combined with automatic or CNC stoppers for feeding and positioning, and corner-connector saws are a separate type. [2] For a double-head saw, ask how the second head is positioned for each length and angle, and choose by your profile cross-sections, length range, angles and batch sizes.
One maker's data for a CNC double-head mitre saw (Jinan JMD, LJJ2DS-500×4200) give an example of the published figures: 500 mm blades (500 × 4.4 × 3.6 × 30 mm, 120 teeth) at 3,000 rpm, 9.5 kW input power on 380 V three-phase 50 Hz, 0.5–0.8 MPa air, cutting length 320–4,200 mm at 90° and 45°, maximum cut 138 mm wide by 290 mm high, rack-driven moving head with 0.02 mm stated repeat positioning accuracy, blade feed by hydraulic damping cylinder on linear guides, 5,950 × 1,750 × 1,500 mm overall and 1,900 kg. [3]
Give the supplier the profile drawings and alloys, maximum width and height, length range, cut angles, batch sizes, accuracy needed, blade diameter, feeding and length measurement, dust and chip extraction, noise limits and power supply.
02
Set the blade: tooth pitch, rake and cutting speed
Hoffmann's carbide-tipped TextFlow 12 aluminium saw blade data sheet recommends fine tooth pitch for thin-walled profiles or plates up to 5 mm, medium pitch for profiles and tubes over 5 mm, and coarse pitch for solid bars; a 6° negative rake for machines with oscillating blade infeed from above; trapezoidal teeth for hard-anodised profiles; and an even feed rate to prevent damage. A 300 mm blade has 96 teeth at 9.8 mm pitch. [1]
The same sheet gives two cutting speeds that do not agree: a note recommends 40–80 m/s, while its user-data table lists 850 m/min (about 14 m/s) for short-chipping aluminium and 650 m/min for alloys with over 10% Si. [1]
Editorial calculation: spindle speed n = cutting speed ÷ (π × diameter). For the 300 mm blade, 850 m/min gives about 900 rpm, while 40–80 m/s gives about 2,550–5,090 rpm. [1] Because the figures differ by a factor of about 3 to 6, confirm the blade's speed rating and the saw's spindle speed with both makers before ordering.
Editorial calculation: the JMD saw's 500 mm blade at 3,000 rpm runs at π × 0.5 m × 3,000 ÷ 60 ≈ 79 m/s, inside the 40–80 m/s note on the Hoffmann sheet and far above its 850 m/min table value. [3][1]
03
Check an automatic-feed saw for short parts
For batches of short parts cut from bar, a third design replaces the operator's push-and-stop with a servo feed. Samdy's CNC-405 specification lists a 405 mm (16-inch) carbide blade of 25.4 mm bore, 3.2 mm kerf and 80 teeth, a 4 kW saw motor and 4 kW hydraulic unit on 380 V, 0.6–0.8 MPa air, a maximum cut of 280 × 120 mm and an 800 mm table. Feed is by servo motor, ball screw and 25 × 25 mm linear guide over a 300–850 mm feeding stroke. [4]
Samdy states cutting accuracy of 0.1 mm, position-rule accuracy of ±0.1 mm, cut perpendicularity of ≤0.1 mm and a minimum last piece of 30–40 mm, which sets the offcut left from each bar. The table gives pneumatic clamping with adjustable pressure, while one paragraph on the same page describes hydraulic clamping, so confirm which is fitted. The machine measures 2,550 × 1,200 × 1,400 mm and weighs 300 kg. [4]
Editorial calculation: tooth pitch = π × 405 mm ÷ 80 teeth ≈ 15.9 mm, against 9.8 mm for the 300 mm, 96-tooth Hoffmann blade; ask which pitch the saw maker fits for your wall thickness. [4][1]
Double-head window saws and servo-feed automatic cutters among the listed makers
DEMAC, Bluetek, Haikai, JMD and Yidao list single- and double-head aluminium cutting saws with other window and door machines; Samdy and Ruiguang list automatic aluminium cutting machines with CNC servo feeding; North Jinfeng lists a CNC aluminium cutting machine alongside its band saws.
05
Saw head, blade infeed, clamps, length stop and chip extraction
The infeed direction ties the machine to the blade: Hoffmann specifies its 6° negative rake for machines whose blade comes down into the profile from above, so state the infeed before ordering blades. [1]
Sets length and position; rack-driven moving head in one CNC saw. [2][3]
Stopper, servo feed, accuracy.
Guarding and extraction
Encloses blade; removes chips.
Guards and chip extraction.
06
Cutting length, capacity at each angle, blade diameter and spindle speed for a saw quotation
The spindle-speed row is where published figures disagree: the JMD saw's 500 mm blade at 3,000 rpm runs about 79 m/s, inside the 40–80 m/s note on Hoffmann's sheet but far above its 850 m/min table value, so ask which speed the fitted blade is rated for. [3][1]
Field
What it means and published values
Ask the supplier for
Cutting length (mm)
Length range between heads; e.g. 320–4,200 mm on one double-head saw. [3]
Minimum and maximum length.
Cutting capacity (mm)
Profile width and height at each angle; e.g. 138 × 290 mm. [3]
8 companies list this product among what they make. Company figures are quoted from each
company's own website; every card states where the relationship came from.
DEMAC
Manufacturing site to be confirmed for the order
Lists single-head, double-head, up-cut and corner-connector aluminium saws.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Single-head or double-head aluminium saw?
Double-head saws carry two saw heads, with 450–600 mm blades in one published range; single-head saws can be combined with automatic or CNC stoppers for feeding and positioning. [2]
Which tooth pitch suits thin profiles?
Hoffmann recommends fine pitch for walls up to 5 mm and medium pitch above 5 mm. [1]
Why use a negative rake blade?
Hoffmann specifies a 6° negative rake for machines where the blade feeds into the profile from above. [1]
What blade speed does a double-head aluminium saw run at?
One maker's 500 mm blade turns at 3,000 rpm, about 79 m/s at the rim (editorial calculation). [3]
What is the shortest offcut on an automatic aluminium saw?
Samdy lists a minimum last cutting length of 30–40 mm for its CNC-405 servo-feed saw, with ±0.1 mm positioning accuracy. [4]
Sources and what still needs a direct check
Sources checked 2026-10-12. Hoffmann Group is a tool supplier; its blade data sheet is used as a worked example. DEMAC, Jinan JMD and Foshan CNC Samdy are suppliers listed on this page; their product data are cited as examples of published figures, not endorsements.