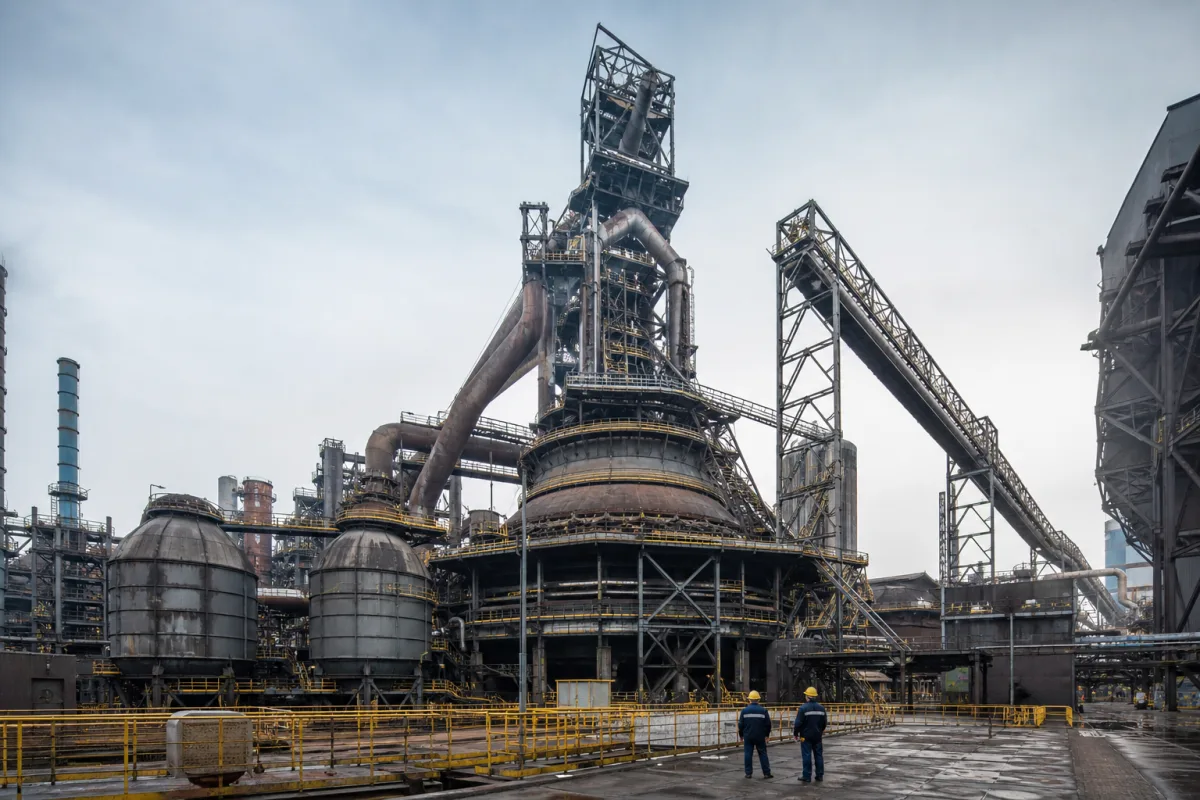
Ironmaking blast furnace: shell, hearth, bosh and stack · Inner volume, hearth diameter, tuyeres and tapholes, copper and cast-iron staves, hearth refractory and campaign life, casting through tapholes and slag runners, top gas cleaning, hot stoves and slag granulation
A blast furnace is the refractory-lined shaft furnace of an integrated steelworks in which iron ore, pellets or sinter, coke and flux charged at the top are reduced by hot air blown through tuyeres near the bottom, so that molten iron and slag collect in the hearth and are cast through tapholes while the top gas is collected, cleaned and burned as fuel. Ask three things first: what hot-metal output and inner volume the furnace must have, how the hearth, bosh and stack will be cooled and lined for the campaign life you need, and which casthouse, top-charging, hot-stove, gas-cleaning and slag-handling plant is in the scope.
Ironmaking blast furnaces and their structural parts: shell, hearth, bosh, stack, lining, stave and plate cooling, tuyeres, tapholes and slag notches, top charging, casthouse, top-gas cleaning, hot stoves and slag granulation where supplied with the furnace. Basic oxygen furnaces (see basic oxygen furnace vessel), direct-reduction shaft furnaces (see direct reduction shaft furnace), electric arc furnaces and ladles are outside this page except where compared.
CNFX editorial research · Sources checked October 11, 2026 · 4 sources
Size the furnace from hot-metal output, volume and openings
US EPA AP-42 describes the blast furnace as a large refractory-lined furnace charged at the top with ore, pellets or sinter, flux and coke, in which the charge reacts with the blast air to form molten iron, carbon monoxide and slag that collect in the hearth while by-product gas leaves through offtakes at the top. It gives the inputs for 1 ton of iron as 1.4 tons of iron-bearing material, 0.5–0.65 tons of coke, 0.25 tons of limestone or dolomite and 1.8–2 tons of air, with 0.2–0.4 tons of slag and 2.5–3.5 tons of blast furnace gas as by-products. [1]
AIST reports that the blast furnace rebuilt by Paul Wurth at NLMK's Lipetsk plant has a hearth diameter of 12.0 m, an inner volume of 3,818 m³, 32 tuyeres and four tapholes, and is designed for a nominal 3.4 million tons of hot metal per year; the contractor supplied the shell, hearth lining and refractories, the cooling system with copper and cast-iron staves, copper cooling boxes, tuyeres and tuyere coolers and pumphouse, tuyere stocks, a bustle pipe and a parallel-hopper bell-less top. Nippon Steel states that seven of its 13 blast furnaces have an inner volume above 5,000 m³. [2][3]
Editorial calculation: 3.4 million t/y ÷ 3,818 m³ ≈ 890 t of hot metal per m³ of inner volume per year, or about 2.4 t/m³ per day over 365 days; and at 1.4 t of iron-bearing material and 0.5–0.65 t of coke per tonne of iron, that output implies roughly 4.8 Mt/y of iron-bearing material and 1.7–2.2 Mt/y of coke to receive and charge. Both assume the nominal output is reached. [2][1]
Give the supplier the hot-metal output and quality, burden (sinter, pellets, lump ore) and coke and injectant rates, required inner or working volume, hearth diameter, number of tuyeres and tapholes, blast volume, temperature and oxygen enrichment, top pressure, campaign life, site layout and what is to be reused from an existing furnace.
02
Set the cooling and lining for the campaign life
Nippon Steel reports that it raised the number of basic cooling pipes in cast-iron shaft staves from six to nine, at intervals under 100 mm, and added a second serpentine pipe; from 2003 it introduced copper staves in the middle and lower shaft, later with protruding ribs — its off-line test found that "the rib pitch with which the burden descent at the rib edge was slowest was roughly 40 mm" and that "a rib height of 5 mm was considered sufficient" — with hard-faced edges so that a stationary burden layer forms on the work surface and reduces wear. [3] It also inserts cooling plates and bars through the lower bosh just above the tuyeres to hold the bosh profile once the bosh bricks wear away. [3]
The same report says that "the BF campaign life is determined mainly by hearth refractory, or the bricks of the hearth wall and bottom", whose service life "is defined mainly by the wear by erosion and breakage due to degradation and embrittlement"; controlling the level of the dead-man coke through blast volume, oxygen and coke rate limited hearth brick damage at Wakayama No. 5 blast furnace, which reached a 31-year campaign when blown out in 2019. [3] NLMK expected its rebuild to extend the inter-repair cycle by 50% to 25 years. [2]
Hot stoves heat the blast air: a combustion chamber burns fuel gas and the hot gas heats checker bricks in a regenerator that then heats the blast, so the checkers see repeated temperature change; Nippon Steel has introduced top-combustion stoves to raise blast temperature. [3]
State the stave material and layout by zone (hearth, bosh, belly, shaft), cooling plates or bars, cooling-water system and flow, hearth and bottom refractory design and monitoring (thermocouples), burden profile measurement, stave and tuyere replacement method, and the campaign life the design is based on.
03
Plan casting, slag handling and top gas cleaning
AP-42 describes casting as drilling a taphole into the clay-filled iron notch at the base of the hearth so that molten iron runs along runners to transport ladles while slag is diverted through separate runners to a slag pit by the casthouse or into slag pots; the taphole is then replugged with clay, and the casthouse encloses the area around the base of the furnace with all its runners. [1]
The FHWA slag manual states that blast furnace slag is about 20% by mass of iron production and describes the cooling routes: slow air cooling in beds gives crystalline lump slag; controlled water, air or steam gives expanded slag; water and air quenching in a spinning drum gives pellets; and rapid water quenching to a glassy state gives granulated slag, which can be ground for use as a cementitious material. [4]
Top gas has a low heating value of about 2,790–3,350 J/L (75–90 Btu/ft³). AP-42 describes a settling chamber or dry cyclone removing about 60% of the particulate, a wet scrubber removing about 90% of the remainder, and a venturi scrubber or electrostatic precipitator removing up to 90% of what is left, giving fuel gas below 0.05 g/m³, part of which fires the hot stoves. [1]
Editorial calculation: the three published stages in series leave 0.40 × 0.10 × 0.10 = 0.4% of the raw dust, i.e. about 99.6% removal, assuming each stage reaches the efficiency AP-42 gives. [1]
Define the casthouse layout, taphole drills and mud guns, iron and slag runners, ladle or torpedo car positions, slag route (granulation, pelletizing, air-cooled pits), top-gas dust catcher, scrubber or precipitator, gas holder connection and emission limits.
04
Hearth to top, then stoves, gas cleaning and slag plant
Rows run from the hearth upward through the bosh and stack to the top, then to the plant built around the furnace.
Part
Role
Fix in the order
Hearth
Collects molten iron and slag; its refractory sets campaign life. [1][3]
Dust catcher, scrubber or precipitator for top gas. [1]
Stages, outlet dust.
Slag treatment
Air cooling, pelletizing or water granulation. [4]
Route and product.
05
Volume, hearth, openings and shell values for the enquiry
Output, burden and site data come from your production plan. Eight of the twelve rows have no published value in these sources; those figures must come from the designer.
Field
What it means and published values
Ask the supplier for
Effective volume (m³)
3,818 m³ inner volume on one rebuilt furnace; above 5,000 m³ at seven Nippon Steel furnaces. [2][3]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What sets the campaign life of a blast furnace?
Nippon Steel reports that "the BF campaign life is determined mainly by hearth refractory"; one of its furnaces reached a 31-year campaign. [3]
How is iron tapped from a blast furnace?
A taphole is drilled into the clay-filled iron notch; iron and slag run along separate runners, then the hole is replugged with clay. [1]
Why are copper staves used in the shaft?
For cooling capacity and wear resistance in the high heat-load middle and lower shaft, with ribs that hold a burden layer. [3]
What happens to blast furnace slag?
It is air-cooled, expanded, pelletized or water-granulated; granulated slag can be ground for cementitious use. [4]
Sources and what still needs a direct check
Sources checked 2026-10-11. AP-42 and the FHWA manual are US government references; the AIST note reports one contractor's rebuild; Nippon Steel's report describes one steelmaker's practice. Design values for your furnace must come from the designer offered.