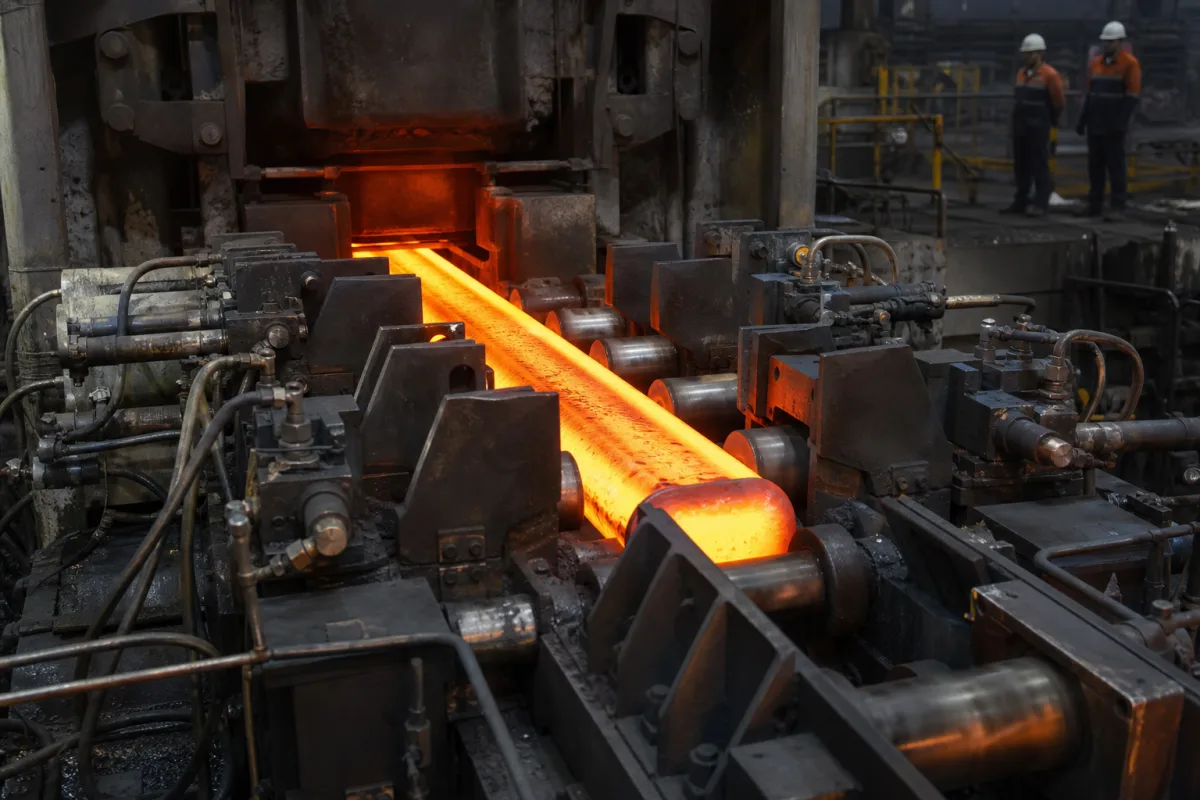
Strand guide system for continuous casters: roller segments, roll pitch and cooled guide rolls
Continuous caster strand guide · Roller segments, roll pitch and bulging, servo roll-gap adjustment for soft reduction, and internally cooled split rolls
A continuous caster strand guide is the run of roll pairs that supports the strand after it leaves the mould, while its shell is still thin and its core liquid: rolls are grouped into segments, the gap between upper and lower rolls is set, and where soft reduction is used it is narrowed near the end of solidification. Ask three things first: what roll pitch and diameter the guide uses against the bulging the strand will see, how each segment sets and changes its roll gap, and how the rolls are cooled, supported and replaced.
Strand guide segments, guide rolls and their bearings, cooling and roll-gap adjustment for slab, bloom and billet continuous casters, from below the mould to the straightener. Mould oscillation tables and drives are covered on the Heavy-duty continuous casting mold oscillator page. Web guide systems for converting lines, linear guide rails for machine tools and parking guidance systems are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
Brian Thomas's Continuous Casting Consortium describes bulging below the mould as caused by ferrostatic pressure on the solidifying shell, and directly responsible for internal cracks, centreline segregation and permanent deformation; it also raises roll loads and wear. Its finite-element case used a 1,350 mm slab, 860 mm roll pitch, 79 mm shell, 1,500 °C liquidus and 1,000 °C surface temperatures, 3.9 m below the meniscus with 0.26 MPa ferrostatic pressure, cast at 0.85 m/min (14.2 mm/s). [1]
The model gave a non-symmetric bulge with its maximum about 65% of the way from the upstream roll, found that creep has a significant effect while the temperature profile has a small one, and computed a maximum deflection of 5.7 mm on a coarse mesh and 6.2 mm on a finer one. [1]
Editorial calculation: 7,000 kg/m³ × 9.81 m/s² × 3.9 m ≈ 0.27 MPa, consistent with the stated 0.26 MPa. At 14.2 mm/s a point on the strand takes 860 ÷ 14.2 ≈ 61 s to pass one roll pitch, and the peak bulge sits about 0.65 × 860 ≈ 560 mm past the upstream roll. [1]
Give the supplier the caster type and radius, strand sizes (thickness and width ranges), casting speeds, steel grades, metallurgical length, the soft-reduction zone and reduction required, segment positions, roll pitch and diameter wanted, roll cooling water available, bearing and lubrication practice, and how segments will be changed and aligned.
02
Specify the segments, roll-gap adjustment and rolls
An SMS Schloemann-Siemag patent on strand guiding segments for slab casters (US 6,328,093 B1) states that groups of at least four roll pairs are combined into segments, the upper rolls mounted on the upper or detachable frame and the lower rolls on the lower frame. Soft reduction near the tip of the liquid phase needs a conical, variable opening during casting, set by four servo piston-cylinder units per segment adjusting the opening width in an infinitely variable manner. [2]
A Voest-Alpine patent now assigned to Primetals Technologies Austria (US 7,325,586 B2) notes that single-piece guide rolls can only be used on slab strands up to 900 mm wide and on bloom and billet sections, and proposes a central shaft carrying roll shells with coolant passages 10–40 mm below the shell surface, giving steady-state surface temperatures of 130 to 180 degrees in casting, so that only the wearing shells need replacing. [3]
Editorial note: on wide slab casters ask whether rolls are single-piece or split with intermediate bearings, how each shell is cooled, and which parts are replaced at a segment overhaul.
03
Choose between single-piece and shell rolls, fixed and servo-set segments
The two patents describe the roll and segment choices a caster buyer faces; the bulging case shows the load those rolls carry.
Choice
What the source states
Decide for your caster
Single-piece roll
Limited to slab strands up to 900 mm wide, blooms and billets; wear means replacing the whole roll. [3]
Strand width range.
Central shaft with cooled roll shells
Coolant bores 10–40 mm below the shell surface; only worn shells replaced. [3]
Cooling water supply; shell spares.
Segment of at least four roll pairs
Upper rolls on the upper or detachable frame, lower rolls on the lower frame. [2]
Segment length and change method.
Servo-set roll gap
Four servo cylinders per segment give a conical, variable opening for soft reduction. [2]
Gap range and position sensing.
Roll pitch
860 mm pitch with a 79 mm shell gave a peak bulge of 5.7–6.2 mm in the CCC model. [1]
Pitch against your shell and speed.
04
Send the caster, strand and segment data together
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
What causes bulging between caster rolls?
The Continuous Casting Consortium attributes it to ferrostatic pressure on the solidifying shell; its model case at 860 mm pitch peaked about 65% along the pitch. [1]
How many roll pairs are in a strand guide segment?
An SMS patent states at least four roll pairs per segment, with four servo cylinders setting the opening for soft reduction. [2]
How are strand guide rolls cooled?
A Primetals (Voest-Alpine) patent places coolant bores 10–40 mm below the roll shell surface, holding surface temperatures of 130–180 degrees in steady casting. [3]
Sources and what still needs a direct check
Sources checked 2026-10-12. The bulging case is from Brian Thomas's Continuous Casting Consortium; the two patents are by SMS and by Voest-Alpine (now Primetals Technologies Austria), read on Google Patents.